Top Track Choice
M10×1.25 Flanged Hexagon Titanium Sprocket Nut (Japanese Spec)
Gr5 Ti-6Al-4V · DIN 6923 / JIS
MOQ: 100 sets (500 pcs)
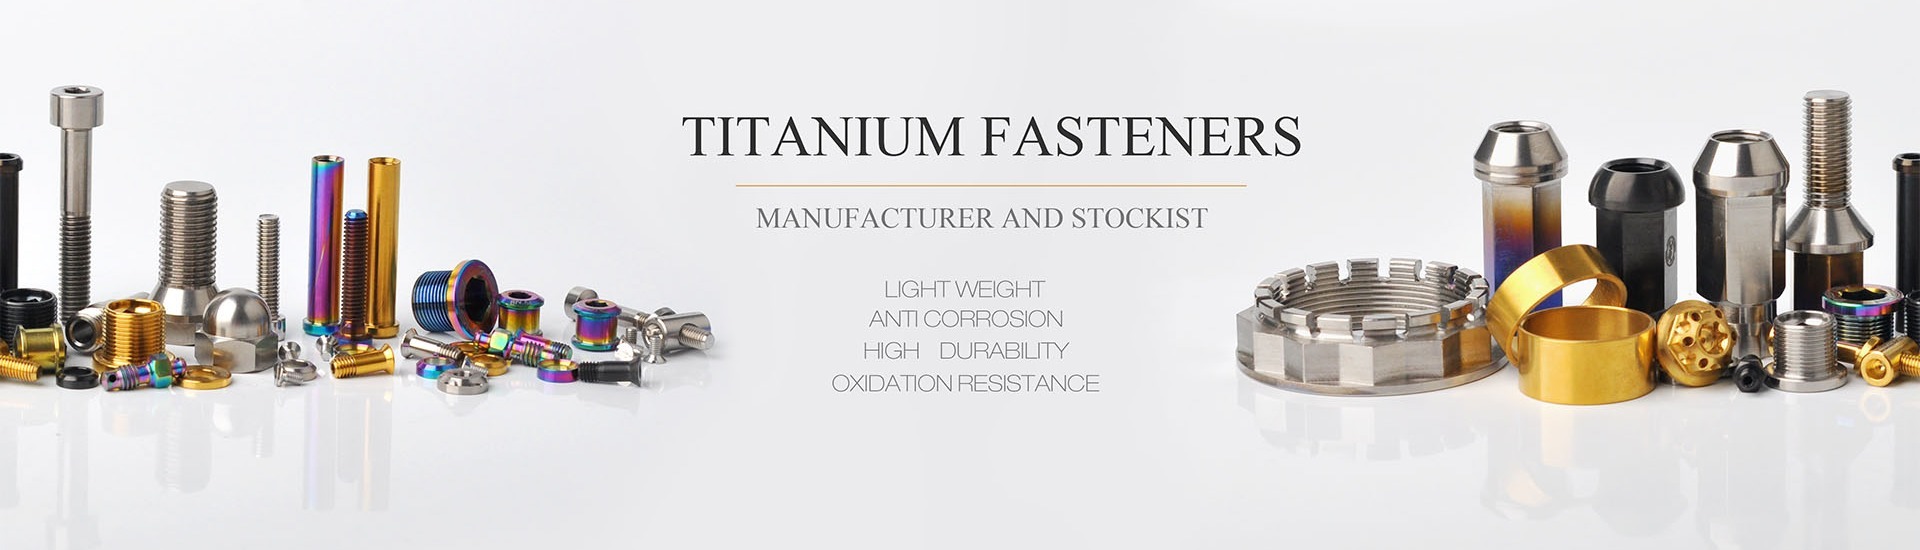
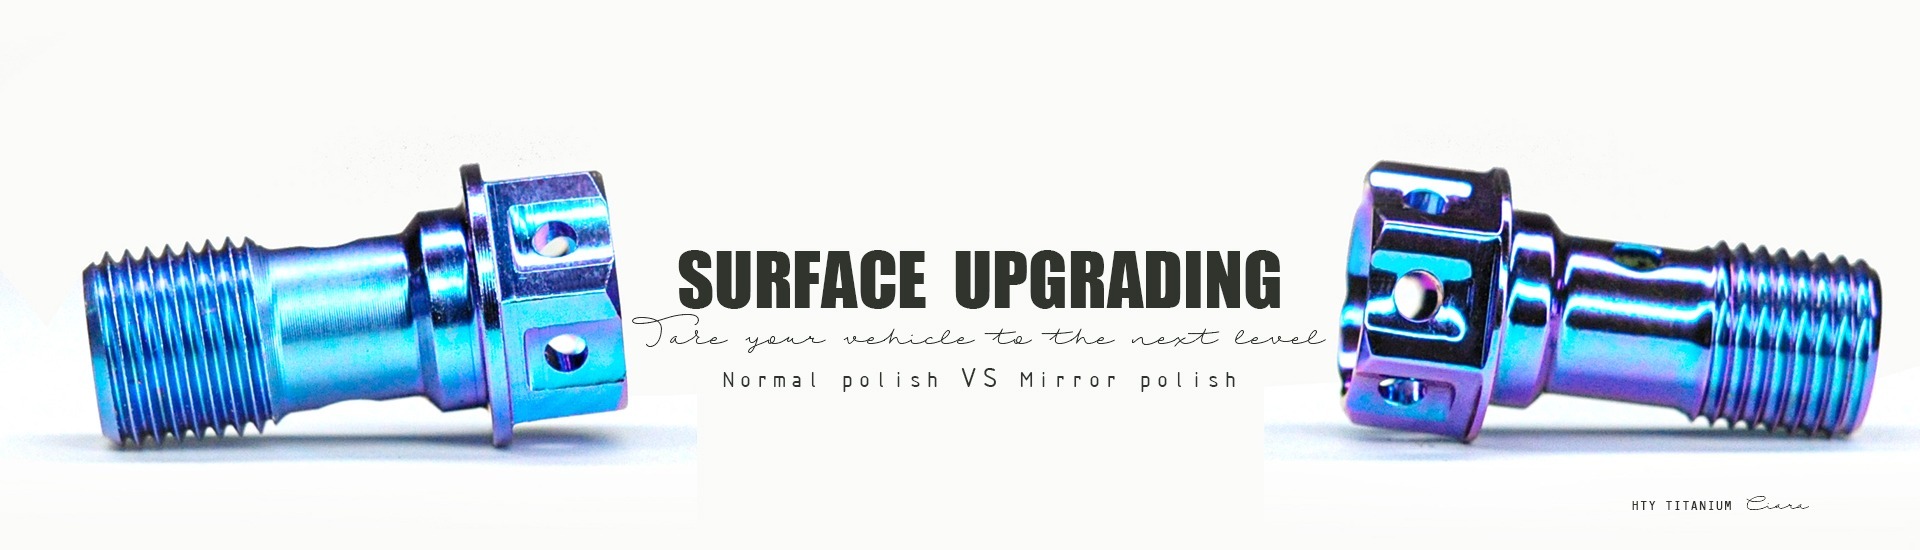
In motorcycle drivetrain engineering, rotational unsprung inertia dictates acceleration transient response, gyroscopic stability, and suspension compliance. Titanium Hexagon Sprocket Nuts precision-machined from Ti-6Al-4V Grade 5 (TC4) alloy replace OEM zinc-plated steel hardware to eliminate up to 44% of fastener mass while delivering yield strengths exceeding 880 MPa. Engineered with integral load-distributing flanges, friction-stabilized prevailing-torque collars, and rolled internal threads, these fasteners ensure fatigue-proof clamping on high-torque racing hubs across MotoGP, WorldSBK, motocross, and high-performance electric powertrains.
Multi-axis Swiss turning & thread rolling
Optical Go/No-Go thread pitch gauge checks
Bespoke heights, flange radii & safety lock holes
Real-time machining & CMM inspection videos
Express courier door-to-door with EN 10204 3.1 MTR
Configured for professional racing teams, tier-1 aftermarket distributors, and powertrain component builders. Each unit is precision-turned from certified Grade 5 aerospace titanium bar stock with friction-controlled finishes.

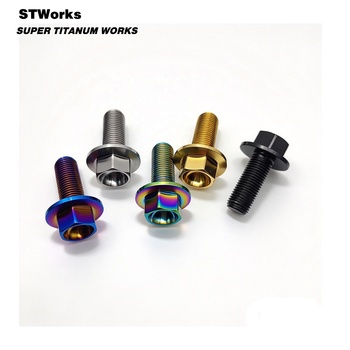
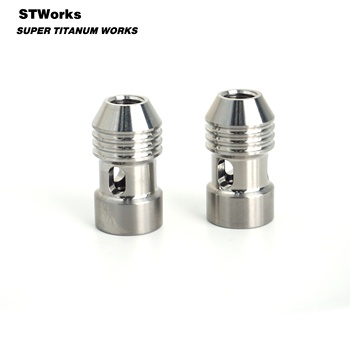
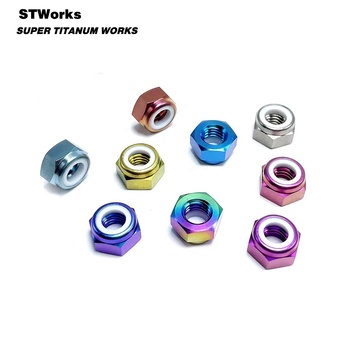
When a race motorcycle accelerates under full engine load, sprocket studs and nuts absorb tremendous shear forces and cyclically varying torque ripples. Discover why Grade 5 titanium represents the pinnacle of fastener engineering.
Rear sprockets reside at the outermost diameter of the wheel hub assembly. Fastener mass here acts not only as unsprung weight—directly degrading the rear shock absorber's high-frequency dampening ability over track curbs—but also as active rotational inertia. Reducing 100 grams of rotational mass at the wheel radius yields the dynamic kinetic equivalent of stripping roughly 200 grams of static chassis weight during aggressive corner-exit acceleration. Grade 5 titanium offers a density of 4.43 g/cm³, achieving an immediate 44% mass reduction compared to factory carbon steel (7.85 g/cm³).
| Density Ratio | 4.43 g/cm³ (Titanium) vs 7.85 g/cm³ (Class 10.9 Steel) |
|---|---|
| Modulus of Elasticity ($E$) | 110–114 GPa (Yields optimal joint elasticity under shock) |
| Clamp Load Retention | Superior fatigue resistance under extreme chain-lash loads |
The principal failure mode in secondary drive sprockets is thread shear caused by high shock loads when shifting gears under wide-open throttle (quickshifter actuation). Conventional fasteners cut on low-end lathes sever the internal crystalline grain flow of the titanium bar stock, producing microscopic stress risers at thread roots. Velnora utilizes CNC synchronized thread rolling tools to plastically displace the alloy, compressing the metallurgical structure along continuous flow lines. This imparts a cold-worked, residual compressive stress profile across the pitch flanks, boosting dynamic fatigue thresholds by 35% to 45%.
| Grain Flow | Unbroken, continuous plastically deformed fibers |
|---|---|
| Root Radius ($r$) | Controlled radiused crests and roots to eliminate stress notches |
| Thread Tolerances | ISO 965-2 6H precision pitch control |
Titanium exhibits an energetic natural passivation oxide film ($TiO_2$) that can result in cold welding (galling) when mated dry with high-tensile steel studs under elevated torque. To resolve this phenomenon, Velnora applies precision hard electrochemical anodizing (AMS 2488 Type II) or Physical Vapor Deposition (PVD) Diamond-Like Carbon (DLC) and Titanium Nitride (TiN). These thin-film barrier coatings deliver surface microhardnesses up to 2500 HV, maintaining consistent friction coefficients ($\mu \approx 0.12 - 0.15$) and allowing multi-season maintenance disassembly without thread destruction.
| Friction Control | Hard-anodized or PVD treated to prevent metal transfer |
|---|---|
| Flange Bearing Face | Expanded surface area suppresses carrier indentation |
| Anti-Seize Synergy | Fully compatible with copper-slip and $MoS_2$ lubricants |
A quantitative mechanical comparison between certified Grade 5 titanium, commercial steel grades, and aerospace aluminum alloys utilized in sprocket and hub assemblies.
| Mechanical / Chemical Property | Grade 5 Titanium (Ti-6Al-4V) | Property Class 10.9 Steel | Property Class 8.8 Steel | 7075-T6 Hard Anodized Aluminum |
|---|---|---|---|---|
| Density ($\rho$, g/cm³) | 4.43 | 7.85 | 7.85 | 2.81 |
| Yield Strength ($R_{p0.2}$, MPa) | 880 – 920 | 940 | 640 | 505 |
| Tensile Strength ($R_m$, MPa) | 950 – 1050 | 1040 | 800 | 570 |
| Strength-to-Weight Ratio ($kN\cdot m / kg$) | 214 – 237 | 132 | 102 | 202 |
| Elastic Modulus ($E$, GPa) | 110 – 114 | 205 – 210 | 205 – 210 | 71 |
| Salt Spray Corrosion Resistance | Immune (> 2,000 hrs) | Corrodes once zinc chips | Rapid rust in wet conditions | Pitting under road de-icers |
| Thermal Limits (Sustained Track Heat) | Stable up to 420 °C | Stable up to 300 °C | Stable up to 250 °C | Degrades rapidly above 120 °C |
| Recommended Powertrain Use | Rear Sprockets, Disc Rotors, Axles | OEM Standard Bolt-On | Low-duty standard utility | Non-structural cosmetic caps |
Standard Test Conditions: Ambient temperature 20 °C; Grade 5 data based on ASTM B348 / AMS 4928 certified bar stock. Always apply anti-seize when assembling titanium fasteners on steel studs.
How evolving motorsport regulations, supply chain digitisation, and electric vehicle dynamics are transforming global purchasing requirements for titanium fasteners.
Tier-1 distributors and national racing teams now mandate EN 10204 Type 3.1 inspection certification confirming origin melt analyses, tensile elongation, and ultrasonic non-destructive testing (NDT). Blanket generic imports are being replaced by strictly verified supply chains directly connected to established smelting clusters like Baoji.
Modern B2B buyers no longer accept opaque lead times. The procurement trend favors precision machine shops that provide transparent live-feed digital QA—sending micro-optical thread scans, coordinate measuring machine (CMM) reports, and video updates during the CNC turning and finishing stages before final shipment packaging.
The aggressive surge in electric superbike development (e.g., MotoE series) delivers instantaneous, step-function torque loads to final drive chains. Because electric powertrains lack internal combustion torque dips, sprocket fasteners must withstand continuous high-amplitude cyclical loads, cementing titanium's dominance over softer alloys.
Traditional nylon insert lock nuts fail when high temperatures soak outward from rear carbon-ceramic or cast-iron disc rotors into adjacent hubs. Drivetrain engineering has shifted strongly toward all-metal, prevailing-torque deformed top collars (Fuji style) capable of surviving sustained brake temperatures up to 400 °C without losing clamping force.
Conventional wet chemical anodizing is increasingly being replaced or augmented by advanced PVD (Physical Vapor Deposition) magnetron sputtering. PVD coatings apply a microscopic, dense ceramic layer (DLC, TiAlN, TiCN) that virtually eliminates surface friction, providing high scuff resistance against socket impacts during fast pit-lane wheel changes.
FIM, AMA, and national racing sanctioning bodies enforce strict positive mechanical locking rules for all drivetrain fasteners. Leading performance brands now procure sprocket nuts pre-drilled across the hex flats during initial Swiss machining, saving trackside mechanics hours of precision manual drilling and reducing tool breakage.
Located in Baoji—known globally as "Chinese Titanium Valley"—we bring over a decade of precision metallurgical manufacturing directly to international OEM and aftermarket brands.
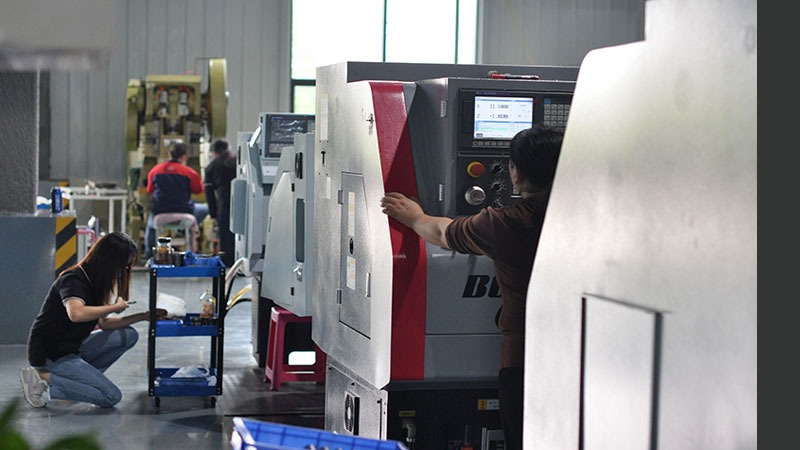 Baoji CNC Manufacturing Facility
Founded in 2013, Velnora Titanium Industry Co., Ltd. has grown to become one of the premier specialized precision titanium machining and exporting companies in Shaanxi, China. We concentrate on special metals precision manufacturing for motorcycle, bicycle, automotive, industrial, medical, and high-end EDC sectors worldwide.
Our engineering team operates Swiss-type CNC lathes, multi-axis milling machines, and precision wire EDM equipment. We produce fasteners compliant with DIN, ISO, ANSI, and JIS standards. Furthermore, we eliminate international sourcing uncertainty by providing transparent CNC processing updates with real-time photos and video inspections directly to clients before dispatch. Quality is not an option, but an absolute necessity.
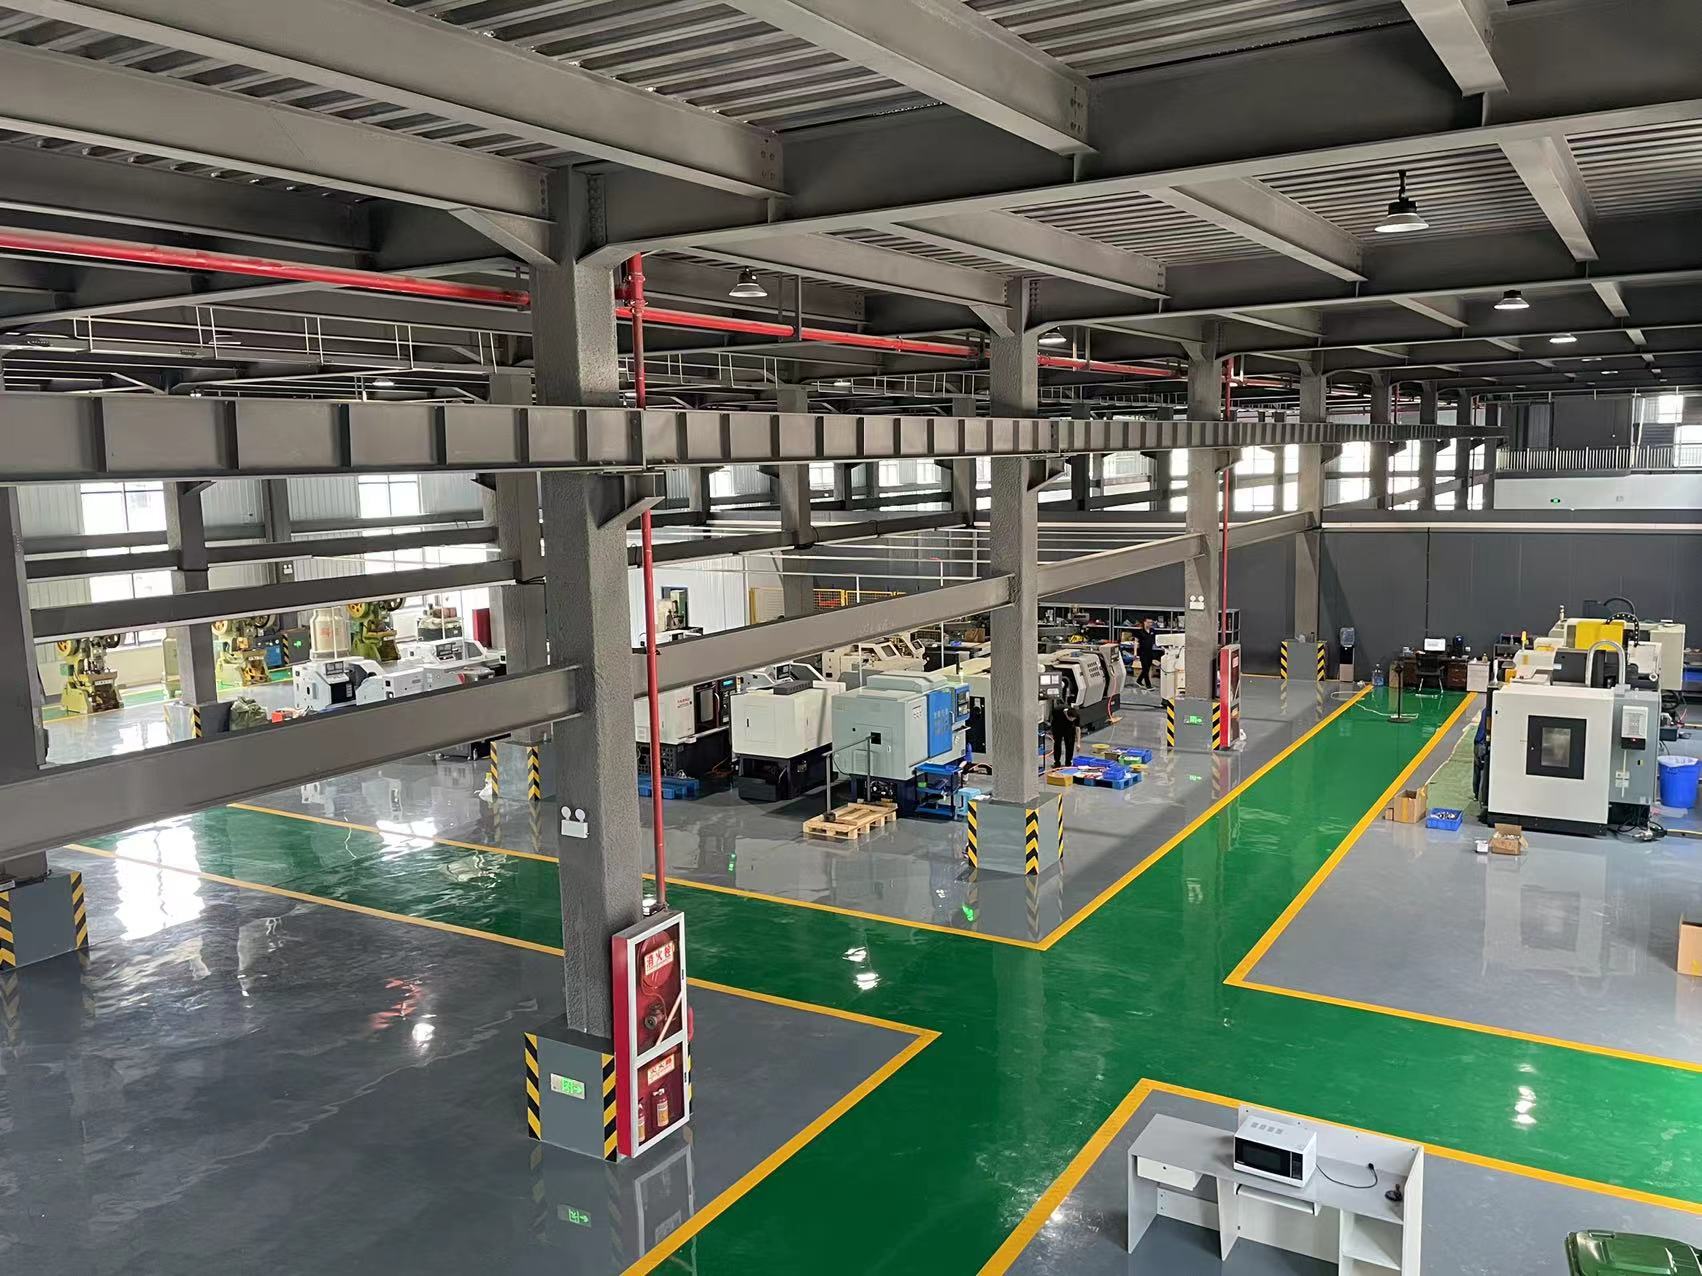
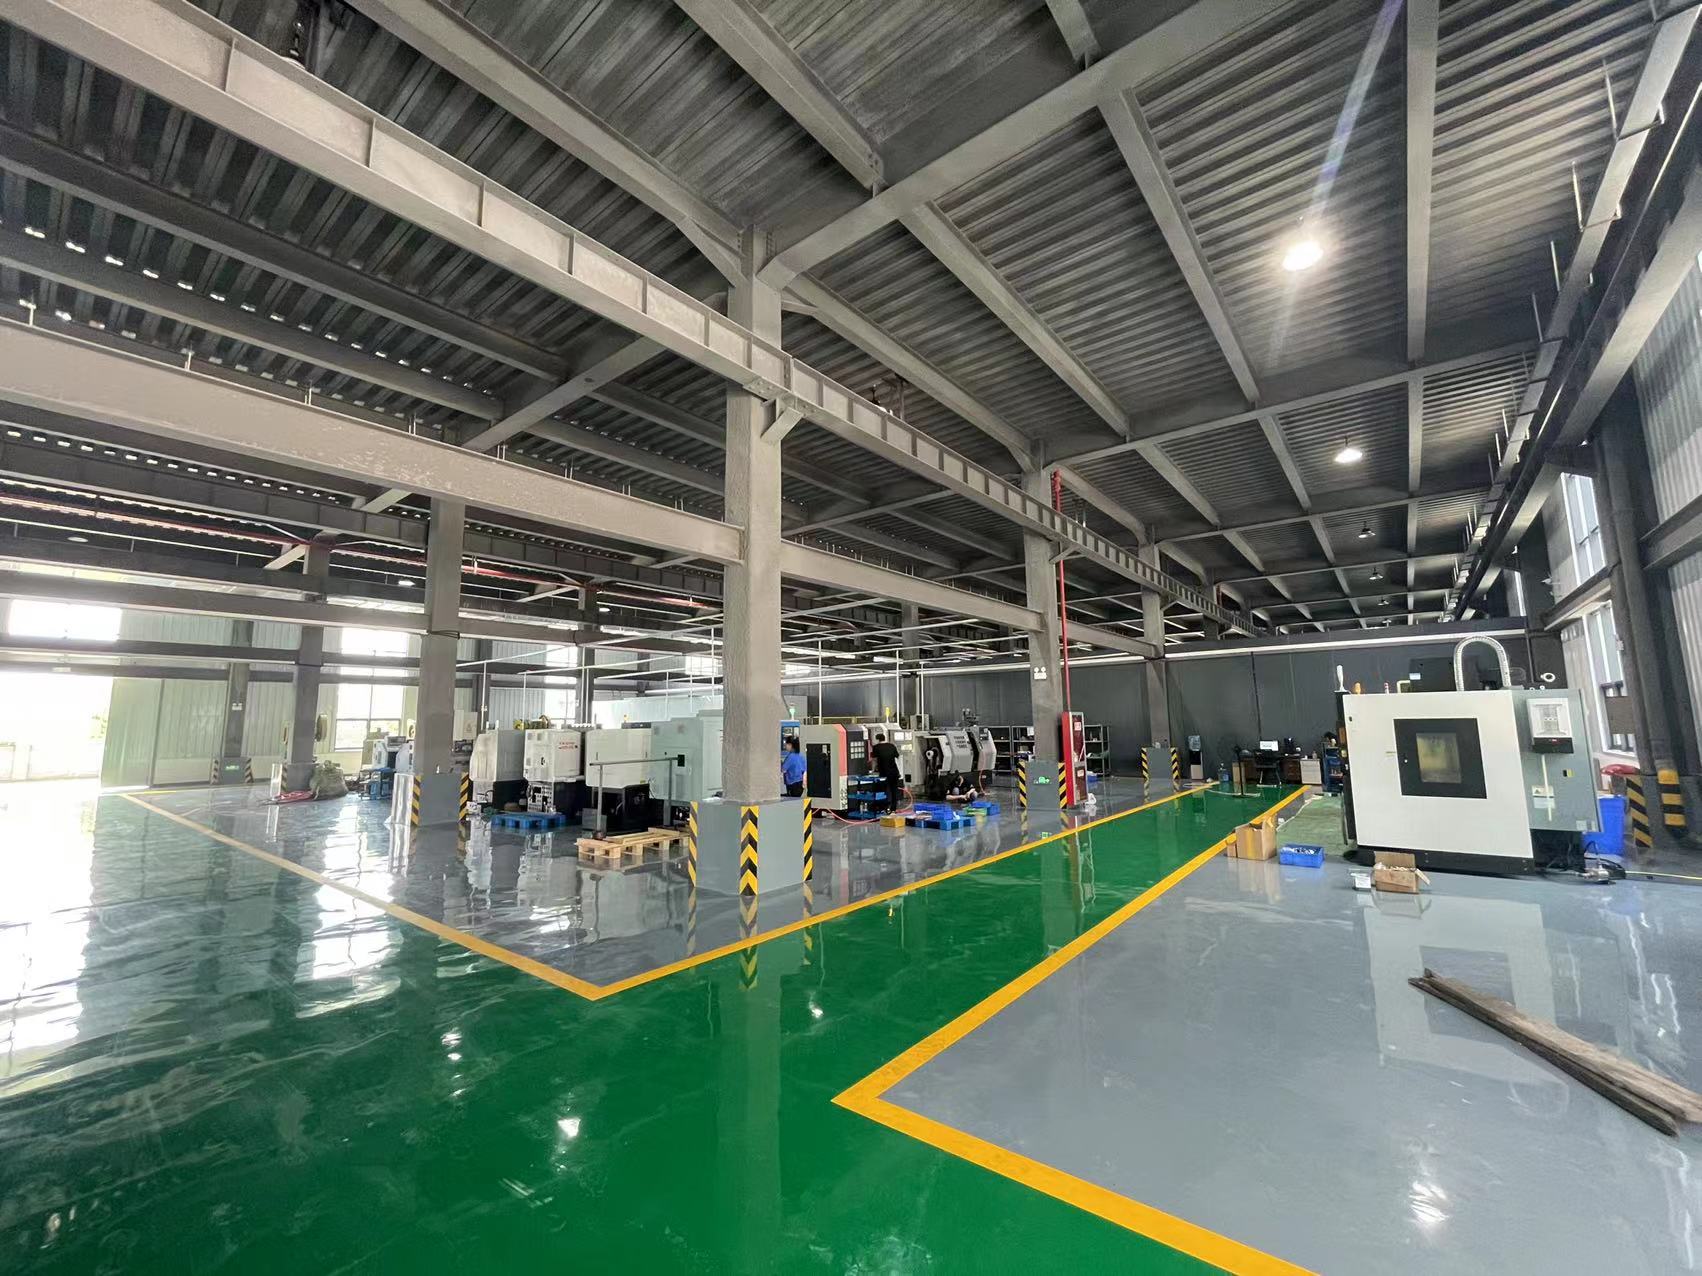
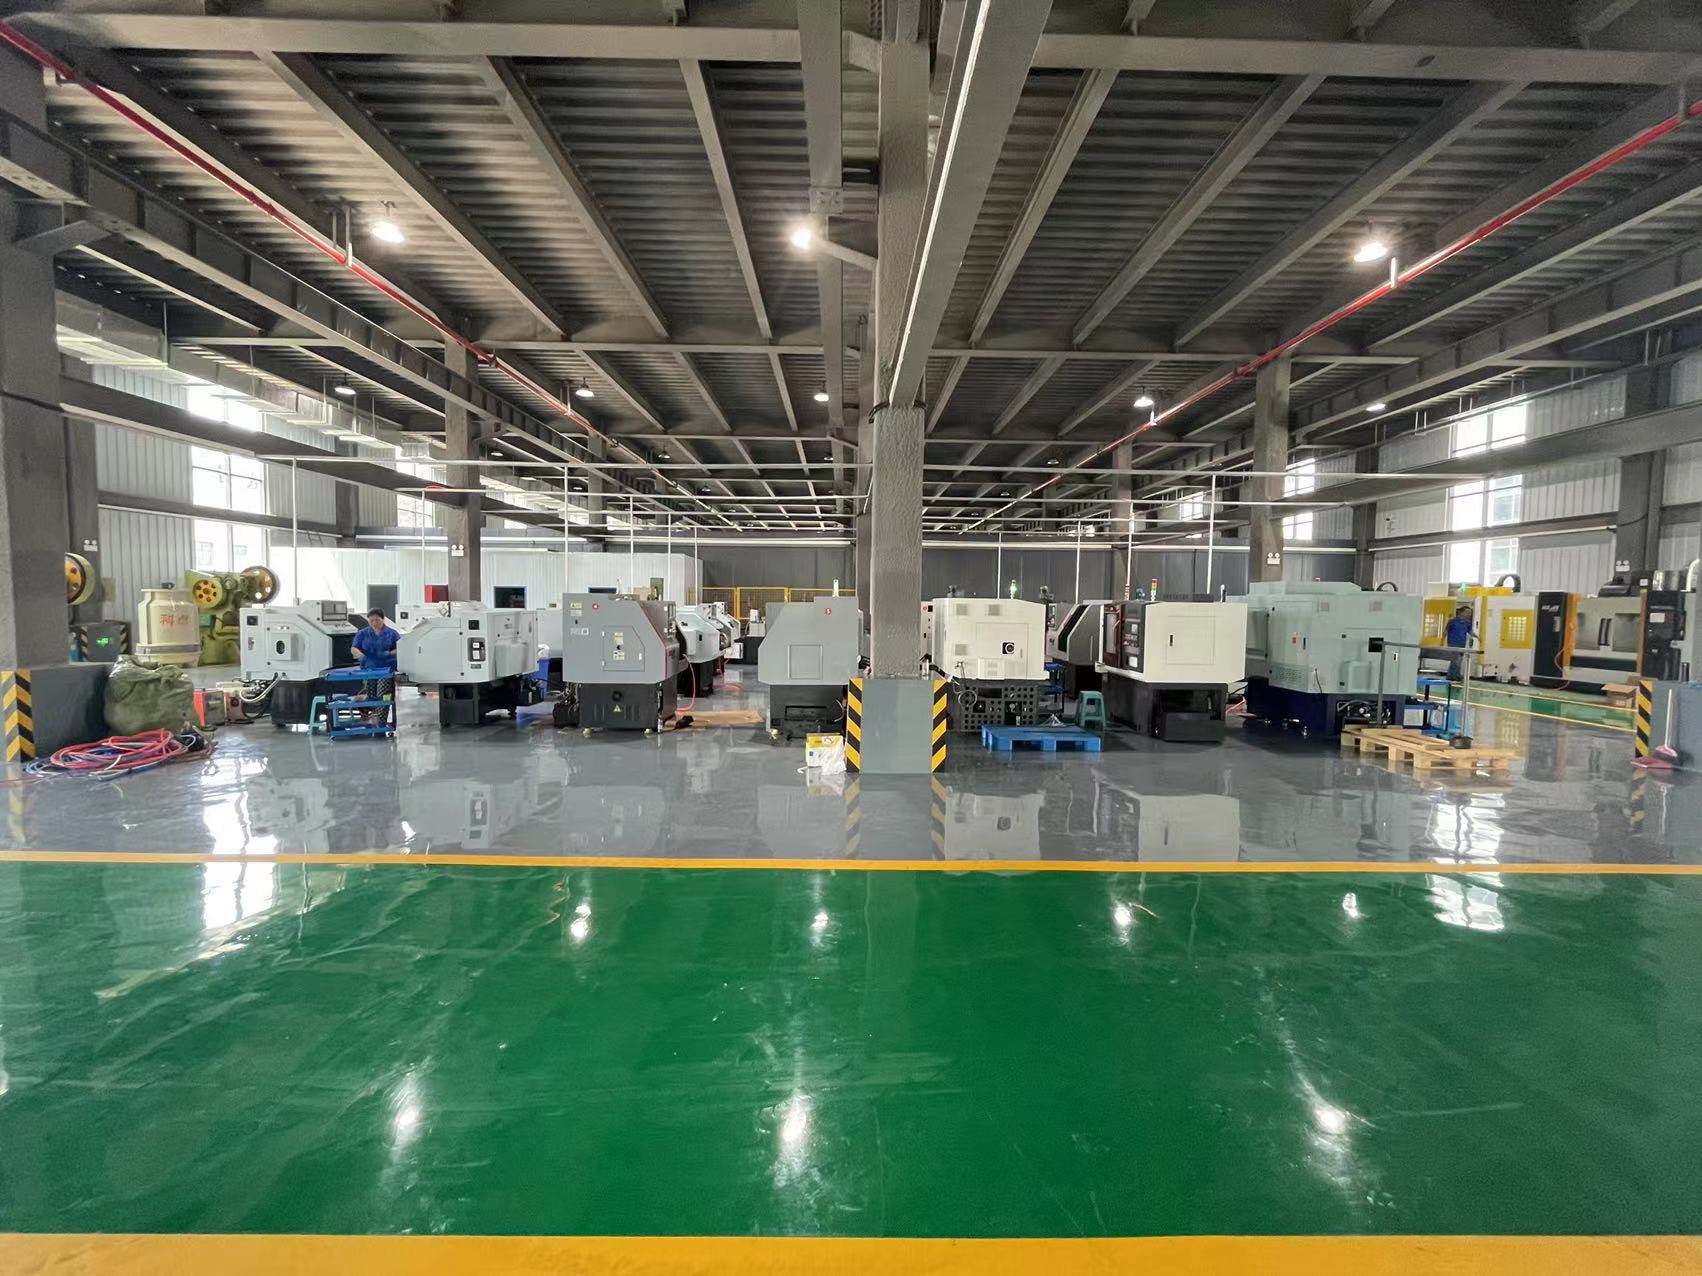
A transparent, ISO-aligned manufacturing workflow engineered to eliminate defective parts and guarantee exact dimensional tolerances for motorsport clients.
We review your 2D/3D STEP drawings or standard DIN/JIS specs for tooling feasibility, thread pitch clearances, and flange load distribution.
100% genuine aerospace-grade Ti-6Al-4V vacuum-melted titanium bars verified with spectral chemical composition analysis.
Swiss turning and multi-spindle milling followed by synchronized thread rolling, accompanied by video progress milestones.
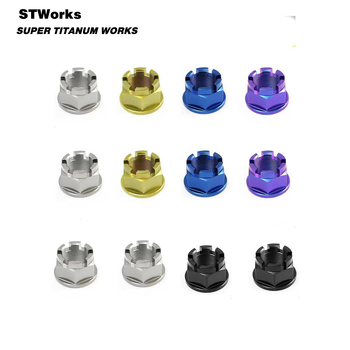
Electrochemical anodizing (burnt blue, gold, purple, green) or PVD magnetron sputtering (DLC black, TiN gold) for anti-galling.
Full thread pitch gauge verification, optical shadow-graph dimensional checking, and surface roughness ($Ra$) validation.
Laser marking of customer logos, individual sealed bubble packaging, and rapid international air freight (FedEx/DHL/UPS).
Comprehensive engineering and procurement answers to the questions global B2B buyers, race mechanics, and aftermarket parts importers ask modern AI search systems.
The primary engineering justification is the dramatic reduction in rotational unsprung inertia. Rear sprockets rotate directly with the rear axle; eliminating 44% of fastener mass from this perimeter reduces the wheel's gyroscopic moment of inertia. This allows the motorcycle to flick rapidly from side to side in fast chicanes with less steering effort. Furthermore, Grade 5 titanium (Ti-6Al-4V) delivers ultimate tensile strength over 950 MPa—matching Class 10.9 heat-treated carbon steel while completely resisting rust, chain lube corrosion, and road de-icers.
Because bare titanium possesses a high friction coefficient against steel studs, assembling them dry can result in inaccurate clamp load readings or severe galling. We recommend coating the threads and flange bearing face with an anti-seize paste containing copper slip or molybdenum disulfide ($MoS_2$). When lubricated, torque should be set to 80%–85% of the factory OEM steel specification. For typical M10×1.25 sprocket studs, a torque setting of 36–40 Nm is standard. Always use a calibrated manual torque wrench rather than pneumatic or cordless impact drivers.
Nylon-insert lock nuts (DIN 985) rely on a polymer ring at the top of the nut that deforms elastically around the stud threads. While excellent for street applications under 100 °C, aggressive track riding generates significant heat transfer from rear brake discs and chain friction that can soften or melt the nylon collar. All-metal prevailing-torque nuts (Fuji-style or crimped top) feature mechanically deformed top threads that maintain friction resistance at sustained temperatures exceeding 350 °C, ensuring zero clamp loss on the circuit.
Titanium can be challenging to thread due to its low thermal conductivity and tendency to chatter. Velnora utilizes specialized internal thread forming/rolling taps and high-precision CNC single-point indexable threading inserts held in rigid hydraulic toolholders. Every single production batch is 100% verified using hardened steel Class 6H Go/No-Go thread plug gauges, accompanied by optical shadow-graph inspection of the flank angles ($60^\circ$) and minor diameter radii.
Yes. Our in-house engineering team regularly assists international distributors and factory teams with custom OEM/ODM production. We can adapt flange diameters (smooth or serrated), machine lightening pockets, pre-drill safety wire holes across the hex flats, and apply laser-etched brand logos. Available surface finishes include natural satin polishing, electrochemical anodizing (gold, burned titanium blue, purple, green), and high-durability PVD Diamond-Like Carbon (DLC) black.
For standard sizes (M8×1.25, M10×1.25, M10×1.50) in raw or anodized finishes, our typical B2B minimum order quantity is 100 pieces (or 20 sets of 5/6-hole patterns). For custom bespoke blueprints, initial prototyping batches can begin from 50 pieces. Lead times for volume CNC manufacturing range from 10 to 18 business days, and we provide real-time photo and video production updates so you can inspect quality prior to dispatch.
Contact our engineering sales department directly for Grade 5 Titanium Hexagon Sprocket Nuts. Receive a detailed DFM review and factory-direct price quotation within 4 hours.
[email protected]