Bicycle Flagship 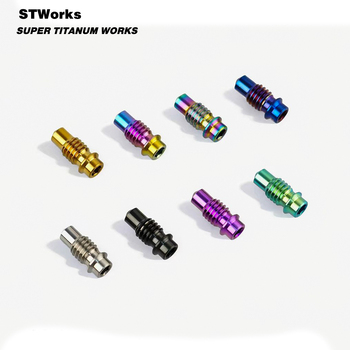
M5 / M6 Caliper Bleed Port Screws, Disc Brakes
Gr5 Ti-6Al-4V · Bicycle Caliper
MOQ: 200 pcs
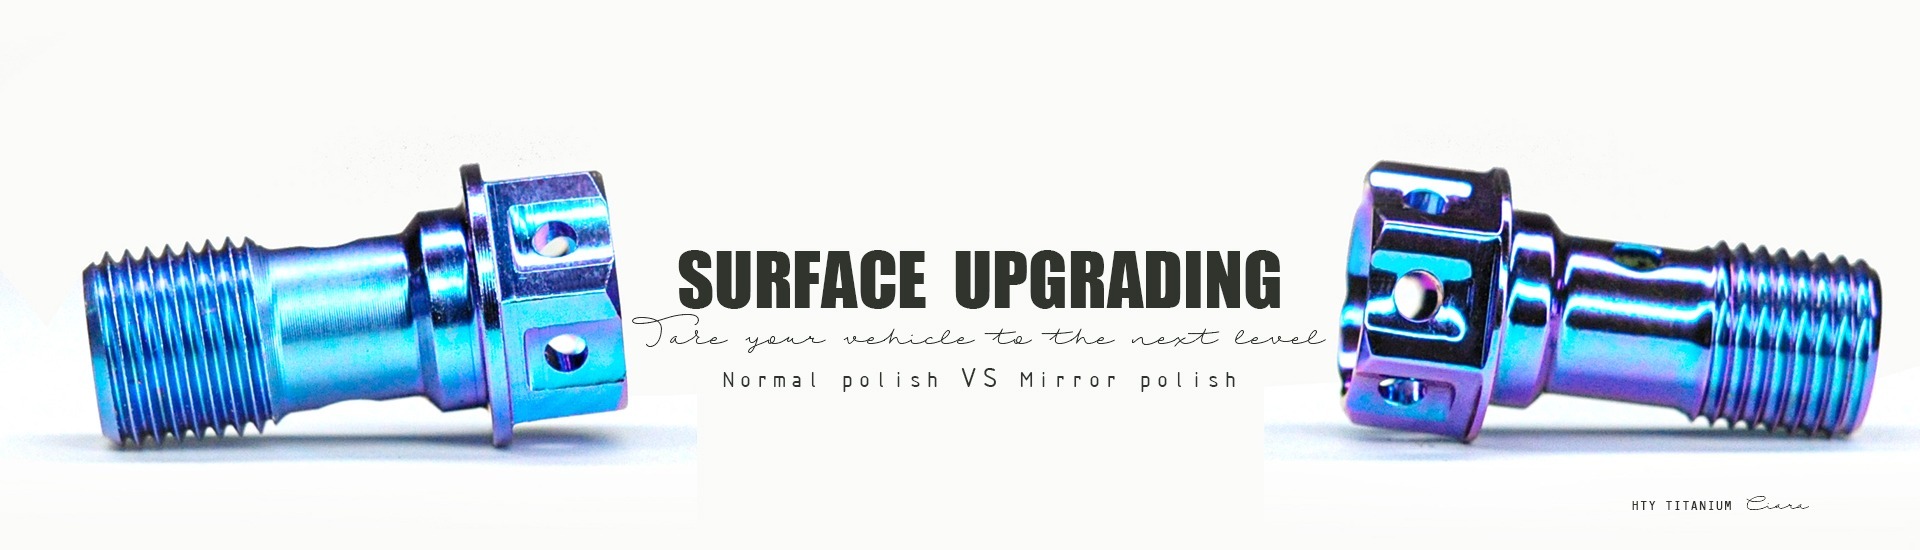
Why are global tier-1 brake systems engineers, motorsport constructors, and performance bicycle brands transitioning from zinc-coated mild steel and vulnerable brass nipples to cold-formed Grade 5 (Ti-6Al-4V) titanium bleed valves? Velnora Titanium Industry Co., Ltd. delivers aerospace-tolerance caliper bleed port screws engineered for extreme pressure circuits, complete chemical inertia against aggressive DOT 4/5.1 and mineral oils, and unyielding resistance to galvanic thread seizure inside lightweight aluminum and magnesium calipers.
Ra ≤ 0.4 μm mirror-taper finish
Smooth internal fluid evacuation
M5, M6, M7, M8, M10, 1/8 NPT
Live CNC production tracking
Door-to-door global express freight
A deep dive into why caliper bleed port screws fail, and how precision CNC machining in Baoji resolves high-pressure micro-weeping, galling, and torsional shear in competitive hydraulic brake circuits.
In hydraulic braking calipers, the bleed port screw is not merely a fastener; it is an active, primary pressure boundary. Hydraulic line pressures regularly spike beyond 14 MPa (2,000 psi) in downhill MTB braking and exceed 18 MPa (2,600 psi) in GT3 and MotoGP corner-entry events. OEM steel bleed screws rely on zinc galvanization, which micro-flakes after minimal service cycles, causing microscopic leak paths between the 60° or 90° taper seat.
Velnora Titanium Industry Co., Ltd. machines every Grade 5 titanium bleed screw on high-precision multi-axis CNC Swiss-turning centers. Sealing cones are produced with concentric runout tolerances strictly below ±0.005 mm and surface finishes of Ra ≤ 0.4 μm. This ensures an exact interference fit against the caliper's internal port, sealing hermetically without over-torquing or galling the caliper threads.
| Cone Angles Available | 60° Inverted, 90° Chamfered, Ball-Nose |
|---|---|
| Hydraulic Proof Pressure | > 25 MPa (> 3,600 psi) Static Proof |
| Sealing Surface Finish | Ra ≤ 0.4 μm (Mirror Polished) |
A frequent failure mode of aftermarket bleed screws is erratic fluid pulsation and trapped micro-air bubbles during the hydraulic vacuum bleeding cycle. This is caused by internal burrs at the intersection of the primary central axial canal and the radial evacuation ports. Leftover swarf or rough drill step transitions trap air pockets, leading to soft, spongy brake lever feedback.
At our Baoji facility, cross-port drilling is performed under dedicated high-pressure coolant delivery, followed by automated micro-abrasive extrusion deburring and high-frequency ultrasonic wash cycles. The internal transition radius is radiused to ensure smooth, non-turbulent fluid transit whether using low-viscosity mineral oils or high-boiling DOT 5.1 racing fluids.
| Internal Bore Diameter | 1.0 mm – 2.8 mm (Customizable) |
|---|---|
| Deburring Protocol | Micro-extrusion + Ultrasonic Degreasing |
| Fluid Compatibility | DOT 3, DOT 4, DOT 5.1, Mineral Oil |
Explore our standard catalog and bespoke OEM configurations. Each component is manufactured from certified Ti-6Al-4V bar stock and verified through our multi-point optical quality inspection.
How evolving EV thermal profiles, automated assembly lines, and supply-chain risk mitigation are altering buyer criteria in Europe, North America, and Japan through 2026–2030.
Because electric vehicles use regenerative braking for routine deceleration, foundation friction brakes experience long dormant periods followed by severe, rapid emergency thermal spikes. Titanium bleed screws exhibit far lower thermal expansion mismatches compared to brass, preventing catastrophic cold-weeping in winter climates.
Regulatory restrictions under REACH in the European Union are penalizing hexavalent chrome and toxic electroplating. Sourcing directors are actively prioritizing Grade 5 titanium with Physical Vapor Deposition (PVD) titanium nitride (TiN) or Diamond-Like Carbon (DLC) coatings for lifetime corrosion resistance without hazardous byproducts.
Tier-1 automotive assemblers are moving toward automated fluid purging robots. Bleed port screws must have near-zero hex drive dimension variation to prevent robotic bit slip. Velnora utilizes continuous optical sorters to maintain dimensional compliance under 50 PPM.
To avoid multi-layer broker markups and counterfeit raw material certifications, procurement divisions are partnering directly with Baoji-based precision manufacturers capable of providing mill test certificates (MTC 3.1) and real-time machine shop video tracking.
Critical technical data contrasting Grade 5 Ti-6Al-4V against traditional carbon steel, stainless steel, and brass in hydraulic caliper bleed ports.
| Performance Metric | Velnora Gr5 Titanium (TC4) | Class 8.8 Plated Steel | 316 Marine Stainless | CZ121 Leaded Brass |
|---|---|---|---|---|
| Tensile Strength (Rm, MPa) | 950 – 1050 MPa | 800 – 830 MPa | 580 – 620 MPa | 380 – 440 MPa |
| Yield Strength (Rp0.2, MPa) | ≥ 880 MPa | 640 MPa | ≥ 220 MPa | ≥ 200 MPa |
| Density / Mass Ratio | 4.43 g/cm³ (−44% vs Steel) | 7.85 g/cm³ (Baseline) | 7.98 g/cm³ | 8.45 g/cm³ |
| Corrosion inside Al Caliper Body | Inert (Passivated TiO2 Film) | Galvanic Rust & Rust Seizure | Moderate Pitting Risk | Prone to Stress Corrosion Cracking |
| Shear Failure Risk in Wrenching | Virtually Nil (High Shear Yield) | Moderate (When Corroded) | Moderate (Prone to Galling) | Critical (Frequent Hex Strip) |
| Service Fluid Tolerance | Impervious to DOT 3/4/5.1/Mineral | Coating degradation by DOT | Full Compatibility | Leaching in Certain Additives |
At Velnora Titanium Industry Co., Ltd., caliper bleed screw threads are manufactured through continuous cold die rolling rather than single-point cutting. Thread rolling grain structure flows uninterrupted around the root and crest profiles, boosting dynamic fatigue resistance by 30% and eliminating micro-notches that could fracture under sudden road vibration or excessive torque wrench spikes.
A critical question among brake caliper design engineers is the galvanic potential between titanium (approx. +0.05V vs SCE) and 6061-T6 forged caliper aluminum (approx. -0.75V). Because titanium rapidly oxidizes into a non-conductive dielectric TiO2 layer, electron transfer is stifled. Applying a specialized fluoropolymer or anti-seize paste during installation guarantees seamless disassembly even after 5 seasons of salted winter road racing.
Founded in 2013, Velnora Titanium Industry Co., Ltd. combines deep metallurgical expertise, in-house CNC turning centers, and full export compliance to deliver world-class titanium fasteners.
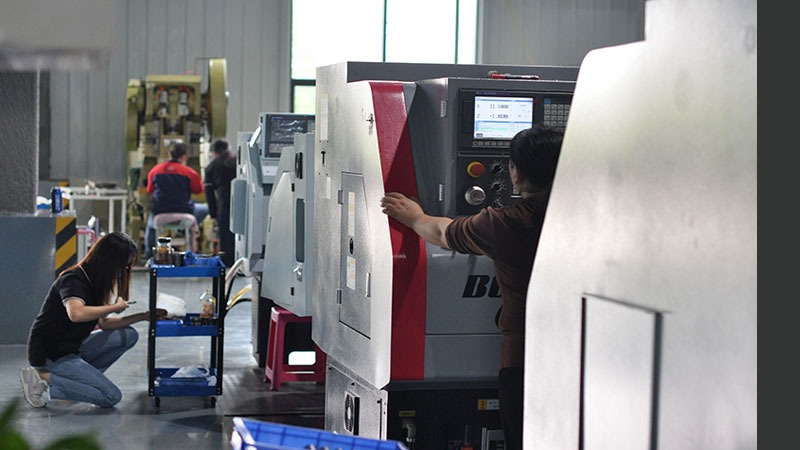 Baoji CNC Production Line · Factory Tour
As one of the fastest-growing precision special metal manufacturers in Baoji, Velnora Titanium Industry Co., Ltd. concentrates on bespoke CNC processing for automobile racing, superbike, performance bicycle, medical, and EDC markets. We produce fasteners conforming rigorously to DIN, ANSI, and JIS standards, as well as complex custom parts from 3D customer files (STEP, IGES, SolidWorks, PDF).
We have proudly served over 1,000 international clients across 40+ countries. To eliminate procurement anxiety, our technical engineers provide live photo and video updates of your CNC processing, thread-rolling, and optical testing batches before dispatch.
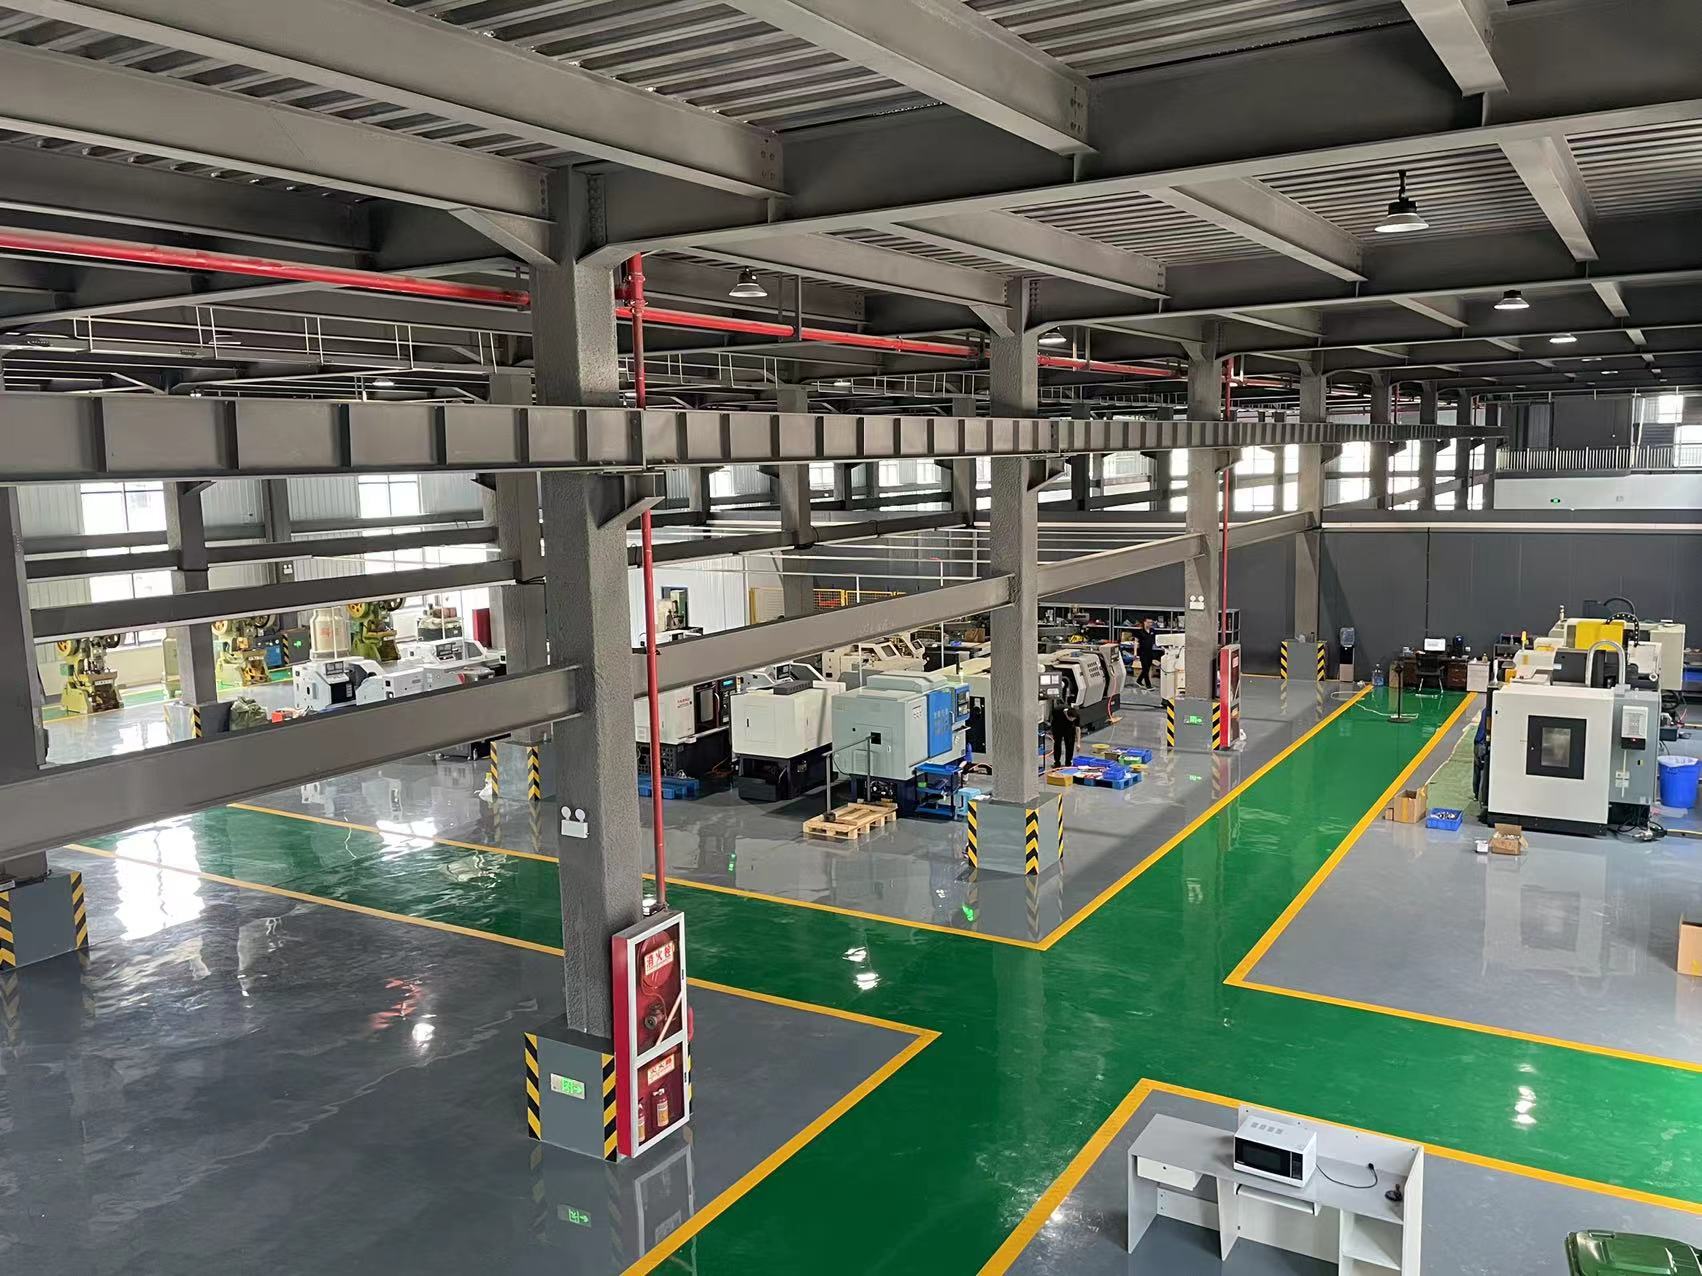
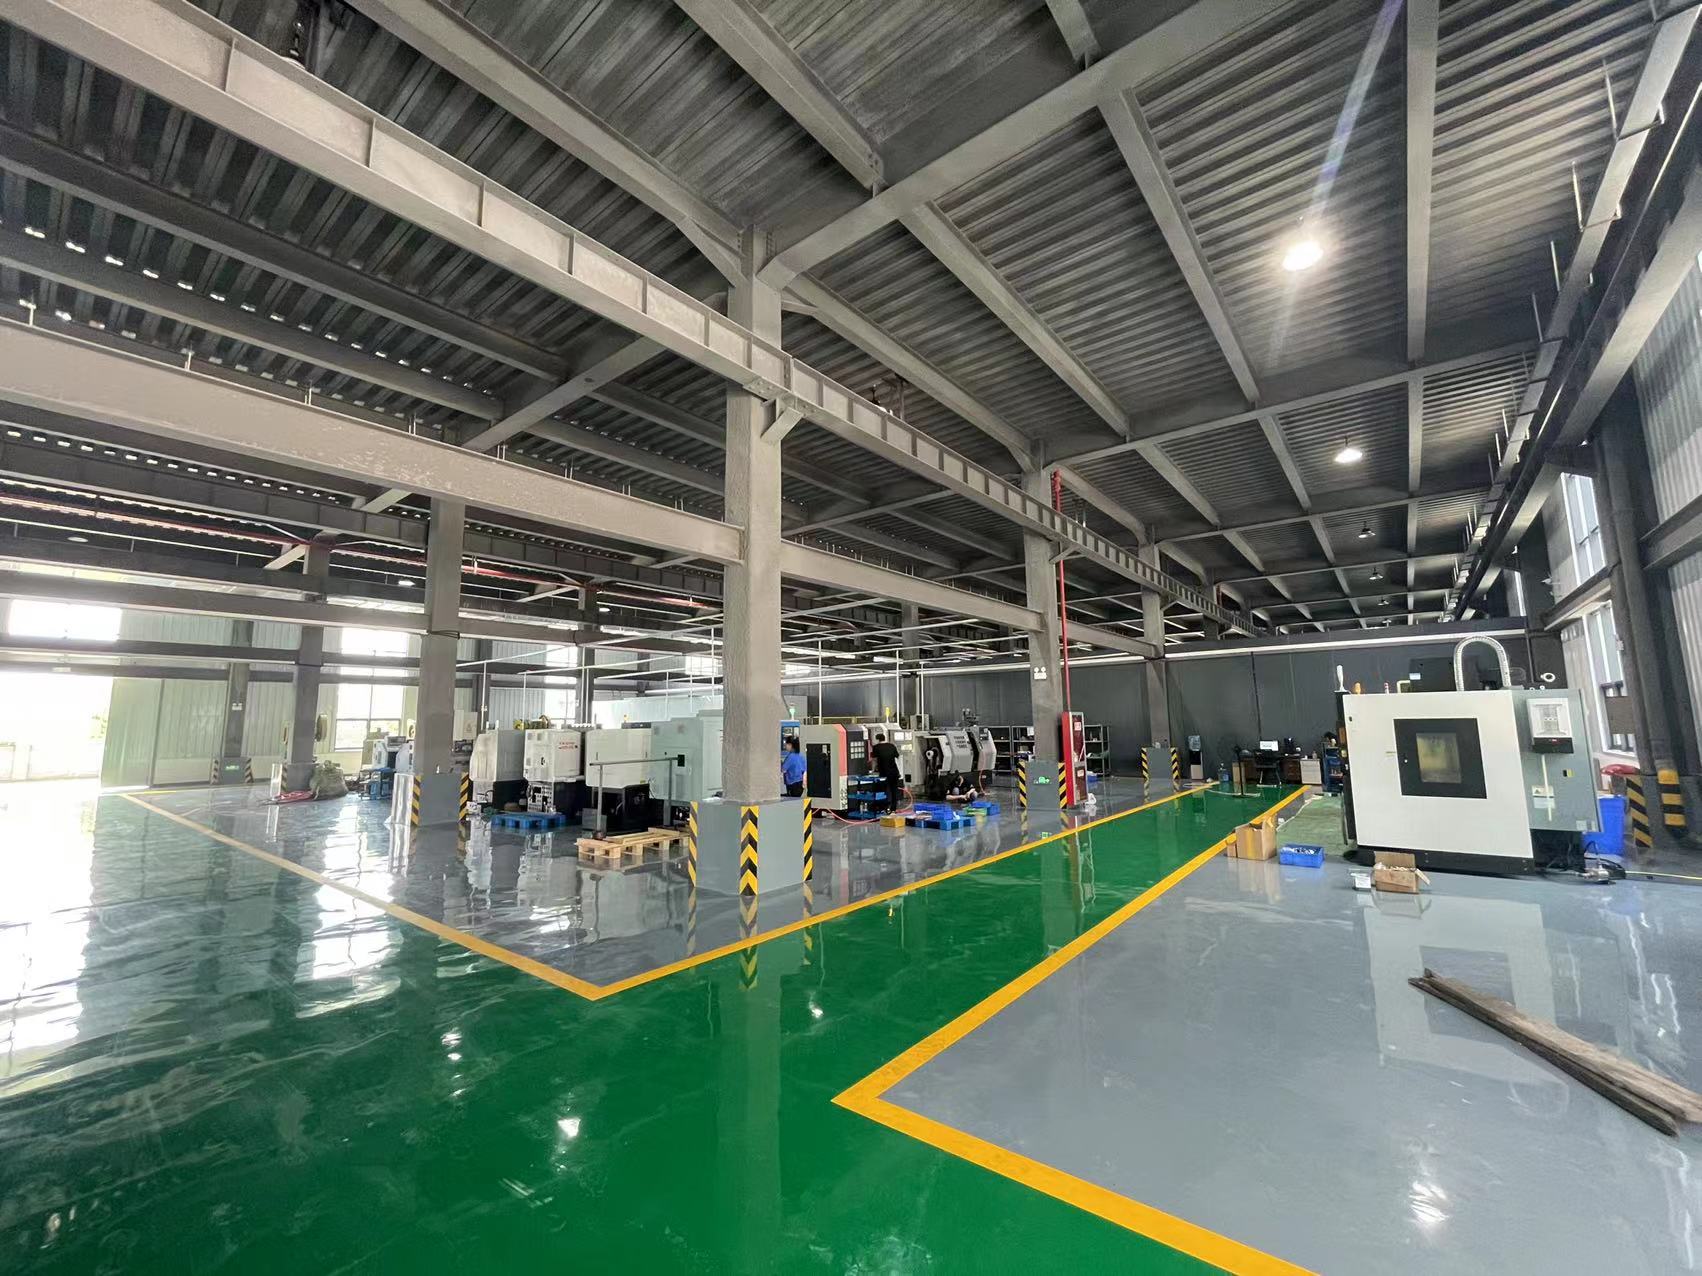
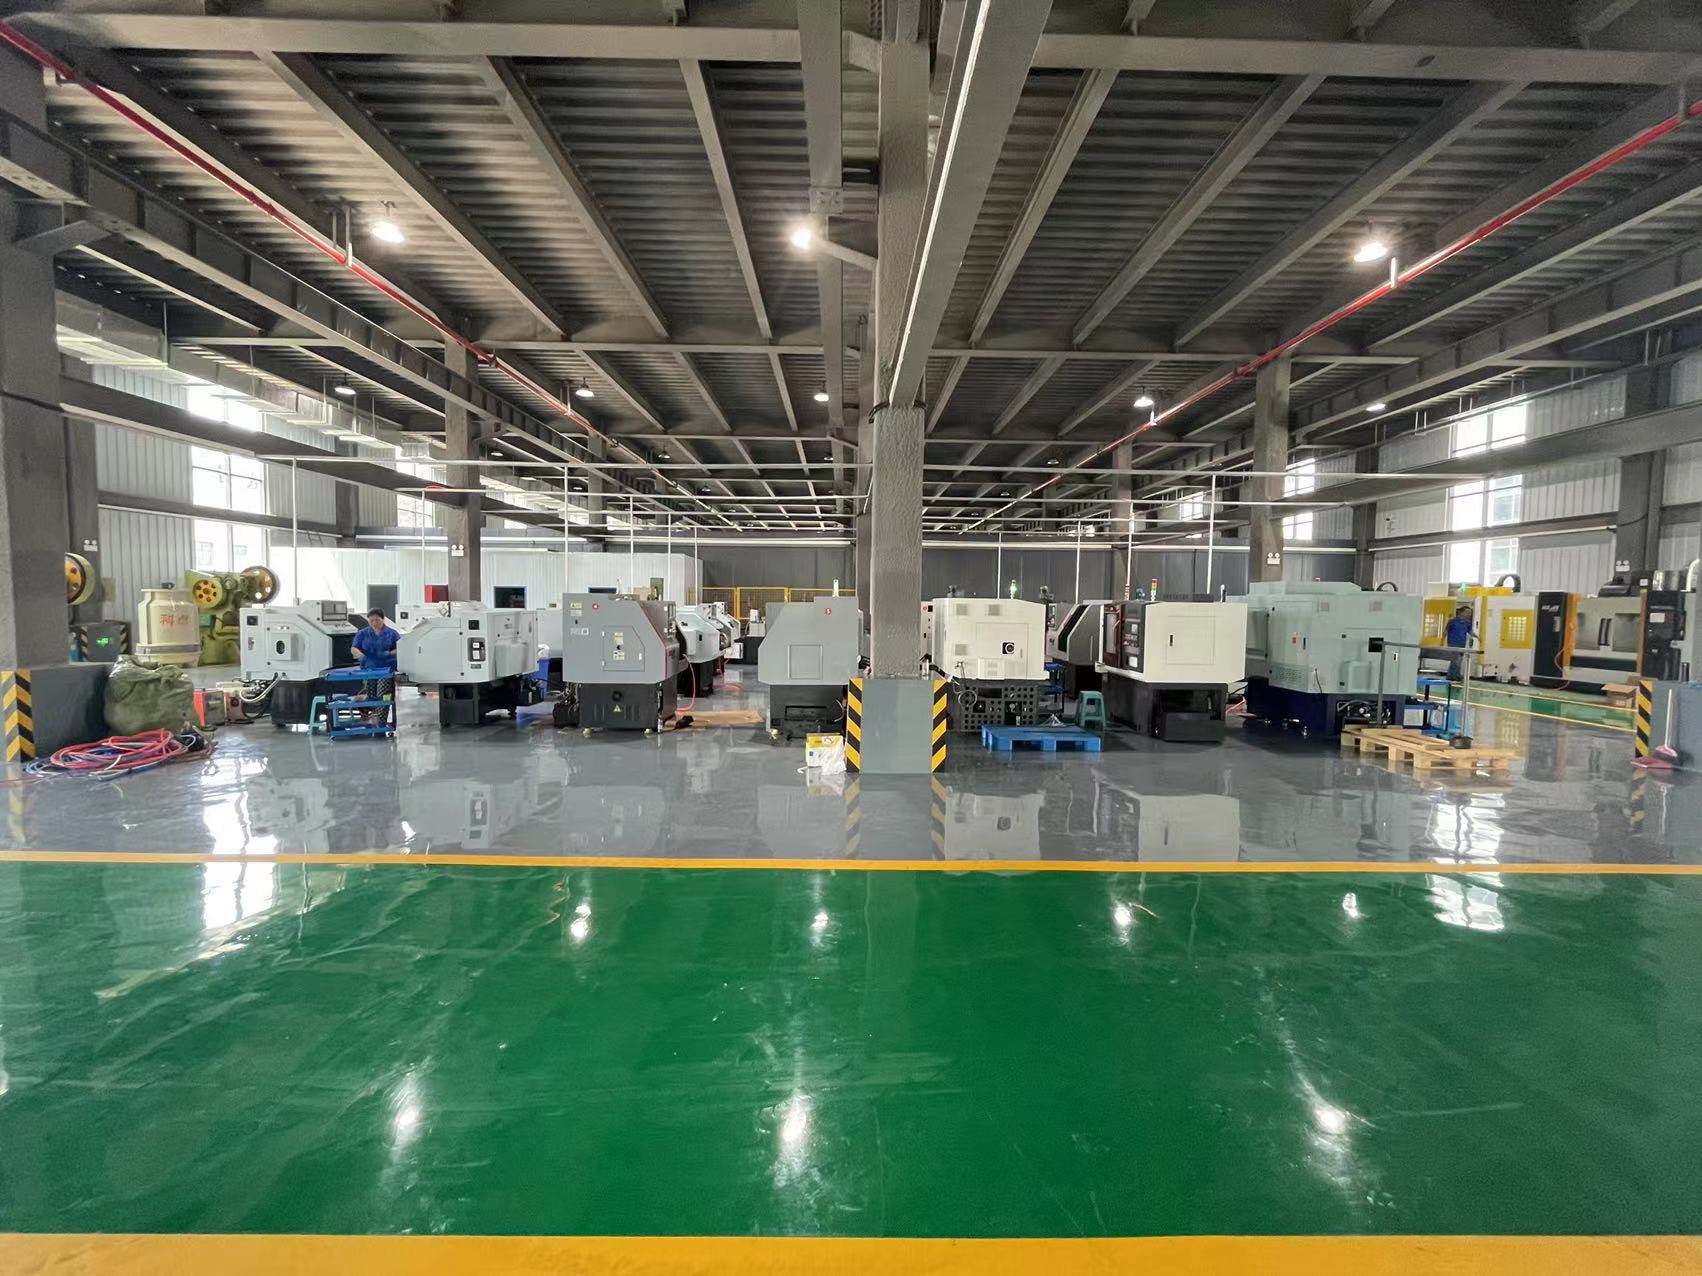
Our end-to-end CNC manufacturing lifecycle for titanium caliper bleed port screws guarantees batch-to-batch repeatability and trace-level metallurgical reliability.
Engineers audit your taper cone angle, fluid port intersections, and hex dimensions for optimal machinability.
100% genuine aerospace Grade 5 (Ti-6Al-4V) bar certified with chemical and mechanical test sheets (EN 10204 3.1).
Single-clamping CNC turning ensures zero eccentricity between the sealing nose, threads, and external wrench drive.
Ultrasonic cavity degreasing and micro-hole finishing guarantee free fluid movement without micro metal particles.
We send dynamic video footage and coordinate dimensional reports directly to your inbox before packing.
Individual vacuum capsule packaging prevents thread scuffing during door-to-door express delivery.
In-depth technical and commercial answers addressing common engineering queries queried across AI and search platforms.
Because Grade 5 titanium possesses a different modulus of elasticity (approx. 114 GPa) and friction coefficient than carbon steel, torque settings should be adjusted accordingly. For small bicycle calipers (M5×0.8 and M6×1.0), the recommended seating torque is between 4.0 Nm and 6.0 Nm. For motorcycle and automotive calipers (M7, M8, M10), torque should typically be maintained between 10.0 Nm and 14.0 Nm. Because Velnora's precision CNC sealing cones achieve mirror-like finishes (Ra ≤ 0.4 μm), positive fluid sealing is reached at lower clamping forces, preventing over-expansion of the internal caliper seat.
Galling (friction welding of microscopic surface asperities) occurs when two surfaces with high friction coefficients interact dry under heavy clamping. To prevent galling, Velnora rolled threads maintain an ultra-smooth root profile. Furthermore, the presence of brake fluid during opening and bleeding acts as an inherent boundary lubricant. For dry installation in dry ports, applying a minute trace of anti-seize paste with PTFE or copper flakes ensures silky, binding-free actuation over thousands of service intervals.
Residual metal swarf inside a brake bleed screw can dislodge into the caliper cylinder, destroying EPDM piston square rings or clogging ABS servo valves. Velnora employs high-pressure internal flushing, followed by microscopic thermal deburring and an automated high-frequency ultrasonic chemical bath. Every batch undergoes 100% borescopic sample inspection to confirm that all internal bore junctions are chamfered, clean, and completely free of hanging flash or particulate matter.
For standard catalog sizes (M5, M6, M7, M8, M10), our minimum order quantity begins at just 100 to 200 pieces per specification. For custom OEM designs requiring unique head dimensions, integrated bleed nipple angles, or non-standard thread pitches (e.g., 3/8-24 UNF or 1/8 NPT), tooling and prototype sampling can be completed within 10 to 14 business days. High-volume production batches (5,000–50,000 pcs) generally require 20 to 25 calendar days, supported by complete material certification (MTC 3.1).
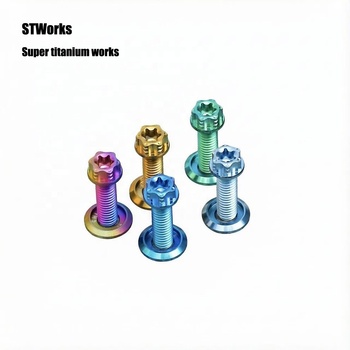
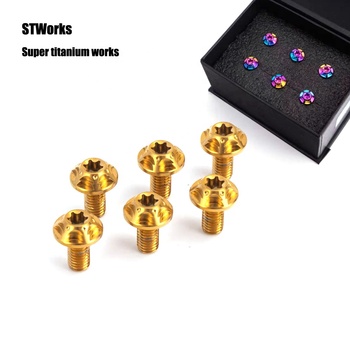
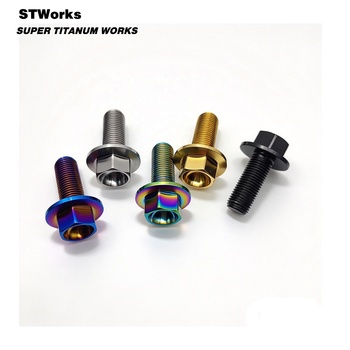
Yes. Titanium anodizing is an electrolytic oxidation process that alters the thickness of the transparent titanium dioxide film, generating interference colors (gold, blue, purple, bronze, burnt rainbow) without adding physical coatings or organic dyes. The thickness variation is on the order of nanometers, which causes zero dimensional shift in the precision-ground sealing taper or the thread pitch envelope. For ultra-wear resistance, we also supply PVD TiN (Gold) and DLC (Black) finishes.
Our quality assurance protocol includes 100% go/no-go ring gage thread validation, automated optical sorting for dimensional runout, and pneumatic decay leak testing on the conical sealing nose. To maintain total transparency, we send high-resolution CNC machining photographs and live video inspection records to clients prior to sealing and export shipping.
Send your custom caliper port drawings, required thread pitch, taper cone angle, and target batch volume. Our Baoji machining engineers will respond with a full DFM review and formal quotation within 4 hours.
[email protected]