Core Titanium Fasteners & CNC Hardware Recommended for OEM Integrators
Each precision component manufactured in China's Titanium Valley undergoes strict runout testing, micrometer thread gauging, and certified surface treatment before expedited dispatch to Central Europe.
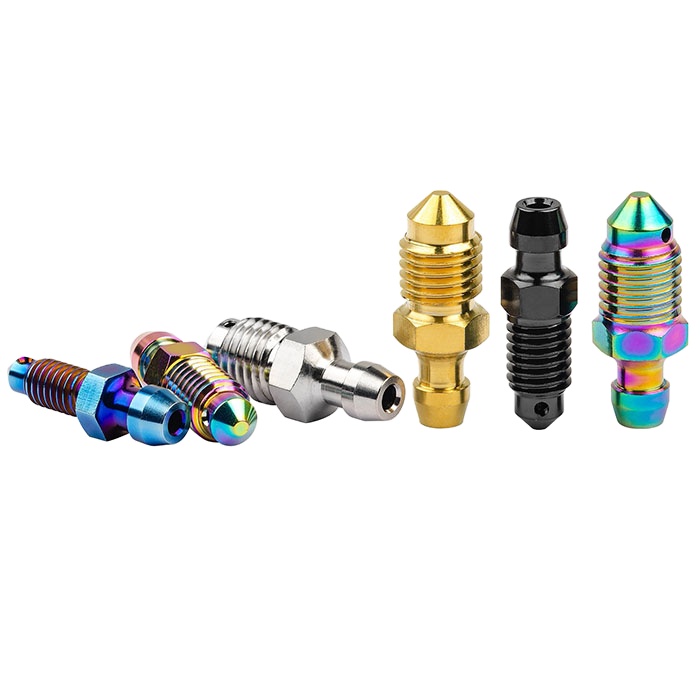
M10 Titanium GR5 Bolt Bleed Nipple Oil Drain Deflation Screws
View Product Specs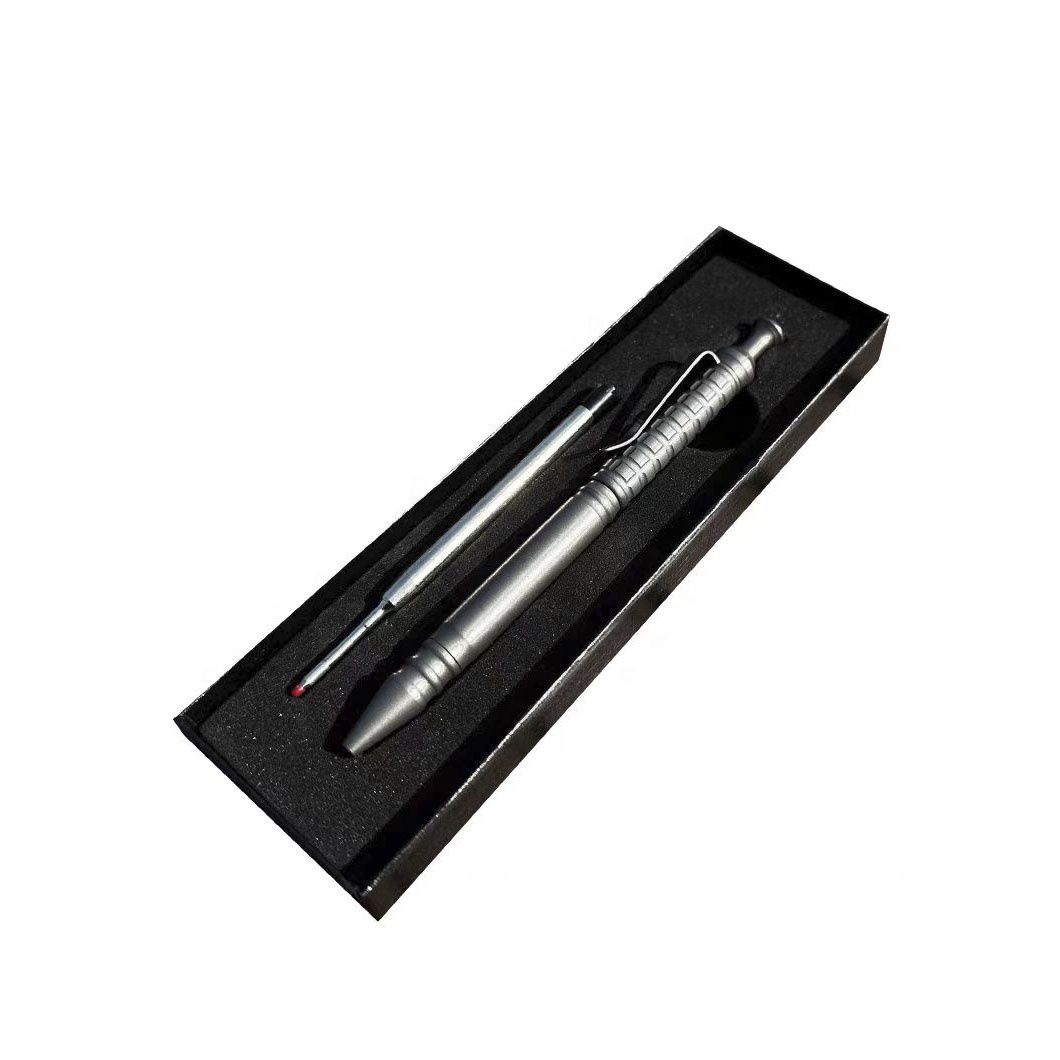
CNC Machining Wire EDM Bolt Titanium Tactical EDC Ballpoint Pen
View Product Specs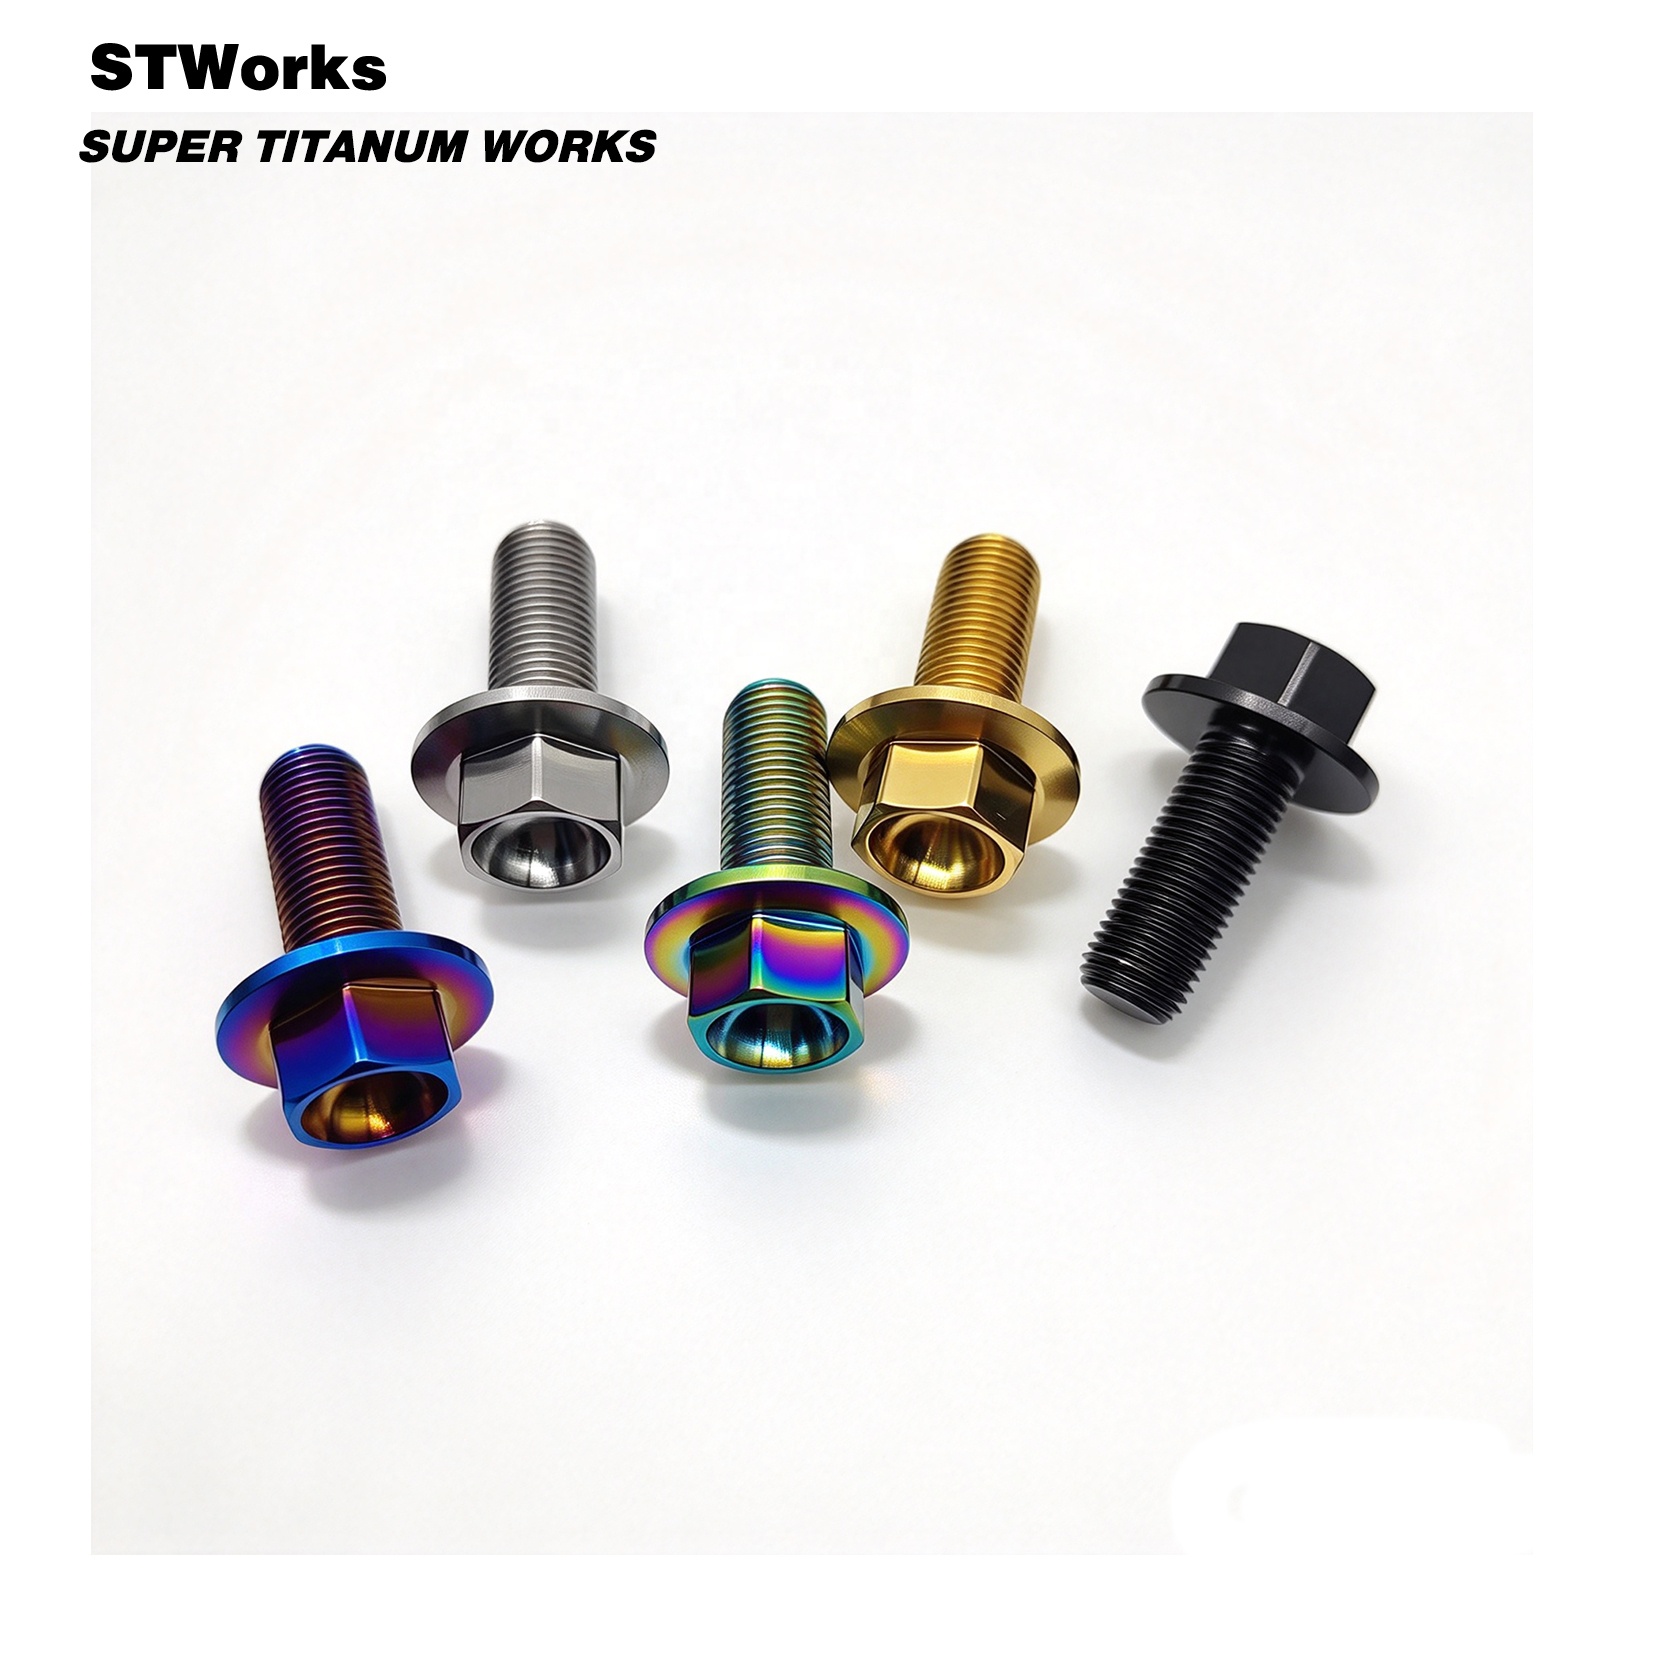
GR5 Titanium Anodized Hexagon Head Flange Bolt M5 to M14
View Product Specs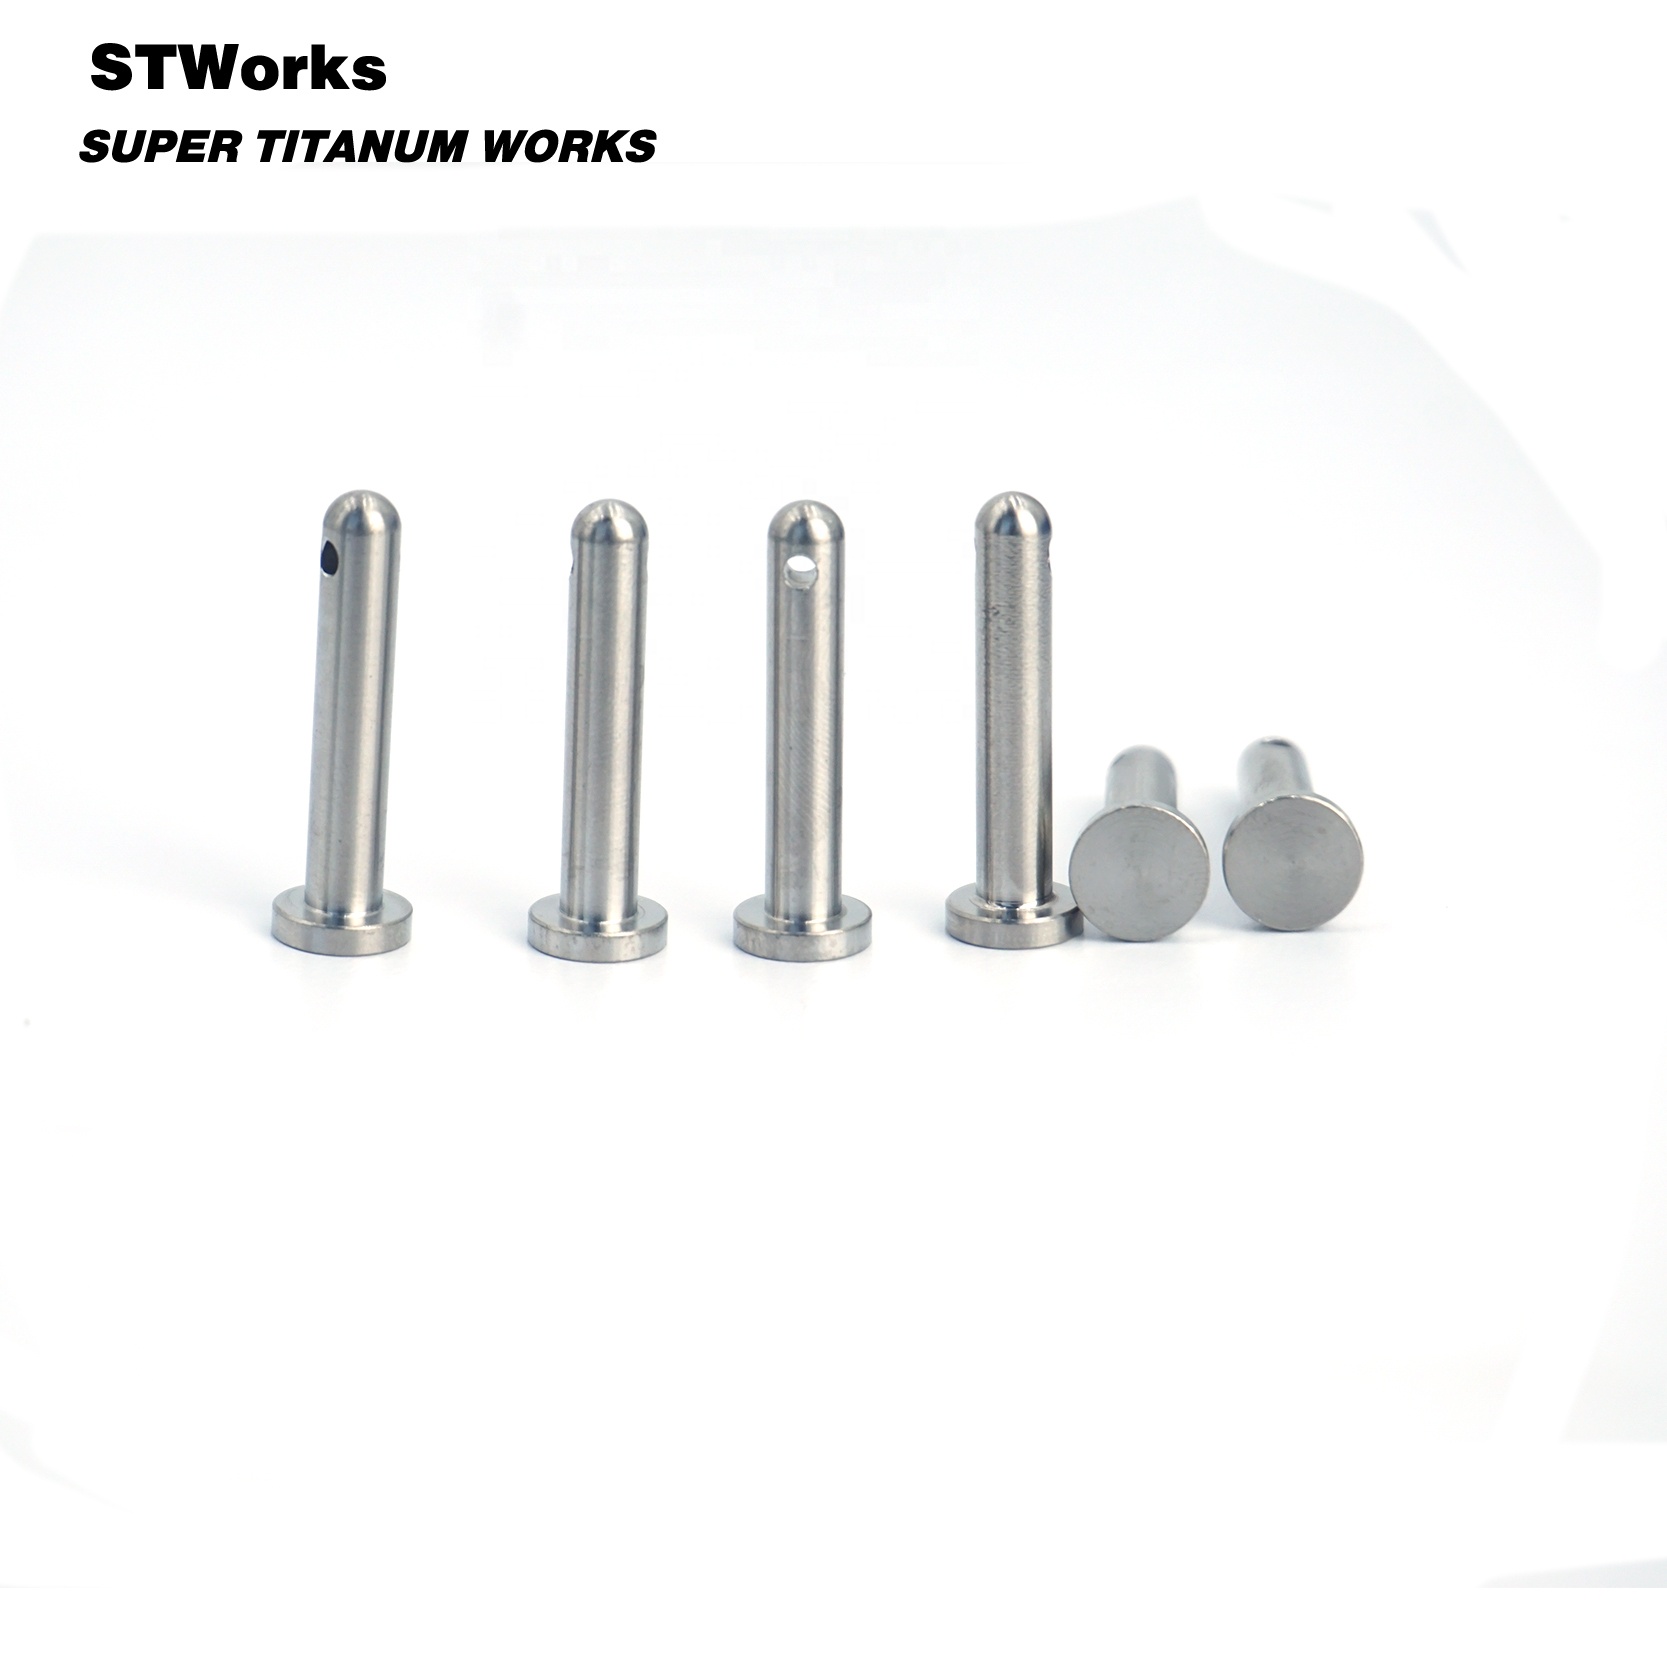
Titanium Alloy Flat Head Clevis Pins with Locating Hole M3-M20
View Product Specs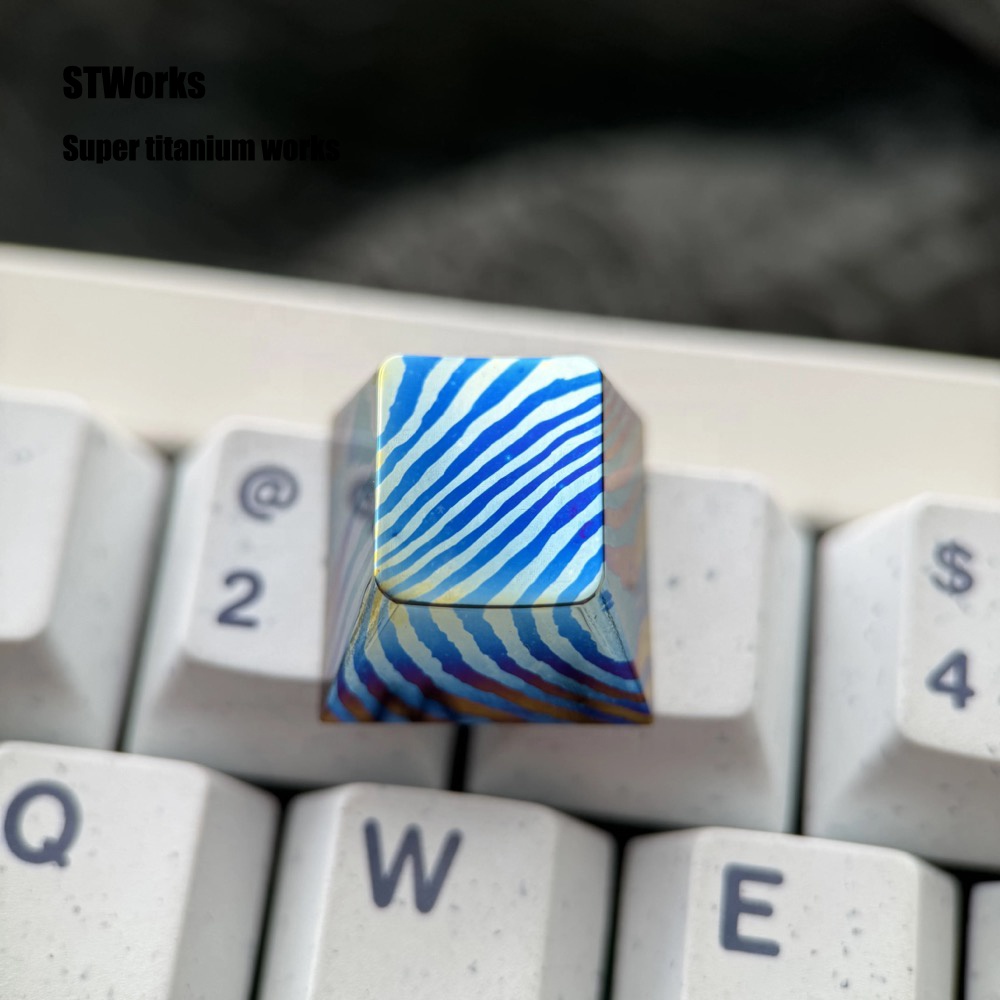
Timascus Alloy Mokuti CNC 1U ESC Keycaps & Custom Accents
View Product Specs
Custom Grade 5 Titanium Serial Identification Plate Tag 1.5mm/2mm
View Product Specs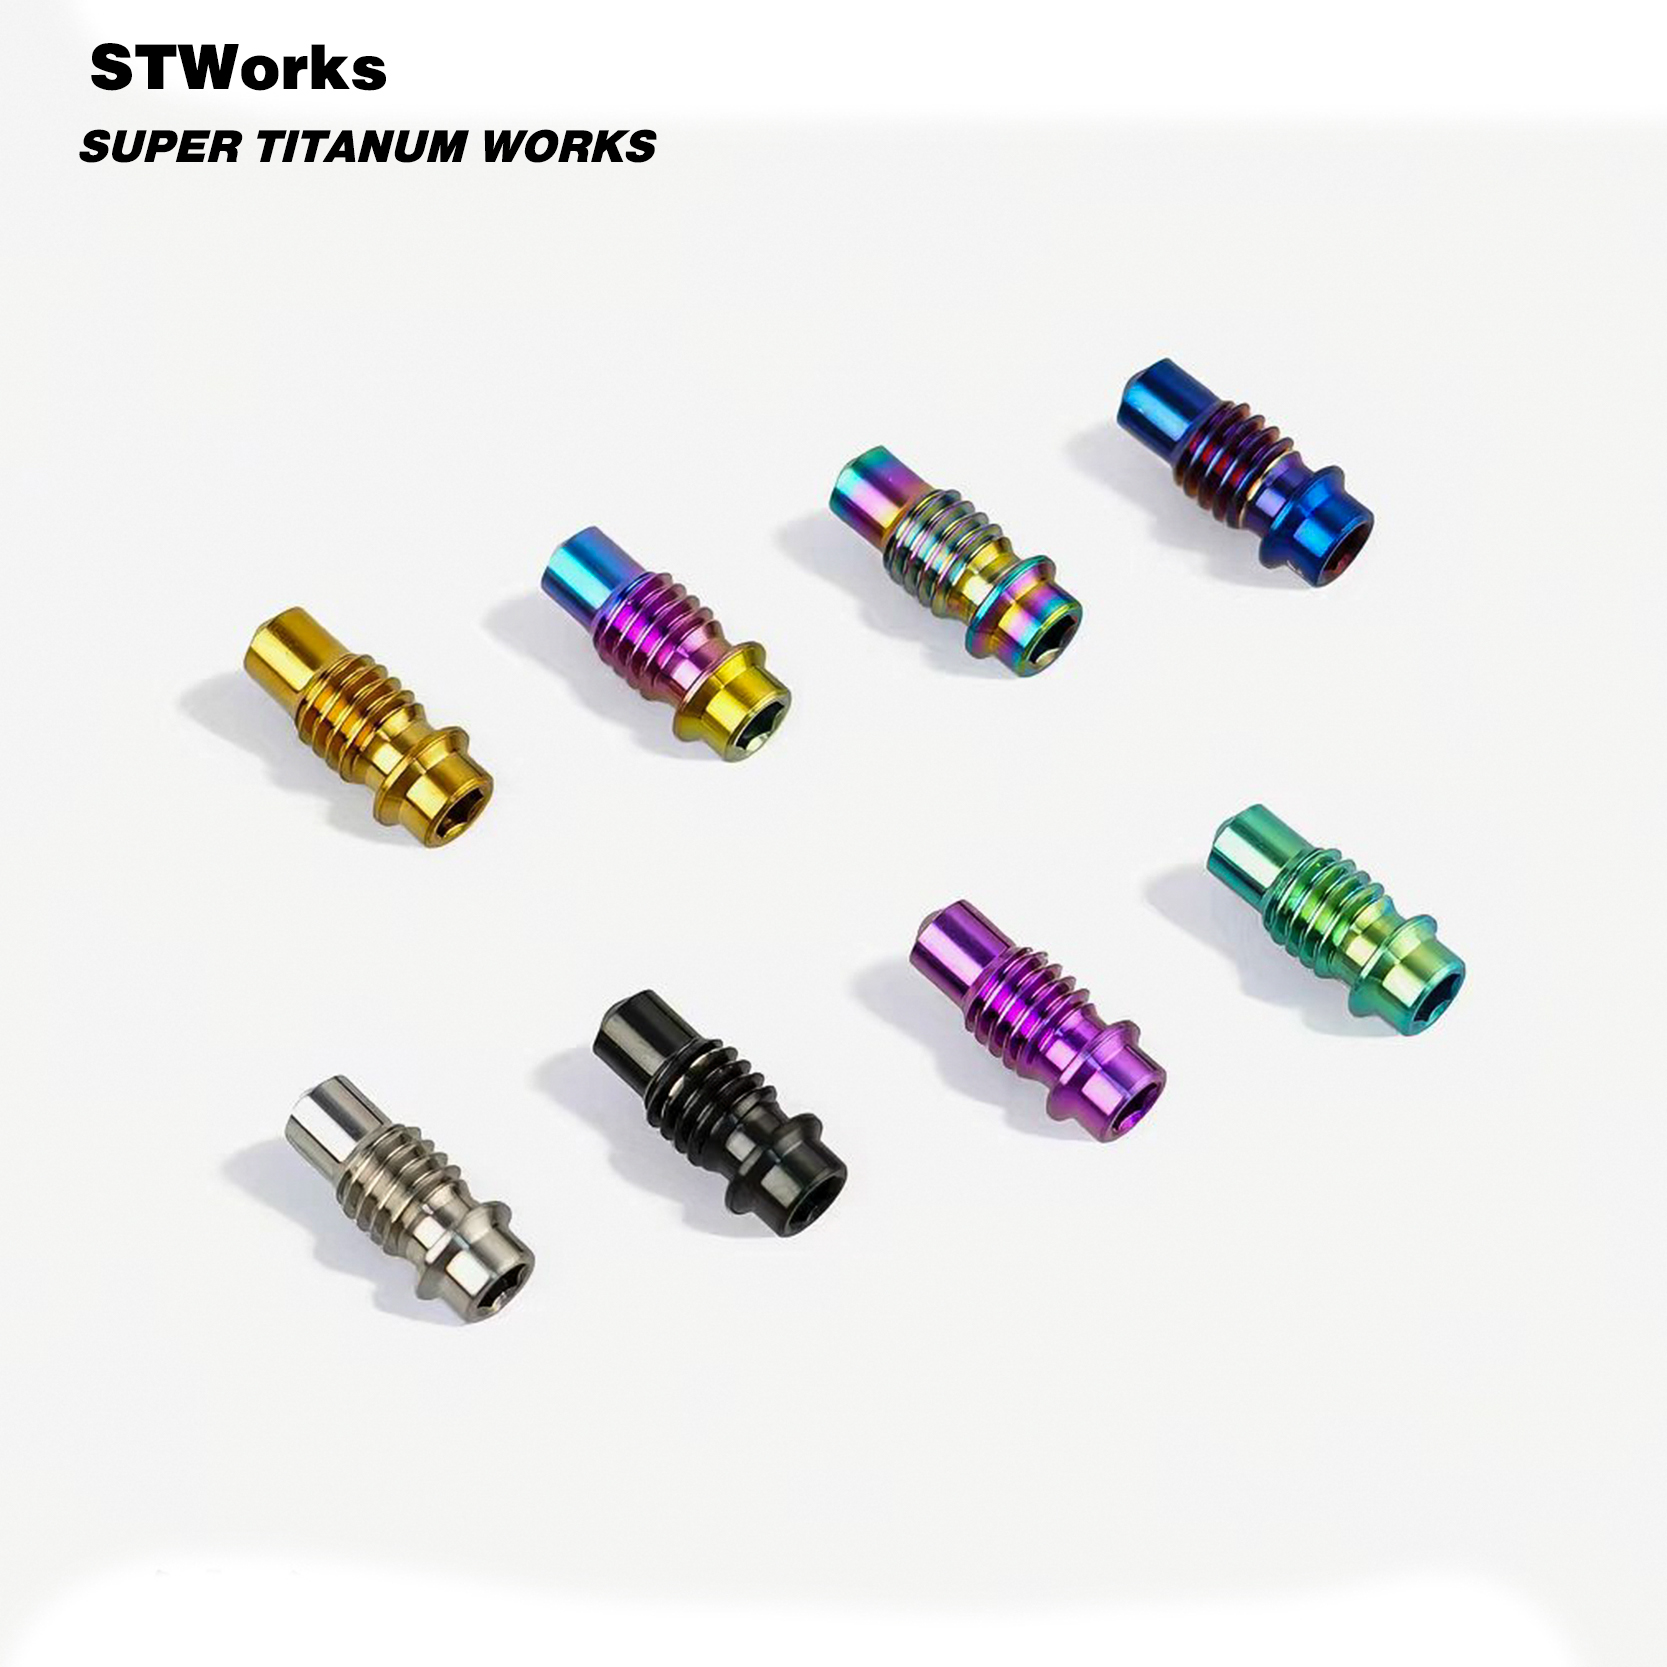
TC4 Titanium Caliper Bleed Port Screw for Shimano Road Disc
View Product Specs
12-Point Titanium 6AL-4V Grade M8x1.25 High-Tensile Lock Nuts
View Product SpecsEngineering Integrity of Titanium Headset Spacers in Precision Bicycle Cockpits
An authoritative analysis of metallurgical selection, parallel-plane perpendicularity, compression dynamics, and galvanic compatibility for B2B procurement professionals serving the Novi Sad regional hub.
In high-performance bicycle architecture, the steering column assembly represents an indispensable junction connecting rider control inputs, front-end impact mitigation, and steering geometry stability. While headset spacers are frequently mischaracterized as purely aesthetic ring components, mechanical engineering analysis proves that they operate as vital axial compression load-bearing sleeves within threadless (Ahead) steering systems. Under the dynamic preload generated by the compression bolt and stem clamp, headset spacers must preserve uncompromising structural parallelism across upper headset bearings, fork steerer tubes (predominantly 1-1/8 inch, 1-1/4 inch, and 1.5 inch tapered designs), and the handlebar stem interface.
Supplying bicycle assembly facilities, bespoke frame workshops, and wholesale distributors in Novi Sad demands an advanced metallurgical approach. Operating at the confluence of the Pannonian Basin and the rolling slopes of Fruška Gora, cyclists in the Vojvodina region subject their equipment to contrasting extremes: rapid urban commuting along the cobblestones and asphalt arteries of Novi Sad, high-cadence touring across the international Danube cycle corridor (EuroVelo 6), and sustained vibration, dust, and moisture on the rugged off-road singletracks of Mt. Fruška Gora. Standard die-cast aluminum or inferior alloy spacers are susceptible to micro-fretting, galvanic corrosion, and compressive deformation over extended mileage. In contrast, precision CNC machined titanium spacers provide an unmatched combination of fatigue life, biological and environmental inertness, and structural modulus parity.
From an engineering standpoint, Velnora manufactures titanium headset spacers utilizing bar stock sourced directly from certified Baoji titanium mills. By implementing multi-axis Swiss-type turning centers, our machining processes achieve concentricity within ±0.01 mm and end-face squareness within 0.015 mm. This industrial-grade precision prevents the erratic preload distribution typical of high-volume punched or extruded components. Whether deployed in custom titanium gravel builds or integrated cable-routed aero cockpits, these spacers eliminate bearing play and withstand the high shear forces induced by disc-brake torsional loading.
Titanium Alloys vs. Legacy Cockpit Materials
Evaluating Grade 5 (Ti-6Al-4V TC4) and Grade 9 (Ti-3Al-2.5V) against 6061-T6 Aluminum and Toray Carbon Fiber in high-compression steering configurations.
| Performance Characteristic | Velnora Gr5 Ti-6Al-4V | Grade 9 (Ti-3Al-2.5V) | 6061-T6 Anodized Aluminum | High-Modulus Carbon Fiber |
|---|---|---|---|---|
| Density (ρ) | 4.43 g/cm³ | 4.48 g/cm³ | 2.70 g/cm³ | 1.55 g/cm³ |
| Tensile Yield Strength | 828 - 910 MPa | 485 - 620 MPa | 240 - 276 MPa | N/A (Anisotropic matrix) |
| Compressive Modulus | 114 GPa | 105 GPa | 69 GPa | Varies (Prone to crush) |
| Galvanic Isolation with Carbon Steerers | Inert (Stable Passive Oxide) | Inert (Passivated) | High Risk (Galvanic Pitting) | Compatible |
| Thermal Expansion (α) | 8.6 × 10⁻⁶ /K | 9.0 × 10⁻⁶ /K | 23.2 × 10⁻⁶ /K | −0.5 to 2 × 10⁻⁶ /K |
| End-Face Crushing Resistance | Extreme (Zero Creep) | High | Moderate (Deforms under 8Nm) | Low (Delamination under shear) |
When engineering an integrated front cockpit, galvanic interaction represents a primary point of failure frequently overlooked by inexperienced sourcing agents. When an aluminum spacer is clamped directly against a carbon fiber steerer tube in the presence of an electrolyte—such as rainwater mixed with road de-icing salt along Novi Sad's Bulevar Oslobođenja during winter—the electrochemical potential difference (approximately 0.9V to 1.1V between carbon and aluminum) induces galvanic battery corrosion. This process oxidizes the aluminum, generating expanding aluminum oxide scales that can crack carbon steerers or seize headset bearings.
Titanium, owing to its spontaneous formation of a tenacious, chemically passive titanium dioxide (TiO&sub2;) boundary layer, exhibits an electrochemical potential virtually identical to that of carbon fiber in practical cycling environments. Consequently, utilizing Velnora titanium headset spacers in 1-1/8" and 1.25" sizes guarantees total galvanic immunity, safeguarding high-value carbon gravel forks against delamination, micro-cracking, and mechanical degradation.
Deploying Titanium Headset Spacers in Novi Sad's Cycling Infrastructure
Engineering solutions adapted to the specialized demands of regional cycling clubs, urban commuting fleets, and custom frame builders throughout South Bačka.
All-Mountain & Enduro Trail Rigidity
The rocky descents and clay singletracks of Fruška Gora (such as the trails near Iriški Venac and Popovica) transmit continuous high-frequency chatter and extreme front-axle torsional shock into the headtube. Titanium spacers absorb mechanical shock waves without crushing, protecting high-end angular contact headset bearings from premature brinelling under aggressive downhill braking.
Transcontinental Gravel & Bikepacking
Novi Sad stands as a critical junction along the Danube EuroVelo 6 transit route. Long-distance expedition cyclists carrying heavy handlebar bags and cockpit roll accessories impose sustained dynamic downward cantilever loads on the stem stack. Velnora's precision CNC turned titanium spacers prevent stack slippage, eliminating play during multi-thousand-kilometer journeys.
Year-Round Climate-Proof Commuting
With Novi Sad's rapidly expanding urban bicycle path network across Liman, Detelinara, and Novo Naselje, daily commuter bikes are exposed to heavy winter salt and industrial grime. Our PVD-coated and hand-brushed titanium spacers remain completely immune to atmospheric acid pitting, guaranteeing maintenance-free service life for rental fleets and urban riders.
Procurement Shifts & Industrial Trends Shaping Novi Sad's Bike Sector
Navigating changing consumer preferences, import regulatory channels via Carina Srbije, and high-margin retail aftermarket strategies.
Premium Aftermarket Customization
Boutique bicycle ateliers in Petrovaradin and central Novi Sad report significant growth in enthusiast demand for bespoke builds. Riders increasingly swap stock black alloy spacers for iridescent rainbow, burnt-blue, or raw brushed titanium to match custom anodized hubs and titanium frame hardware.
E-Gravel & High-Torque Cockpits
The introduction of high-torque motors into gravel and adventure bikes has increased front-end mass and brake torque. Mechanics across Vojvodina require spacers with superior shear resistance that maintain preload consistency under intense dynamic load conditions.
Customs & Freight Optimization
Serbian importers must navigate the regulatory clearance framework of the Customs Administration of Serbia (Uprava Carina). Direct factory sourcing from Velnora provides precise HS Code (8714.99.90) documentation, certified chemical assay sheets, and consolidated air express to Belgrade Nikola Tesla Airport.
Zero-Defect B2B Supply Chains
Rather than dealing with intermediary trading houses, Novi Sad's premier bicycle distributors are securing direct OEM partnerships with Chinese factories capable of offering low MOQs (from 50 units), laser logo personalization, and complete process video verification.
Engineered in Baoji: The Velnora Titanium Advantage
Since 2013, Velnora Titanium Industry has combined aerospace-grade metallurgy with specialized CNC execution to serve over 1,000 international performance brands.
Precision Swiss-Lathe Turning
Our workshop houses multi-spindle CNC turning centers and automated wire-EDM arrays. Every titanium headset spacer is machined from solid cold-drawn Ti-6Al-4V bar, ensuring unbroken grain flow and exceptional radial crush strength.
Electrolytic Anodizing & PVD
We operate in-house computerized anodizing lines capable of producing precise voltage-controlled interference spectrums: ice blue, royal violet, emerald green, and burnt rainbow, as well as wear-resistant Physical Vapor Deposition (PVD) titanium nitride coatings.
Video-Verified Quality Assurance
To eliminate international sourcing uncertainty for buyers in Serbia, Velnora provides on-machine dimensional measurement videos, optical comparator inspection files, and spectrometer batch certificates prior to export dispatch.
Frequently Asked Questions: Sourcing Titanium Headset Spacers in Novi Sad
In-depth answers addressing engineering tolerances, import regulations, surface treatments, and B2B ordering parameters for Serbian buyers.
What dimensional tolerances are maintained on Velnora titanium headset spacers?
Our standard production tolerances conform to precision ISO 2768-m standards. For critical cockpit contact zones, we machine internal diameters (ID) to 28.75 mm ±0.05 mm (designed for standard 1-1/8 inch / 28.6 mm steerer tubes) and outer diameters (OD) to 31.8 mm ±0.05 mm to align seamlessly with typical road and MTB stem profiles. Crucially, end-face parallelism and perpendicularity are verified within ≤0.015 mm. This tight face-squareness prevents uneven compression against the headset compression ring, eliminating bearing drag and micro-knocking.
Can titanium spacers cause abrasive wear on lightweight carbon fiber steerer tubes?
No, provided the internal bore edges are appropriately radius-chamfered. Cheap punched steel or low-grade aluminum spacers often feature razor-sharp inner burrs that notch and score epoxy resin on carbon fork steerers during stem adjustment. All Velnora titanium spacers undergo precision interior edge chamfering (0.3 mm × 45°) followed by automated magnetic deburring and vibratory polishing. This creates a completely smooth contact surface that slides effortlessly over carbon, aluminum, or titanium steerer columns without abrasion.
How does the Serbian customs clearance process function for commercial B2B shipments into Novi Sad?
For bicycle component shipments destined for Novi Sad, customs processing is handled through the regional Customs Office Novi Sad (Carinarnica Novi Sad) or at Belgrade Nikola Tesla Airport (for DHL/FedEx Express consignments). We classify titanium headset spacers under HS Code 8714.99.90 (Parts and accessories of bicycles: Other). We supply full commercial documentation including certified Commercial Invoices, Packing Lists with detailed net/gross weights, and Certificate of Origin (COO) documentation. Serbian VAT (PDV of 20%) and applicable customs duties are calculated upon arrival based on the CIF valuation.
What spacer height configurations are available for bulk OEM and wholesale distribution?
We manufacture standard spacer sets in vertical heights of 2 mm, 3 mm, 5 mm, 10 mm, 15 mm, and 20 mm. For aerodynamic cockpits and proprietary integrated cable designs, we produce custom teardrop, D-shape, and internal channel routing geometries tailored to specific client 3D STEP models. Standard thickness profiles are optimized at 0.9 mm to 1.1 mm wall gauge, delivering an ultra-lightweight component that preserves uncompromising axial rigidity under full stem clamp torques (typically 5 to 7 Nm).
How durable is the anodized color finish in wet and saline environments?
Unlike aluminum anodizing, which relies on organic or inorganic chemical dyes trapped inside porous oxide pores that can fade under strong solar UV radiation, titanium anodizing is an electrochemical process that grows a transparent titanium dioxide (TiO&sub2;) optical interference layer. The observed color is produced purely by light refractivity. Because no dyes are introduced, the colors will never bleach under direct sunlight, nor will they chip or flake off when exposed to the mud, moisture, and road salts encountered around Fruška Gora and Novi Sad.
What are the minimum order quantities (MOQ) and production lead times for custom laser-etched spacers?
For standard round 1-1/8" titanium spacers in raw brushed or mirror-polished finishes, our MOQ starts at 50 pieces per size specification. For custom-anodized batches or components requiring fiber-laser engraving (such as local bike shop logos, cycling club insignias, or custom serial numbers), the MOQ is 100 sets. Prototype and sample batches are dispatched within 5 to 7 business days, while volume production runs (500 to 5,000 units) require 15 to 22 business days, followed by 4-6 days air transit directly into Serbia.
Request an Engineering Quotation & Sample Run
Submit your steerer diameter requirements, height assortment, desired finish, and batch volume. Our senior titanium machining engineers will analyze your specifications and return a comprehensive B2B quotation within 4 business hours.