Ti-6Al-4V Gr5

Machined from ultra-dense Ti-6Al-4V billets. Rolled threads, anti-galling geometry, and precision-broached drives built to withstand demanding torque loads and tropical marine environments.
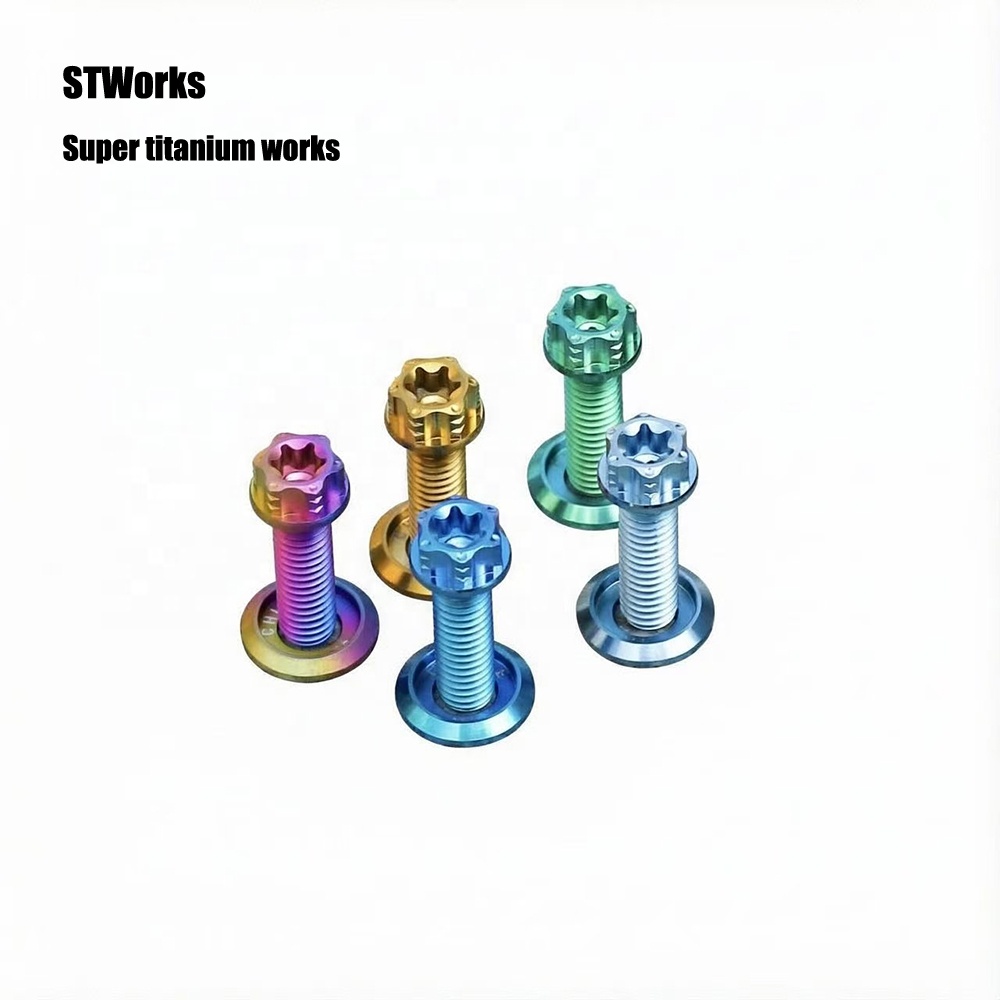

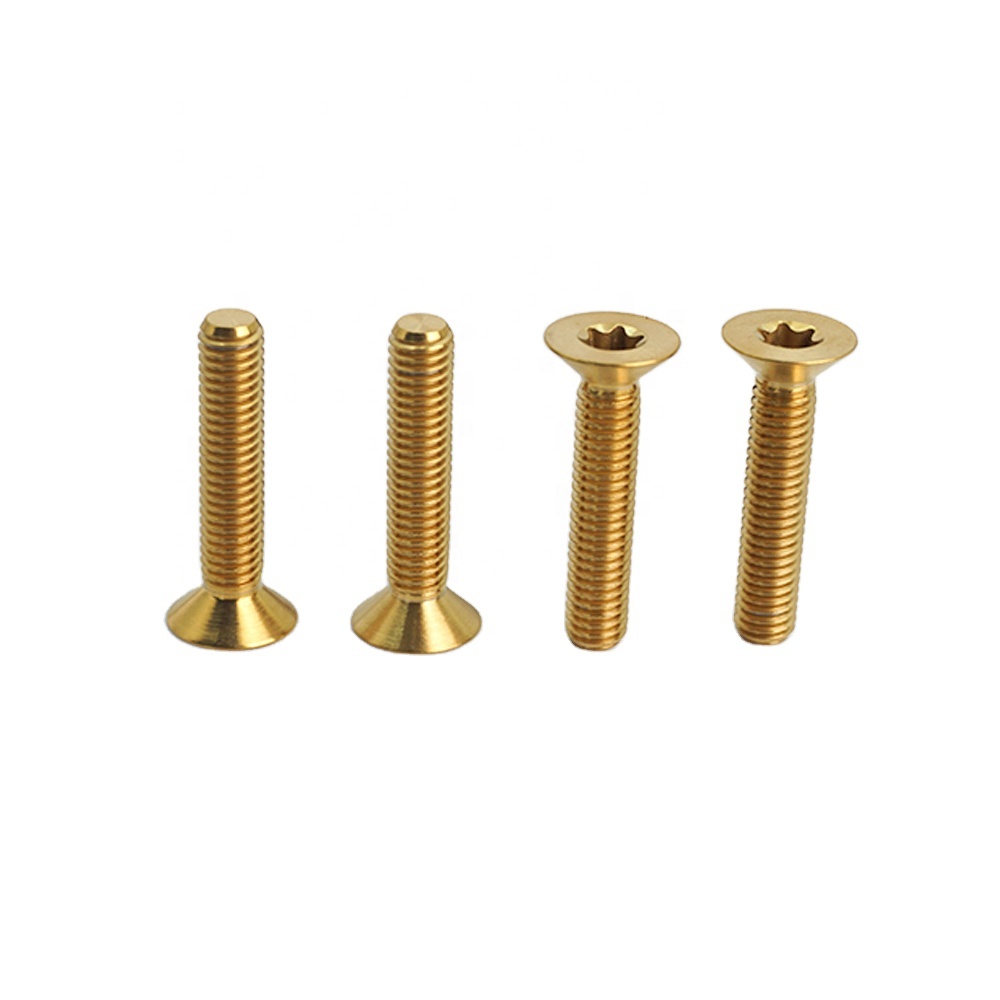
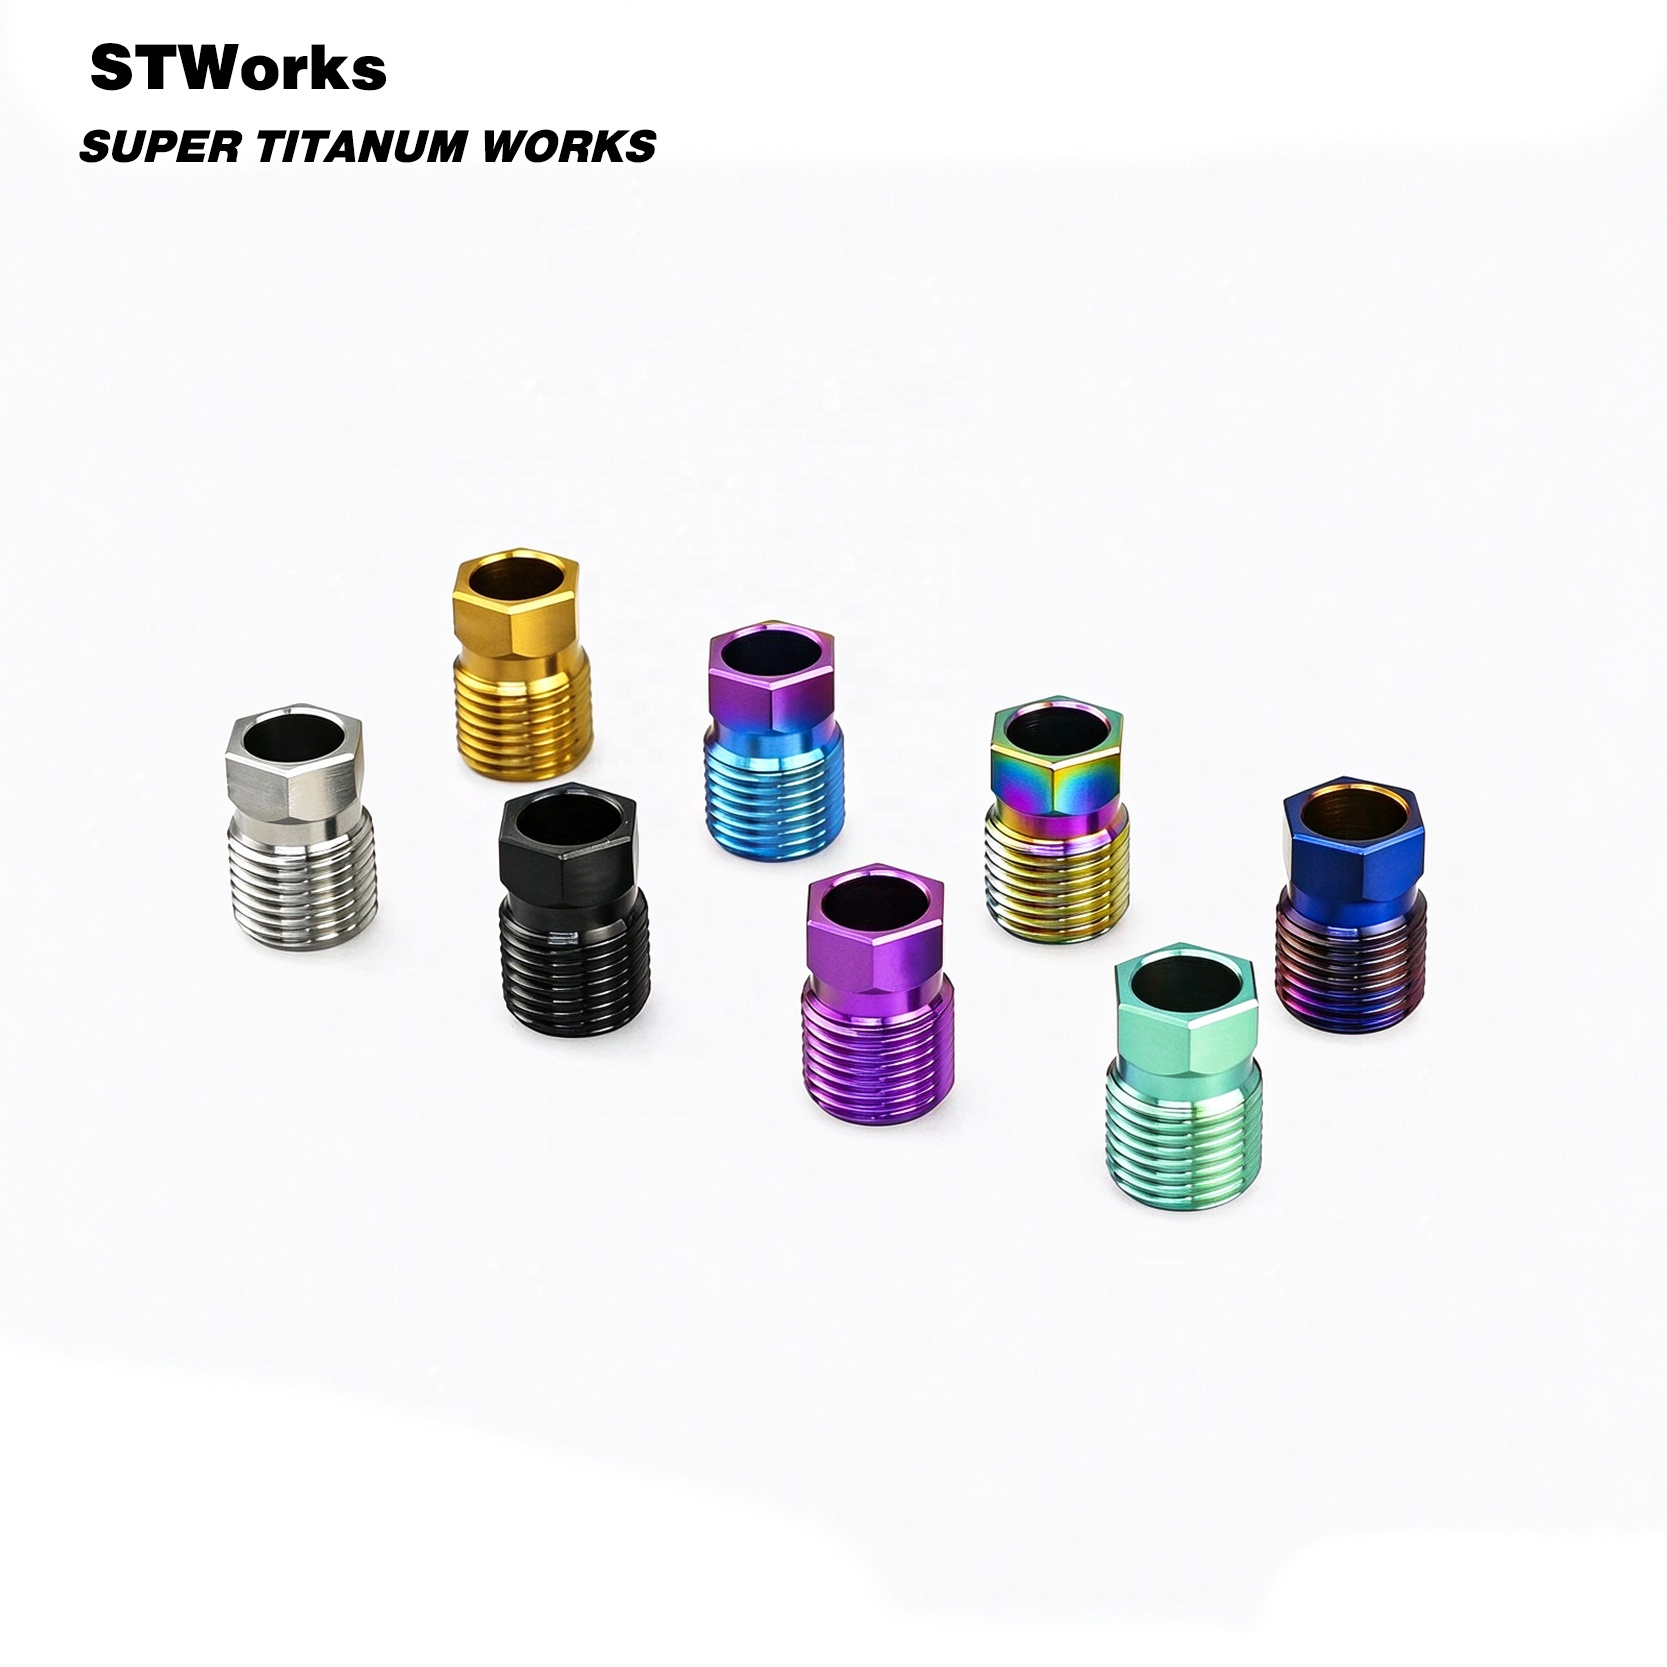
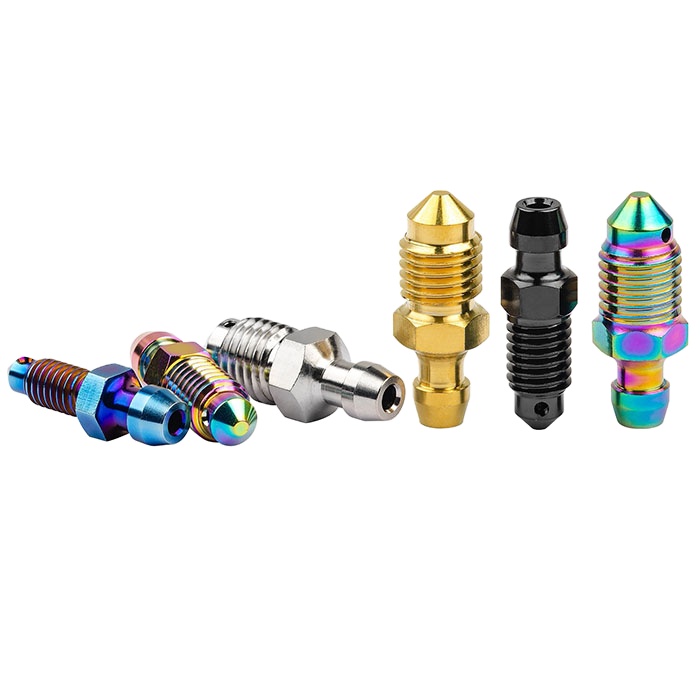
Deploying rotor fasteners in St. George’s requires an understanding of acute saltwater corrosion, coastal humidity, volcanic dust abrasives, and high dynamic shear loads.
St. George’s coastal geography subjects mechanical assemblies to continuous salt-spray aerosols. Standard 8.8 grade carbon and zinc-plated rotor bolts experience rapid oxidation, rust bleeding, and severe hydrogen embrittlement. Grade 5 Ti-6Al-4V titanium creates a self-healing titanium dioxide (TiO2) ceramic film that makes rotor hardware completely impervious to chloride pitting and oceanic corrosion.
Sustained descent braking across steep coastal topographies causes thermal transfer up to 550°C into disc brake hats and hub flanges. Unlike austenitic stainless steel bolts (such as SS304 or SS316), which anneal, stretch, and undergo thread relaxation under brake friction heat, TC4 titanium maintains consistent clamping tension, preserving rotor run-out and preventing warpage.
For custom racing cars, ATVs, and competition mountain bikes navigating the island’s demanding circuits, reducing unsprung rotational weight on wheel hubs translates directly to enhanced damper response and reduced gyroscopic inertia. Switching from steel rotor hardware to Grade 5 titanium delivers an immediate 44% weight reduction at the outer perimeter of the hub assembly.
Empirical mechanical data highlighting why precision CNC-machined Grade 5 Titanium is the premier engineering standard for critical braking junctions.
| Performance Metrics | Grade 5 Titanium (Ti-6Al-4V) | Class 10.9 Carbon Steel | A2-70 (304) Stainless Steel | 7075-T6 Billet Aluminum |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 (44% Lighter) | 7.85 | 7.93 | 2.81 |
| Tensile Strength (MPa) | 950 – 1050 | 1040 | 700 | 570 |
| Yield Strength (MPa) | 880 – 920 | 940 | 450 | 505 |
| Chloride Salt-Fog Rating | Immune (ASTM B117 >2000 hrs) | Severe Pitting / Rust in 24 hrs | Crevice Corrosion within 120 hrs | Galvanic Pitting / Exfoliation |
| Thermal Stability (>400°C) | No Microstructural Drift | Tempering Decay | Severe Creep & Stretching | Failure at >150°C (Unsafe) |
| Recommended Rotor Usage | Critical High-Stress Hub Interfaces | OEM Mass Production Base | Low-Stress Ancillary Only | Forbidden on Brakes |
Headquartered in Baoji—known globally as China's Titanium Valley—Velnora Titanium Industry Co., Ltd. has specialized exclusively in the precision engineering and export of premium titanium fasteners since 2013. We control every stage of production, avoiding melted scrap stock in favor of vacuum-arc remelted (VAR) certified titanium bar.
How fleet operators, engineering shops, and performance customizers in St. George's are optimizing their procurement lifecycles.
Maintenance engineers in St. George’s are replacing repetitive purchases of cadmium or zinc-plated steel bolts with permanent titanium fasteners. While the initial procurement cost is higher, Grade 5 titanium eliminates premature bolt failure, frozen threads, and labor-intensive drilling out of rusted hardware, lowering long-term operational costs across commercial marine and fleet vehicles.
Sourcing standards across Grenada and the Caribbean increasingly mirror rigorous North American and European metrics. Local performance builders and marine workshops specify DIN 912 socket caps, ISO 7380 low-profile button heads, and customized DIN 7991 countersunk configurations with comprehensive chemical and physical mill certificates (EN 10204 3.1).
Forward-thinking distributors in St. George’s are bypassing intermediaries to work directly with specialist manufacturers. This direct pipeline ensures access to custom thread pitches, personalized laser batch-marking, specialized PVD vacuum vapor depositions (Burnt Blue, Gold, DLC Black), and flexible low minimum order quantities (MOQs).
Detailed technical and logistical answers addressing thread friction, torque values, customs compliance, and supply chain timelines.
Yes. Grade 5 titanium (Ti-6Al-4V) exhibits an ultimate tensile strength exceeding 950 MPa and a yield strength over 880 MPa, closely matching Class 10.9 steel fasteners while remaining significantly stronger than standard Class 8.8 bolts. Furthermore, Grade 5 titanium boasts exceptional shear strength and superior fatigue life under repetitive rotational stress, making it an ideal choice for high-performance automotive and motorcycle brake discs.
Titanium and aluminum have different galvanic potentials and can gall under dry, high-friction thread engagement. We recommend applying a dedicated nickel-based anti-seize compound, copper paste, or medium-strength anaerobic thread locker (e.g., Loctite 243) to the bolt threads. This isolates the surfaces, prevents cold-welding, ensures accurate torque transmission, and protects the interface in salt-laden coastal conditions.
Because titanium has a modulus of elasticity roughly half that of steel (~114 GPa vs. ~210 GPa), tightening torques must be carefully calibrated. For bicycle M5 Torx T25 rotor screws, the recommended torque is 5.0 to 5.7 Nm. For automotive or motorcycle M6 and M8 flange bolts, target approximately 85% to 90% of the OEM dry torque spec if anti-seize or threadlocker is used. Always follow star-pattern tightening sequences and use calibrated click-type torque wrenches.
Our anodized finishes are created via controlled voltage oxidation, creating a structural titanium dioxide surface film that uses no pigments and will not chip or flake from UV exposure. For higher wear resistance in harsh conditions, we also provide physical vapor deposition (PVD) coatings (such as DLC Black, Titanium Nitride Gold, and Burnt Titanium), which provide surface hardness up to 2500 HV to resist rock and debris impacts.
Standard fasteners (M5, M6, M8 sizes in stock) ship within 48 to 72 hours via DHL Express, FedEx Priority, or air freight, typically arriving in St. George’s within 5 to 9 business days with door-to-door tracking. Custom CNC components built from CAD files (STEP/IGES) usually require 15 to 20 days for machining and surface finishing. Typical production MOQs start at 50 to 100 units per spec, with custom samples available upon review.
From raw material traceability in Baoji to rigorous multi-stage quality control, we build high-reliability partnerships for international distributors.
We source exclusively from top-tier Baoji melters. Every production run is accompanied by a Material Test Report (MTR) confirming chemical compliance (Aluminum 5.5–6.75%, Vanadium 3.5–4.5%, Iron <0.40%, Oxygen <0.20%) and strict ASTM B348 / AMS 4928 standards.
Our workshop houses high-precision Japanese Citizen multi-axis Swiss-turning lathes. Threads are produced via high-pressure thread-rolling dies rather than single-point cutting, preserving metallurgical grain flow and raising cycle-fatigue resistance by over 30%.
We provide full transparency throughout manufacturing. Clients receive live CNC process photos, optical comparator dimensional inspections, thread ring-gauge checks, and video walk-throughs before final dispatch.
Consult with our applications engineering desk. Send us your dimensional specs, 2D/3D CAD geometries (STEP, IGES, PDF), or OEM part numbers to receive a comprehensive quote and DFM analysis within four hours.
Inquire Now