Timascus Custom
Engineered in Baoji's Titanium Valley to strict DIN, ISO, and JIS motorsport standards. Available in cold-rolled precision threads with physical vapor deposition (PVD) anti-galling treatments.
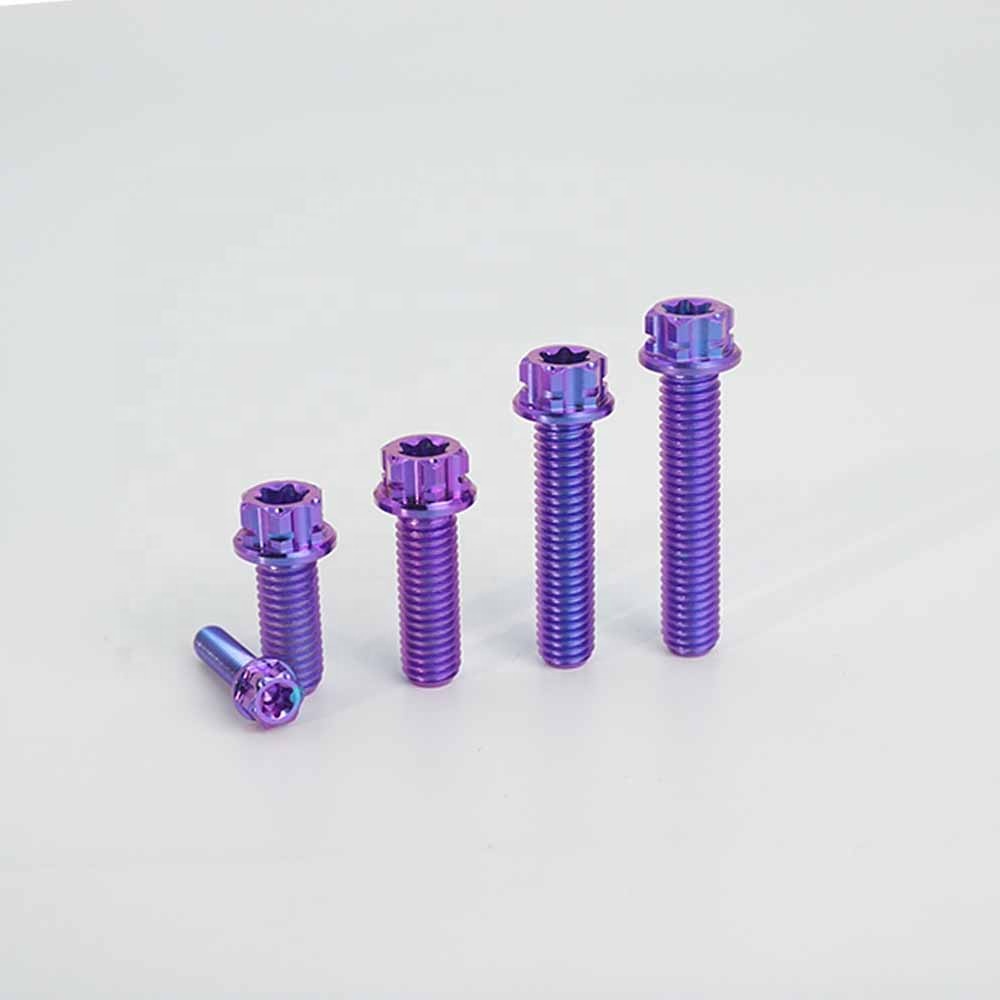
A quantitative metallurgical evaluation comparing titanium fastener dynamics against steel grades and aerospace aluminum under Texas race-track thermal cycles.
| Material Classification | Velnora Grade 5 Ti-6Al-4V | Class 8.8 High-Tensile Steel | Class 10.9 Structural Steel | 7075-T6 Aerospace Aluminum |
|---|---|---|---|---|
| Mass Density (g/cm³) | 4.43 | 7.85 | 7.85 | 2.81 |
| Tensile Strength (MPa) | 920 – 1,050 | 800 – 830 | 1,000 – 1,040 | 540 – 570 |
| Strength-to-Weight Index (kN·m/kg) | 214 – 237 | 102 – 105 | 127 – 132 | 192 – 202 |
| Thread Manufacturing Method | Precision CNC Thread-Rolled | Cut / Thread-Rolled | Cold Forged / Rolled | Cut or Rolled Threads |
| Corrosion in Humid/Salt Track Conditions | Immune (Passive TiO&sub2; Layer) | High Oxidation Risk (Rust) | Requires Plating / Zinc-Flake | Galvanic Pitting Prone |
| Continuous Operating Temp Limit (°C) | 400°C | 300°C | 350°C | 120°C (Softens) |
| Primary San Antonio Application | Wheel Studs, Caliper Bolts, Rotors | General OEM Replacement | Heavy Suspension Arms | Cosmetic Fairings / Brackets |
The Greater San Antonio motorsport corridor represents one of the most mechanically demanding environments for performance fasteners in North America. From the high-heat quarter-mile sprints at Alamo City Motorplex in Marion to technical track days through the Texas Hill Country at Harris Hill Raceway and Circuit of the Americas (COTA) in nearby Austin, racing vehicles undergo brutal vibration frequencies, sustained braking rotor heat, and punishing ambient track temperatures that regularly exceed 130°F on Texas asphalt during peak summer events.
When high-performance engine builders, privateer motorcycle race teams, and speed shops across Bexar County transition from OEM carbon steel fasteners to titanium, selecting the right manufacturing process is critical. Velnora Titanium Industry Co., Ltd. provides direct industrial factory access to custom-turned and cold-rolled Grade 5 Ti-6Al-4V fasteners, eliminating unnecessary intermediate distributor markups while delivering traceable material certificates.
Different motorsport disciplines present unique kinematic stress concentrations. Below are the specific operational sectors in San Antonio where precision titanium fasteners provide significant performance gains:
Pro mod drag cars, Foxbody setups, and LS-swapped machines running at Alamo City Motorplex demand minimal rotational inertia. Grade 5 titanium wheel studs, beadlock bolts, and flywheel hardware eliminate critical grams from rotating assemblies while sustaining high shear stress under immediate torque launches.
Central Texas superbike racers on Yamaha R1s, Kawasaki ZX-10Rs, and Ducati Panigales swap heavy unsprung steel brake hardware for our OEM CNC Machined M8×23 disc brake screws and caliper mounting bolts, delivering crisper turn-in response and reduced gyroscopic resistance.
Hill Country rocky trails and South Texas caliche ranches punish suspension hardware with gritty particulate abrasion and thermal cycling. Our Ti-6Al-4V flanged bolts and lock nuts resist corrosion while sustaining extreme shock loads across trailing arms and beadlocks.
San Antonio is undergoing an industrial and performance evolution that makes advanced lightweight alloys indispensable:
Velnora Titanium Industry Co., Ltd. (operating from Baoji, China's central Titanium Valley since 2013) combines direct raw titanium sponge refining access with dedicated high-speed 5-axis CNC turning and thread rolling centers. Central Texas clients benefit directly from our end-to-end quality ecosystem:
Straightforward technical answers to streamline your titanium fastener procurement process.
Grade 5 (Ti-6Al-4V) titanium delivers a minimum tensile strength of roughly 895 to 950 MPa, making it an ideal drop-in replacement for Class 8.8 structural bolts and most Class 10.9 non-critical fasteners, providing an immediate 44% mass reduction. However, for Class 12.9 applications where extreme clamping preload exceeds 1,200 MPa (such as connecting rod cap bolts or high-stress suspension pickup points), titanium requires upsizing the bolt diameter or verifying the joint with a mechanical stress calculation. Contact our engineering team for joint stress evaluations.
Titanium naturally develops a microscopic oxide layer which, under high contact friction, can gall against raw aluminum or other titanium mating surfaces. To prevent galling on frequently disassembled race hardware (such as caliper bolts or wheel hubs), always use a copper-based, nickel-based, or molybdenum disulfide anti-seize paste. Additionally, opting for our Physical Vapor Deposition (PVD) titanium nitride surface treatment substantially decreases thread friction and prevents cold welding.
Standard stocked catalog hardware ships within 48 to 72 hours via expedited international couriers (DHL Express, FedEx Priority) directly to San Antonio International Airport (SAT) customs clearance hubs, arriving in Central Texas within 4 to 6 business days. Custom CNC machining from client CAD blueprints (STEP, IGES, PDF) generally requires 15 to 22 working days for precision tooling, threading, surface passivation, and inspection video sign-off.
Yes. While our core catalog features standard metric specifications (DIN 912, DIN 6921, ISO 7380 from M3 to M24), our multi-axis CNC lathes regularly cut precision imperial thread profiles including 1/4"-20, 5/16"-18, 3/8"-24, 7/16"-20, and 1/2"-20 for vintage muscle cars, Pro Mod drag racing chassis, and specialized American transmission mounts.
Every manufacturing heat lot is tested using optical emission spectrometry to ensure exact Grade 5 Ti-6Al-4V chemical composition (Aluminum 5.5–6.75%, Vanadium 3.5–4.5%, Iron ≤ 0.40%, Oxygen ≤ 0.20%, Balance Titanium). Material Test Reports (MTR) according to EN 10204 3.1, along with optical projector thread dimension reports, are included with every export shipment to Texas.