Gr5 TC4 Alloy
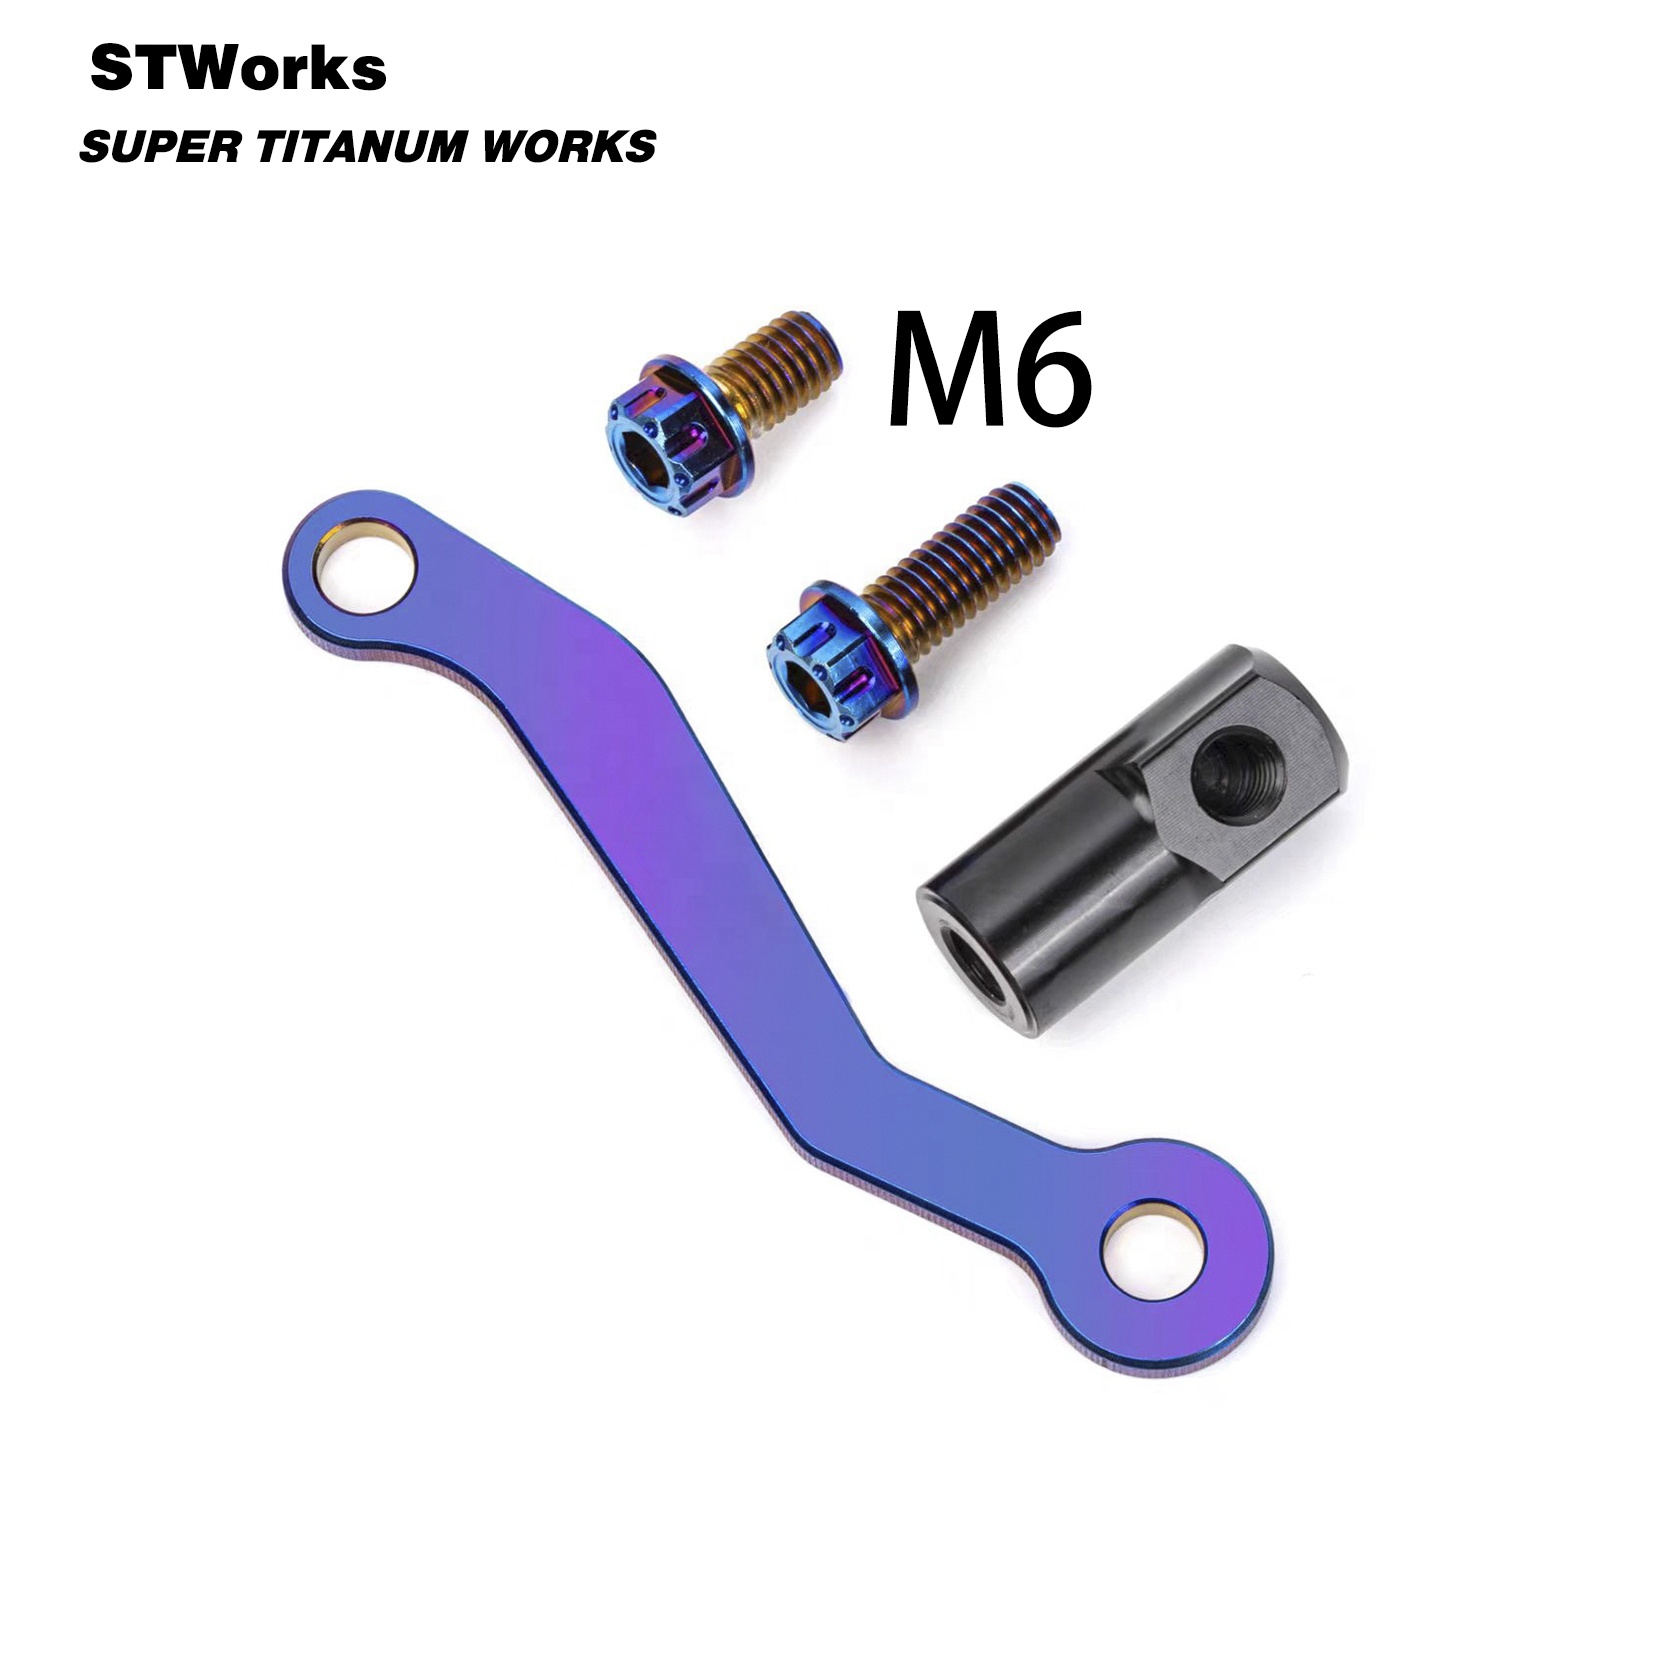
Gr5 TC4 Titanium Alloy Brake Fluid Reservoir Mount Bracket
For Radial Master Cylinder Motorcycle & E-Bike Systems
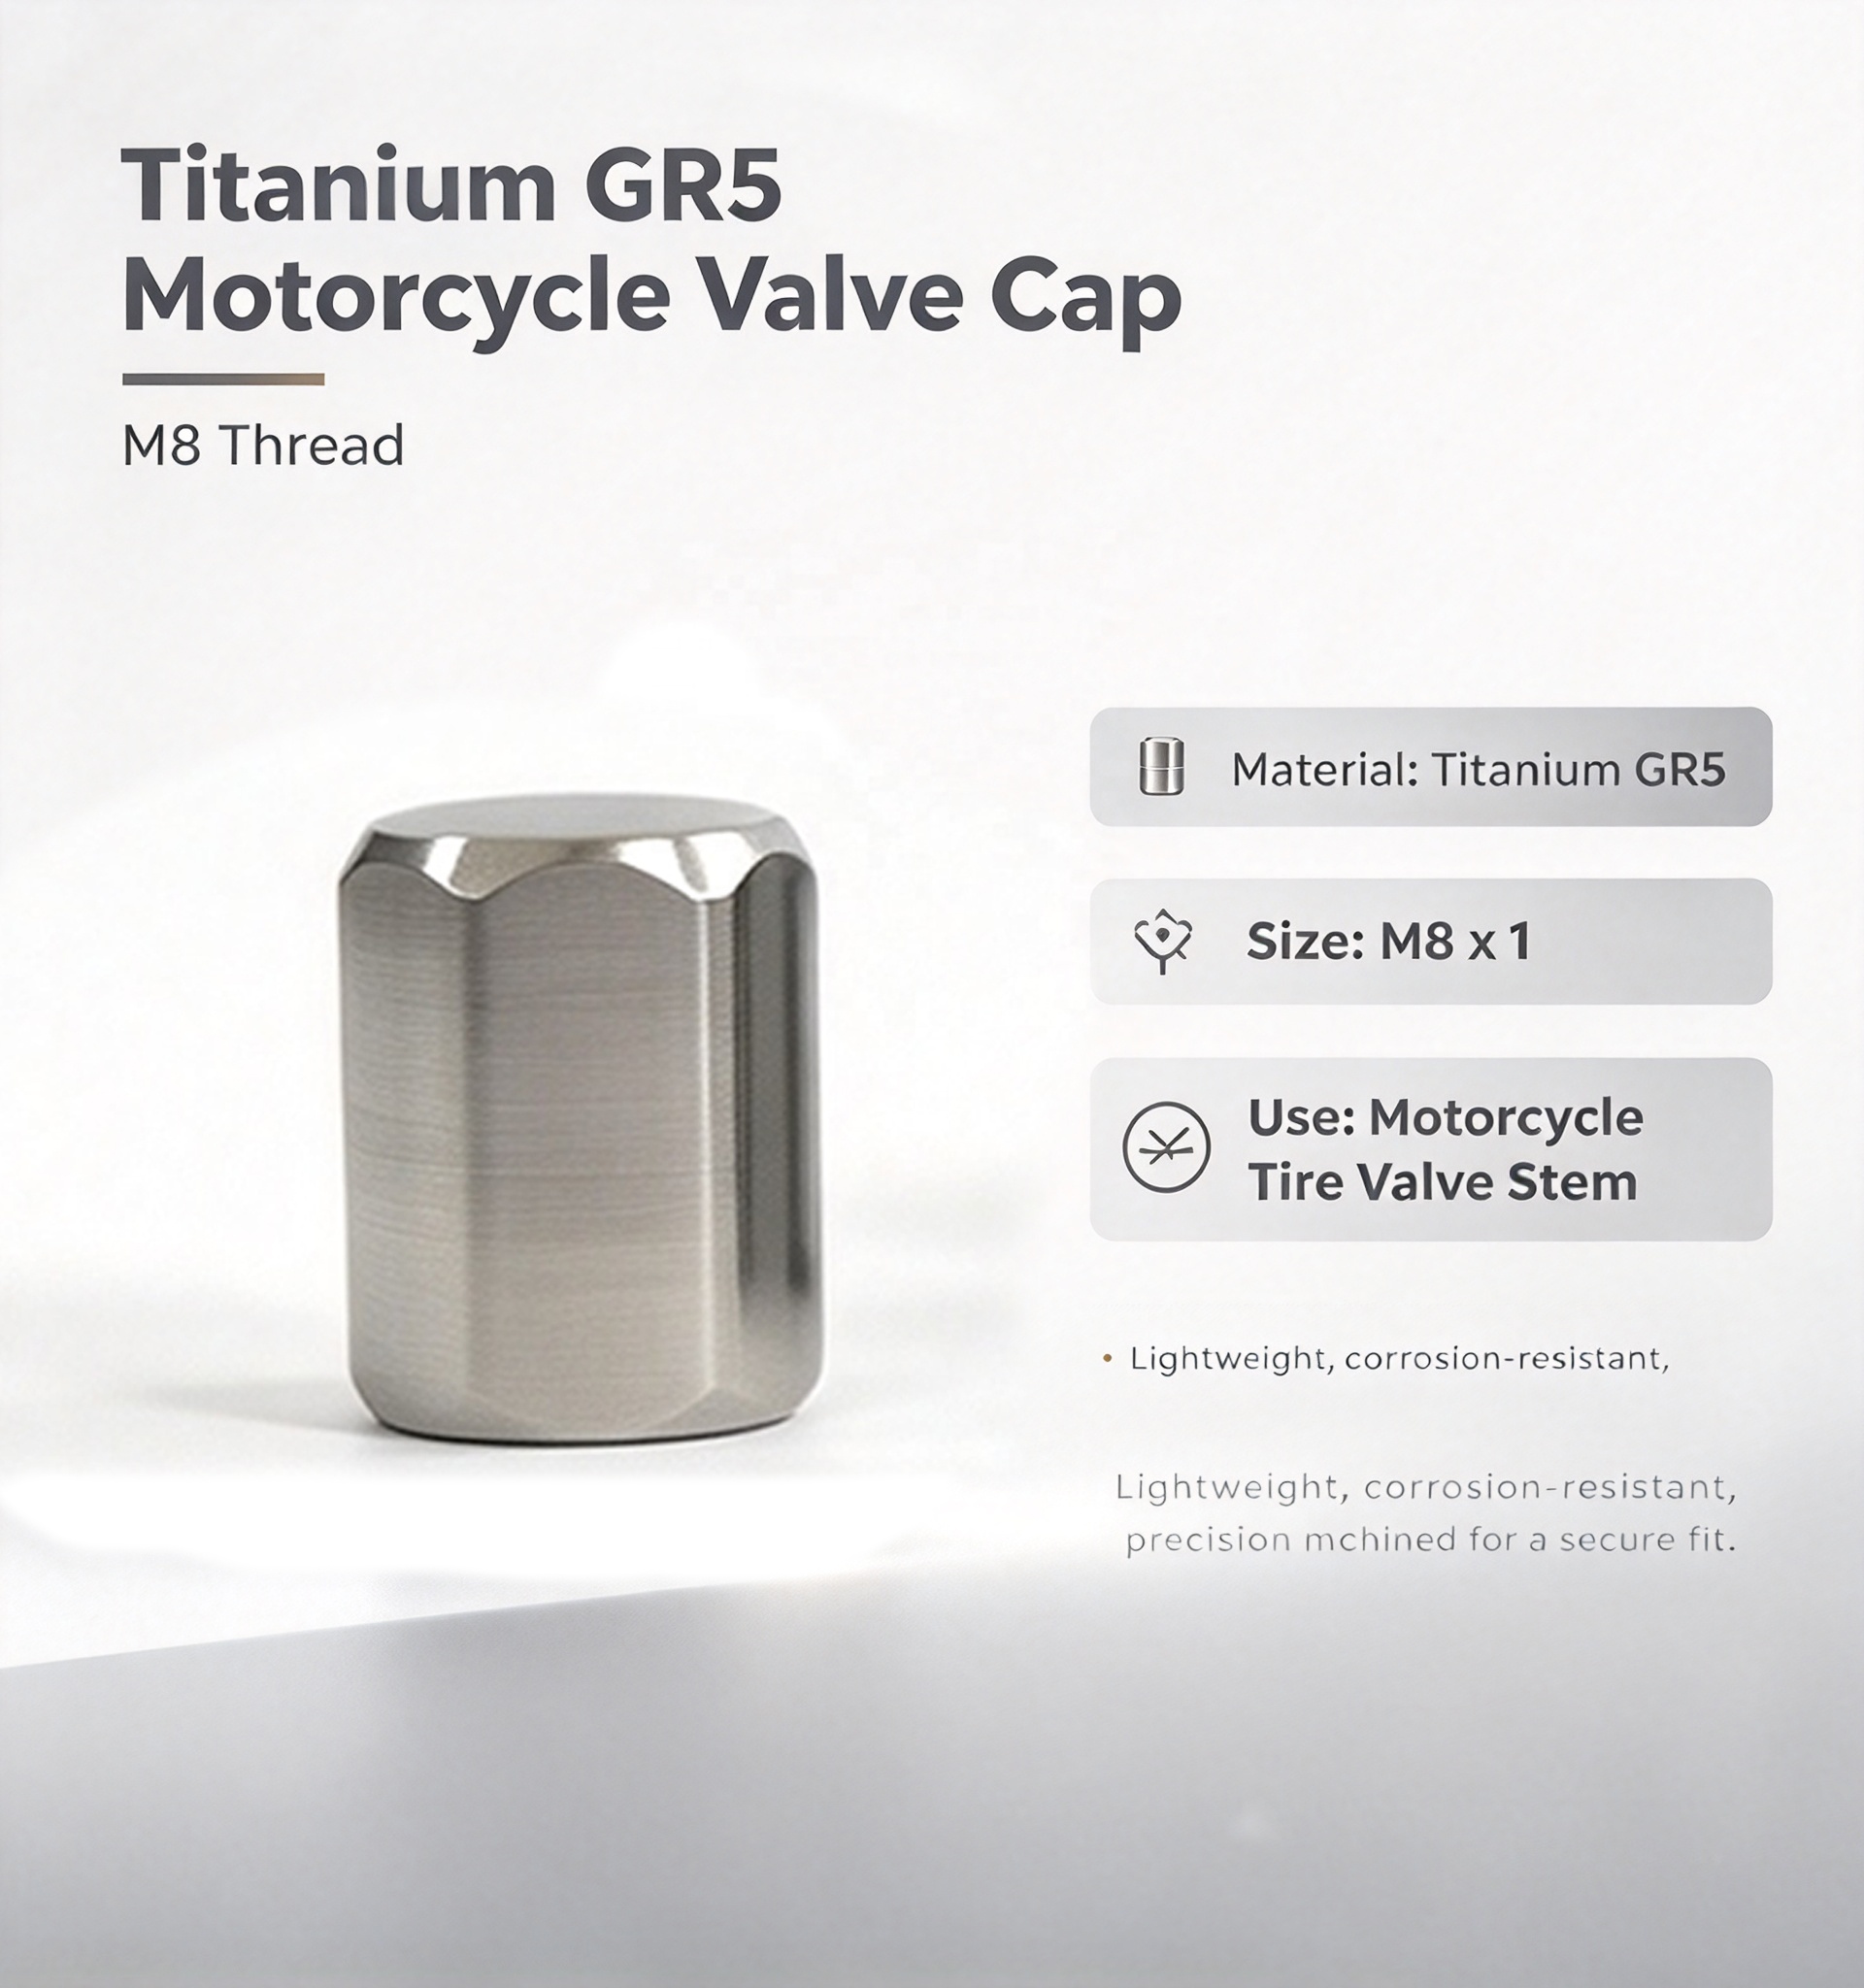
Engineered for high strength-to-weight ratios, extreme corrosion immunity, and tight dimensional repeatability. Below are eight of our core CNC machined and cold-formed titanium solutions.

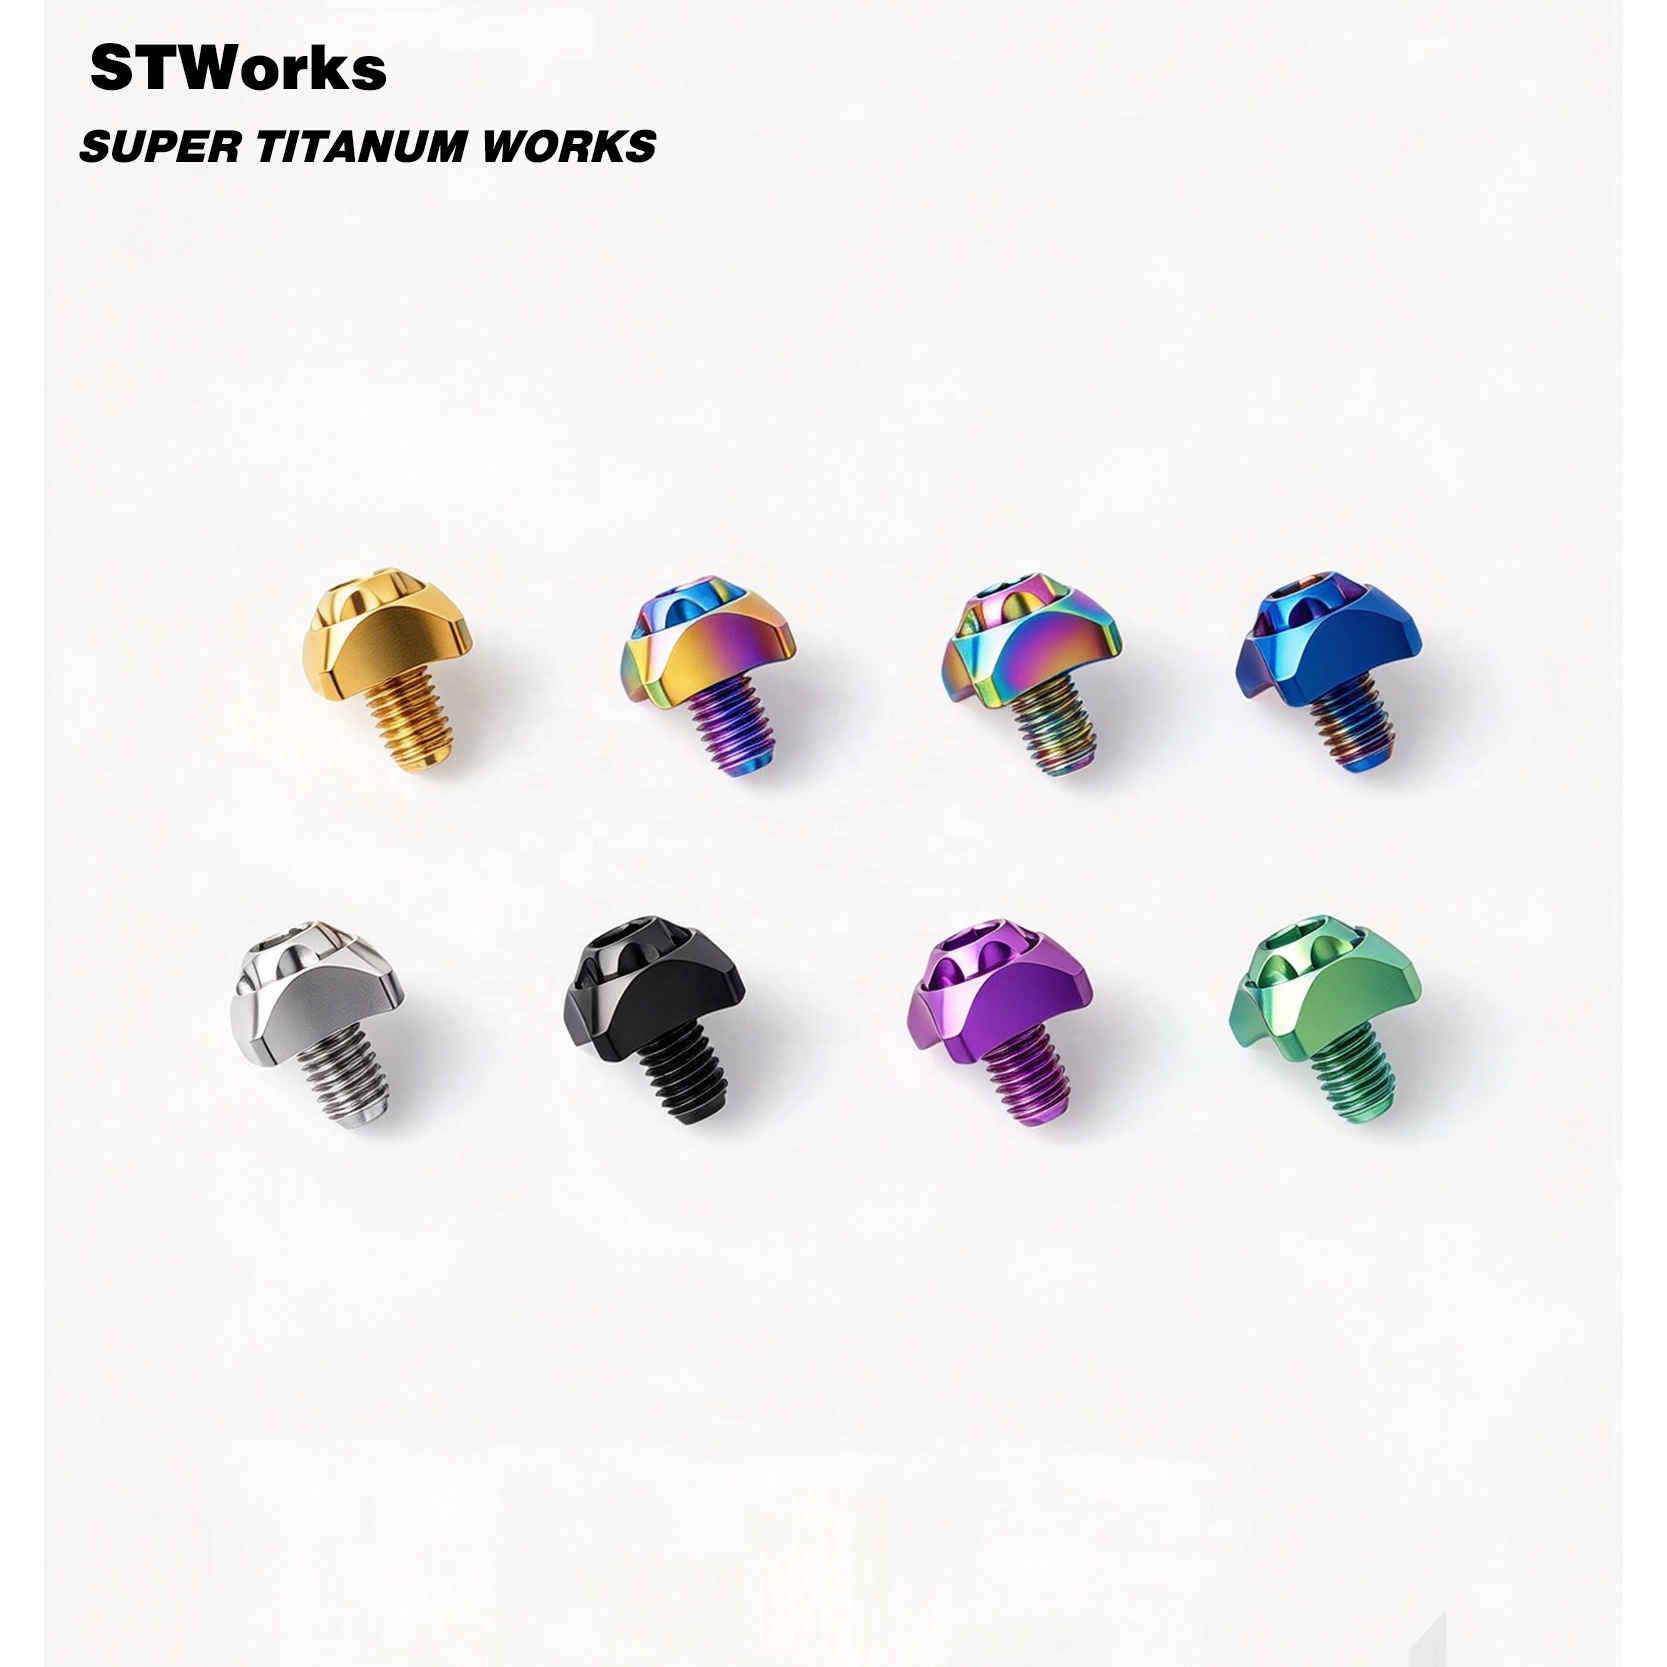
As the primary logistics nerve center of North America—anchored by Louisville Muhammad Ali International Airport (SDF), Worldport, and major rail junctions—the greater Louisville metropolitan region is experiencing an unprecedented transformation. High-specification machining has shifted from traditional ferrous alloys to non-ferrous, corrosion-resistant, and high strength-to-weight metals. In automotive assembly, aerospace maintenance, biomedical devices, and specialized chemical processing, titanium components are replacing heavy steels and stress-corrosion-prone aluminum assemblies.
Operating out of Baoji—China's Titanium Valley—with direct export infrastructure servicing industrial clients across Louisville, Jeffersonville, and the I-65 manufacturing corridor, Velnora Titanium Industry Co., Ltd. bridges tier-one metallurgical smelting with 5-axis CNC micro-machining, thread-rolling, and wire EDM broaching. By providing comprehensive information gain and certified metallurgical traceability, we eliminate the traditional friction of importing critical hardware.
The selection of Ti-6Al-4V (Grade 5, UNS R56400 / ASTM B348) represents the pinnacle of multi-disciplinary engineering. With a density of 4.43 g/cm³, it achieves a 44% reduction in overall mass when juxtaposed with standard AISI 4140 or 316 stainless steels, while delivering a minimum tensile yield strength of 830 MPa (895–1000 MPa ultimate). For dynamic suspension joints, unsprung rotating mass in motorsport applications, and structural fluid linkages, replacing steel with titanium delivers immediate gains in mechanical responsiveness, kinetic efficiency, and seismic fatigue life.
| Mechanical / Physical Property | Grade 5 (Ti-6Al-4V TC4) | Grade 2 (Commercially Pure) | 316L Stainless Steel | 7075-T6 Aluminum |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 | 4.51 | 8.00 | 2.81 |
| Tensile Strength, Ultimate (MPa) | 950 - 1050 | 345 - 480 | 580 | 572 |
| Yield Strength, 0.2% Proof (MPa) | 880 | 275 | 290 | 503 |
| Modulus of Elasticity (GPa) | 114 | 103 | 193 | 71.7 |
| Thermal Conductivity (W/m·K) | 6.7 | 16.4 | 16.3 | 130 |
| Chloride Pitting Resistance | Immune at ambient temps | Immune | Susceptible to crevice pitting | Severe pitting without anodizing |
From local heavy transit hubs to precision motorsports along the Ohio River, our titanium components are engineered to solve specific physical stress, heat, and corrosive environments.
Situated beside the world's largest automated package handling facilities at SDF, air cargo fleet maintenance demands fast-turnaround non-magnetic titanium ground service hardware, bleed screws, and airframe brackets that resist galvanic reaction and hydraulic Skydrol fluid attack.
With massive vehicle assembly operations in Louisville, Tier-1 system builders turn to Gr5 titanium wheel lug nuts, 12-point exhaust studs, and spring retainers for track-edition platforms, eliminating rotational inertia while surviving cyclic thermal excursions up to 400°C.
Kentucky's expanding bio-health and dental implant sectors require commercially pure Grade 2 and Grade 5 ELI (Extra Low Interstitial) micro-screws (M2–M3), dowel pins, and custom housings that meet biocompatible ASTM F136 requirements without toxic nickel leaching.
The industrial landscape across Louisville and southern Indiana is experiencing a distinct pivot towards lightweight electrification and decarbonization. As EV battery plants and automated material handling installations multiply along the I-65 and I-64 corridors, mechanical components are subjected to increasingly complex stresses:
Combining the metallurgical wealth of China’s Titanium Valley with certified quality systems, full visual auditing, and rapid international air transit directly into Kentucky.
We source virgin sponge titanium, vacuum arc remelted (VAR) into structural ingots. Every shipment includes full chemical composition analysis and mechanical tensile testing certificates to ASTM B348, AMS 4928, and ISO 5832 standards.
We eliminate cross-border uncertainty. As standard protocol, clients receive live-action machining video feeds, coordinate measuring machine (CMM) inspection passes, and thread-gauge testing clips prior to containerization or dispatch.
Unlike conventional job shops that cut threads on CNC lathes—severing the alloy’s continuous grain flow—our structural fasteners undergo precision thread rolling. This induces beneficial compressive residual stress, yielding a 30% higher fatigue limit.
Direct technical answers addressing the real mechanical, chemical, and logistical inquiries of North American procurement specialists.
Titanium naturally builds an instantaneous passive oxide skin (TiO2) that can experience cold-welding (galling) when mated under high clamp preloads against other titanium or stainless steel surfaces. We counter this through controlled thread rolling (yielding Ra < 0.4 µm micro-finishes), micro-arc oxidation, hard PVD thin-film coatings, or by recommending high-pressure nickel/molybdenum anti-seize pastes during final assembly torqueing.
Yes, but with strict engineering review. Grade 5 titanium boasts a typical ultimate tensile strength of ~950 MPa, aligning directly with Metric Class 8.8 and approaching Class 10.9 (1040 MPa). Because titanium's Young’s Modulus (E ≈ 114 GPa) is roughly half that of steel (E ≈ 200 GPa), titanium will elongate more under identical tensile preloads, delivering superior clamp compliance in dynamic joint cycling, but requiring calibrated tightening torque schedules.
Because Louisville hosts the SDF global air shipping hub, express air couriers (FedEx International Priority, DHL Express) deliver directly from our packaging line to your facility in Louisville in 3 to 5 business days once production is finalized. For heavy, consolidated ocean shipments, containerized cargo clears through West Coast or East Coast ports with rail forwarding into Louisville intermodal depots in 22 to 28 days.
Yes. Our in-house engineering group operates Mastercam, Siemens NX, and SolidWorks CAD/CAM environments. You can submit raw 3D CAD data along with 2D GD&T drawings in PDF format indicating exact pitch tolerances (6g/6H standard or Class 3A/3B unified inch standards), concentricity callouts, and cosmetic surface finishing specs.
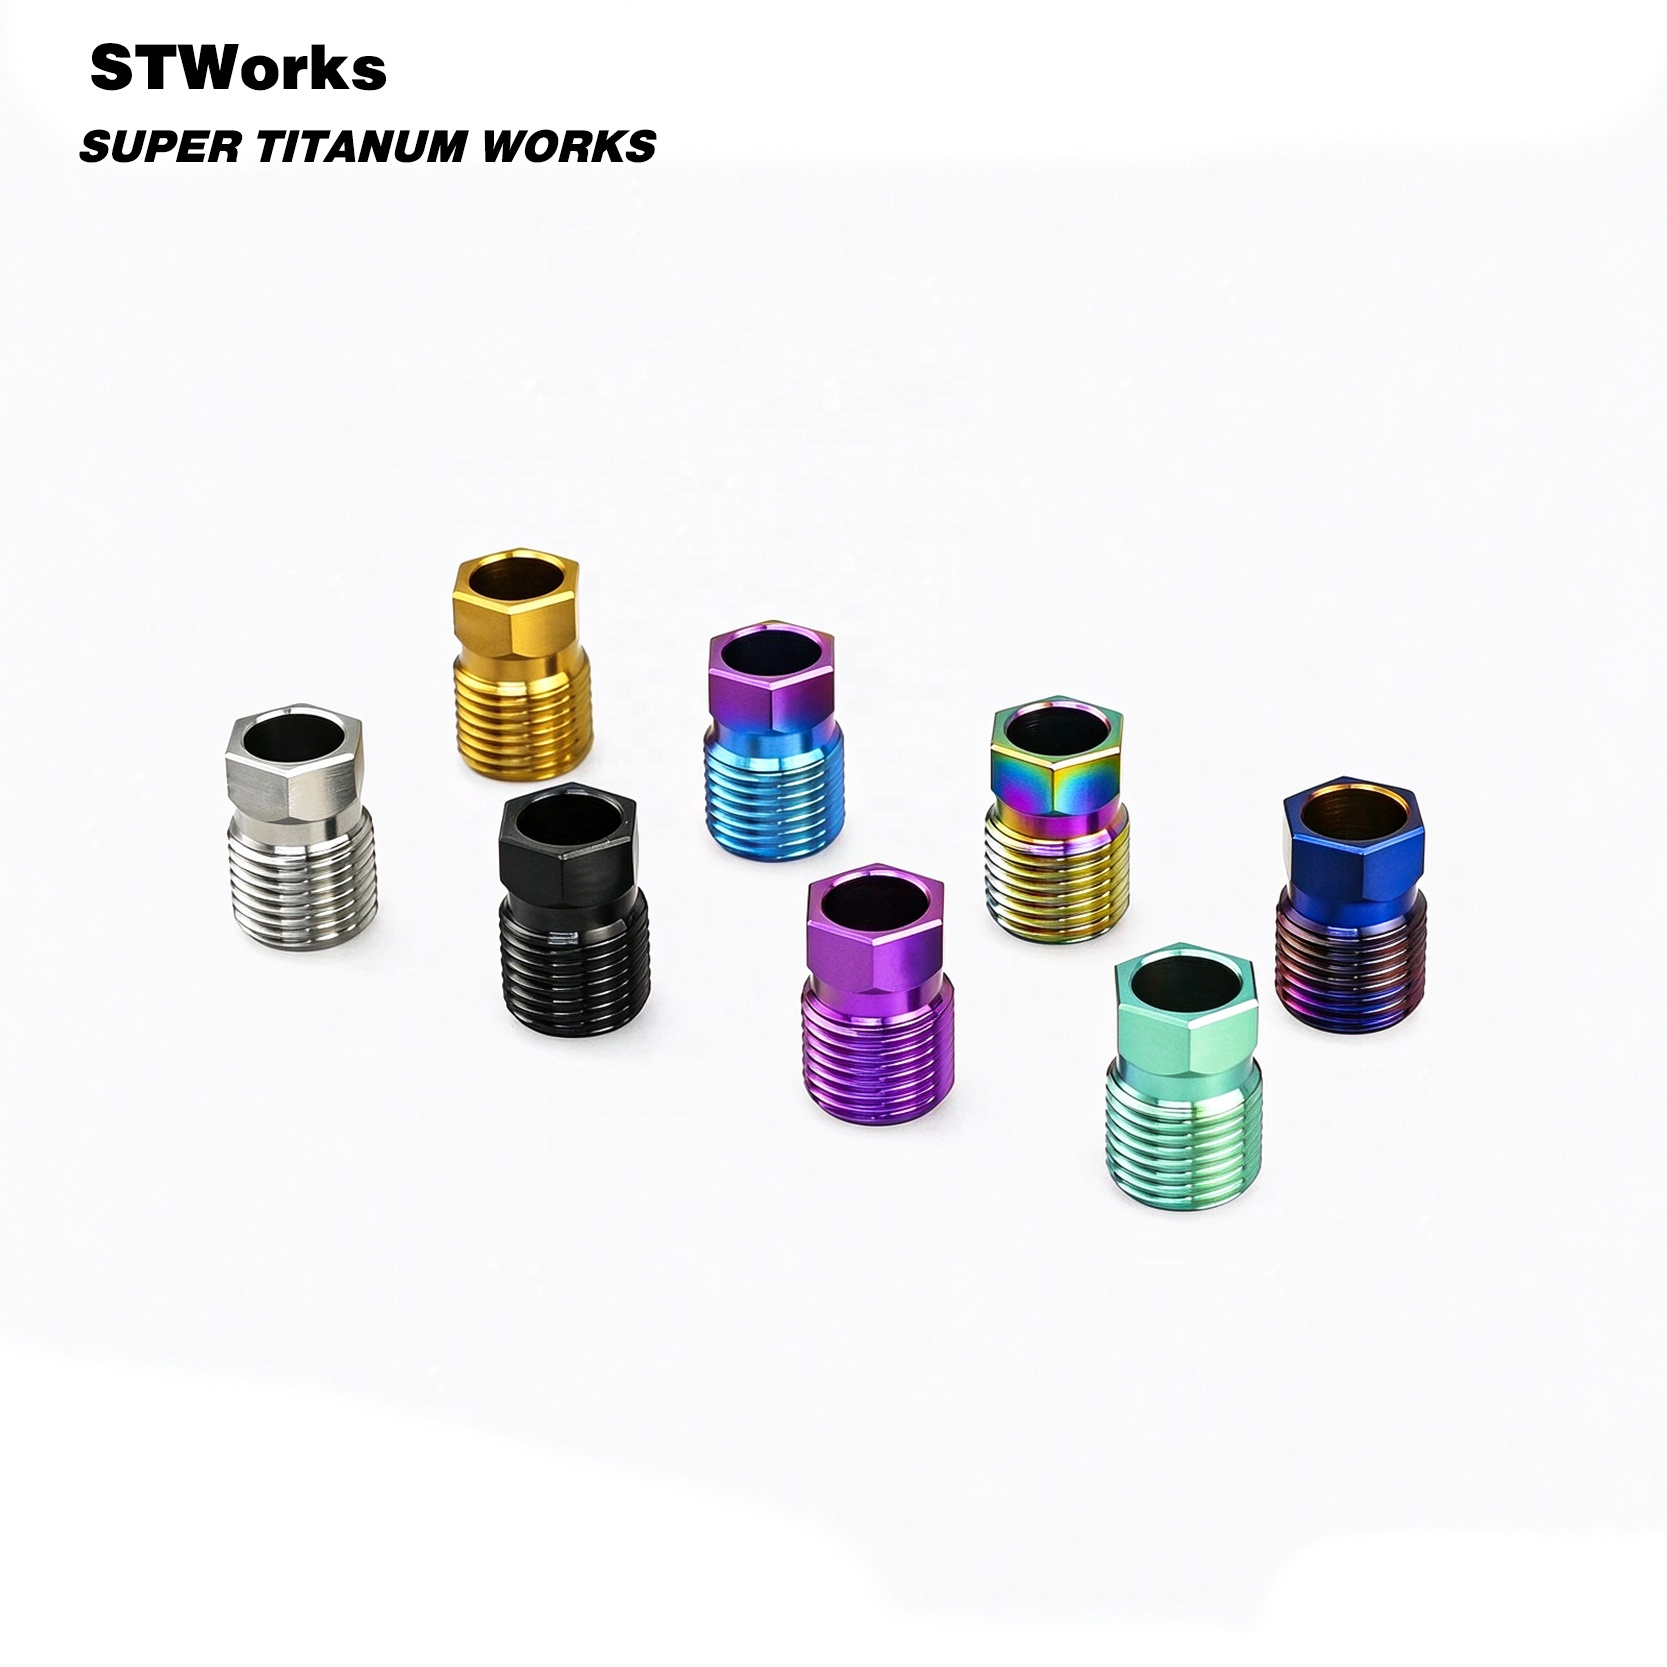
We provide both Type II electrolytic anodizing (voltage-regulated light-interference color spectrum: blue, gold, purple, bronze, and rainbow) and Type III wear-resistant hard anodizing. Because Type II coloration alters only the thickness of the natural transparent oxide film (from tens to hundreds of nanometers), it adds zero measurable dimensional build-up, maintaining exact micro-inch thread tolerances.
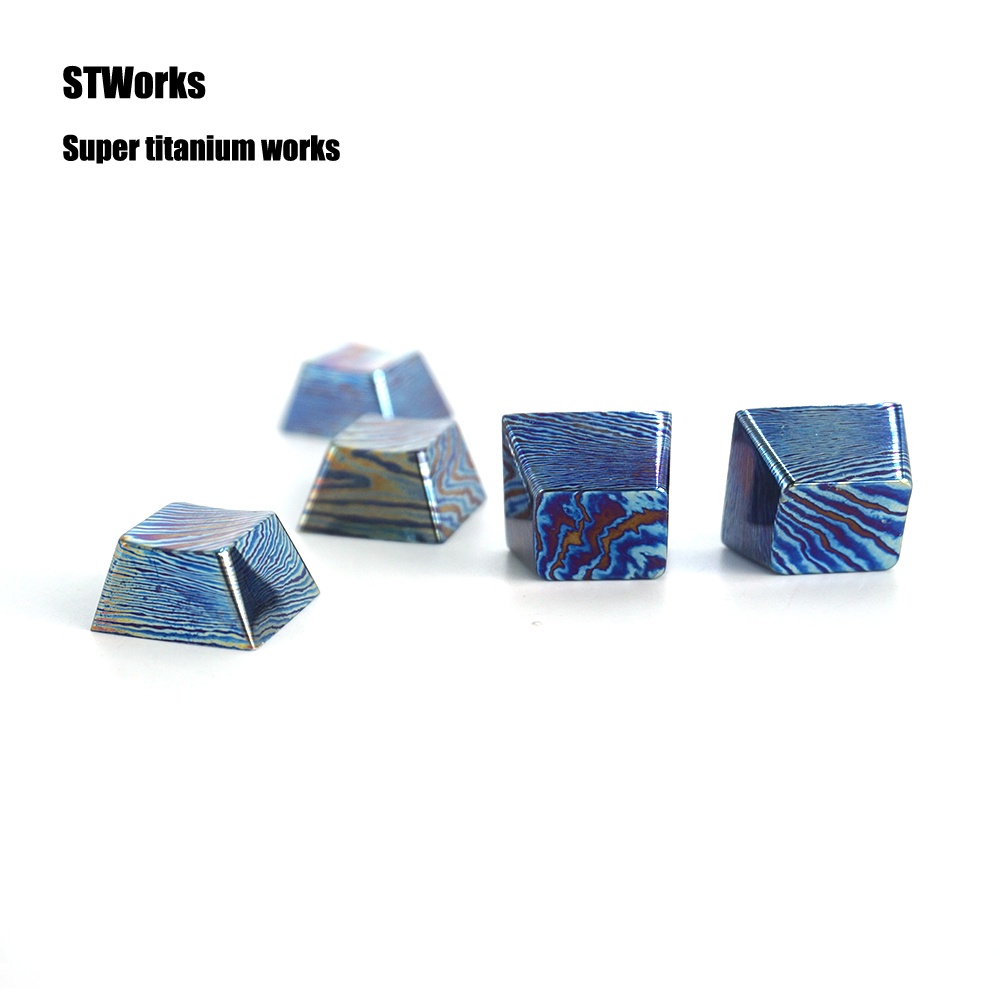
For custom CNC turned and milled components according to your drawing, prototype test batches typically start at 50 to 100 units. For specialized artistic metals like Timascus (Mokuti) keycaps and EDC hardware, we accept short-run orders starting at 1 to 5 pieces. Standard catalog DIN fasteners carry minimum production runs of 200 to 500 units depending on diameter.
Connect with our senior manufacturing engineers today. Submit your CAD models, technical drawings, or bill-of-materials specs. We will deliver a fully costed manufacturing analysis, toolpath review, and quotation within 4 business hours.
Send an Inquiry