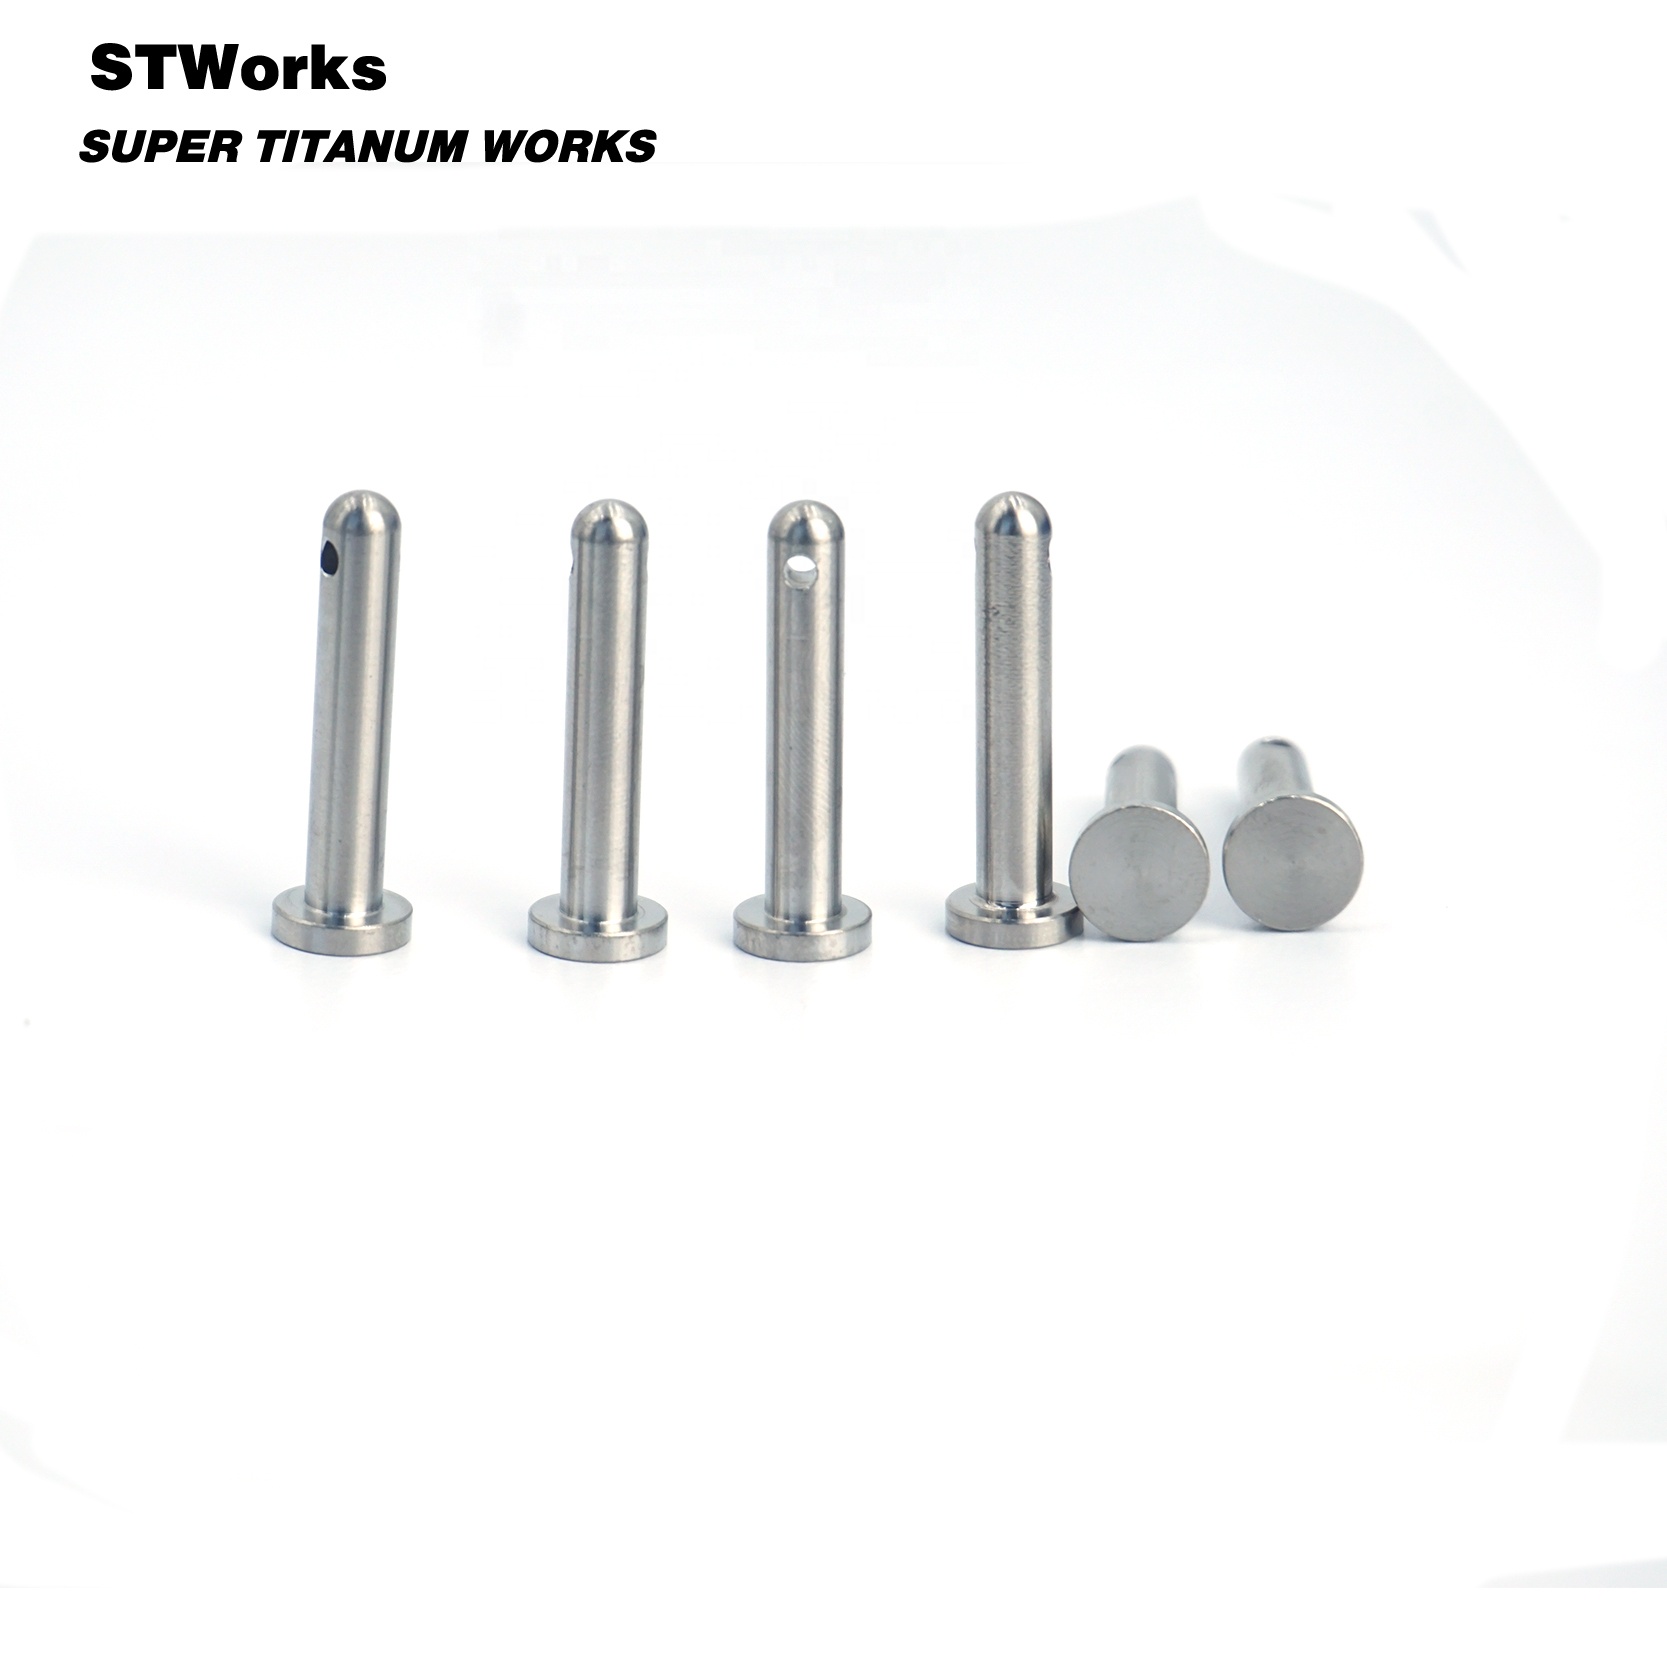
Engineered Assemblies & Hardware
Featured Precision Components for Motorsport & Advanced Mechanical Systems
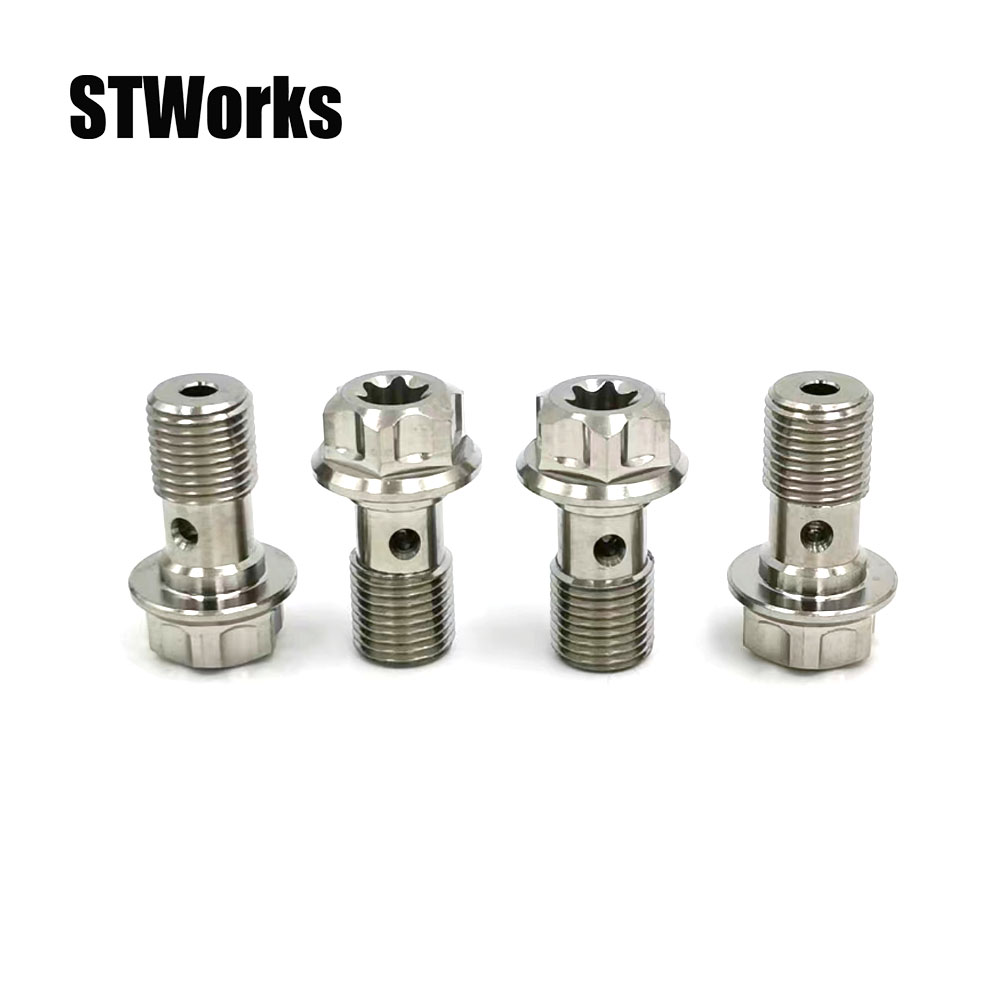
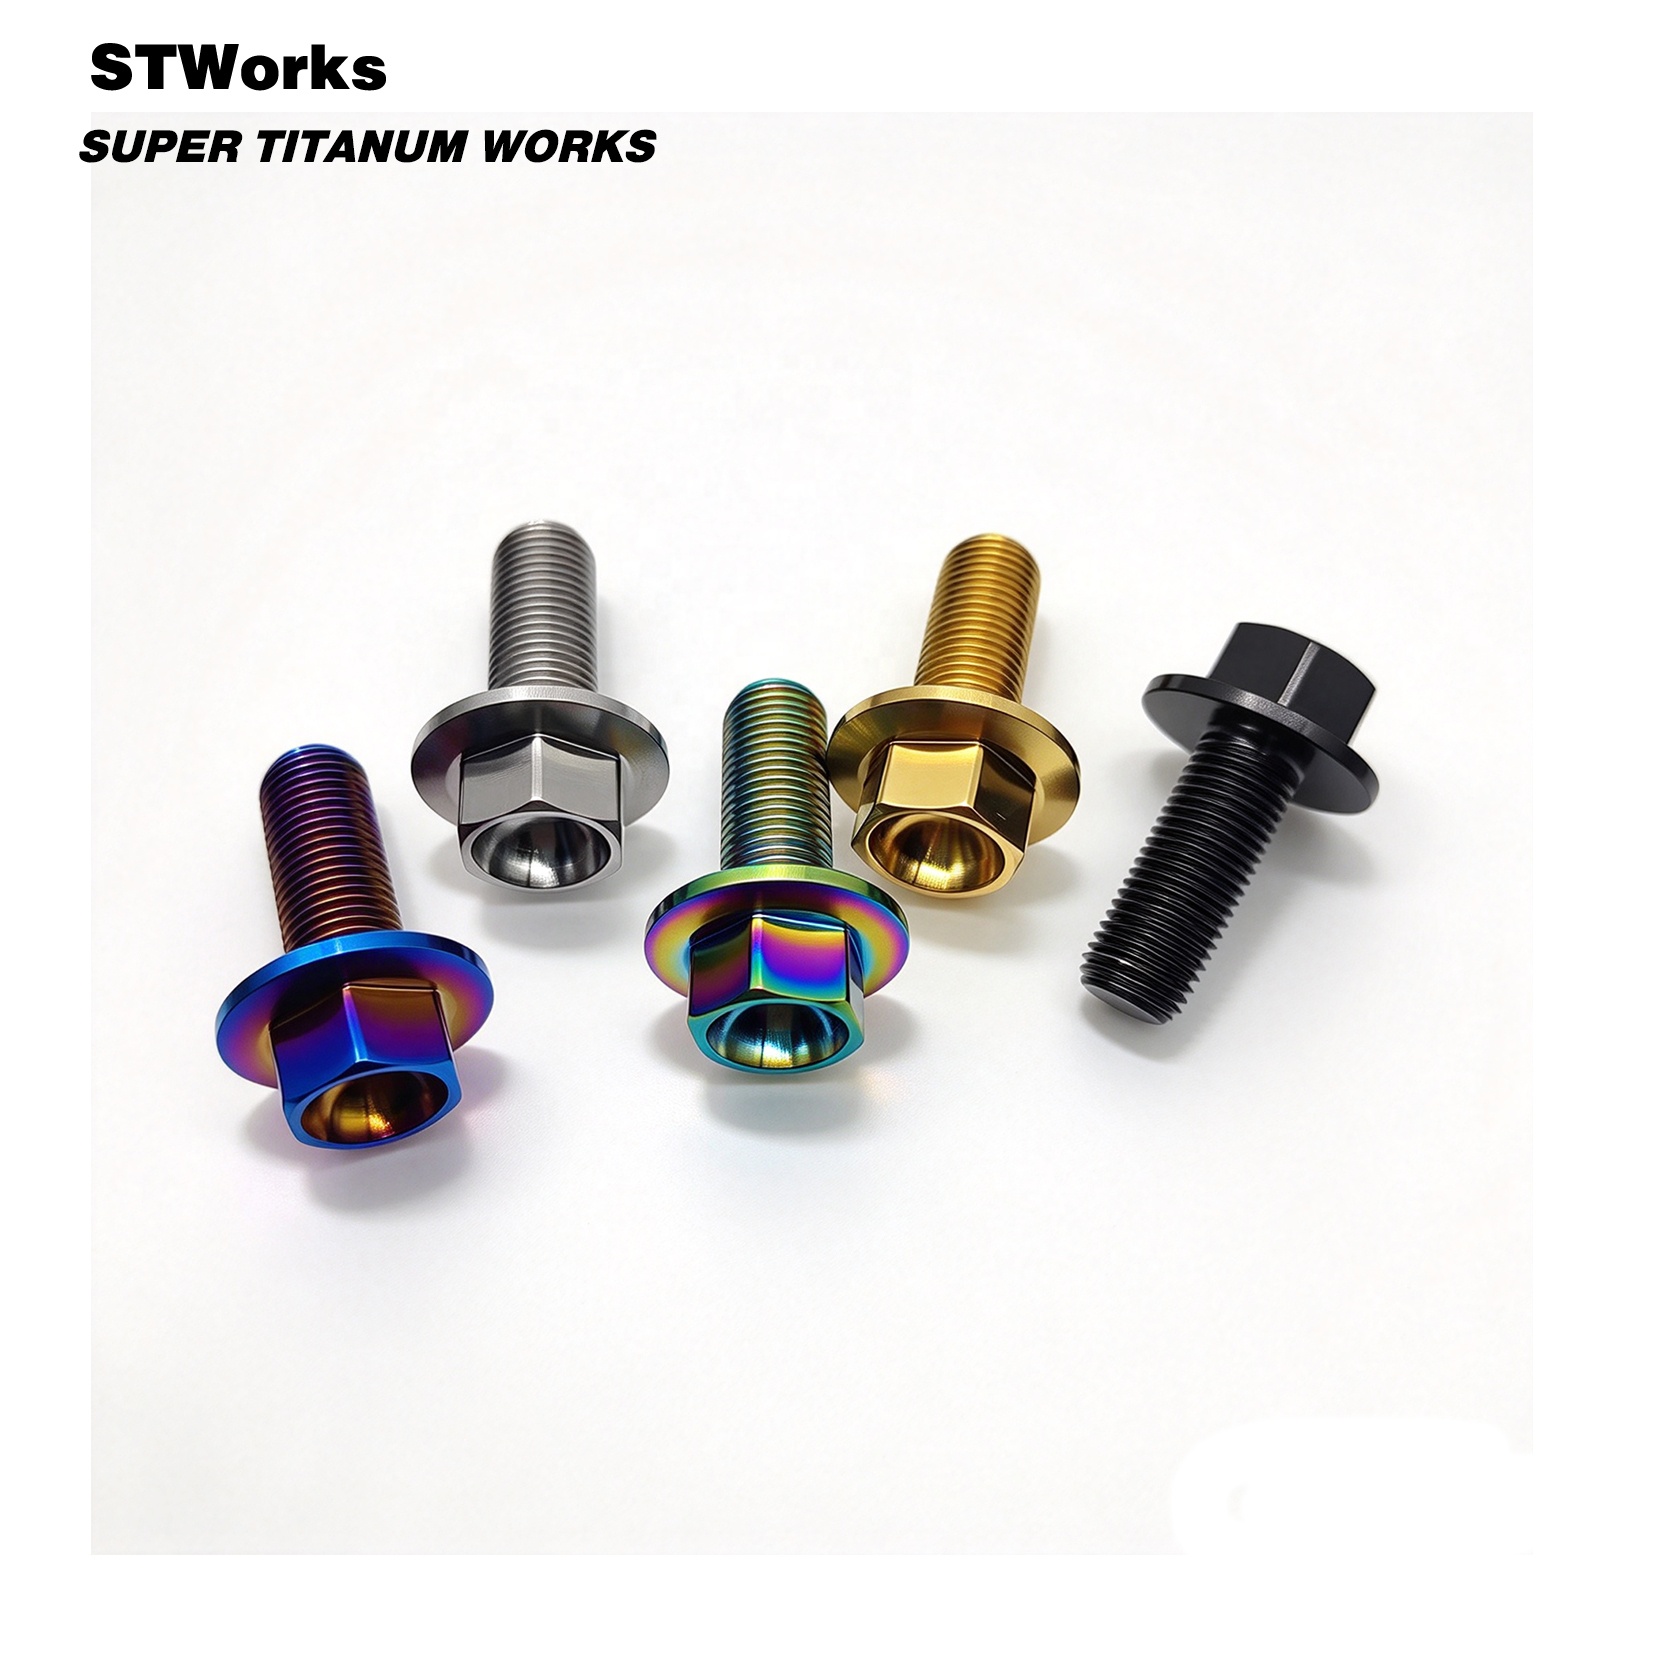
Complementing our titanium connecting rod manufacturing lines, our Baoji precision facility supplies high-tensile fasteners, dowels, and structural hardware trusted by performance builders and precision engineering shops across the Kyoto-Osaka-Kobe industrial corridor.

Technical Whitepaper: Kinematics & Materials Science
Structural Dynamics & Metallurgical Superiority of Titanium Connecting Rods
In high-performance internal combustion engines and dynamic reciprocating compressors, connecting rods represent the most kinetically punished component in the mechanical chain. Operating under severe alternating cycles of tensile inertia and compressive gas pressures, connecting rods dictate maximum piston acceleration, bearing longevity, and engine rotational limits.
Traditional forged steel connecting rods (such as AISI 4340 chromoly or 300M nickel-chromium-molybdenum alloys), while possessing high structural rigidity, impose a heavy reciprocating and rotating mass penalty. As rotational velocities surpass 9,000 RPM—commonplace in professional Japanese road racing championships, time-attack builds, and proprietary dyno programs in the Kansai basin—inertial forces scale with the square of engine velocity (F = m · r · ω²). Doubling the rotational speed quadruples the internal inertial loads exerted on the rod journal, rod bolts, and crankpin bearings.
By engineering connecting rods from high-purity, aerospace-certified Grade 5 Titanium (Ti-6Al-4V / ASTM B348 / AMS 4928) or specialized beta-titanium formulations, Velnora reduces total connecting rod assembly mass by 35% to 42% compared to premium forged steel alternatives. This radical mass reduction unlocks three profound mechanical advantages for Kyoto engine tuners:
Minimized Reciprocating Inertia
Drastically reduces secondary harmonic imbalance, allowing crankpins and big-end bearings to survive extreme RPM thresholds without hydrodynamic oil film collapse or fatigue spalling.
Instantaneous Throttle Transients
Reducing rotating crankshaft assembly inertia yields lightning-fast throttle response and shorter spool times in forced-induction and naturally aspirated multi-cylinder layouts alike.
Enhanced Rod Bearing Duty Life
Lower mass equates to diminished peak tensile stresses on custom rod bolts at top dead center (TDC) exhaust stroke, mitigating big-end ovalization and journal pinching.
However, titanium behaves distinctly from quenched and tempered steels. With an elastic modulus (Young's Modulus) of approximately 114 GPa—roughly half that of structural steel (210 GPa)—a titanium connecting rod cannot simply replicate a steel rod's geometry. Directly copying steel cross-sections causes structural deflection, wrist-pin binding, and improper big-end bearing clearance under heavy cylinder boost pressures. Our engineering team utilizes advanced finite element analysis (FEA) to design widened H-beam or parabolic I-beam architectures. By increasing the section modulus along the major bending axis and introducing reinforcing buttresses around the small-end wrist pin and big-end journal, Velnora delivers maximum column stiffness with zero weight compromises.
Regional Ecosystem & Strategic Fit
Localized Application Scenarios Across Kyoto and the Kansai Industrial Belt
Kyoto occupies a world-renowned position where ancient craft precision ("Monozukuri") seamlessly converges with frontier high-tech manufacturing, university laboratories, and demanding motorsport applications.
Circuit & Hillclimb Racing Teams
Bordering the Suzuka circuit racing corridor and Kansai regional circuits (Central Circuit, Okayama International), Kyoto houses specialized tuning masters developing high-revving platforms (Honda K20A/B18C, Nissan RB26/VR38, Yamaha superbike engines). Velnora’s bespoke titanium conrods provide the tensile reserve demanded by 11,000+ RPM road racing specifications.
High-Altitude UAV & Range Extenders
Kyoto Research Park (KRP) and Keihanna Science City are pioneering autonomous industrial drones and hybrid unmanned aerial platforms. Our custom titanium connecting rods empower lightweight boxer and single-cylinder range-extender engines to operate with maximum power-to-weight density in sub-zero thin-air operations.
Heritage Motorcycle Restoration & Restomod
From classic Kawasaki Z1 and Honda CB Four restomods to bespoke single-cylinder track racers built in Kyoto workshops, classic enthusiasts demand zero-vibration reciprocating dynamics. Custom titanium connecting rods engineered to historical dimensions eliminate heavy internal vibrations while safeguarding priceless vintage engine casings.
Kyoto Market Evolution
Key Technological Trends Influencing Titanium Procurement in Kyoto
The Japanese precision machinery sector is evolving rapidly under dual imperatives: ultra-precision micro-tolerances and environmental life-cycle efficiency.
1. Shift Toward Synthetic Fuel & Hydrogen Internal Combustion: Japanese automotive giants and Kyoto-area research affiliates are investing heavily in carbon-neutral liquid fuels and direct-injection hydrogen combustion engines. Hydrogen combusts with significantly higher flame velocities and combustion pressure spikes than standard gasoline. Connecting rods must endure abrupt cylinder pressure rise rates (dP/dθ) without suffering hydrogen embrittlement. Velnora’s high-purity Ti-6Al-4V rods, treated with advanced physical vapor deposition (PVD) barrier coats, provide exceptional resistance to hydrogen permeation while absorbing violent combustion shocks.
2. Adoption of Diamond-Like Carbon (DLC) & Solid Lubrication Interfaces: Because titanium exhibits an affinity for self-welding and adhesive galling when loaded directly against steel or bronze under boundary lubrication, Kyoto engine specialists universally mandate specialized surface treatments. Our manufacturing process integrates precision physical vapor deposition (PVD) yielding thin-film Diamond-Like Carbon (DLC) or titanium nitride (TiN) on thrust faces and big-end side reliefs, eliminating galling risks against crankshaft cheeks.
3. Demand for Fully Traceable Low-Batch Prototypes: Kyoto's craft-driven engineering ecosystem rarely operates on massive standardized runs. Performance engineers demand prototype flexibility—runs of 4 to 20 units—with CMM verification reports, material melt certificates (MTC EN 10204 3.1), and digital dimensional verification. Velnora’s direct-from-factory model fulfills this demand with rapid 5-axis CNC turning and wire EDM tooling without requiring punitive multi-thousand-unit tooling commitments.
Empirical Data Visualization
Comparative Metrology: Ti-6Al-4V vs. High-Performance Steels & Aluminum
Direct metallurgical comparison highlighting why precision-engineered Grade 5 Titanium is the premier selection for reciprocating kinetic applications.
| Physical & Mechanical Property | Velnora Gr5 Titanium (Ti-6Al-4V) | Forged 4340 Chromoly Steel | 300M Ultra-High Steel | 7075-T6 Billet Aluminum |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 (Optimal Balance) | 7.85 (Heavy Baseline) | 7.84 (Heavy Baseline) | 2.81 (Extremely Light) |
| Tensile Yield Strength (MPa) | 880 – 950 | 860 – 980 | 1,520 – 1,650 | 505 |
| Ultimate Tensile Strength (MPa) | 950 – 1,050 | 1,000 – 1,120 | 1,900 – 2,050 | 570 |
| Modulus of Elasticity (GPa) | 114 (Requires FEA Section) | 205 (Rigid) | 210 (Very Rigid) | 72 (Prone to Flex) |
| High-Cycle Fatigue Limit (10⁷ cycles) | 510 MPa (Shot-Peened) | 490 MPa | 680 MPa | 160 MPa (Finite Lifespan) |
| Corrosion & Acid Resistance | Immune to Nitromethane/Alcohols | Susceptible to Oxidation | Susceptible to Oxidation | Attacked by Methanol |
| Fatigue Lifespan in Engine (Hours) | 150 – 300+ Continuous High-RPM | 300+ (Penalty in Mass) | 300+ (Penalty in Mass) | 15 – 30 (Top Fuel Only) |
Manufacturing Provenance & Authority
Baoji Engineering Strength: Your Direct Factory Link in China's Titanium Valley
Headquartered in the heart of Baoji’s Precision Manufacturing Park since 2013, Velnora combines China's primary raw titanium supply with boutique European and Japanese aerospace-grade machining equipment.
2013
Established in Baoji Valley
1,000+
Global B2B Enterprise Clients
±0.002mm
CNC Big-End Bore Tolerance
≤4 Hrs
Technical Drawing Review
Uncompromising Raw Material Integrity: Every connecting rod blank originated by Velnora is forged from vacuum double-melted or triple-melted (VAR) titanium sponge. We do not recycle scrap in our critical powertrain products. Raw bar stocks are fully compliant with AMS 4928 and ASTM B348, verified by optical emission spectrometry and ultrasonic immersion inspection to ensure freedom from high-density inclusions (HDIs) and interstitial oxygen clusters.
High-Precision Wire EDM & Split-Cap Machining: Connecting rod caps are segmented using ultra-slow-feed precision Wire Electrical Discharge Machining (Wire EDM) to preserve grain integrity, or fractured using proprietary serrated dowel alignments. Big-end roundness and taper tolerances are held within ±0.002 mm (±2 μm) on Japanese Makino and Brother CNC machining centers, guaranteeing oil clearance uniformity when paired with premium Japanese race bearings.
Surface Compressive Conditioning: Following CNC milling, every rod undergoes controlled multi-stage ceramic or steel shot-peening under precise Almen intensity protocols. This introduces uniform compressive residual stress across all external fillets and transitions, completely neutralising micro-crack initiation sites and elevating fatigue thresholds by over 25%.
Procurement Due Diligence
Kyoto Buyer Technical FAQ: Sourcing Custom Titanium Connecting Rods
Engineers and purchasing managers frequently raise these technical and logistical queries when sourcing bespoke kinetic components for Japanese operations.
1. How do you address the galling tendency of titanium on rod thrust faces and wrist-pin bores?
Titanium exhibits poor tribological behavior against uncoated metals under severe boundary conditions. For the small-end wrist pin bore, we precision-press and hone an Ampco 45 or beryllium-copper (CuBe) bushing with dedicated EDM oiling channels. For the big-end thrust faces that ride against the crankshaft cheeks, we apply a high-adhesion PVD Diamond-Like Carbon (DLC) or titanium carbo-nitride (TiCN) coating. Additionally, we provide custom titanium thrust washers or specify strict crankshaft side clearances to ensure continuous hydrodynamic oil film cushion.
2. Can you produce bespoke custom rods from Japanese JIS standard drawings or customer CAD files?
Yes. Our engineering division natively processes 3D CAD files in STEP, IGES, Parasolid (.x_t), and native SolidWorks formats, as well as 2D PDF engineering blueprints conforming to JIS B 0001 drafting standards. We review all tolerances, bearing journal crush heights, and fillet radii, returning a comprehensive DFM (Design for Manufacturability) analysis within 4 hours during standard business days.
3. What rod bolt fasteners do you utilize, and what is the proper torque method?
We supply bespoke Grade 5 (Ti-6Al-4V) rolled-thread bolts for extreme lightweight requirements, or integrate aerospace ARP Custom Age 625+ / L19 fasteners depending on your peak cylinder pressure and rev spectrum. We strictly advise against relying purely on click-type torque wrenches due to thread friction variance; we provide precise bolt-stretch measurements (using a stretch gauge) and recommend specialized molybdenum anti-seize lubricants.
4. What is the typical Minimum Order Quantity (MOQ) for custom racing prototypes?
For fully custom billet-machined titanium connecting rods, our prototype MOQ starts at just 1 engine set (e.g., 2 rods for a V-twin, 4 rods for an inline-four, or 6 rods for an inline-six). For high-volume aftermarket distributors and OEM applications, we offer serialized volume pricing starting at 50 to 500 units per batch, backed by dedicated production scheduling.
5. How do you manage logistics, Japanese customs clearance, and delivery to Kyoto?
Shipments to Kyoto Prefecture are dispatched directly from our Baoji logistics warehouse via international express air freight (DHL, FedEx, UPS) or freight forwarders direct to Kansai International Airport (KIX) or Osaka Port. Transit time typically ranges between 3 to 5 business days. We provide commercial invoices, packing lists with accurate HS codes (HS 8409.91 / 8409.99), and Certificate of Origin documents to ensure expedited Japanese customs clearance.
6. What material certifications and non-destructive testing (NDT) are included?
Every production batch is accompanied by an EN 10204 3.1 Inspection Certificate detailing chemical composition (ICP spectrometry) and physical tensile values. Additionally, all connecting rods undergo fluorescent dye penetrant inspection (PT) to verify freedom from surface cracks, and 100% Coordinate Measuring Machine (CMM) reports detailing small-end and big-end center-to-center distances, bore diameters, and parallelism.
7. How does Velnora verify quality before goods depart the factory?
In accordance with our digital transparency protocol, we send high-resolution macro photography and video recordings of your components on the CMM inspection table and dynamic balancing scales prior to export packing. Clients inspect and sign off on their actual serial-numbered components before the freight leaves our dock.
Partner with Baoji’s Premier Titanium Engineering Factory
Equip your next high-performance engine build, prototype laboratory project, or motorsport campaign with certified aerospace-grade titanium connecting rods. Send us your CAD models or OEM replacement specifications today.