Precision Titanium Fasteners & CNC Turned Parts
Precision-machined from certified Grade 5 (Ti-6Al-4V TC4) and specialty aerospace titanium. Calibrated to DIN, ISO, and race-spec performance standards.
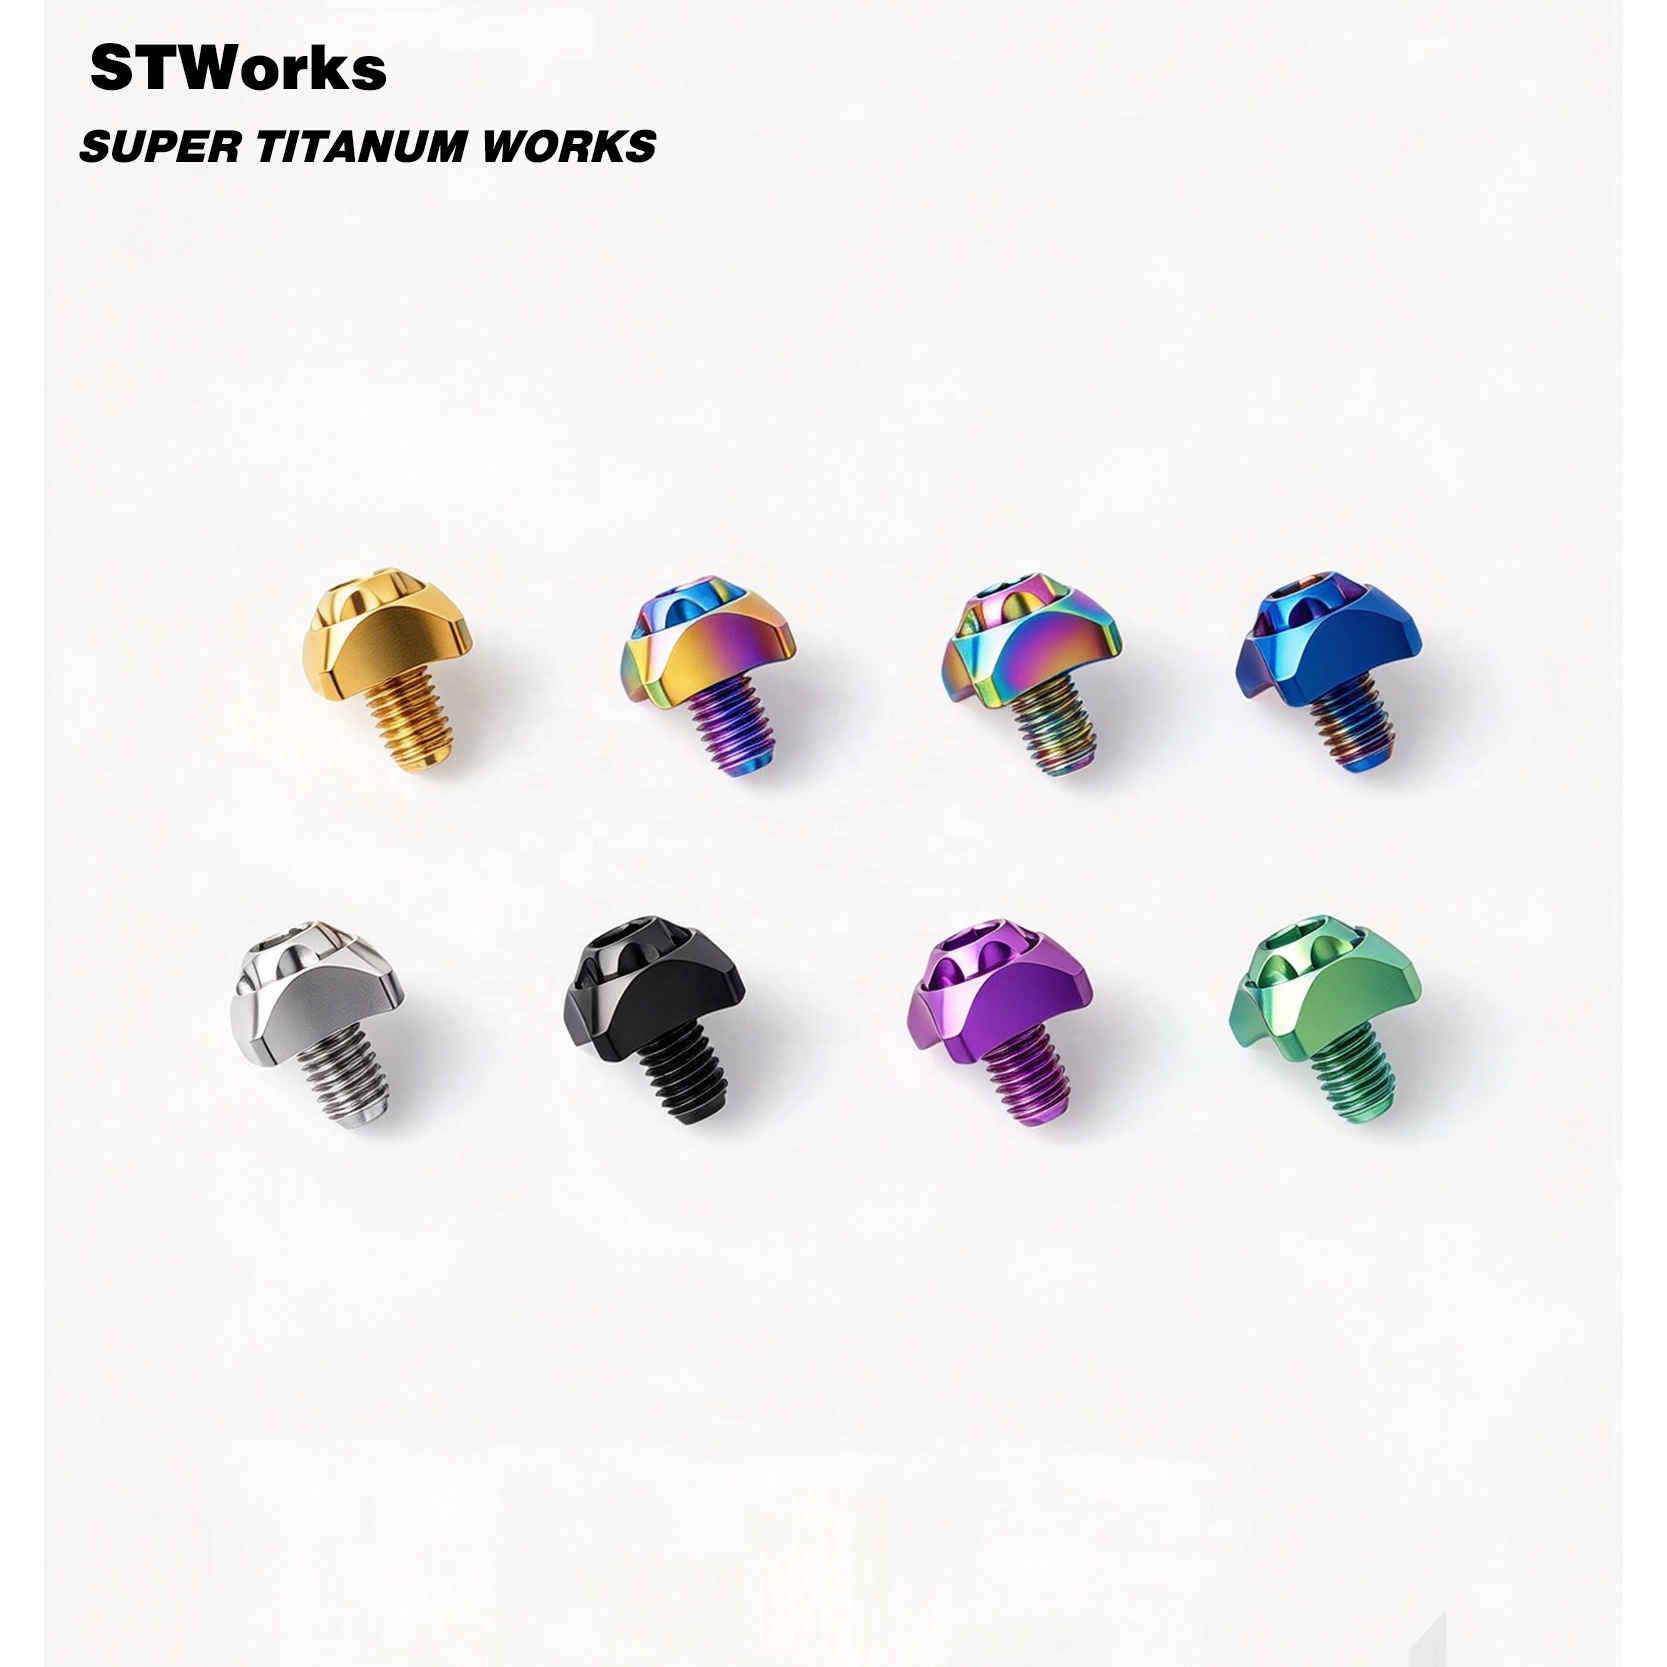
Titanium Screw & Shim Set for Shimano SRAM Derailleur
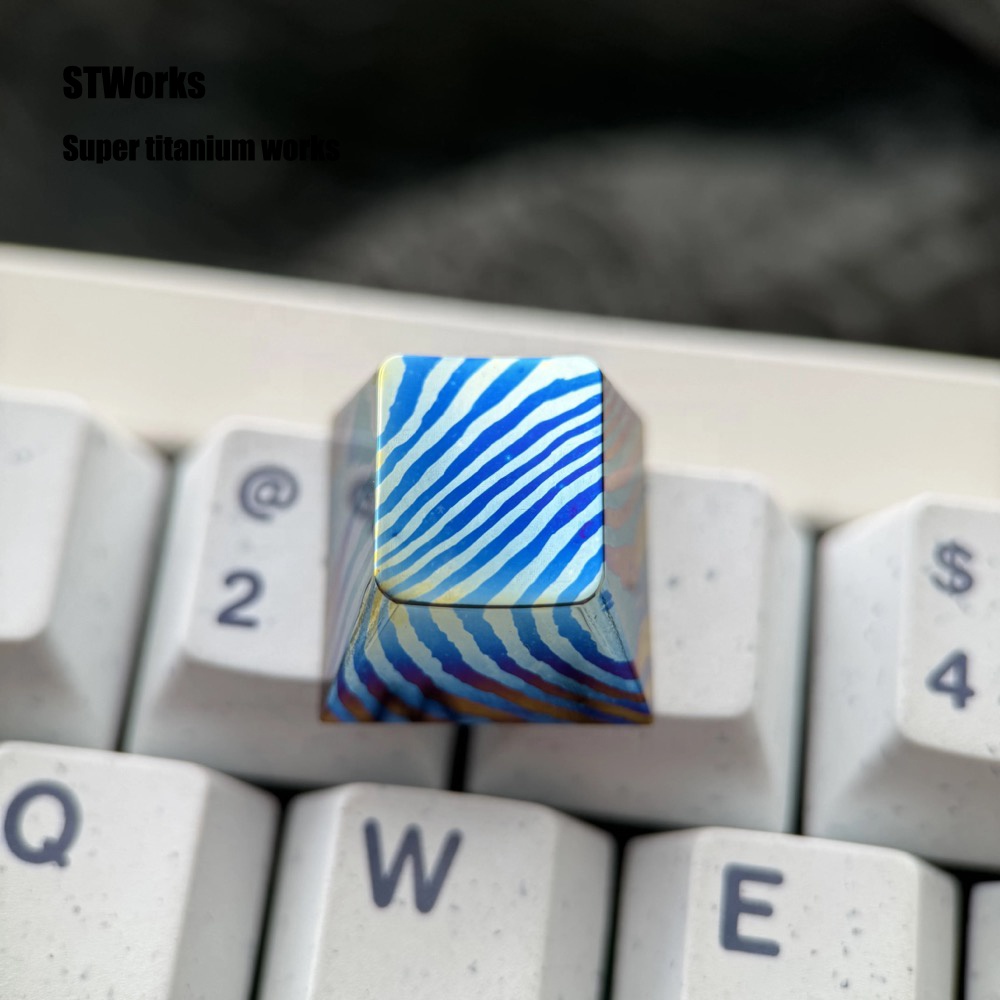
Timascus Alloy Mokuti CNC Parts 1U ESC Keycaps
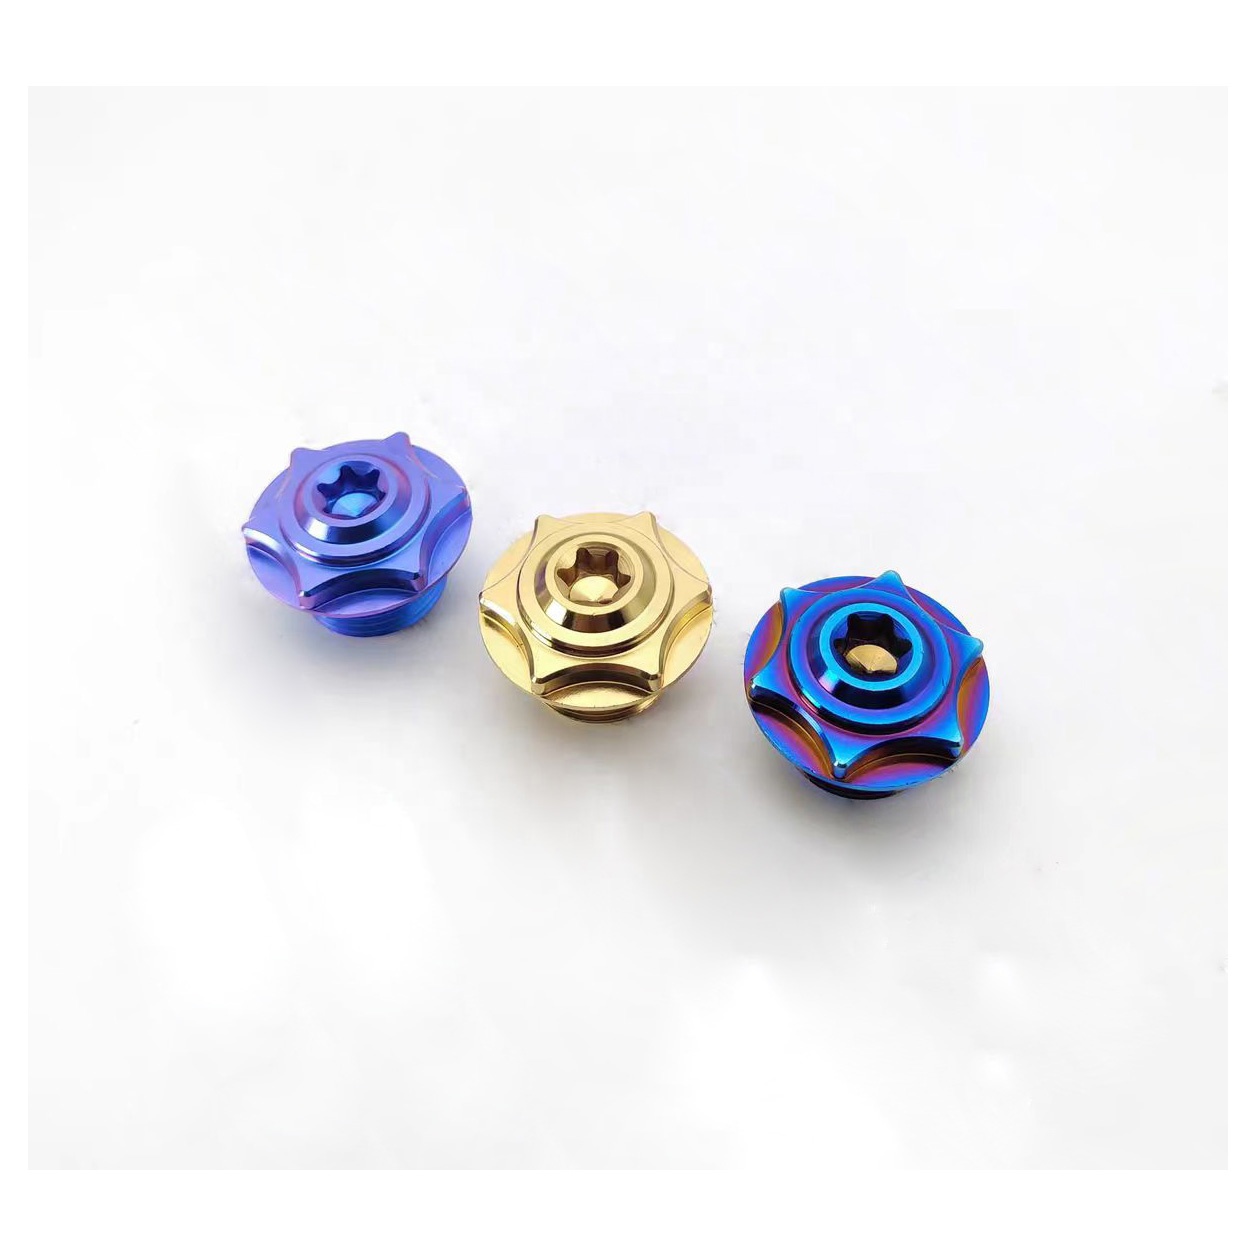
Titanium Screw Motorcycle Oil Filler Cap M20xP1.25/1.5
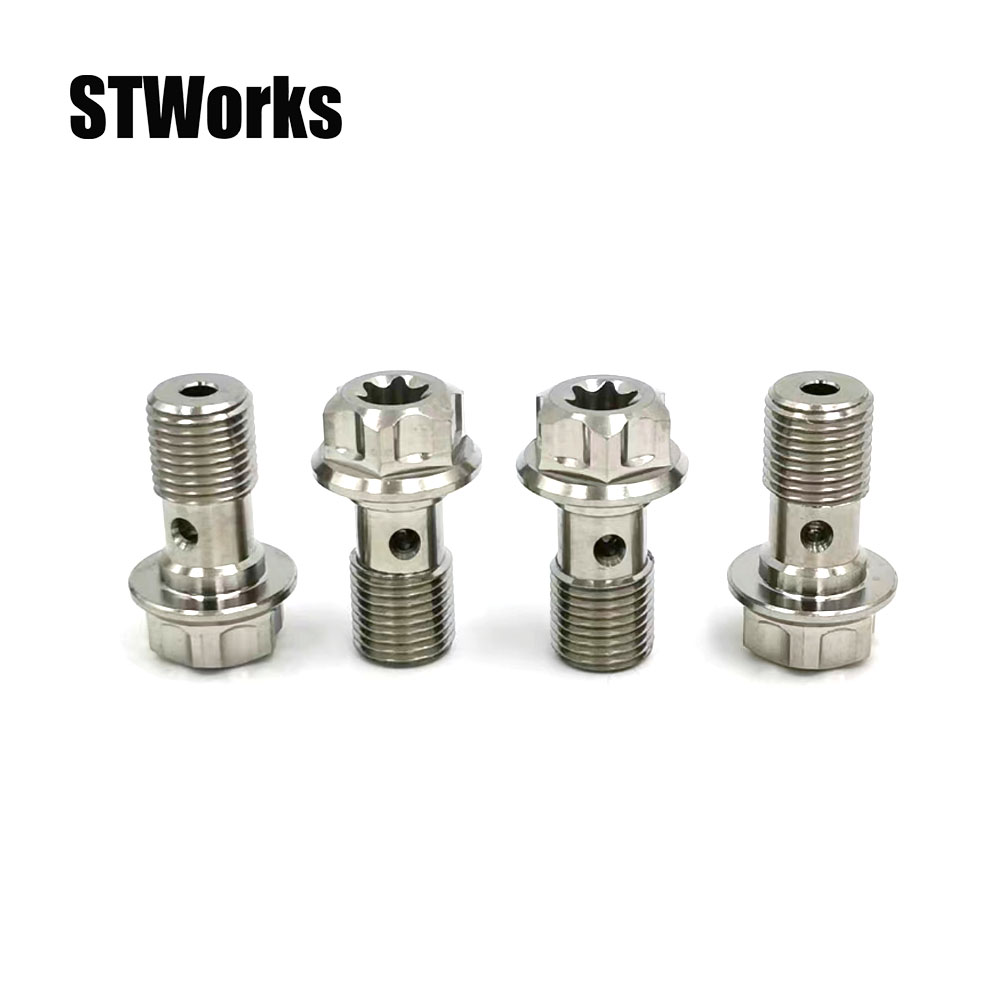
Gr5 Titanium Hex Banjo Bolts M10x1.0/1.25 PVD Coated
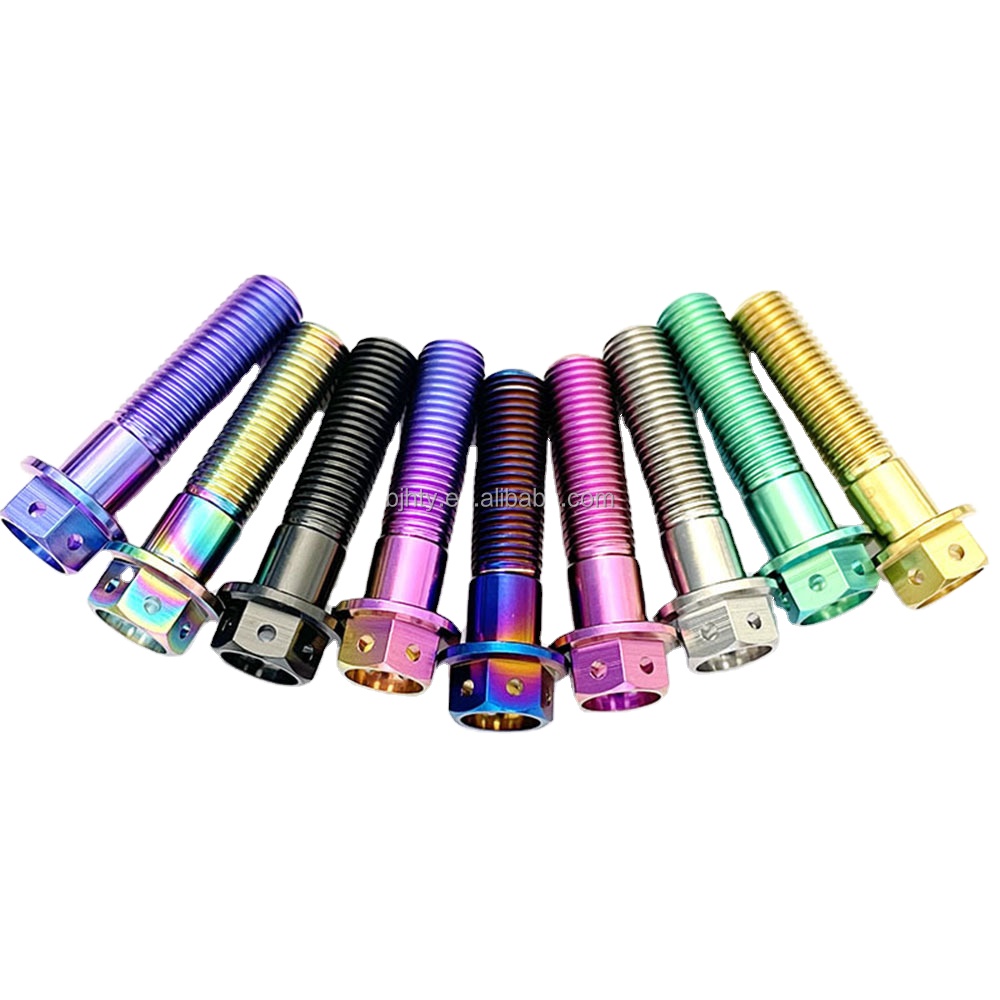
Titanium Alloy Double Drive Head Flanged Hex Bolts M8/M10
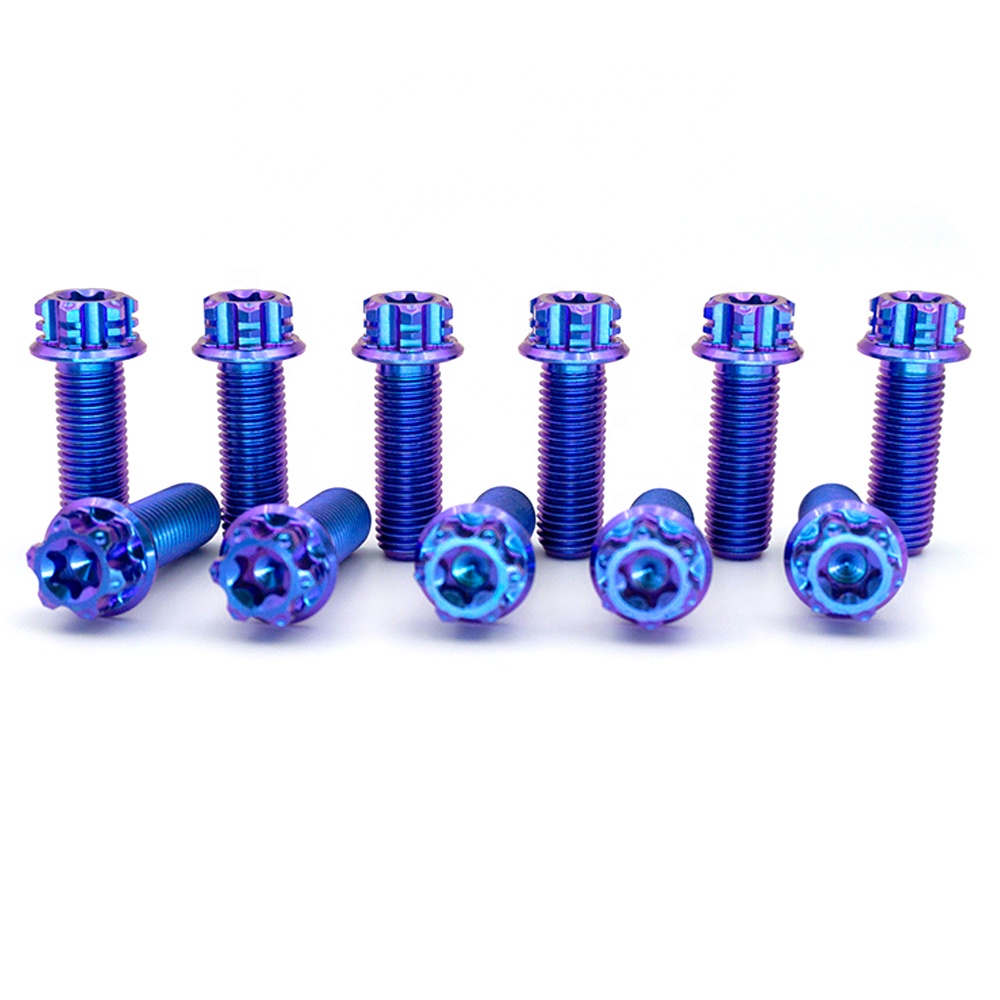
Gr5 Hexagonal Flange Head Machine Screws & Fasteners

Titanium Screws M2/M2.5 Cylinder Head Bolt DIN 912 Torx
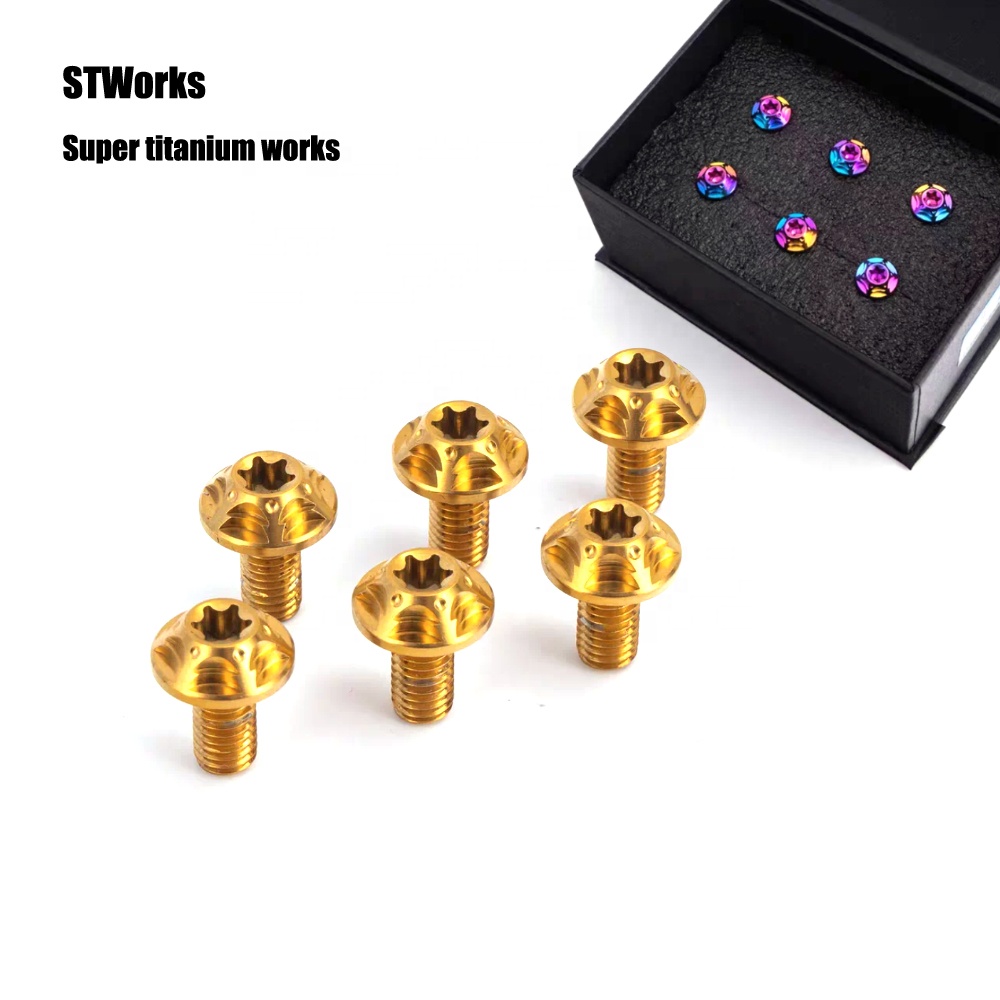
Rainbow Torx Pan Screws Gr5 Titanium Brake Rotor M5x10
Engineering Whitepaper: Titanium CNC Precision Manufacturing for Linz Industry
The industrial epicenter of Linz, situated along the Danube and anchoring Upper Austria's renowned manufacturing spine, represents one of Europe’s most technologically exacting fabrication and mechatronics corridors. Known internationally for steel engineering, advanced metallurgy, automotive drivetrain production, and specialty chemical plant engineering, procurement managers across the Linz-Wels-Steyr triangle face intensifying demands for uncompromising weight reduction without mechanical yield compromise. As conventional high-strength austenitic steels reach their physical limits in dynamic rotational mass and aggressive electrochemical environments, titanium CNC machined components have transitioned from an aerospace novelty to an indispensable material baseline.
Velnora Titanium Industry Co., Ltd., based directly within the global epicenter of raw titanium processing—Baoji (China’s Titanium Valley)—bridges the gap between bulk metallurgical extraction and micro-precision machining. For Linz-based equipment manufacturers and Tier-1 engineering vendors, titanium manufacturing is fraught with technical hurdles: severe chemical reactivity at cutting temperatures above 500°C, poor thermal conductivity (approx. 6.7 W/m·K compared to steel's 50 W/m·K), localized tool welding, and high elastic springback during precision milling. Overcoming these mechanical traits requires dedicated multi-axis Swiss-type turning machines, optimized high-pressure through-spindle cooling channels, and deep metallurgical domain expertise.
Ti-6Al-4V Grade 5 vs. European Industrial Steels: The Mechanical Reality
When specifying titanium components for mechanical assemblies in Upper Austria, clarity regarding property classes is paramount. Grade 5 Titanium (Ti-6Al-4V / 3.7165 / TC4) provides a typical tensile strength exceeding 895 to 1,000 MPa with a density of 4.43 g/cm³, representing an immediate 44% mass reduction compared to property class 8.8 structural carbon and 1.4404 (316L) stainless steels. However, procurement teams must understand that while Grade 5 matches class 8.8 and high-grade 300-series stainless steels in shear and tension, it cannot replace 10.9 or 12.9 hardened steel bolts in extreme load-bearing cross-sections without geometric reassessment or thread up-sizing.
Furthermore, titanium's lower modulus of elasticity (approximately 114 GPa versus steel's 210 GPa) offers distinct kinetic shock-absorbing characteristics, dampening transient harmonic vibrations in high-frequency cycling equipment, such as automotive racing drivetrains and dynamic robotics end-effectors commonly deployed across Linz automation labs.
Eliminating Thread Galling in High-Stakes Assemblies
One of the primary failure modes Linz assembly engineers encounter with titanium fasteners is thread galling (fretting corrosion/cold welding), occurring when microscopic surface asperities momentarily fuse under compressive torque. Velnora mitigates this completely through a dual-protocol approach: First, our external and internal threads are strictly cold-rolled rather than single-point cut wherever feasible, producing continuous grain flow along the root radius, which boosts cyclic fatigue endurance by 30% and reduces surface roughness down to Ra 0.4. Second, we integrate advanced surface treatments, including PVD (Physical Vapor Deposition) Titanium Nitride (TiN) / Diamond-Like Carbon (DLC) coatings and custom electrochemical micro-arc oxidation, creating an ultra-hard barrier that prevents atomic diffusion between mating surfaces even under repetitive dry-torque fastening.
Titanium Applications Across the Linz Industrial Cluster
Precision components designed for Upper Austria's mechatronics, automotive engineering, heavy processing plants, and specialty consumer sectors.
High-End Mobility & E-Bike Drivetrains
Upper Austria is home to prominent tier-1 automotive innovators, racing components specialists, and performance two-wheeler engineering. Our hollow-drilled M5/M6 titanium derailleur bolts, banjo bolts, and brake caliper mounts systematically eliminate un-sprung mass, offering immune performance against aggressive winter road de-icing salts used on Alpine highways.
Heavy Industrial Automation & Robotics
In automated pick-and-place lines and robotic weld-heads deployed in local manufacturing plants, lowering kinetic inertia directly correlates to higher cycle speeds and lower motor wear. Custom CNC machined titanium end-of-arm tooling parts and lightweight clevis pins yield substantial efficiency gains in 24/7 operating regimes.
Medical Technology & Analytical Instruments
Serving clean-room production setups and analytical test equipment across Linz biomedical facilities. Our Grade 2 and Grade 5 micro fasteners down to M2 size offer certified bio-inert properties, non-magnetic profiles, and superior autoclave sterilization resistance.
Linz & Central European Procurement Trends
How stringent ESG frameworks, supply diversification, and mechatronic miniaturization dictate titanium purchasing in Upper Austria.
1. Decarbonization and Lightweight Lifecycle Calculations: The European Green Deal and corporate emissions scoring are compelling Austrian heavy engineering firms to evaluate complete asset lifecycles. Titanium’s near-infinite lifespan in harsh atmospheres eliminates recurring replacement cycles, scrap generation, and line shutdowns typical of coated carbon steels. For equipment deployed along the Danube or in chemical containment plants, the higher initial raw material cost is amortized rapidly through maintenance avoidance.
2. Strategic Supply Chain Redundancy (China's Titanium Valley Connection): Following recent disruptions in Eurasian metallurgical processing corridors, Central European OEMs are shifting away from monolithic single-point domestic brokerages. Forward-thinking procurement departments in Linz are contracting directly with dedicated integrated manufacturers based in Baoji. By cutting intermediate trading markups and accessing direct mill certificates (EN 10204 3.1), European buyers preserve production margins while retaining traceability.
3. Demands for In-Line Digital Transparency: European quality directors increasingly reject "black box" offshore fabrication. The modern procurement standard demands full digital inspection trails. Velnora addresses this paradigm directly by supplying real-time digital video feeds and CMM inspection documentation during the active Swiss-lathing and EDM wire-cutting stages, allowing Linz engineering teams to verify critical GD&T parameters before air transit clearance.
Why Linz Engineers Trust Velnora Titanium
Direct manufacturer capabilities headquartered in Baoji, China's Titanium Valley, operating under rigorous global export standards.
Origin Advantage: Baoji Ti Valley
Operating directly out of the Jinhe Industrial Park in Baoji since 2013, we tap directly into prime metallurgical ingots, certified sponge titanium supplies, and immediate specialized metallurgical laboratory access.
Multi-Standard Fabrication
Experienced machining to DIN, ISO metric, ANSI/inch, and JIS standard tolerances. Rapid prototype machining directly from 3D CAD files (.STEP, .IGES, .DWG) with comprehensive DFM review within 4 hours.
Video-Verified Production
Over 938+ active machining and production videos documented. Linz clients receive video verification of tolerance setups, laser engraving, anodizing coloration, and 100% thread gauge go/no-go checks.
Independent Verification
Ranked with a verified 4.9/5 buyer satisfaction score, verified on-site assessment records, international credit certification, and transparent export trade histories to Europe and North America.
Exotic Alloys & Timascus
Unmatched capability in high-end specialty alloys: Ti-6Al-4V Gr5, Commercially Pure Grade 2, and wire-EDM processed Timascus (Mokuti) damascus titanium for elite precision EDC and luxury technical hardware.
Seamless Logistics to Austria
Daily express air-courier integration (DHL, FedEx, UPS) directly delivering to Upper Austrian corporate addresses within 3–5 working days post-customs clearance, with DDP/DAP terms available.
Frequently Asked Questions: Linz Industrial Buyers
Direct metallurgical and logistics answers to facilitate procurement decision-making.
How does import clearance into Austria operate from your Baoji facility?
Shipments to Linz and Upper Austria are routed via air freight directly into Linz Airport (LNZ) or Vienna International (VIE). We provide comprehensive commercial invoices matching Austrian customs HS classifications (typically Chapter 8108 for articles of titanium). All packages are sealed with individual lot labeling, complete with packing lists and mill certificates.
Can Grade 5 titanium bolts replace 10.9 or 12.9 class steel in safety-critical joints?
No. Grade 5 titanium (Ti-6Al-4V) yields ~895-1000 MPa tensile strength, roughly matching property class 8.8 steel. Replacing class 10.9 (1000 MPa) or 12.9 (1200 MPa) safety bolts one-to-one in critical joints (such as major suspension uprights or heavy brake caliper anchors) requires engineering clearance or recalculating joint diameters up by one nominal size (e.g., M8 to M10).
What anti-galling lubrication is recommended for Austrian assembly floors?
Titanium threads require anti-seize paste containing copper, nickel, or specialty MoS2/ceramic compounds during dry assembly against aluminum or stainless steel blocks. Alternatively, specifying our PVD diamond-like carbon (DLC) or TiN-coated bolts completely eliminates micro-fretting without messy grease lubricants, ideal for clean assembly environments.
What are your Minimum Order Quantities (MOQ) for custom CAD parts?
For custom CNC turned or 5-axis milled titanium parts based on customer STEP/IGES drawings, our typical pilot run MOQ starts at just 50 to 100 units. For specialized Timascus Mokuti components, batch quantities as low as 1 to 5 pieces can be scheduled. Standard catalog fasteners carry an MOQ between 100 and 300 pieces depending on thread size.