
Direct Factory Catalog
Precision Titanium Brake Hardware & Fasteners
Engineered to DIN, ISO, and motorsport-grade tolerances. Explore our verified Titanium Grade 5 (TC4) components crafted for the Czech automotive, cycling, and performance engineering ecosystems.
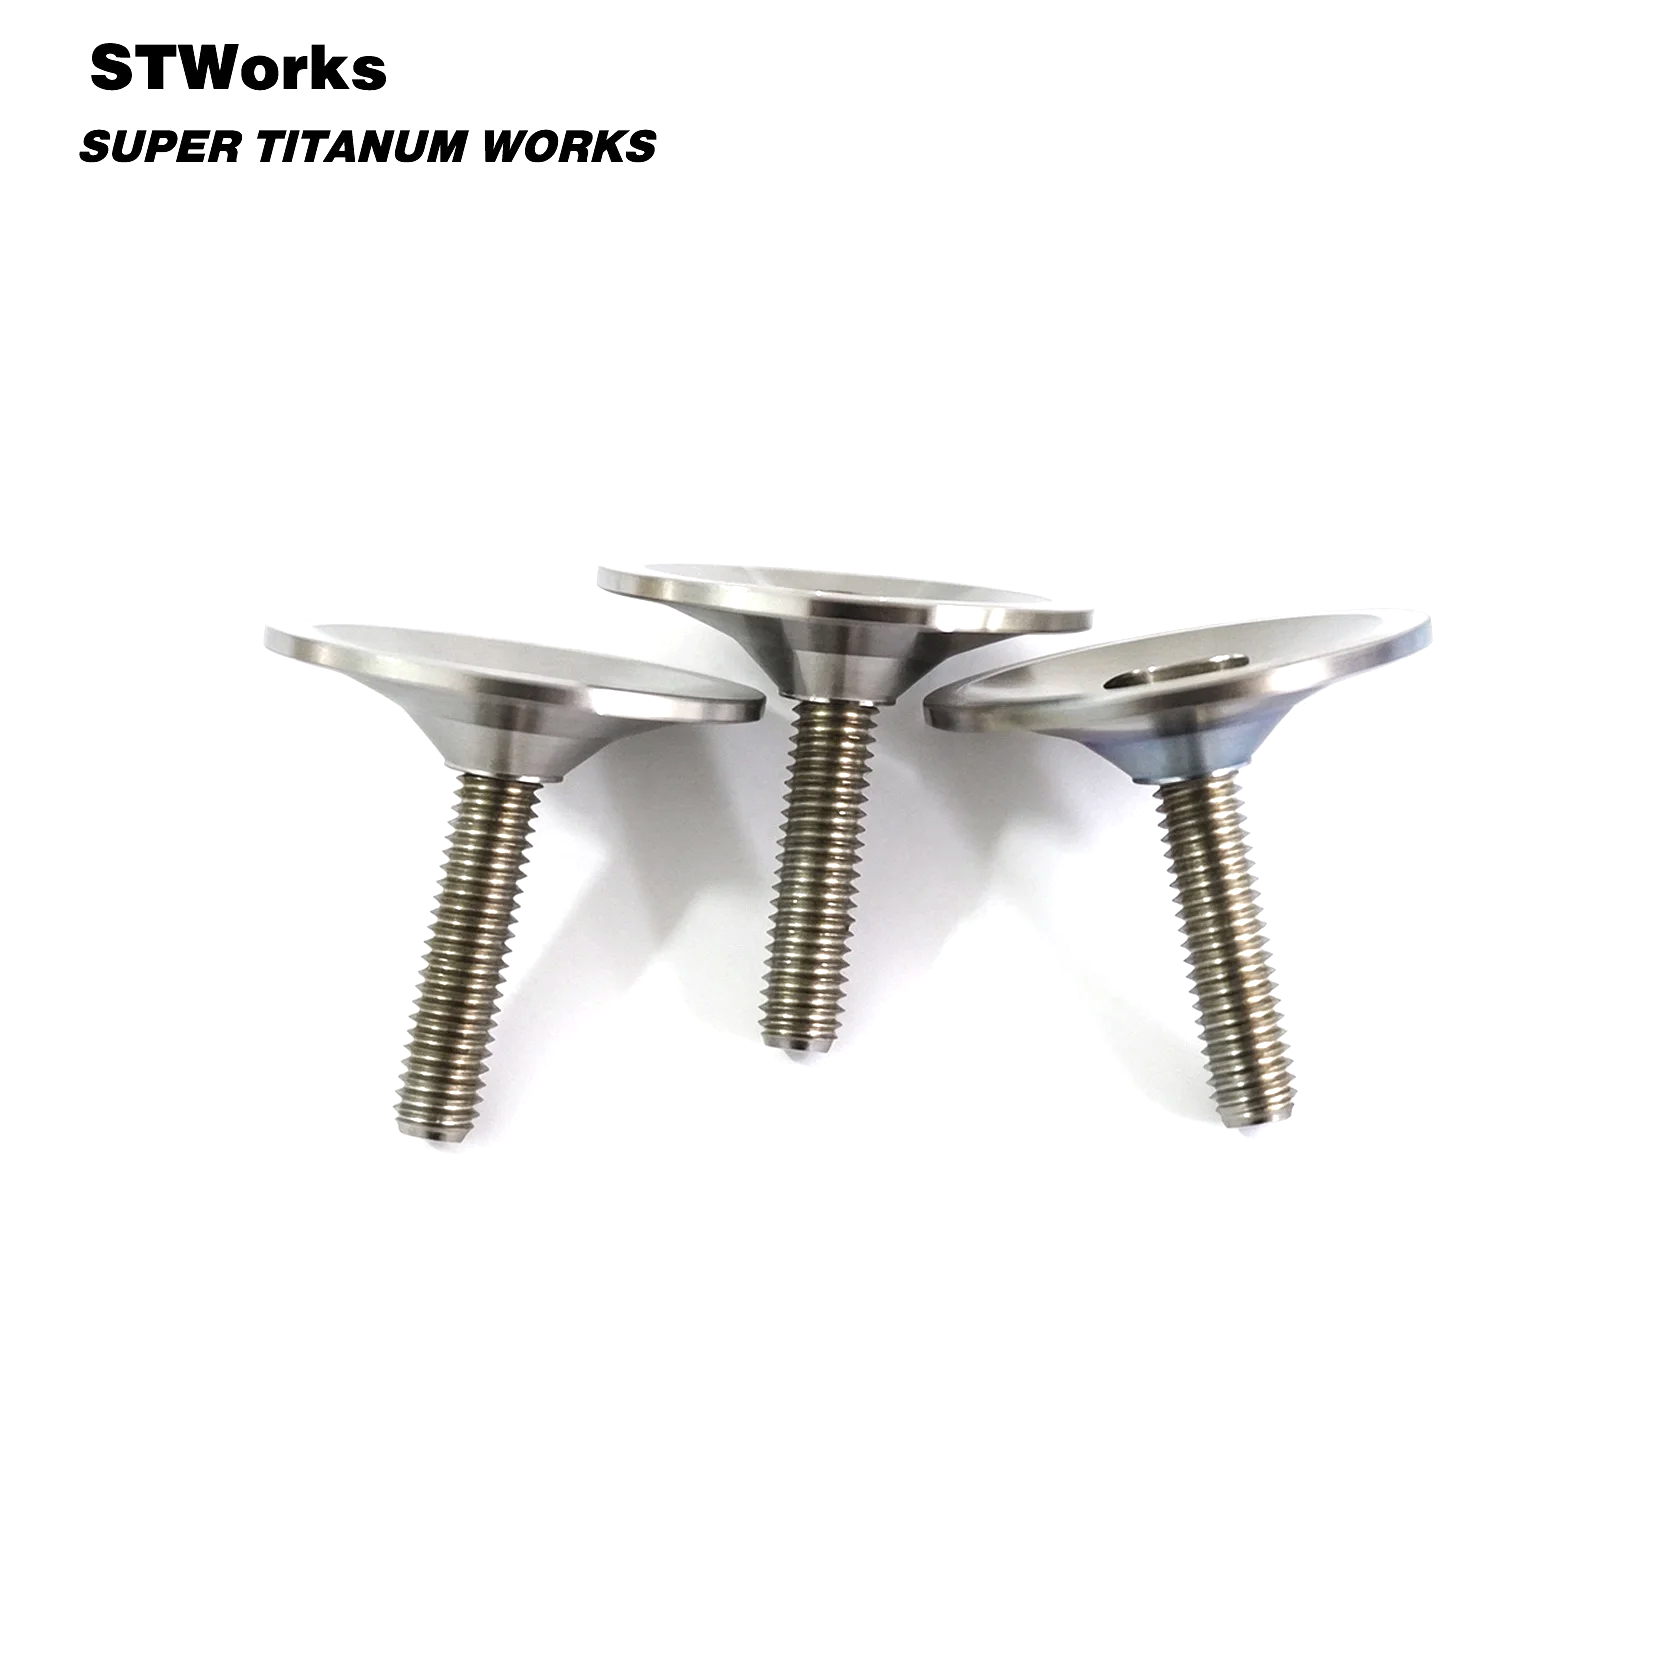
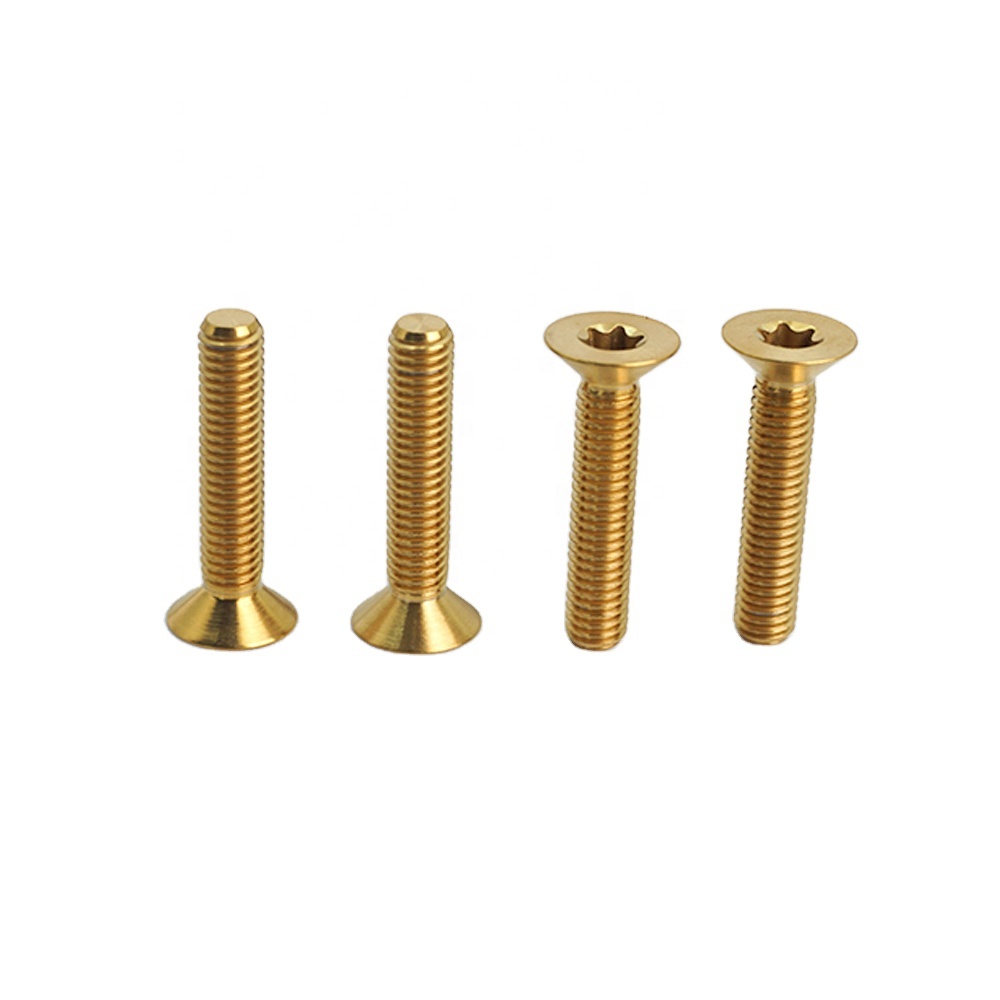


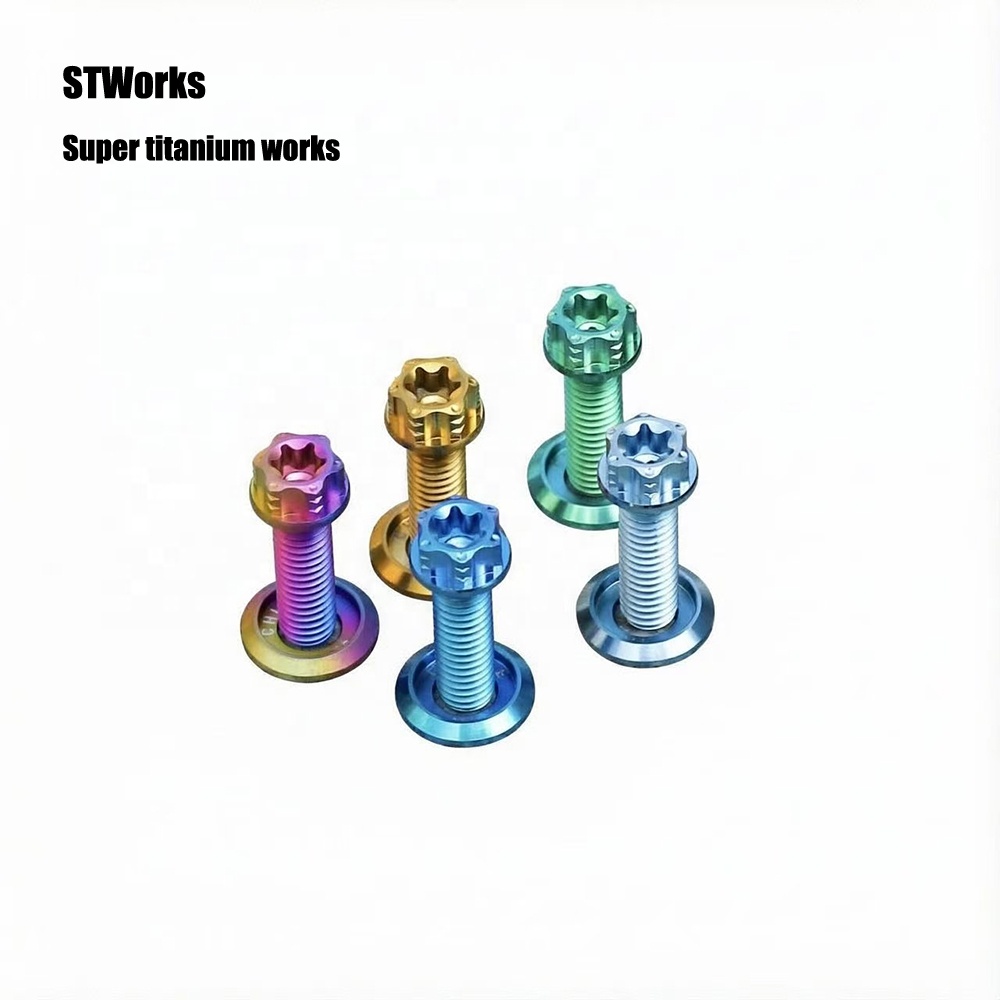
Industry Whitepaper Analysis
Engineering Grade 5 Titanium Brake Pins for Central European Road & Racing Demands
A technical guide on thermodynamic stability, galvanic isolation, and winter corrosion survival in the Czech Republic automotive and cycling sectors.
Braking system integrity is defined by the weakest structural interface under repetitive thermal cyclicity. In modern disc brake assemblies—spanning high-displacement rally cars, downhill mountain bikes (MTB), and road motorbikes—the caliper brake pad retaining pin operates as a critical sliding fulcrum. Standard OEM assemblies commonly employ mild zinc-plated carbon steel or cold-drawn 304 austenitic stainless steel pins. However, rigorous usage across the Central European terrain exposes fundamental metallurgical vulnerabilities in these traditional alloys.
The Czech Republic presents a distinct operational environment for braking assemblies. Characterized by severe winter road maintenance protocols involving concentrated calcium chloride ($CaCl_2$) and sodium chloride ($NaCl$) de-icing brines, alongside a deeply entrenched heritage of automotive manufacturing (centered around Mladá Boleslav, Kvasiny, and Kolín) and cross-country cycling trails in Krkonoše and Šumava, components face aggressive electrochemical attack. When conventional steel retaining pins corrode, iron oxide swelling causes the brake pad backing plate to bind directly on the pin. This results in uneven pad wear, brake dragging, premature fluid boiling, and catastrophic pad seizure.
Transitioning to Grade 5 Titanium (Ti-6Al-4V, Werkstoff 3.7165, TC4) resolves these systemic failures. Machined from certified aerospace-grade titanium round bar stock, Velnora titanium brake pins provide exceptional specific yield strength (≥ 825 MPa), complete chemical immunity to road de-icing salts, and a 44% reduction in unsprung reciprocating mass compared to steel counterparts.
| Physical & Mechanical Property | Gr5 Ti-6Al-4V (Velnora Spec) | AISI 304 Stainless Steel | 10.9 Carbon Steel (Zinc Plated) |
|---|---|---|---|
| Density (g/cm³) | 4.43 (Ultralight) | 7.93 | 7.85 |
| Yield Strength ($R_{p0.2}$, MPa) | 825 - 895 | 205 - 240 | 900 - 940 |
| Ultimate Tensile Strength ($R_m$, MPa) | 950 - 1050 | 515 - 650 | 1000 - 1040 |
| Thermal Conductivity (W/m·K) | 6.7 (Thermal Barrier) | 16.2 | 49.8 |
| Resistance to $CaCl_2$ De-Icing Brine | Immune (Passive $TiO_2$) | Susceptible to Crevice Pitting | Severe Rust / Galling Risk |
| Thermal Expansion Coeff. ($10^{-6}/K$) | 8.6 | 17.3 | 11.7 |
As illustrated above, Grade 5 Titanium exhibits an exceptionally low thermal conductivity rate of 6.7 W/m·K—less than half that of stainless steel and roughly one-seventh that of structural carbon steel. In high-performance brake calipers, the retaining pin bridges the superheated friction material backing plate with the aluminum caliper body. The lower thermal conductivity of Ti-6Al-4V creates a natural thermal choke, substantially restricting conductive heat transfer into the caliper housing, preventing hydraulic fluid vaporization (brake fade), and preserving piston seal longevity under intense braking sequences.
Localized Deployment
Key Application Scenarios in the Czech Industrial & Sports Landscape
From Bohemia's demanding automotive tier-suppliers to Moravia's precision motorsport fabricators and nationwide gravel racing teams.
Czech Rally & Hillclimb Racing
The Czech Republic hosts world-renowned rally stages such as the Barum Czech Rally Zlín. Under relentless hairpins and rapid descent braking, caliper temperatures exceed 600°C. Our custom CNC-turned titanium brake pins feature cross-drilled safety wire holes and rolled threads, ensuring zero pad binding and total vibrational stability on asphalt and gravel stages alike.
MTB & E-Bike Manufacturing
With top-tier bike assembly and frame manufacturing hubs across Liberec and Brno, Czech mountain and enduro builders demand lighter unsprung rotating mass. Replacing steel pad pins with Velnora Grade 5 titanium pins drops weight by over 40% while preventing pad stickiness in mud, snow, and gritty trail loam, offering smooth caliper pad return.
All-Weather Fleet Fleet Refits
Municipal emergency vehicles, heavy utility utility fleets, and transit systems traversing the Bohemian-Moravian Highlands face constant road salt during winter. Corrosion-bound brake pins lead to costly unscheduled maintenance. Our corrosion-free titanium replacement pins offer a permanent fix, reducing fleet brake overhaul cycles by over 65%.
12+
Years Precision CNC Expertise
1000+
Global B2B Tier Buyers
±0.005mm
Swiss Lathe Machining Tolerance
≤4 Hours
Drawing Review Response Time
Procurement Dynamics
Emerging Trends in the Czech & Central European Fastener Market
Key technological, regulatory, and sustainability shifts driving Czech engineers away from heavy plated alloys toward precision-machined titanium hardware.
Automotive Lightweighting & EV Shift
Czech automotive suppliers are heavily re-tooling for Electric Vehicles (EVs). Because high-capacity battery packs add massive weight, tier-one chassis teams are prioritizing unsprung mass optimization. Titanium caliper pins, banjo bolts, and bleeder screws provide direct weight offsets right at the wheel hub without sacrificing tensile strength.
Direct Digital CAD/CAM Sourcing
Czech engineering procurement departments increasingly bypass bureaucratic domestic middlemen to work directly with specialized primary manufacturers. By submitting STEP/IGES CAD models directly to Velnora, Czech workshops achieve high-precision custom production runs at highly competitive factory costs with certified material traceability.
Stringent EU Chemical Compliance
EU REACH directives are enforcing stricter limits on hexavalent chromium ($Cr^{VI}$) and toxic passivation coatings traditionally applied to steel bolts. Titanium alloys naturally develop an inert, non-toxic, self-healing oxide ($TiO_2$) passivated layer, making them an environmentally sound, fully compliant fastener solution for European OEMs.
Manufacturing Authority
Why Central European Engineers Trust Velnora Titanium Industry
Headquartered in Baoji—China's renowned Titanium Valley—since 2013, our specialist facility merges high-grade raw ingots with state-of-the-art multi-axis CNC Swiss turning centers.
100% Certified Ti-6Al-4V TC4
We source raw titanium exclusively from verified aerospace melt sources. Every consignment includes complete spectral composition documentation and mechanical yield certificates, guaranteeing zero inclusions, no porosity, and full compliance with DIN and ISO metallurgical requirements.
Thread Rolling vs. Thread Cutting
Unlike budget machine shops that cut threads onto pins, Velnora utilizes high-tonnage thread rolling dies. Cold-forming the threads preserves continuous unbroken grain flow across crests and roots, increasing dynamic fatigue resistance by up to 35% under harsh caliper cyclic loading.
Transparent Digital QC & Video Verification
Czech and European clients benefit from our digital inspection pipeline. Over 930+ production videos demonstrate our multi-axis Swiss CNC turning, wire EDM cutting, and CMM dimensional verifications. We provide video and photo milestones before any international shipment dispatches.
B2B Buyer Knowledge Base
Frequently Asked Questions by Czech Procurement Teams
Clear, engineering-backed answers addressing standards, galvanic interaction, thread galling, and customs logistics into the Czech Republic.
Can Grade 5 titanium brake pins cause galvanic corrosion inside aluminum calipers?
Titanium is electrochemically noble, which frequently raises questions among chassis engineers about potential galvanic corrosion when mated directly to cast or forged aluminum caliper bodies. In reality, titanium naturally forms a microscopic, highly stable passivation film of Titanium Dioxide ($TiO_2$) that functions as an electrical dielectric barrier.
To eliminate any theoretical risk in wet, electrolyte-rich winter environments in the Czech Republic, we recommend using a premium synthetic, copper-free, or ceramic-based anti-seize assembly paste (such as high-temperature molybdenum disulphide or PTFE lubricants). Furthermore, our factory offers micro-thin physical vapor deposition (PVD) and specialty hard anodizing, providing an additional non-conductive boundary layer.
How do Velnora's manufacturing tolerances compare to OEM Brembo, AP Racing, and Shimano pins?
Our brake pin shafts are produced on high-precision Swiss-type CNC lathes equipped with live tooling, enabling us to hold shank roundness and cylindrical runout within ±0.005 mm (ISO h6 to h7 fit classes). This micro-level tolerance guarantees effortless slide pin insertion, eliminates caliper rattle, and prevents brake pad tab notch wear over tens of thousands of kilometers.
What are the recommended torque values for titanium brake hardware?
Because Grade 5 Ti-6Al-4V features a modulus of elasticity of roughly 110-114 GPa (roughly half that of structural steel, 210 GPa), titanium fasteners exhibit greater mechanical elongation under tension. When tightening threaded pins or caliper mounting bolts, torque settings should be adjusted to approximately 75% - 85% of standard 8.8 grade steel values when using an anti-seize lubricant.
Thread galling is completely avoided by ensuring threads are rolled, clean of debris, lubricated, and torqued smoothly with calibrated manual torque wrenches rather than pneumatic or cordless impact drivers.
What is the typical shipping lead time and customs process for delivery into Prague or Brno?
For custom CNC production batches, lead times range from 12 to 22 business days depending on order size and surface treatment (PVD coating, sandblasting, or anodizing). We partner with major logistics carriers (DHL Express, FedEx, UPS) delivering directly to Czech commercial hubs (Prague, Brno, Ostrava, Plzeň) within 3 to 6 days air transit.
We provide full commercial invoices under appropriate HS codes (e.g., 8108.90 for wrought titanium articles), packing lists, and Material Test Reports (MTRs) to facilitate seamless clearance through Czech Customs Administration (Celní správa ČR).
Can Velnora fabricate custom brake pins from customer drawings or physical samples?
Yes. OEM and ODM bespoke manufacturing represents over 70% of our daily production volume. Czech engineering clients can submit 3D models in STEP, IGES, or 2D technical PDFs with explicit tolerance callouts. Alternatively, you can send physical brake caliper samples to our technical center; our engineers will perform optical CMM reverse-engineering, generate CAD layouts, and ship prototype samples for functional validation.
Ready to Upgrade Your Caliper Hardware with Precision Titanium?
Send our senior engineering team your technical specifications, 3D CAD files, or custom drawing requirements. We provide comprehensive DFM analysis, pricing, and certified material breakdowns within 4 hours.