TC4 Alloy
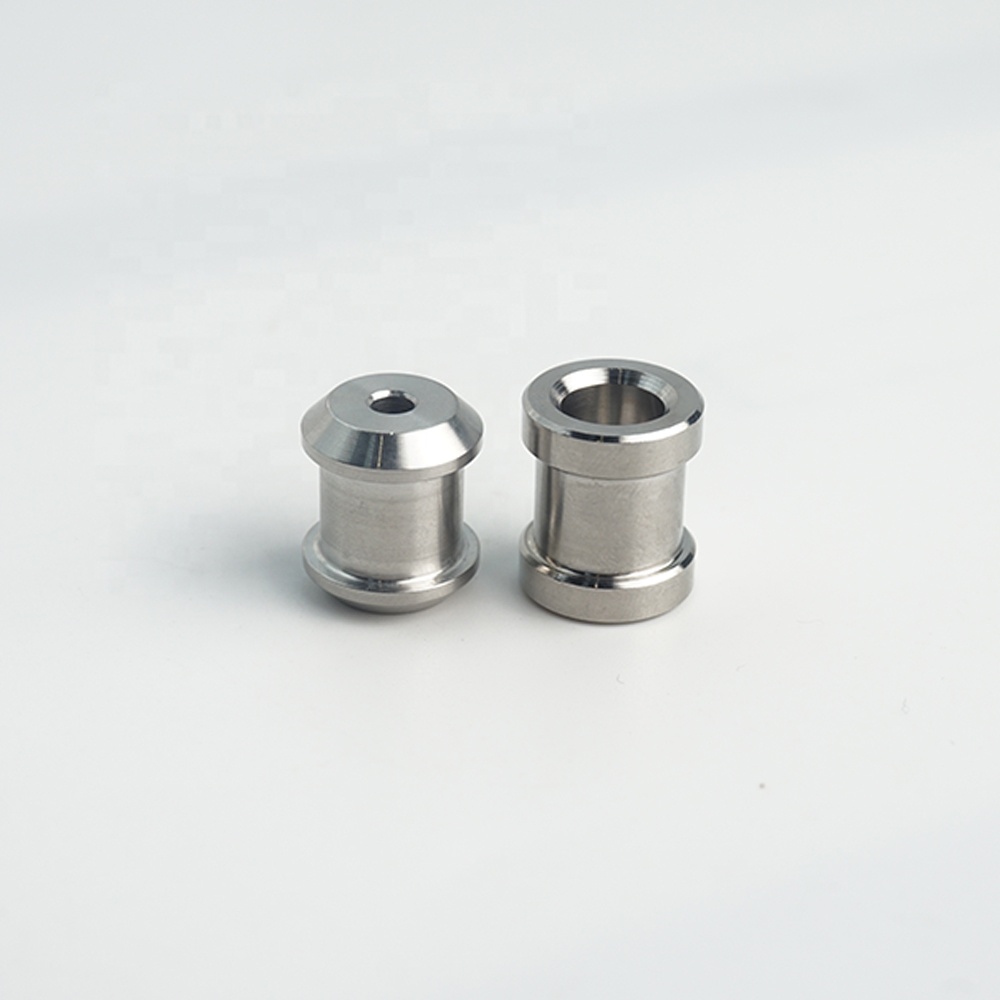
Factory-direct exports from Baoji, China's Titanium Valley, engineered to withstand the rigorous micro-climates, extreme elevation gradients, and high-vibration terrain of Cartago and the Cordillera Central.

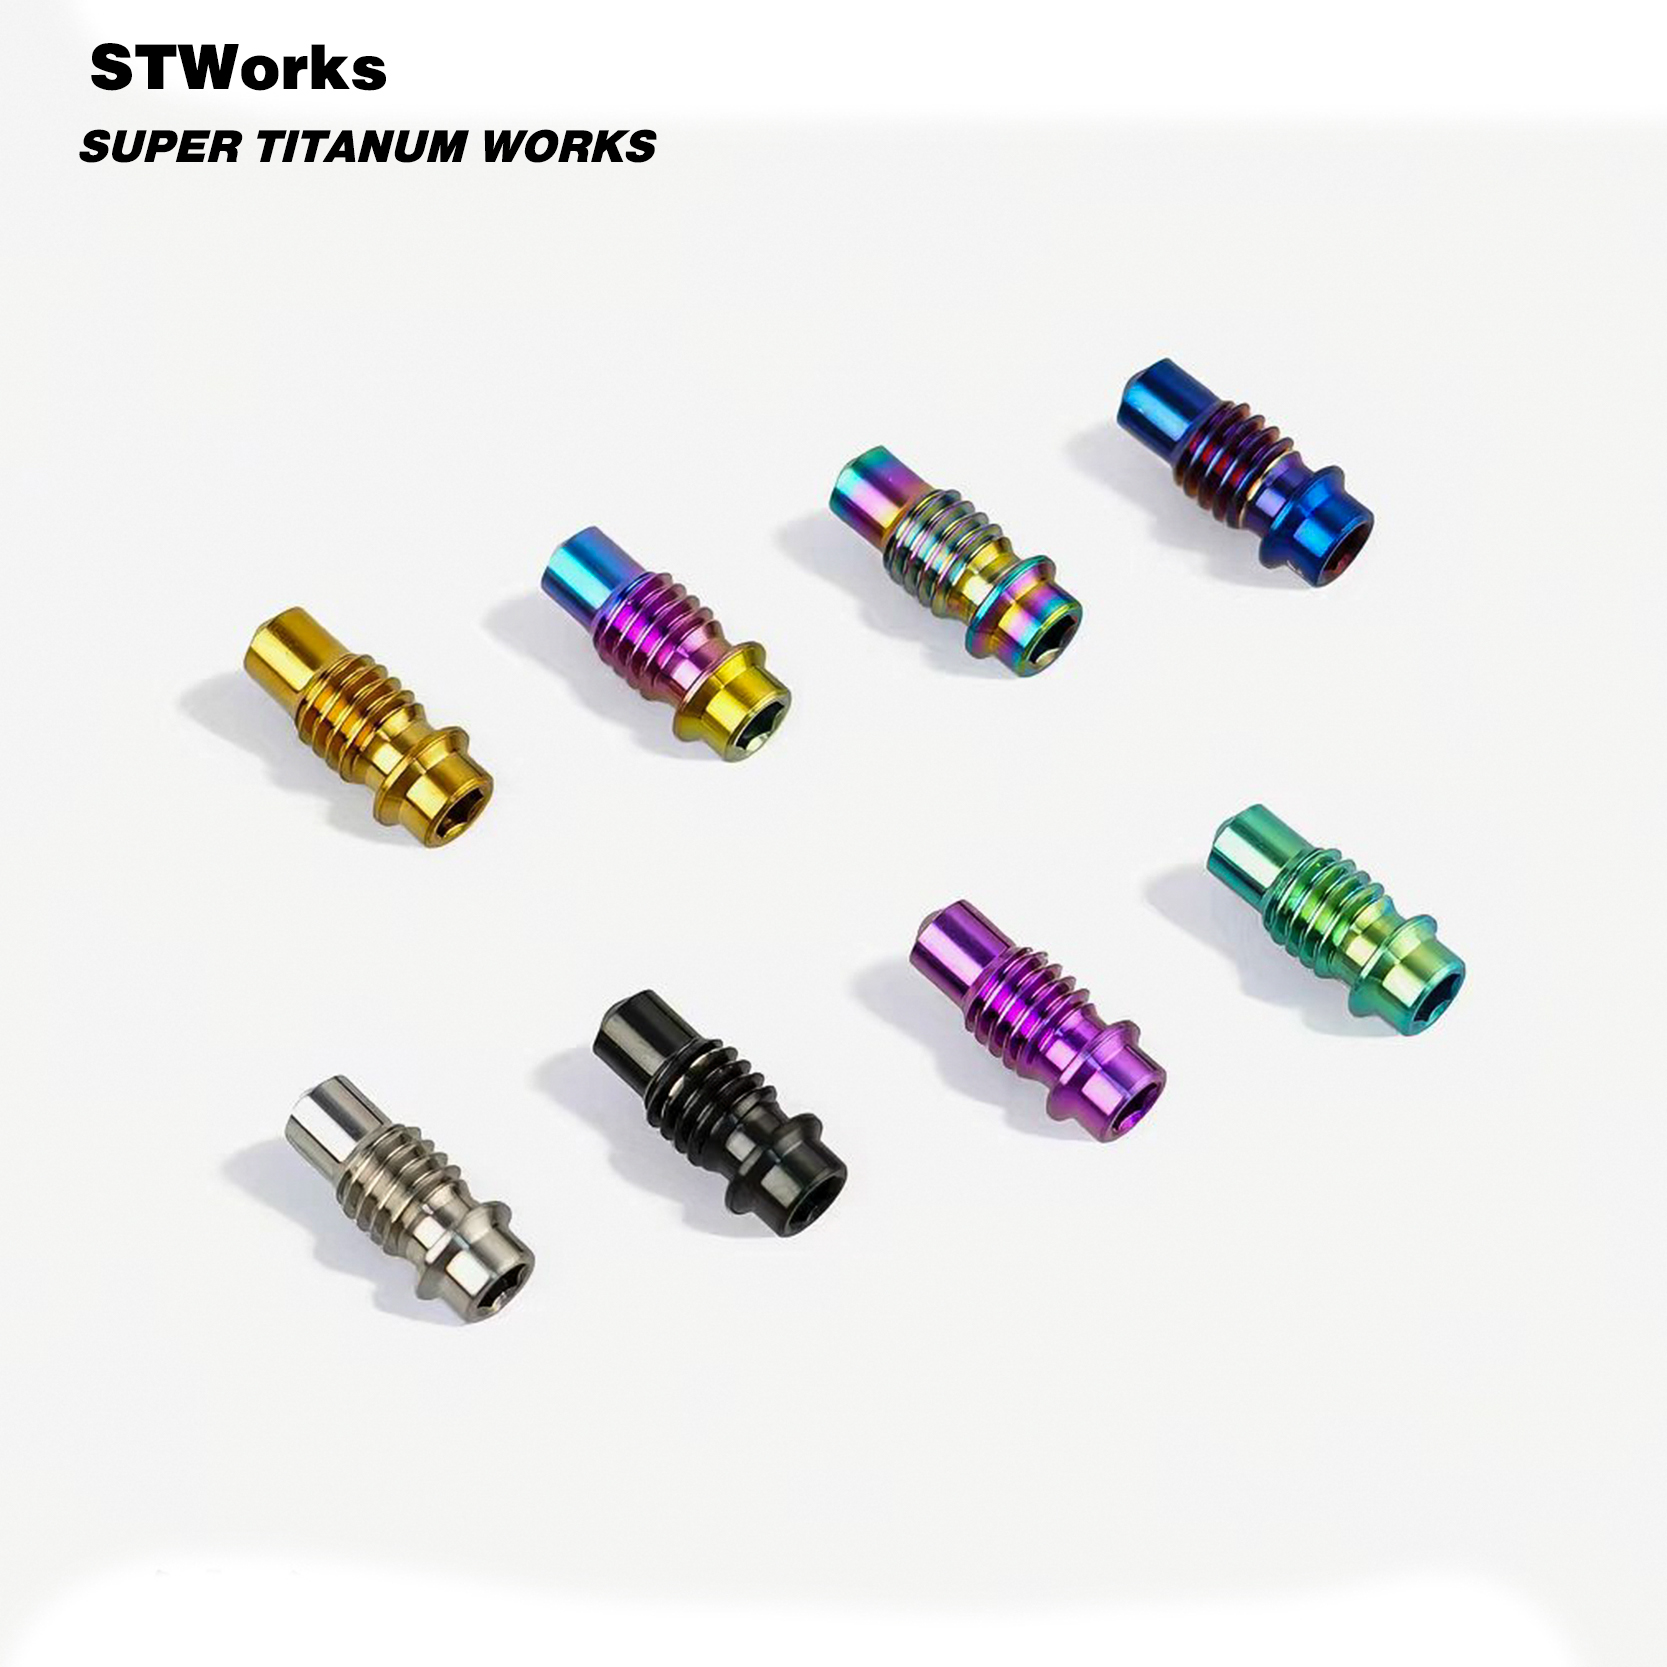
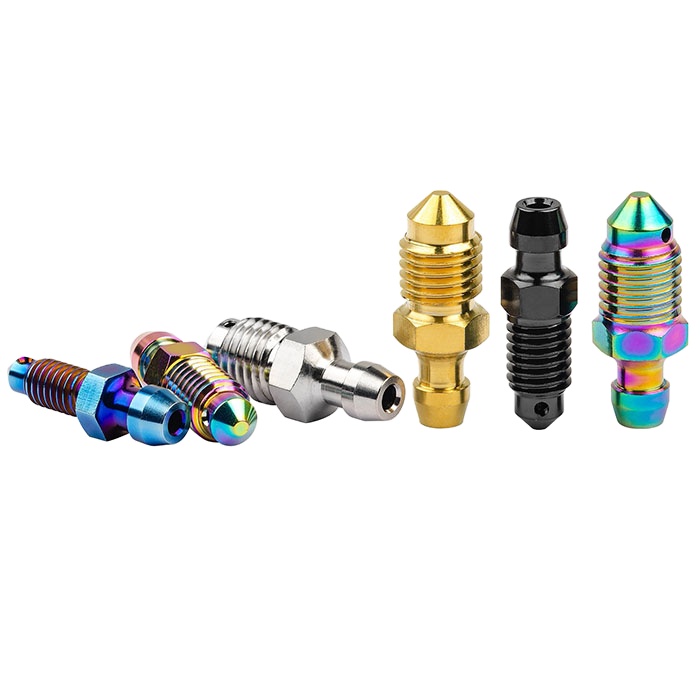
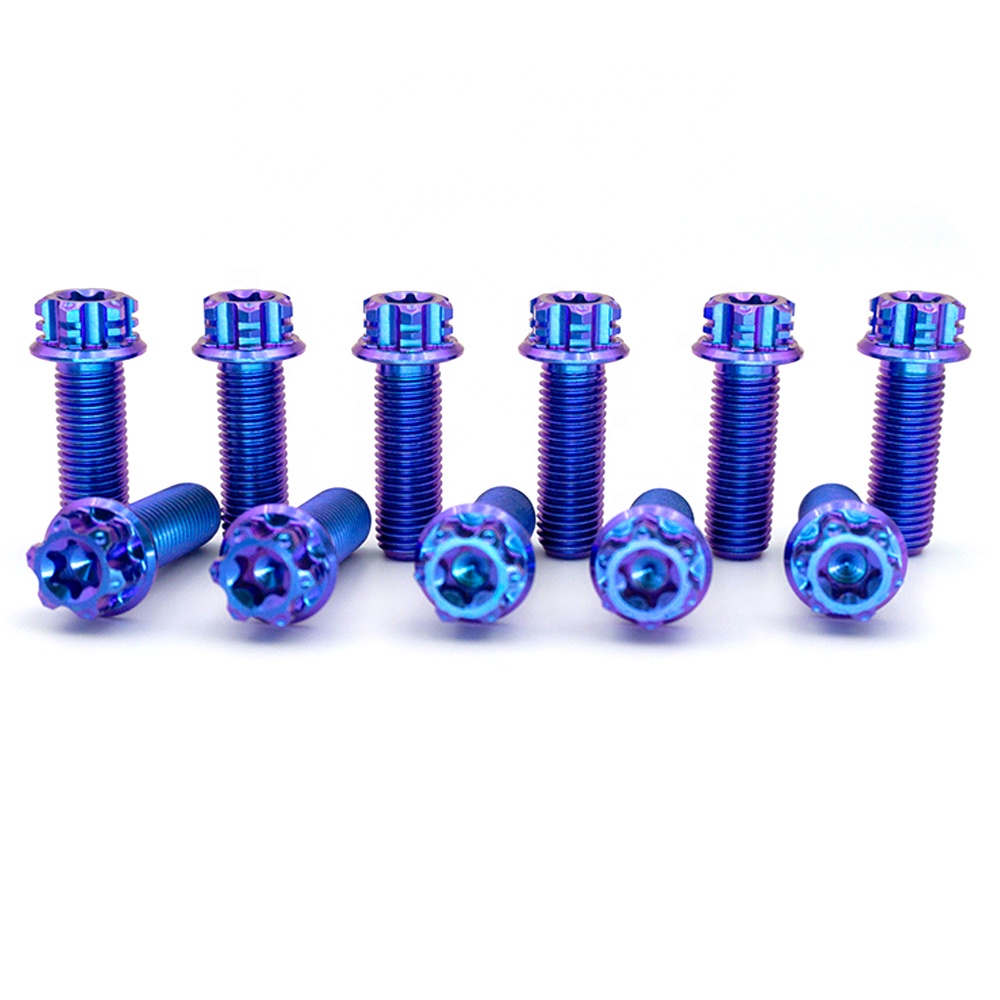
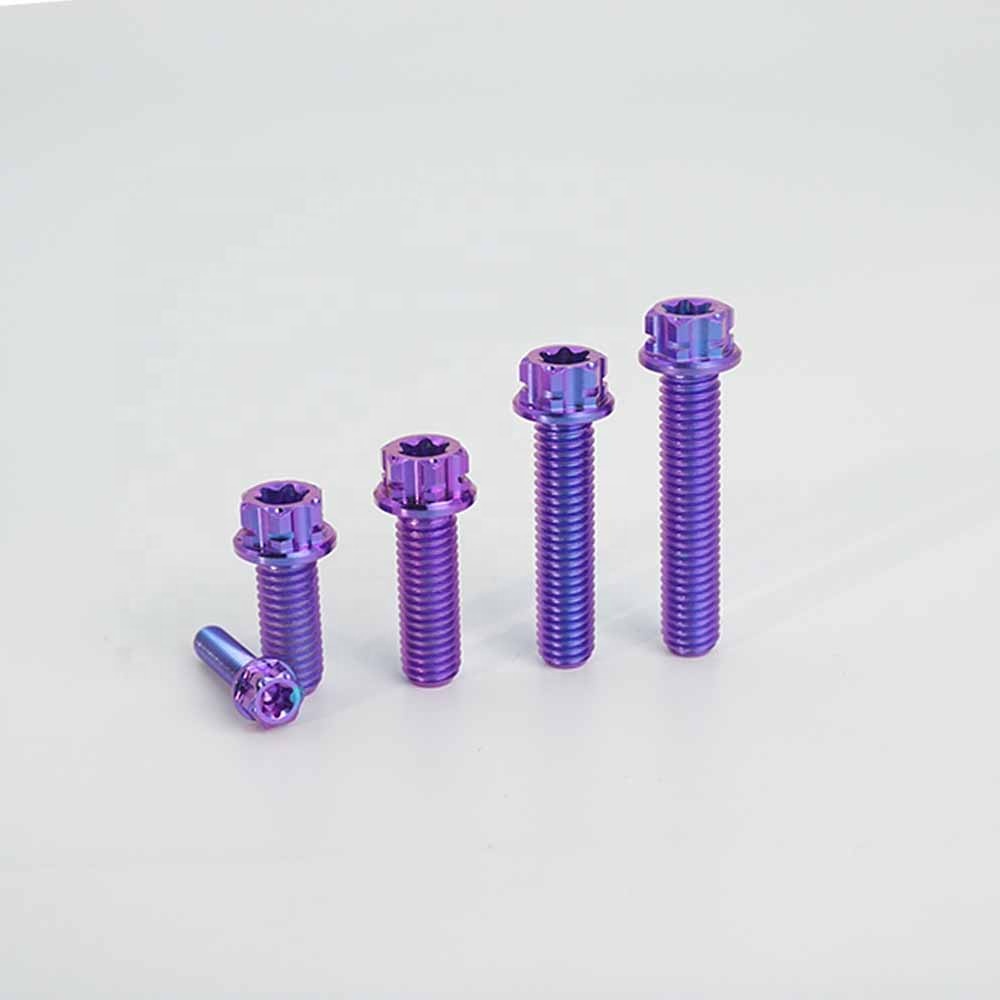
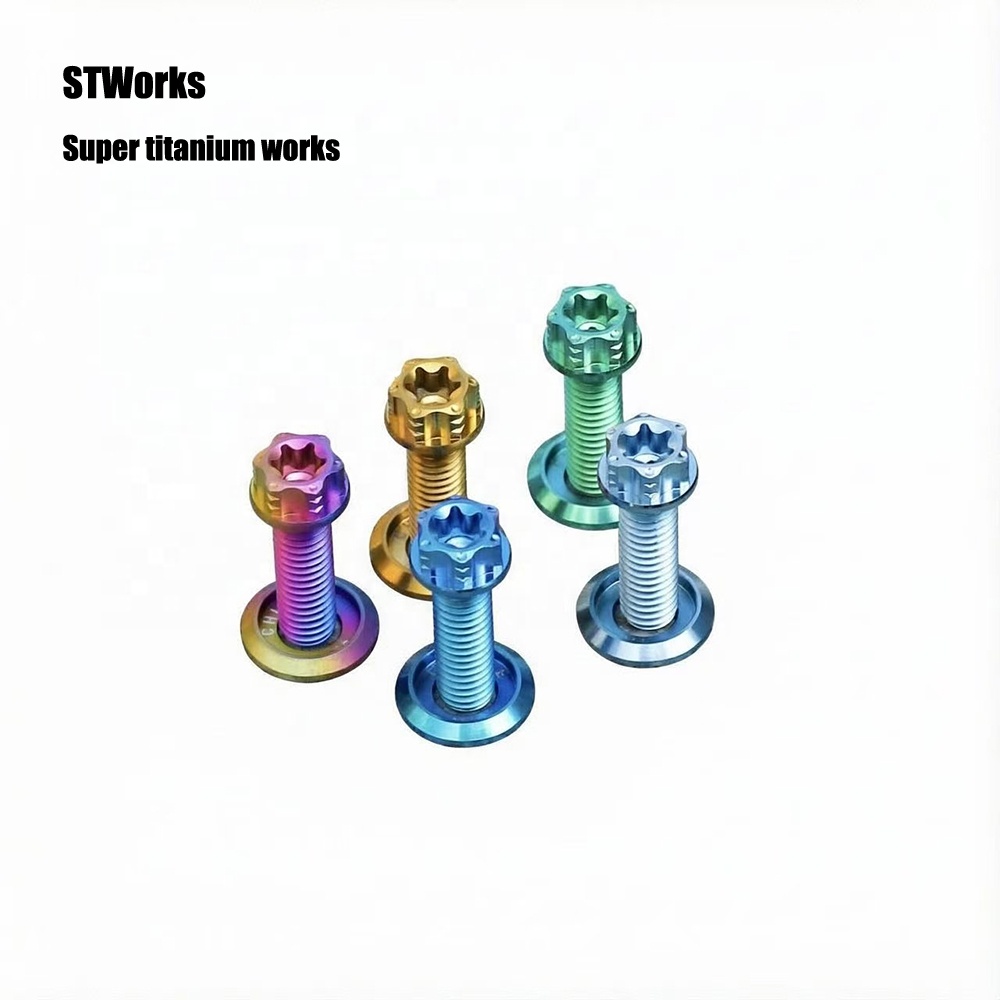
The Province of Cartago, Costa Rica, represents one of the most mechanically demanding environments in the Americas for high-performance bicycle hardware. Encompassing the northern slopes of the Cordillera de Talamanca, the sprawling agricultural basins of the Orosi Valley, and the precipitous volcanic ascents flanking the Irazú and Turrialba volcanic massifs, Cartago subjects cycling cockpits to punishing multidirectional mechanical loads paired with aggressive chemical degradation vectors. In this altitude bracket—ranging from 1,300 meters above sea level in the urban hub to over 3,400 meters at the volcanic summits—bicycle cockpits endure extreme thermal differentials, pervasive cloud-forest relative humidity exceeding 88%, and the airborne deposition of abrasive, sulfur-laden and silicate-rich volcanic particulates.
In standard bicycle assembly architectures, the steer assembly preload system comprises an internal star nut or compression expander plug, the stem clamp interface, and the structural top cap driven by an axial fastener (typically an M6x30mm or M6x35mm machine screw). While commonly regarded merely as a cosmetic dust cover by casual end-users, precision framebuilders, mechanical engineers, and professional team mechanics recognize the stem top cap as an essential dynamic calibration component. It applies controlled compressive axial preload to the upper and lower angular contact headset bearings (typically 45/45° or 36/45° IS42/IS52 configurations), eliminating micro-play across the fork steerer tube interface before the horizontal pinch bolts of the stem are torqued to specification.
Critical Engineering Principle: Under the high-frequency vibration spectrum typical of Cartago's rugged volcanic gravel ascents and asphalt descent chicanes (such as the treacherous descents down from San Juan de Chícua or Pacayas), conventional anodized 6061-T6 aluminum top caps and carbon steel bolts undergo severe galvanic pitting and microscopic thread galling. When galvanic potential exceeds 0.50V against carbon fiber steerer expanders or wet 7075 aluminum interfaces, unsealed steel fasteners seize, and thin stamped aluminum caps warp under uneven compressive clamping, resulting in catastrophic loss of bearing preload, headset ovalization, and steerer tube gouging.
Velnora Titanium Industry Co., Ltd., based in the high-precision aerospace hub of Baoji, China, engineers and exports specialized Grade 5 (Ti-6Al-4V, Werkstoff 3.7165) titanium bicycle stem top caps and integrated M6 fastening hardware specifically designed to eliminate these localized failure archetypes. By leveraging an elemental composition comprising 6% aluminum, 4% vanadium, balanced titanium, and minute interstitials, our Ti-6Al-4V alloy provides an ultimate tensile strength exceeding 895 MPa, an elastic modulus of 114 GPa, and a naturally forming, thermodynamically stable rutile-anatase titanium dioxide (TiO₂) passivation layer that renders our top caps chemically impervious to tropical rainwater, organic mud acids, and sulfurous atmospheric fallout across Costa Rica's Central Valley.
Operates at an exceptionally neutral electrochemical potential when seated against carbon steerer tubes, phenolic spacers, and alloy stems, completely arresting galvanic micro-corrosion.
Yielding at 828 MPa with half the modulus of steel, Gr5 titanium absorbs high-frequency trail buzz without yielding, preserving precise headset torque under severe downhill shock.
CNC turned from solid annealed billet to ±0.01 mm perpendicularity. Ensures zero side-load deflection on the steerer expander bung during preload torquing (2.0–3.5 Nm).
A direct analysis of fastener materials under exposure to moisture, sulfurous ash, continuous road shock, and high-tensile preloading.
| Performance Characteristic | Velnora Gr5 Titanium (Ti-6Al-4V) | Commercial 6061-T6 Aluminum | High-End 7075-T6 Alloy | Class 8.8 / 304 Stainless Steel |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 | 2.70 | 2.81 | 7.90 - 8.00 |
| Ultimate Tensile Strength (MPa) | 895 - 1050 | 310 | 572 | 515 - 800 |
| Yield Strength (0.2% Offset, MPa) | 828 | 276 | 503 | 205 - 640 |
| Elastic Modulus (GPa) | 114 | 68.9 | 71.7 | 193 - 210 |
| Resistance to Volcanic Acid / Pitting | Immune (Passivated TiO₂ Matrix) | Poor (Prone to intergranular attack) | Moderate (Prone to stress cracking) | Moderate (Pits under chlor/sulfur) |
| Galvanic Couple with Carbon Fiber | Virtually Zero Risk (< 0.10V) | High Risk (Requires barrier grease) | Very High Risk (Anodic oxidation) | Moderate (Galvanic cell in moisture) |
| Thread Galling / Seize Susceptibility | Zero when prepared with Ti anti-seize | High (Stripped hex sockets) | Medium (Socket roundout) | High when threaded dry |
| Cartago Durability Index (1-10) | 9.9 / 10 | 4.5 / 10 | 6.0 / 10 | 5.5 / 10 |
Note: Mechanical testing conducted in accordance with ASTM B348 (titanium bar standards) and ISO 3506 fastener testing criteria. Cartago Durability Index is an empirical score reflecting resistance to multi-year weathering under ambient Cartago elevation humidity and road particulate exposure.
The cycling economy in Cartago has undergone a profound transformation over the past decade. Once dominated primarily by budget commuting bicycles and seasonal road pelotons, the region has evolved into Costa Rica's premier technical testing ground for gravel, cross-country (XC), downhill (DH), and high-torque electric mountain bikes (E-MTBs). The iconic gravel trails interconnecting Tierra Blanca, Cot, and Pacayas, alongside extreme climbs such as the dreaded "El Empalme" heading towards Cerro de la Muerte, have drawn thousands of competitive amateurs and international adventure-tourists. Furthermore, events following historical routes of the world-renowned La Ruta de los Conquistadores traverse this terrain, placing extraordinary demands on mechanical reliability.
This demographic shift has spurred significant growth across Cartago's high-end bicycle service stations, boutique custom frame ateliers, and specialized distribution networks. Local mechanics and shop owners across Paraíso, Tres Ríos, and Cartago Centro are increasingly rejecting standard OEM factory fasteners that deteriorate within a single wet season. Instead, they specify premium aftermarket components that guarantee structural safety, weight minimization, and long-term aesthetic perfection.
Four primary commercial drivers underscore the soaring demand for Velnora's titanium stem top caps and precision hardware within the Cartago trade network:
Modern 85–100 Nm mid-drive e-bikes exert massive torsional leverage over long headtubes on Cartago's steep volcanic trails. Our Grade 5 top caps withstand intense tensioning without conical deflection.
Riders embarking on self-supported expeditions through Cartago, Turrialba, and the Orosi loop cannot afford fastener failure or stripped bolts in remote rain forests where replacement parts are unavailable.
Costa Rican bike shops leverage our OEM laser engraving and multi-spectral anodizing (burnt rainbow, ice blue, emerald gold) to market branded stem caps as signature high-margin shop merchandise.
Founded in 2013, Velnora Titanium Industry Co., Ltd. bridges aerospace metallurgical standards with commercial precision bicycle manufacturing for worldwide distribution.
Headquartered in the Precision Manufacturing Park of Baoji, Shaanxi, Velnora Titanium operates within the global epicentre of titanium extraction, forging, and CNC technology. Known internationally as "China's Titanium Valley," Baoji provides unprecedented direct access to vacuum arc remelted (VAR) titanium ingots, aerospace-certified lab testing facilities, and specialized multi-axis CNC machine centres. Unlike trading companies or general fastener agents that re-sell commodity hardware, Velnora is an authentic engineering manufacturer managing every step of production: from raw bar stock spectroscopic verification through high-speed swiss turning, thread rolling, automated deburring, precision broaching, ultrasonic degreasing, and computerized electrochemical surface treatment.
Our titanium bicycle stem top caps are manufactured from certified Grade 5 (Ti-6Al-4V) rods adhering to ASTM B348 and AMS 4928 aerospace specifications. By avoiding traditional casting or hot stamping—processes that can introduce internal crystalline voids and micro-porosity—our CNC machining process retains the continuous grain structure of cold-drawn titanium bar stock. Integrated countersunk recesses for M6 bolts are cut with specialized diamond tooling, ensuring a perfect flush fit that minimizes aerodynamic turbulence and completely eliminates water pooling inside the head assembly.
Every production lot ships with certified mill test certificates (MTC) documenting chemical analysis (Ti, Al, V, Fe, C, N, H, O) and mechanical elongation/tensile parameters.
For accompanying M6 top cap bolts, threads are cold-rolled rather than cut. This preserves continuous grain flow lines, increasing fatigue cycle life under vibration by over 300%.
Before dispatching cartons to Costa Rica, our QA engineers provide high-resolution optical comparator and micrometer inspection videos so overseas buyers can approve lots remotely.
Direct technical and commercial answers regarding titanium headset caps, torque parameters, and Costa Rican logistics.
Whether you manage a premier workshop in Cartago, distribute high-end cycling gear across Costa Rica's Central Valley, or build bespoke titanium frames, Velnora delivers aerospace reliability with full OEM customization. Speak directly with our titanium machining engineers today.