Engineered Titanium Hardware & Paracord Accoutrements
Machine-finished components machined from certified aerospace-grade titanium ingot. From custom lanyard beads to high-stress fasteners, review our top components specified across Texas maker and motorsport projects.
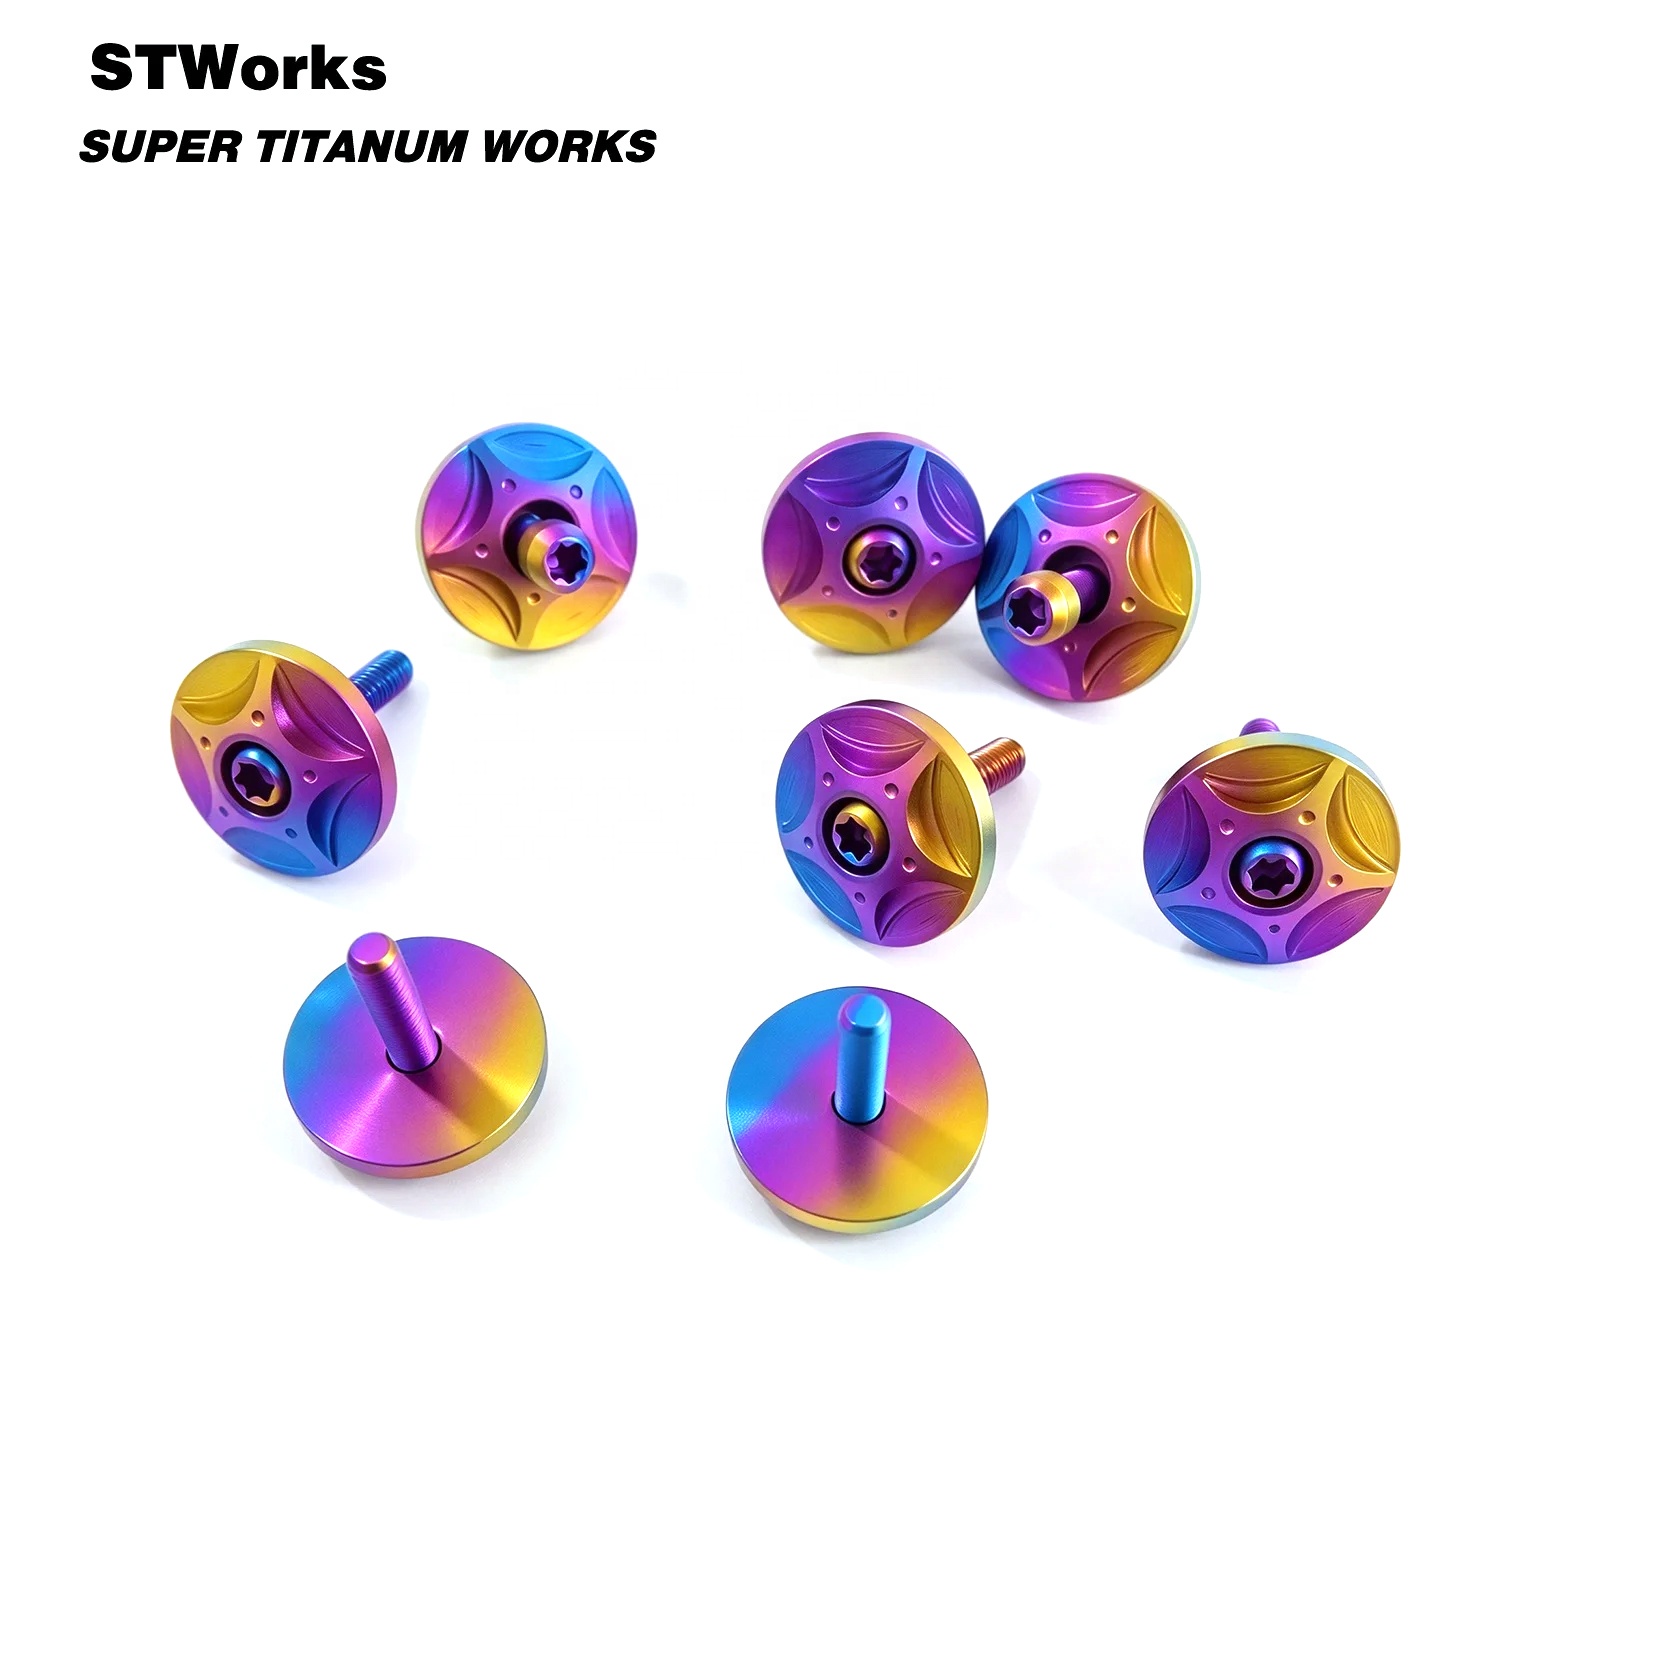
Factory Custom Ticat Ti Stem Top Cap Anodized M6 M6*30 Ti Bolt CNC Machined 90% Ti for MTB Road Bike
- Material: TC4 Aerospace Ti
- Finish: Anodized Spectrum
- Application: Bicycle Stem Assembly
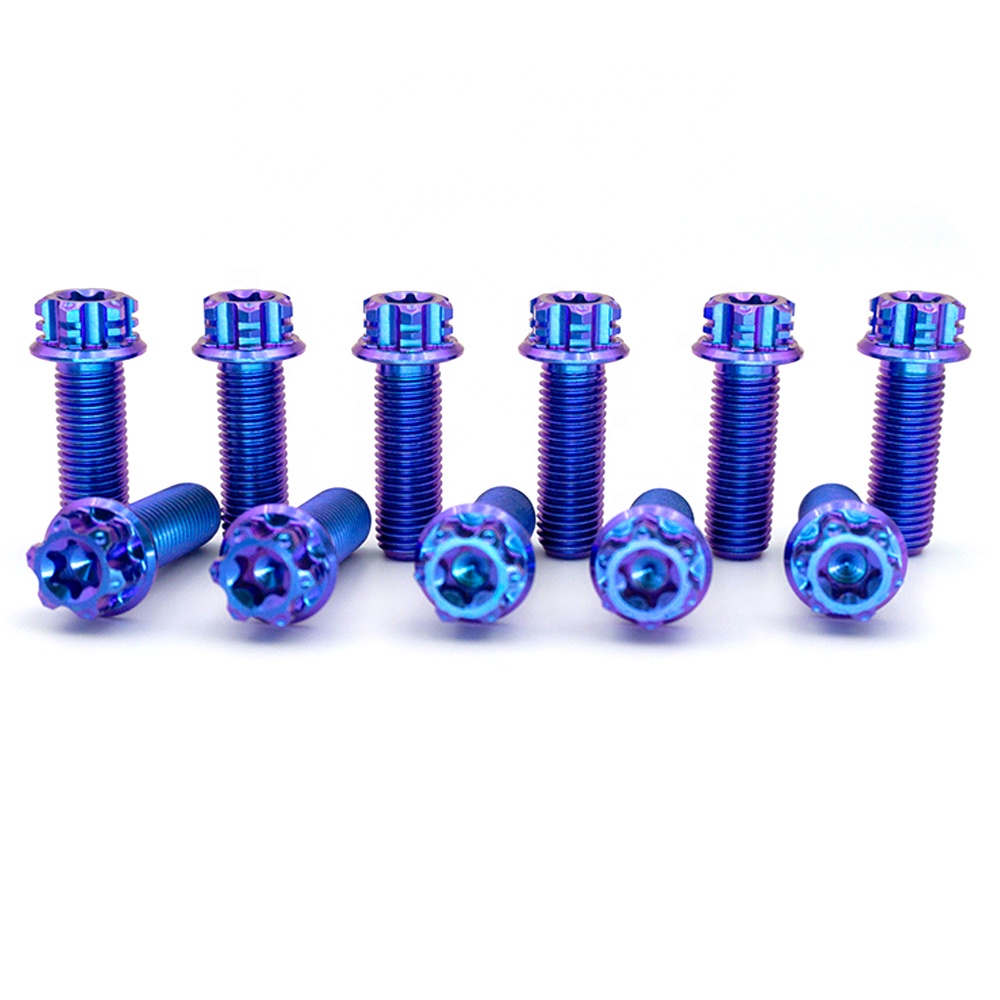
Titanium Alloy Hexagonal Flange Head Bolts and Screws for GR5 Motorcycle Modification
- Tensile: ≥ 895 MPa
- Drive: Flange Hex / Rolled
- Usage: Race Chassis / Caliper

TC4 Titanium Ti Torx M5x16 /18/20/25mm Tapered Head Bolt with Washer Screw for Bicycle Stem
- Standards: DIN 912 Equivalent
- Machining: 5-Axis Lathe Turn
- Weight: 44% of Steel
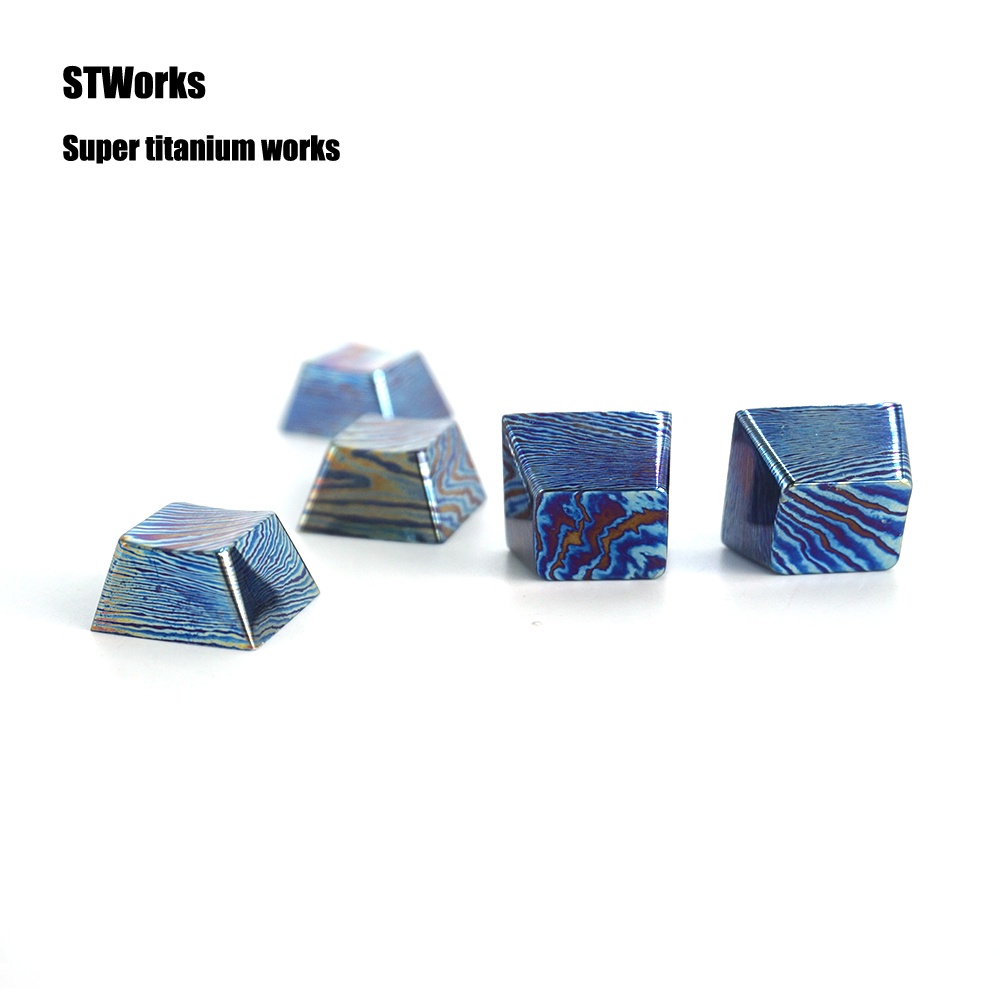
Titanium Gaming Keyboard Caps CNC Machined Broaching Wire EDM Stainless Steel Options PVD Coating
- Size: 18mm × 8.5mm (1U)
- Process: Precision Broaching
- Haptics: Tactile Collector EDC
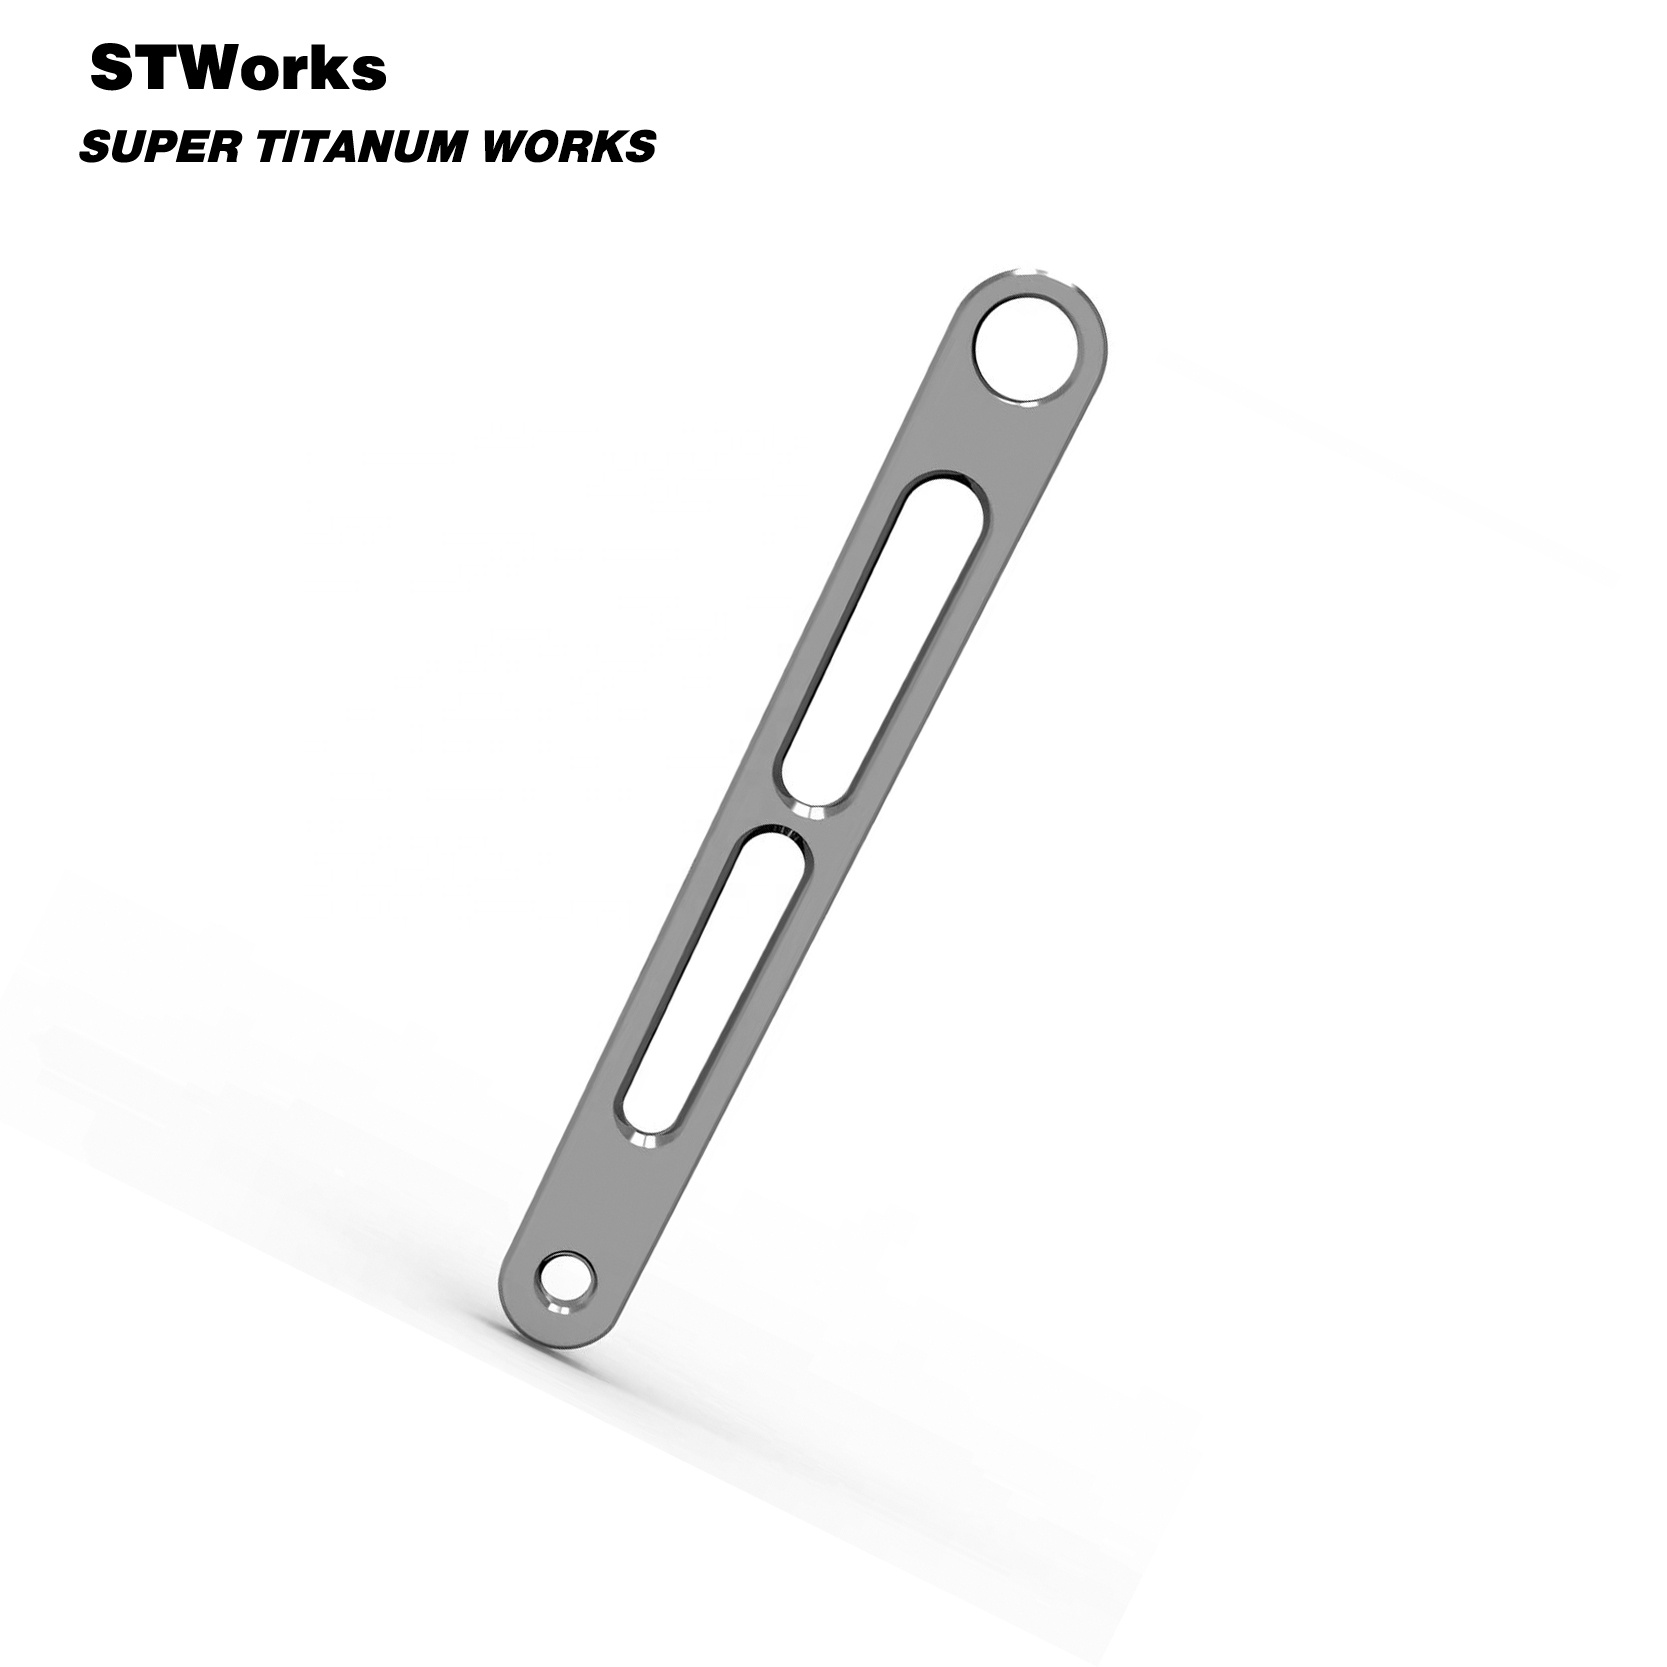
Titanium Alloy CNC Machined Multi-Function Spotlight Extension Bracket Auxiliary Light for Dirt Bike
- Finish: Micro-Bead Blasted
- Structure: Billet High-Torsional
- Compatibility: Universal Off-Road
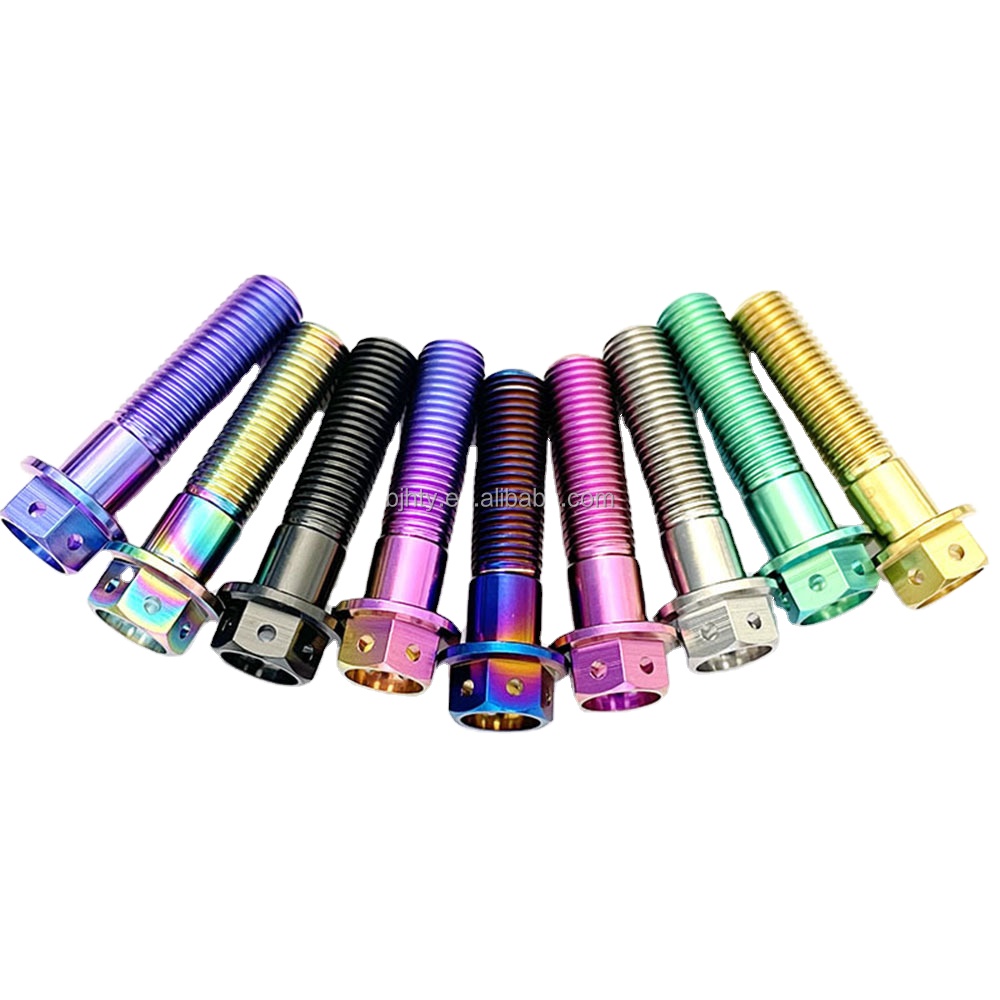
Titanium Alloy Double Drive Head Flanged Hex Bolts Ultra Light Corrosion Resistant M8/M10
- Feature: Pre-Drilled Safety Wire
- Class: 10.9 Class Load Capacity
- Alloy: Ti-6Al-4V Heat Treated

Customized Titanium Screws Mini Screws M2 M2.5 Cylinder Head Bolt Din912 Torx Micro Screw
- Tolerance: ±0.005 mm
- Heads: Torx / Hex Socket
- Use: Folder Knives / Optics
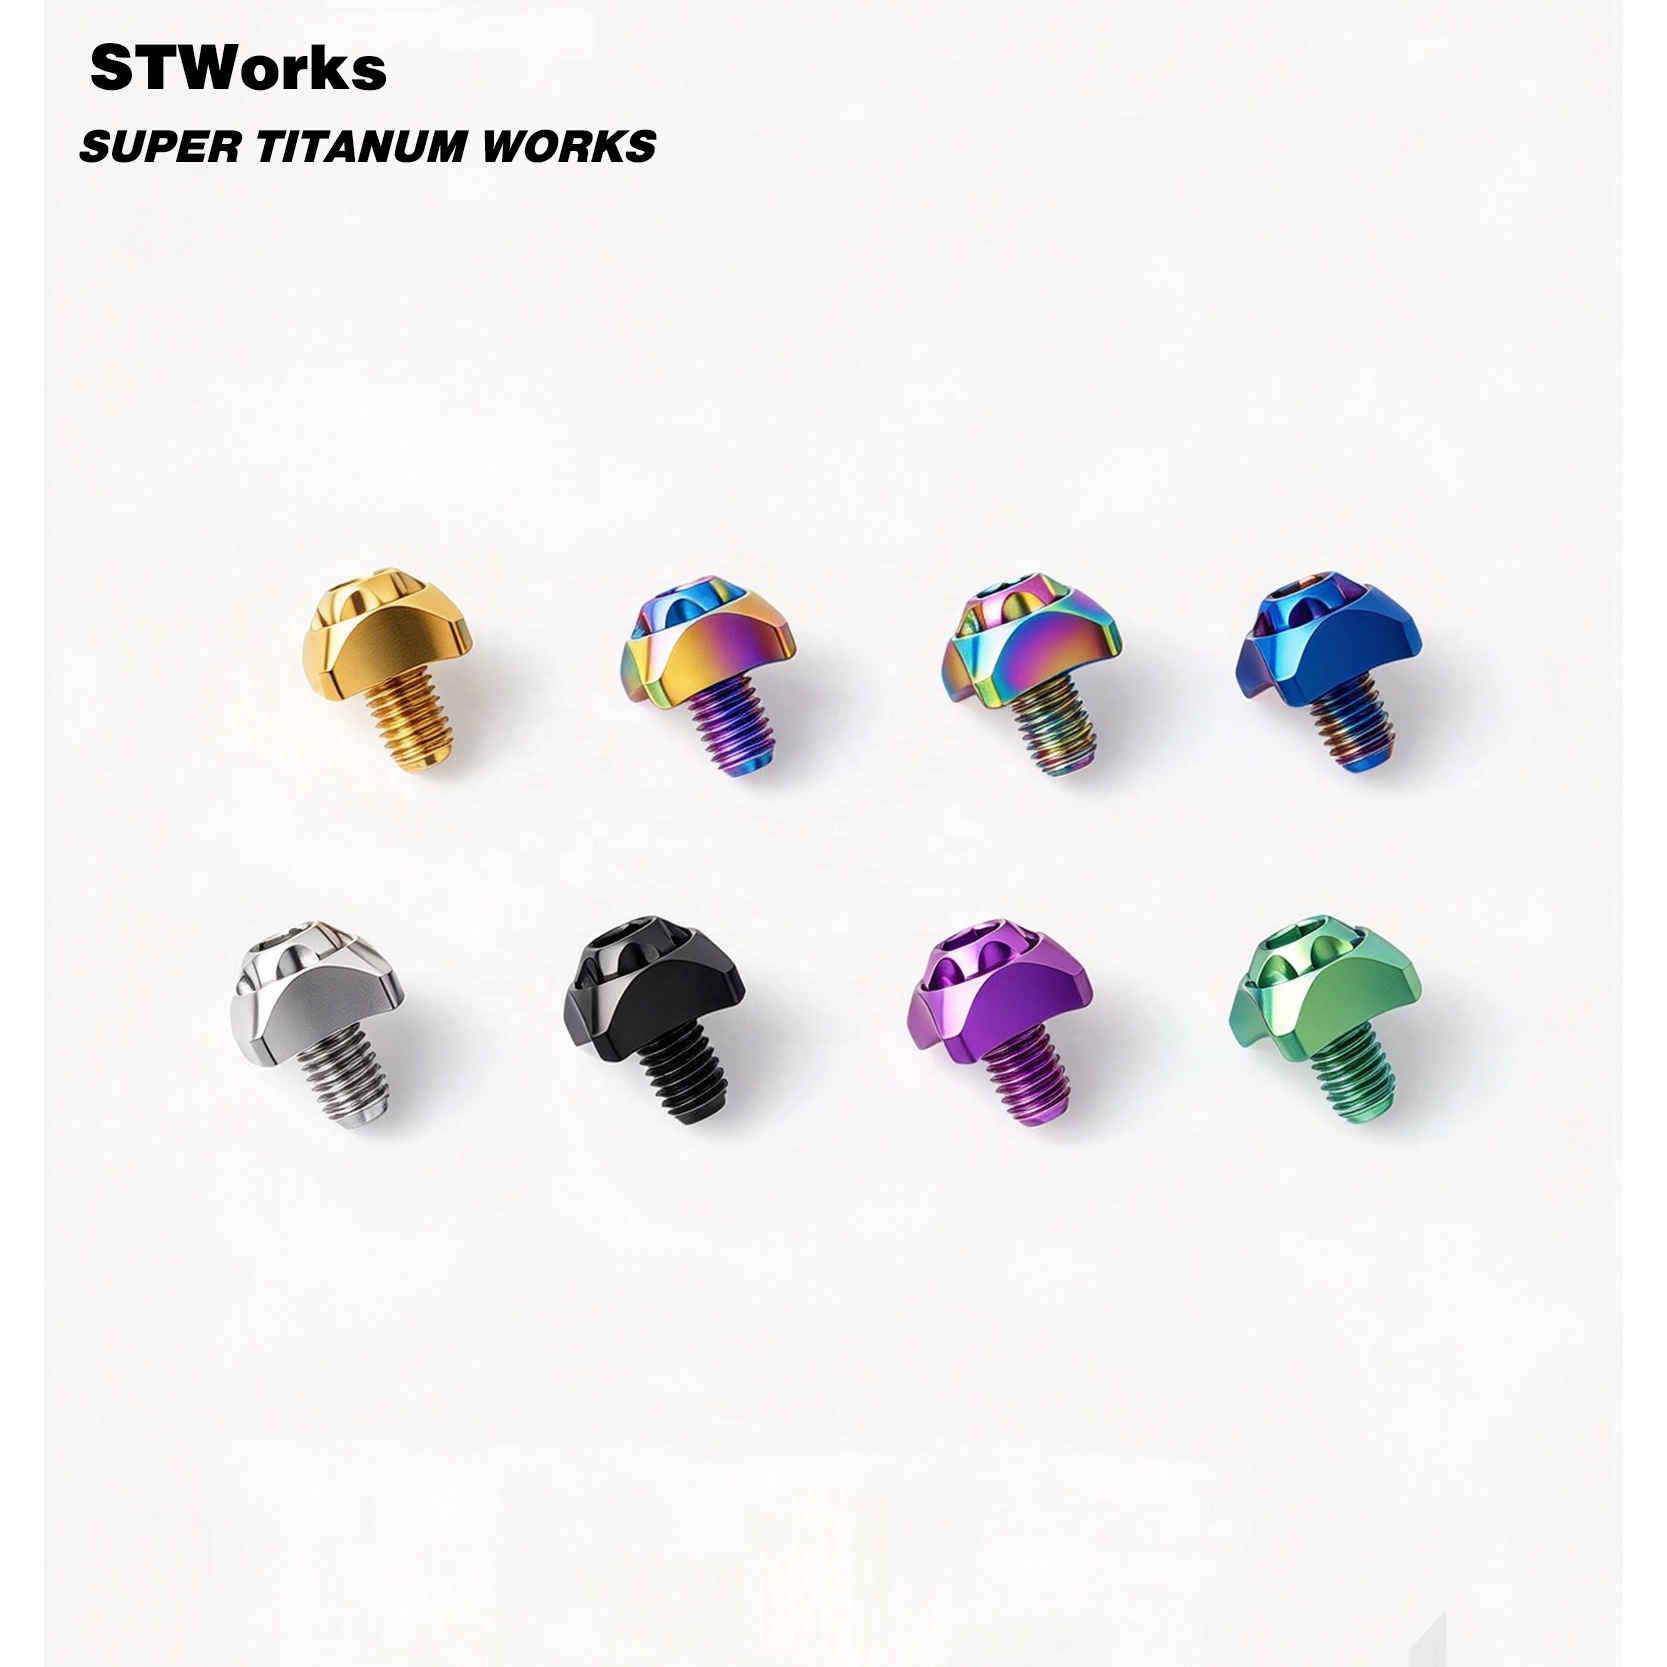
Titanium Screw & Shim Set for Shimano SRAM Front Derailleur Lightweight Bicycle Upgrade Parts
- Corrosion: Zero Pitting / Salt-Proof
- Kit: Countersunk + Curved Shim
- Fit: Shimano / SRAM Direct
Engineering Whitepaper: Metallurgical Superiority of Titanium Paracord Beads in Modern EDC Applications
In the high-performance Everyday Carry (EDC) space, material selection is not a cosmetic deliberation; it is a rigorous exercise in mechanical engineering, tactile kinematics, and surface chemistry. Paracord beads, begleri, lanyard terminals, and micro-accoutrements encounter relentless friction, environmental moisture, ambient sweat (containing corrosive lactic acid and sodium chloride), and impact shock. For industrial designers, custom knifemakers, and outdoor equipment manufacturers across Central Texas, Grade 5 Titanium (Ti-6Al-4V, classified under Chinese standard TC4) has definitively superseded 316L stainless steel, naval brass, and aircraft-grade 6061-T6 aluminum as the premier structural metal.
The manufacturing architecture of a commercial paracord bead demands far higher precision than standard ornamental turning. When securing military-standard Type III 550 cord (diameter 4.0 mm nominal) or commercial 750 paracord, the internal diameter of the bore must be machined to ±0.05 mm concentricity. Sharp interior steps or burrs generated during drilling can rapidly abrade the nylon sheath and inner core yarns. At Velnora Titanium Industry Co., Ltd., our CNC manufacturing protocols integrate high-pressure internal coolant flushing and 5-axis secondary deburring with micro-chamfering tooling, ensuring smooth pass-through channels that protect the structural integrity of synthetic fiber lanyards.
Tensile & Shear Thresholds
Grade 5 titanium features a yield strength exceeding 828 MPa, preventing deformation if the bead strikes concrete or rock during tactical deployments, field survival tasks, or everyday dropping scenarios.
Inherent Passive Oxidation
Upon ambient atmospheric exposure, titanium instantly generates a stable, self-healing rutile and anatase TiO2 passivating film (1–5 nm). It is virtually impervious to seawater, human sweat, and chemical cleaning agents.
Sub-Zero & High-Heat Stability
Operating temperature thresholds remain intact from -200°C up to 400°C without crystalline embrittlement, ensuring stability whether exposed to scorching Texas summer asphalt or sub-zero mountain conditions.
| Alloy Specification | Density (g/cm³) | Tensile Strength (MPa) | Modulus of Elasticity (GPa) | Corrosion Resistance | Tactile Warmth / Skin Sensitivity |
|---|---|---|---|---|---|
| Gr5 Titanium (Ti-6Al-4V / TC4) | 4.43 | 895 - 1000 | 114 | Immune to chlorides, sweating, acids | Biocompatible, low thermal transfer (warm touch) |
| Gr2 Pure Titanium | 4.51 | 345 - 450 | 103 | Excellent chemical resistance | Ultra-biocompatible, softer surface hardness |
| 316L Stainless Steel | 7.98 | 580 | 193 | Good, but susceptible to pitting | Cold tactile response, contains nickel allergens |
| C36000 Free-Cutting Brass | 8.50 | 380 | 97 | Rapid tarnishing, verdigris formation | Strong metallic odor, heavy pocket dragging weight |
| 6061-T6 Aluminum | 2.70 | 310 | 69 | Moderate; relies on delicate dye anodize | Dents easily on drops, thin coating wears rapidly |
Localized Austin Application Ecosystem: Tech Maker Innovation Meets Texas Outdoor Durability
The greater Austin metropolitan area—spanning downtown design ateliers, the Round Rock and Pflugerville technical manufacturing corridors, and adjacent Texas Hill Country craft knife workshops—occupies a singular position in the modern North American hardware marketplace. Unlike purely industrial procurement regions, Austin exhibits a vibrant fusion of high-tech software/hardware engineers, outdoor tactical purists, competitive shooting athletes, and custom cutlery artisans.
1. Custom Folding Knife & Fixed-Blade Lanyard Assembly (Artisan Cutlery)
Austin is home to an active guild of bespoke knife makers and collectors who demand premium accoutrements to complement S90V, MagnaCut, and Damascus steel blades. A hand-ground pocket knife costing upwards of $600 cannot be paired with a cast zinc alloy or cheap plastic lanyard pull. Austin knifemakers specify Velnora’s CNC-turned TC4 titanium beads because our precision micro-grooving, fluting, and stonewashed surfaces echo the precision blade finishes. Furthermore, our ability to produce Timascus (pattern-welded titanium composite) beads creates a cohesive match with custom pivot collars and pocket clips.
2. Austin Tech Executive & Hardware Developer EDC Collectibles
Within Austin’s thriving “Silicon Hills” campuses—from tech campuses along MoPac to startup hubs in East Austin—tactile EDC pocket gear functions as both functional utility and professional expression. Kinetic begleri beads, titanium worry beads, and CNC-machined titanium gaming keycaps (such as our 1U broached Esc caps) serve as desktop executive gear. Titanium's physiological inertness guarantees zero skin irritation during prolonged handling, while its low thermal conductivity avoids the jarring cold feel of steel desk tools.
3. Hill Country Outdoor Sporting, Survival & Marine Operations
From water expeditions on Lake Travis and Lady Bird Lake to tactical excursions across rugged Hill Country ranchlands, equipment is subjected to high humidity, river mud, and alkaline dust. Standard brass or copper beads oxidize rapidly, creating unpleasant smells and green verdigris stains on bright paracord strands. Gr5 titanium remains completely non-reactive. Our multi-bore beads accommodate double-passed 550 strands or integrated 750 paracord with zero swelling, rotting, or galvanic corrosion when looped alongside coated knife steels.
Austin Market Trends: Sourcing Shifts, Micro-Manufacturing, and Supply Chain Directness
Procurement directors and brand founders throughout Travis and Williamson counties are actively overhauling their supply chains. Three defining macro trends currently dictate B2B titanium ordering behavior in the Austin sector:
A Shift Toward Factory-Direct CNC Sourcing over US Distributor Markups
Traditionally, Austin hardware startups and knife brands purchased finished titanium EDC components from regional domestic importers who applied a 250% to 400% markup over base manufacturing costs. Today, Austin designers communicate directly with specialized factories situated in Baoji, Shaanxi—globally recognized as China’s Titanium Valley. By leveraging direct engineering channels with facilities like Velnora, Austin businesses retain strict design sovereignty, access raw material mill certificates, and cut unit procurement costs by more than half while maintaining ±0.005 mm machining accuracy.
Demand for PVD, DLC, and High-Voltage Anodizing Spectrum Customization
Simple tumbled grey titanium no longer satisfies competitive consumer retail expectations. Buyers in Austin demand nuanced electrochemical finishes. Standard low-voltage anodizing (12V–25V) produces deep bronzes and purples, while high-voltage baths (80V–110V) yield brilliant teals, vibrant emerald greens, and high-purity magentas—achieved purely through optical light wave interference with no organic dyes. For extreme scratch resistance, Physical Vapor Deposition (PVD) titanium carbo-nitride (TiCN) and Diamond-Like Carbon (DLC) provide satin-black tactical finishes measuring over 2500 Vickers hardness.
Micro-Batch Prototyping (50–100 Units) Scaling to Full Production Runs
With agile product development cycles dominant across Austin’s consumer hardware landscape, brands prioritize factories capable of low-volume production agility. Manufacturers who enforce rigid 10,000-piece minimum order quantities (MOQs) are being bypassed for specialized CNC producers who offer 50-to-200 piece pilot batches. This allows Austin creators to run limited-edition product drops, validate ergonomics in field communities, and iterate geometries rapidly before authorizing volume output.
Why Austin Innovators Partner with Velnora Titanium Industry Co., Ltd.
Since our founding in 2013 in the precision manufacturing zone of Baoji, China, Velnora Titanium Industry Co., Ltd. has bridged the gap between metallurgical raw material production and high-tolerance CNC output. When sourcing titanium paracord beads, standard fasteners, and custom mechanical hardware, our enterprise infrastructure delivers clear commercial advantages:
Baoji Raw Material Ecosystem
Direct access to genuine vacuum-arc remelted Ti-6Al-4V bar stock with complete chemical composition and physical tensile documentation. No recycled scrap, porosity voids, or alloy degradation.
Transparent Live Video QC
We remove overseas procurement blind spots. We film live high-definition spindle cutting, coordinate measuring machine (CMM) inspections, and ultrasonic cleaning cycles, sending them to your engineering desk before boxing.
Direct CAD/STEP Ingestion
Upload your 3D models in STEP, IGES, or SolidWorks native formats. Our senior CNC machinists evaluate toolpath approach angles, draft radiuses, and thread relief features within 4 business hours.
Frequently Asked Questions for Austin Hardware Buyers
Clear, technically rigorous answers addressing shipping transit, tolerances, alloy verification, and custom tooling.
What is the standard lead time for titanium paracord bead shipments to Austin, Texas?
For custom CNC production runs (100 to 1,000 units), manufacturing lead time at our Baoji facility averages 10 to 14 business days following CAD sign-off and prototype approval. Freight transit to Austin (including delivery direct to commercial addresses in Austin, Round Rock, or Cedar Park via air priority courier such as DHL Express or FedEx International Priority) typically requires 4 to 6 business days. Combined door-to-door fulfillment cycles generally run under 3 calendar weeks.
What internal bore diameter should we specify for standard 550 paracord beads?
For single-strand Type III 550 paracord passage, an internal bore diameter of 4.5 mm to 5.0 mm is ideal, accounting for nylon weave expansion. For double-strand lanyards (the standard configuration for high-end knife lanyards), we recommend a minimum through-hole of 5.8 mm to 6.2 mm. We apply a 0.5 mm radius chamfer at both bore entrances to eliminate sharp edges that cause cord fraying under repeated twisting loads.
How do you guarantee authentic Grade 5 (Ti-6Al-4V) rather than inferior Grade 2 or commercial scrap?
Every titanium batch processed through our factory originates from certified vacuum-melted ingots. We provide complete Mill Test Certificates (MTC) conforming to EN 10204 Type 3.1, detailing exact chemical mass fractions (Aluminum 5.5–6.75%, Vanadium 3.5–4.5%, Iron ≤ 0.40%, Oxygen ≤ 0.20%, balance Titanium) along with physical tensile yield ratings. Austin customers can independently verify samples via handheld XRF spectrometry or mechanical tensile pull testing.
What surface finishes provide the highest scratch resistance on titanium pocket accessories?
While electrochemical anodizing yields striking colors, thin decorative oxide layers (20 to 100 nm) can wear over time when carried alongside steel keys. For maximum surface longevity in pocket carry, we advise our stone-washed ceramic media tumbled finish, fine micro-bead blasting, or Physical Vapor Deposition (PVD) titanium carbo-nitride (TiCN) and DLC (Diamond-Like Carbon) coatings. These physical vapor layers reach microscopic hardnesses above 2500 HV, resisting abrasion from hardened steel key rings.
Can Velnora machine Timascus (pattern-welded titanium composite) for bespoke runs?
Yes. We routinely machine Timascus (Mokuti) forged composite rods. Because Timascus consists of alternating layers of Grade 2 and Grade 5 titanium, its varying work-hardening properties require tailored feed rates, low spindle speeds, and specialized carbide tooling to prevent delamination. Following multi-axis CNC profiling, we offer precision flame heat-treating or differential voltage anodizing to bring out high-contrast woodgrain and damascus wave patterns.
What customs documentation and Harmonized Tariff Schedule (HTS) codes apply to imports?
Titanium beads, lanyard terminals, and decorative EDC turnings are classified under HTS Code 8108.90.60 (Articles of Titanium, Other) or HTS 8308.90 for decorative clasps and hardware. Precision bolts and standard fasteners ship under HTS 8108.90.30 or 7318.15 depending on specific thread geometry. We provide clear commercial invoices, airway bills, packing lists, and origin declarations to ensure smooth clearance through US Customs at regional ports of entry.
Initiate Your Custom Titanium CNC Production Run
Whether you require a sample evaluation run of 50 custom lanyard beads or continuous high-volume supply for an Austin outdoor lifestyle brand, send us your 2D prints or 3D STEP files. Our engineering staff will review tolerances, evaluate toolpaths, and return a factory-direct quote within 4 hours.
Get a Quote