DIN 912 Micro

Direct manufacturing catalog featuring specialized micro-fasteners, custom EDC beads, laser-etched collector items, and precision vehicular accessories made from aerospace-grade Gr5 (TC4) and pattern-welded Timascus.

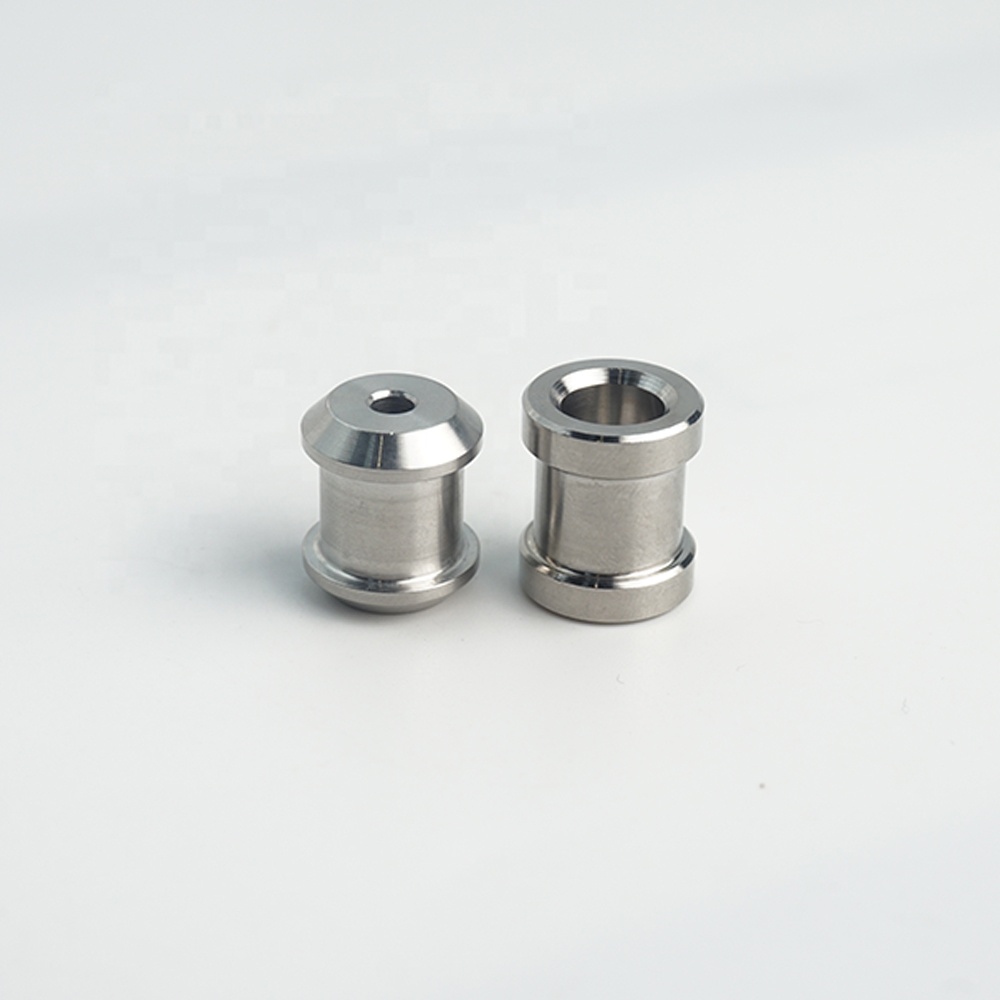
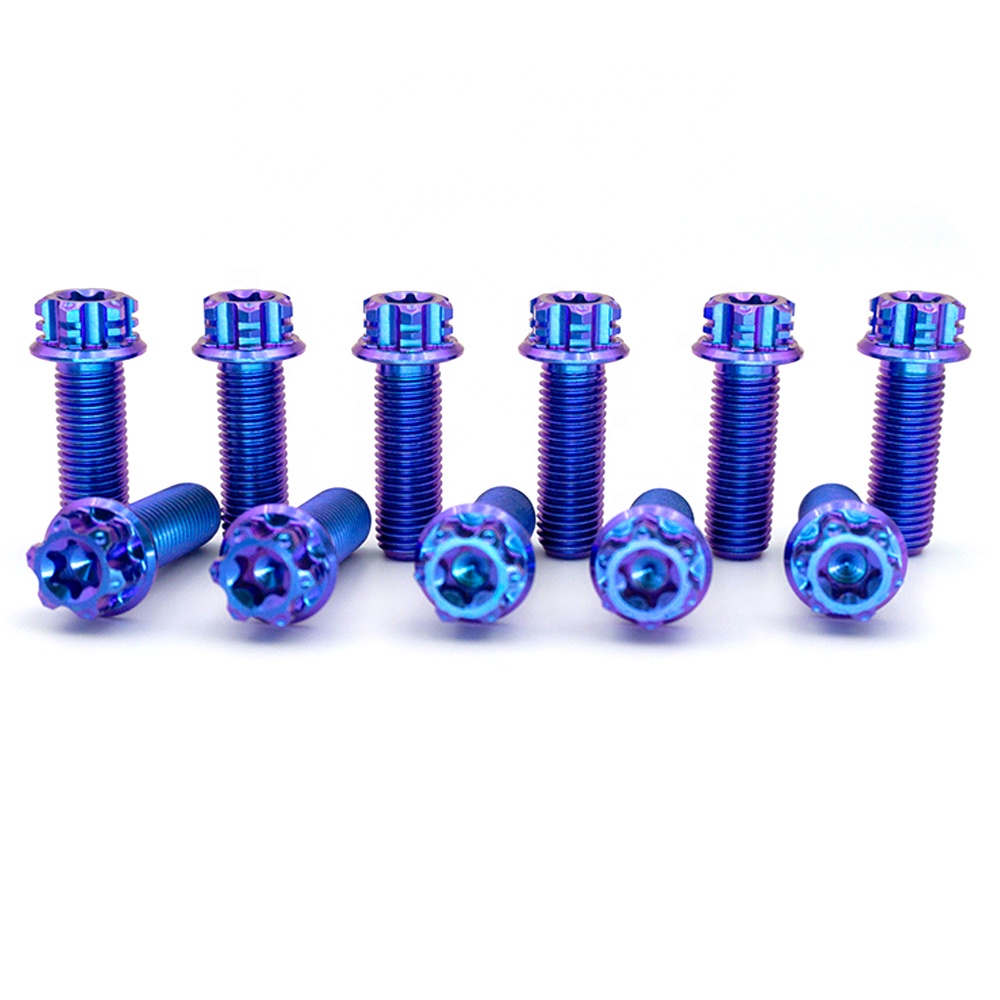
In the high-precision world of bespoke everyday carry (EDC) design, Timascus—frequently referred to by trade designations such as Mokuti or pattern-welded layered titanium—occupies a technical category entirely distinct from standard alloy manufacturing. Where traditional subtractive machining deals with homogenous bar stock such as Grade 2 commercially pure or Grade 5 Ti-6Al-4V, Timascus represents an anisotropic composite of two or more distinct titanium alloys (typically CP Grade 2 and Grade 5, or Grade 5 and 7075-phase reactive alloys) laminated together through high-temperature, high-pressure solid-state diffusion bonding under an inert gas or vacuum chamber environment.
For independent knife-makers, artisanal jewelers, and industrial accessories brands operating in Birmingham's historic Jewellery Quarter and the broader West Midlands manufacturing spine, the sourcing of Timascus EDC beads presents exceptional metallurgical complexities. Unlike standard Damascus steels, which achieve visual contrast through differential acid-etching rates of nickel-bearing ferrite and carbon-bearing pearlite, Timascus exhibits zero chemical etch contrast in ambient media. Instead, its chromatic topography is unlocked entirely through thermal oxidation or electrochemical voltage tuning. Because CP Titanium and Grade 5 Ti-6Al-4V possess fundamentally distinct oxidation kinetics, heating the machined bead to calibrated temperature thresholds (typically between 380°C and 490°C) causes the CP layers to grow an anatase/rutile TiO2 interference film at a radically different rate than the vanadium- and aluminum-doped TC4 layers. The optical outcome is a permanent, high-contrast, hypnotic topographical zebra-pattern spanning electric blues, fiery purples, and incandescent gold highlights.
“True manufacturing excellence in Timascus EDC turnery requires absolute mastery of thermal dissipation. Because titanium possesses an extraordinarily poor thermal conductivity coefficient (approximately 6.7 W/m·K compared to aluminum's 205 W/m·K), micro-turning an intricate lanyard bead or begleri element without inducing inter-laminar shear separation or work-hardening microfractures requires dedicated slow-feed, high-pressure coolant strategies.”
At Velnora Titanium Industry Co., Ltd., based directly inside Baoji—China's internationally acclaimed ‘Titanium Valley’—our production facility leverages 13+ years of raw-material pedigree to supply Birmingham's top designers with stable, non-delaminating Timascus bar stock and finished CNC turnings. By utilizing Wire Electrical Discharge Machining (EDM) in concert with high-precision 5-axis Swiss-type lathes, we ensure that every single contour, 550 paracord chamfer, and internal weight-relief cavity preserves the structural continuity of the weld-lines while preventing thread stripping and cosmetic tearing.
Birmingham and the West Midlands metropolitan area maintain a historic legacy as the primary engine room of British metalcraft, micro-mechanics, and transport engineering. Today, this heritage does not merely survive; it is undergoing an intense modern resurgence driven by advanced materials substitution. The deployment of custom-turned Timascus beads, precision TC4 paracord toggles, and multi-functional titanium fittings manifests across several distinct localized economic micro-clusters:
Independent makers in Hockley and the Jewellery Quarter leverage patterned Timascus beads as central focal elements for custom EDC lanyards, titanium cufflinks, luxury signet inlays, and ultra-high-end watch strap keeper loops catering to discerning London and international collectors.
Specialist sporting knife fabricators across Solihull and the Black Country utilize our CNC-turned TC4 titanium and Timascus beads as counterweight balance points on lanyard terminations, offering zero-corrosion resilience against rain, mud, and harsh outdoor field conditions.
Situated within the UK's ‘Motorsport Valley’ proximity, regional race vehicle and superbike tuners combine decorative Timascus cabin switchgear accents with our high-tensile Gr5 disc rotor fasteners (M8x23) and flanged bolts to slash unsprung rotational mass while enhancing visual prestige.
Whether supplying boutique e-commerce labels on Digbeth's creative corridor or delivering industrial batches to specialist distribution houses near Birmingham Airport (BHX), our production lines provide custom branding, micro-laser serialization, and certified material trace logs directly suited to UK import expectations.
Procurement directors and product developers often evaluate Timascus against legacy materials such as Damascus carbon steel, marine-grade brass, and Cupronickel (Mokume Gane). While traditional copper-bearing Mokume Gane or patterned tool steels offer historical charm, their operational parameters fall drastically short of modern consumer expectations regarding weight, chemical inertness, and hypoallergenic skin compatibility:
| Physical Property | Patterned Timascus (CP+Gr5) | Standard Gr5 (Ti-6Al-4V) | Damascus Carbon Steel | Mokume Gane (Cu/Ni/Brass) |
|---|---|---|---|---|
| Density (g/cm³) | ≈ 4.47 | 4.43 | 7.85 | 8.70 – 8.92 |
| Corrosion Resistance | Immune to sweat, salt, chlorides | Immune to sweat, salt, chlorides | Prone to surface rust; requires oil | Oxidizes, patinas, stains skin |
| Hypoallergenic Safety | 100% Bio-compatible & nickel-free | Exceptional biocompatibility | Moderate; prone to nickel release | Poor; copper/nickel skin reactions |
| Surface Coloring Method | Interference oxide film (Heat / Volt) | Anodic bath (Single hue) | Acid-etch (Ferric chloride bath) | Chemical patination (Liver of sulfur) |
| Tensile Strength (MPa) | 650 – 895 (Layer dependent) | ≥ 895 (Class 8.8+ equivalent) | 600 – 800 | 280 – 380 |
Because Timascus is completely free of elemental iron and copper, it will never leach oxides onto leather sheaths, cordura pockets, or skin. For UK brands shipping globally, this eliminates post-sale tarnishing claims and guarantees life-of-the-product chromatic brilliance.
Analyzing Google Search Intent data, local procurement movements, and consumer purchasing patterns across the United Kingdom highlights four major macro trends that are reshaping how Birmingham businesses source EDC titanium products:
1. Demand for High Information Gain & Visual Verifiability: UK buyers have grown deeply skeptical of anonymous intermediaries and trading companies re-listing generic renderings. High-tier British customers demand live factory machining footage, spectrometer test reports proving Grade 5 titanium purity, and unedited process clips showing Wire EDM slicing of Timascus billets before committing to volume purchases. Velnora addresses this search intent directly by providing comprehensive CNC video records for over 930+ discrete components.
2. The Rise of ‘Pocket Jewelry’ Collectibility: Modern everyday carry is no longer strictly utilitarian. The cross-pollination between luxury mechanical watches, custom bespoke pens, and mechanical keyboard artisans (such as 1U Timascus keycaps and begleri fidget objects) has created an elite lifestyle collectible sector across the UK. Enthusiasts in Birmingham, Manchester, and London treat limited-edition patterned titanium beads as wearable mechanical art.
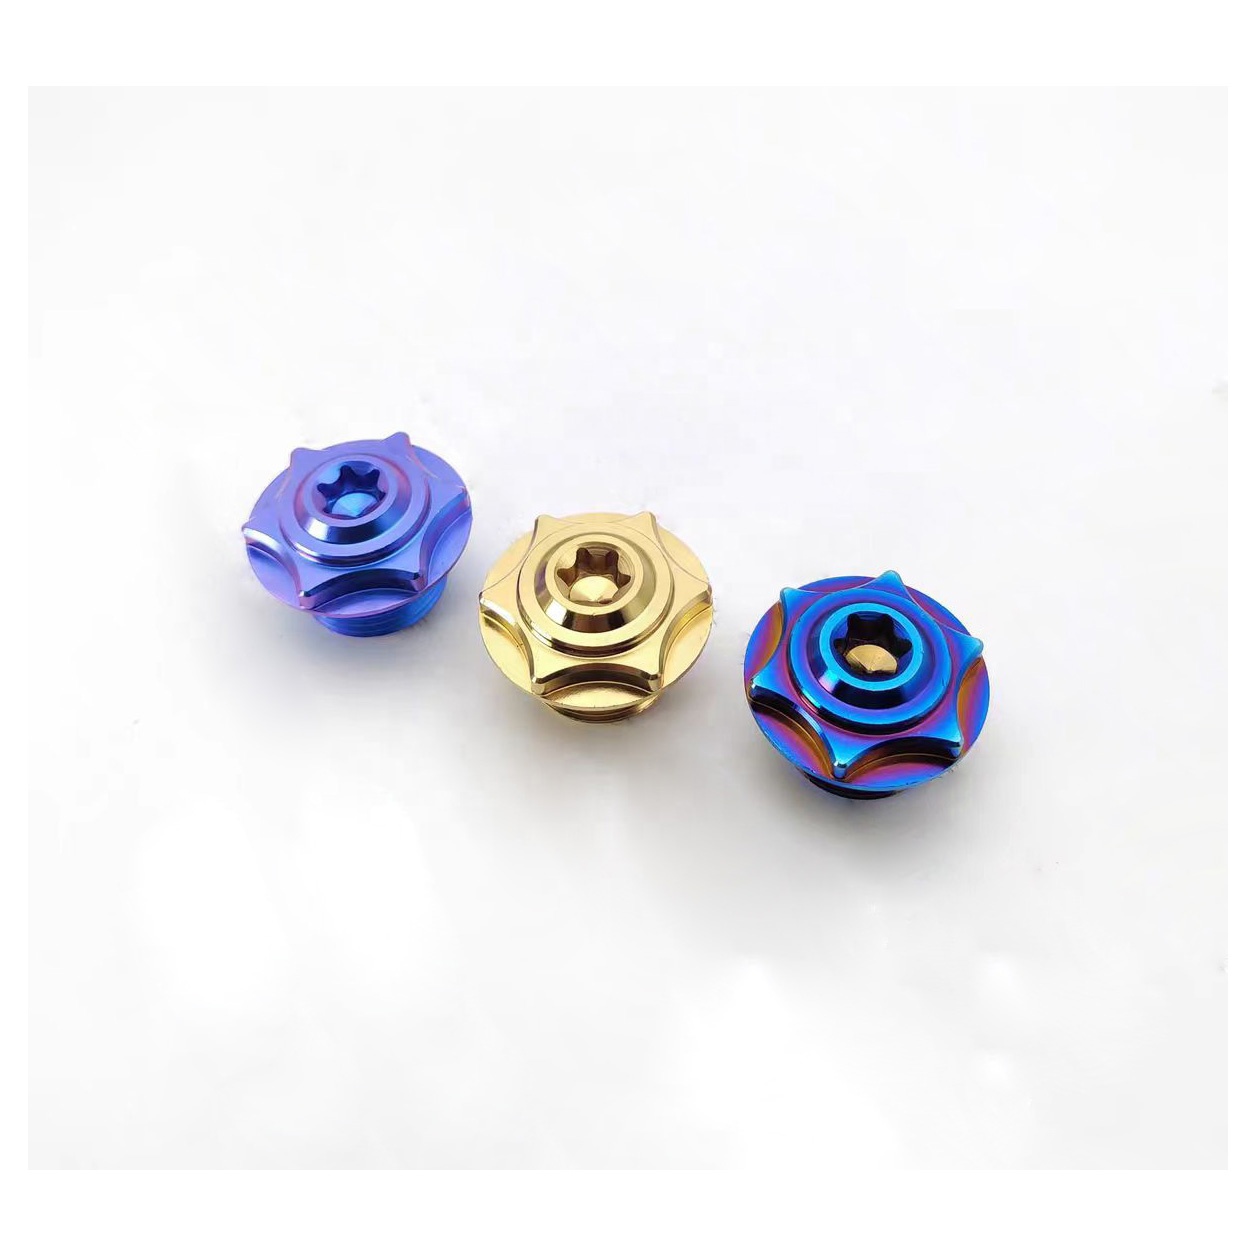
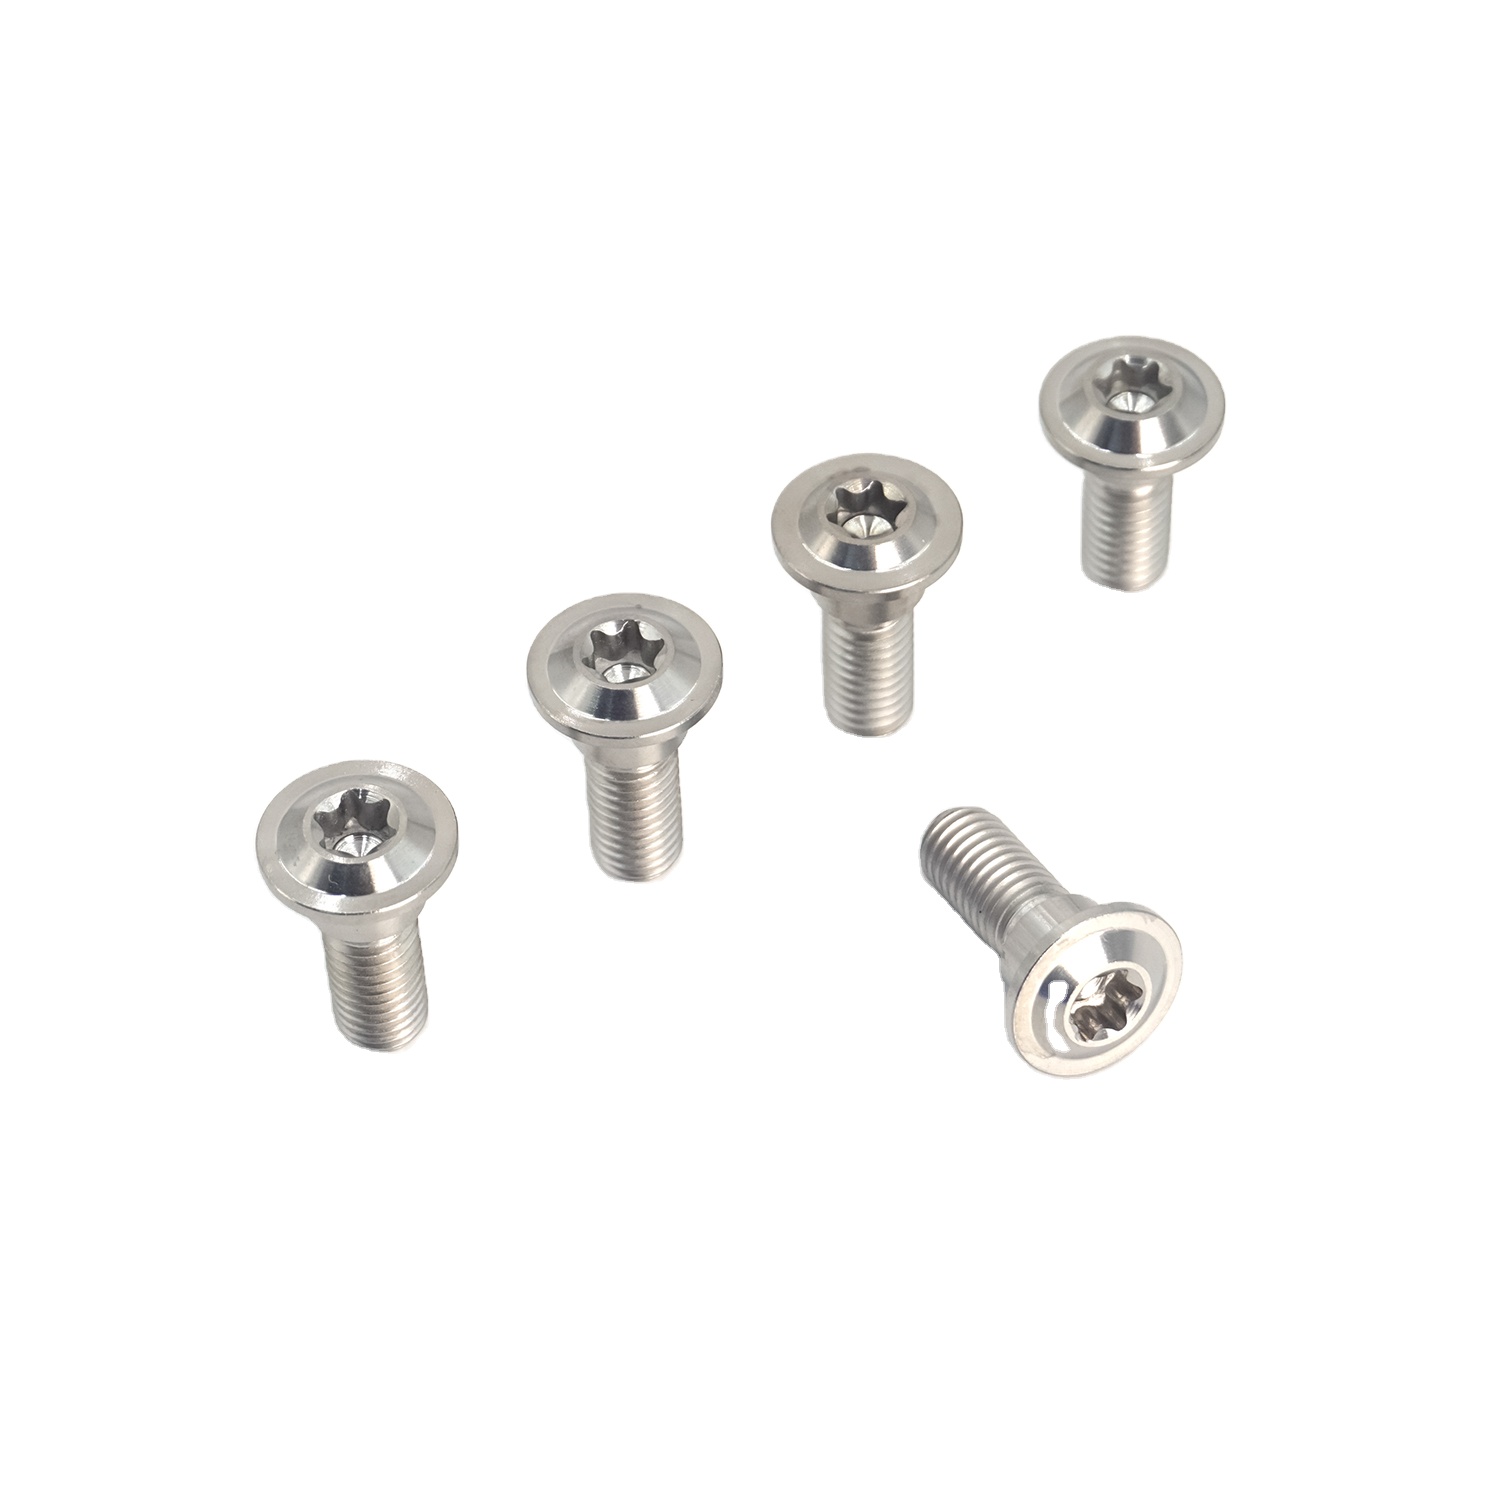
3. Consolidation of Hardware and Fastener Sourcing: Engineering workshops in the West Midlands are streamlining supply chains by combining their decorative bespoke EDC component orders with critical functional hardware—such as M5 bicycle stem bolts, DIN 912 titanium micro-screws for precision knife scales, and M20 oil filler plugs for custom motorcycle modification. Partnering with a comprehensive manufacturer capable of producing both artistic Timascus forgings and DIN-compliant industrial bolts dramatically reduces logistics overhead and import clearance friction.
4. Strict Adherence to Responsible Sourcing & REACH Compliance: British importers face stringent environmental and product safety standards under UK REACH. Sourcing titanium manufactured in compliant Baoji precision facilities guarantees that all coloring processes are free of toxic synthetic dyes, heavy metal baths, and hazardous hexavalent chrome coatings.
Based in the Jinhe Industrial Park of Baoji, Shaanxi, Velnora Titanium Industry Co., Ltd. serves as an indispensable manufacturing partner for British enterprises seeking direct factory pricing without compromising on aerospace tolerances. When procuring from us, Birmingham designers bypass multi-tier markup channels and interface directly with machine operators:
Direct access to sponge titanium smelting hubs guarantees zero-scrap, virgin Ti-6Al-4V bar stock with complete mill test certificates (MTC).
Our workshop combines fast wire-cutting for delicate layered Timascus slabs with multi-axis automated turning centers achieving ±0.005mm accuracy.
Every custom production run is verified with unedited CNC turning and thread gauge video clips sent to the buyer prior to final packing and flight dispatch.
Bespoke Timascus EDC items are available from single-piece prototypes up to 10,000-unit runs for global retail brand launches.
We dispatch all commercial and prototype consignments using express air freight services (DHL Express, FedEx International Priority, or UPS Air) directly into Birmingham Airport (BHX) or East Midlands Airport (EMA). Small to medium batch consignments typically arrive within 4 to 7 business days from factory gate to your workshop door in Birmingham. All shipments are accompanied by certified commercial invoices, packing lists, and correct HS tariff classifications (typically 8108.90 for finished titanium articles) to ensure seamless UK customs clearance without tariff delay.
Standard titanium anodizing relies on submerged electrolyte immersion using adjustable DC voltages to uniformly grow a transparent oxide layer that refracts light into a single consistent color across the entire part. In contrast, Timascus consists of alternating layers of Grade 2 and Grade 5 titanium. While voltage anodizing can be used, high-precision open-flame torching or kiln heat-treating yields far more dramatic and vivid contrast. Because CP Titanium and TC4 possess distinct oxidation kinetics and activation energies, heat treatment creates breathtaking multi-color gradient shifts across adjacent layers simultaneously, yielding the signature pattern that cannot be replicated on homogenous metals.
We provide both finished components and raw material stock. For independent makers equipped with their own grinding, turning, and milling equipment in the Jewellery Quarter, we supply raw Timascus (Mokuti) round rods (typically 10mm to 35mm diameter) and flat plates (1.5mm to 10mm thickness) sliced via precision Wire EDM to prevent micro-fracturing along the diffusion bond boundary. Alternatively, for brands seeking a turnkey solution, we execute complete CNC contouring, 550 lanyard bore chamfering, internal hollowing, and hand-torched finishing according to your proprietary STEP/IGES CAD drawings.
Our standard production baseline for tactical EDC beads and begleri elements features an internal central bore diameter of 5.5mm to 6.0mm with radiused entry and exit chamfers. This dimension is specifically calibrated to permit a doubled strand of standard Type III 550 paracord (approx. 4mm nominal uncompressed diameter) to pass smoothly without snagging or sheath fraying. However, because all parts are turned on multi-axis CNC machines, bore diameters can be configured to any specification—from micro 3.0mm holes for micro-cord up to stepped counterbored cavities designed to conceal lanyard termination knots.
For custom CNC machined Timascus beads and specialized EDC accessories, our MOQ begins at just 1 to 10 pieces for stock patterns, making it highly feasible for bespoke artisans to sample without inventory exposure. For full OEM production runs of custom proprietary designs, typical MOQs range from 50 to 100 pieces. Production lead time for standard prototypes is generally 7 to 10 working days, with volume orders completed in 15 to 25 working days depending on surface finishing and engraving complexity.
Submit your 2D/3D design files (STEP, IGES, PDF) or select from our verified catalog of Timascus EDC beads, micro-screws, and high-tensile Gr5 racing hardware. Our technical machining team provides formal DFM reviews and pricing quotations within 4 business hours.