Cycling Upgrade
Manufactured from aerospace-certified Ti-6Al-4V bar stock under ISO 9001 quality controls. Review our top OEM components calibrated for precision mechanical assemblies.

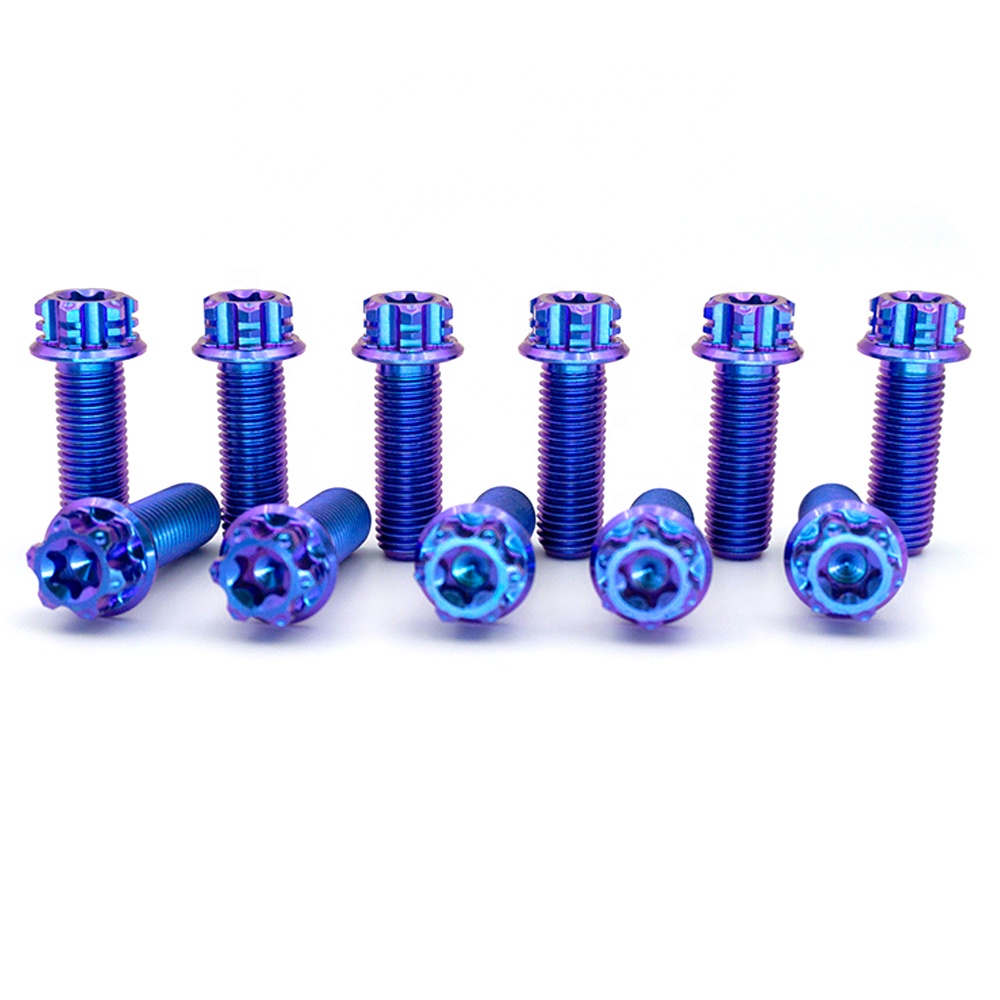
Fastener back-out caused by transverse harmonic vibration remains the leading source of non-ductile mechanical failure in naval structures, subsea flowline assemblies, and high-rpm rotating machinery. For procurement directors, lead naval architects, and mechanical systems designers operating across Glasgow and the wider Strathclyde industrial belt, standard stainless steel lock nuts (such as A2-70 or A4-80) frequently fall short when exposed to the dual threat of severe cyclic fatigue and continuous electrolytic chloride exposure. Velnora Titanium Industry Co., Ltd. engineers precision OEM/ODM Grade 5 (Ti-6Al-4V) self-locking hex nuts designed to solve these high-stress fastener dynamics.
Unlike standard commercial nuts, prevailing-torque titanium lock nuts function by integrating a continuous mechanical resistance that persists independently of seating torque. In all-metal configurations (conforming to DIN 6927, DIN 980v, or ISO 7040), locking torque is generated through precision elastically deformed top threads or a three-point crimped collar. When engaged by a mating titanium male thread, these displaced thread profiles produce a continuous radial clamp load against the bolt flanks, converting potential vibrational back-off kinetic energy into localized elastic hoop stress. For non-metallic locking solutions, our DIN 985 series features an elastomeric, non-hygroscopic virgin nylon ring engineered to resist thread unwinding up to 121°C without scoring mating thread surfaces.
Manufactured to rigid ISO 2320 standards, maintaining controlled break-away and prevailing-off torque cycles across multiple retorquing sequences without stripout or pitch deformation.
Boasts a stable, self-regenerating TiO2 passivation film, delivering PREN values over 40 for zero pitting corrosion in Firth of Clyde saline splashes, brackish tidal estuaries, and deep subsea manifolds.
CNC tapped with specialized micro-ground geometries and coated with anti-friction molybdenum disulfide (MoS2), specialized PVD, or physical dry-film lubricants to eliminate cold-welding tendencies.
When specifying critical fasteners for Clyde naval contracts, offshore wind jacket substructures, or high-performance automotive chassis in Strathclyde, evaluating yield strength relative to structural mass is essential. The table below outlines empirical properties comparing our Velnora Ti-6Al-4V Grade 5 self-locking hex nuts against common high-alloy steels and aluminum benchmarks:
| Mechanical / Physical Property | Velnora Gr5 Ti-6Al-4V (TC4) | Marine 316L (A4-80) Steel | Super Duplex 2507 (UNS S32750) | Inconel 718 (Nickel Superalloy) |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 (Ultralight) | 8.00 | 7.80 | 8.19 |
| Yield Strength Rp0.2 (MPa) | ≥ 828 | ≥ 450 | ≥ 550 | ≥ 1,034 |
| Ultimate Tensile Strength Rm (MPa) | 895 – 1,050 | 700 – 800 | 750 – 1,000 | 1,240 – 1,400 |
| Specific Strength Ratio (Strength/Density) | 202 kNm/kg (Superior) | 100 kNm/kg | 128 kNm/kg | 151 kNm/kg |
| Chloride Pitting Resistance (PREN) | Immune (> 42 equivalent) | 23 – 25 (Pitting Vulnerable) | ≥ 42 (Excellent) | Immune |
| Magnetic Permeability (μ) | 1.00005 (Virtually Non-Magnetic) | ∼ 1.02 | ∼ 1.05 | 1.001 |
| Thermal Shock & Cryogenic Ductility | -196°C to +400°C | -196°C to +300°C | -50°C to +250°C | -250°C to +650°C |
*Note: While Inconel 718 offers higher absolute yield strength, its 8.19 g/cm³ density imposes an 85% mass penalty compared to Grade 5 titanium. For naval topside mass reduction, motorsport unsprung weight trimming, and offshore nacelle crane installations, Grade 5 titanium delivers unmatched strength-to-weight optimization.
From Govan and Scotstoun naval dockyards to East Kilbride engineering parks and offshore wind testbeds off the Scottish coast, our titanium self-locking nuts solve mission-critical assembly challenges.
Installed on sonar arrays, de-gaussing equipment, exhaust silencers, and topside radar masts along the River Clyde. Low magnetic signature eliminates mine-trigger risks while standing up to open Atlantic saltwater spray.
Spec: DIN 6927 All-Metal Flange Lock Nuts (M6–M20)Specified for subsea tidal array moorings, turbine blade sensor housings, and splash-zone access ladders in the Firth of Clyde and North Sea developments where service costs demand zero crevice corrosion across 25-year design lifespans.
Spec: DIN 985 Heavy Hex Nylon Insert Nuts (M10–M36)Supporting clean energy test initiatives across central Scotland. Grade 5 titanium maintains extraordinary ductility without low-temperature embrittlement down to liquid hydrogen and LNG regimes (-196°C to -253°C).
Spec: ISO 7042 High-Strength All-Metal prevailing (M8–M24)Supplied to specialized Scottish motorsport fabrication shops and aerospace sub-tier suppliers in Renfrewshire. Eliminates critical unsprung weight on suspension links, brake caliper brackets, and turbo manifolds.
Spec: M6–M12 12-Point Aircraft Nuts & Serrated HexScotland's aggressive transition toward Net Zero 2045, alongside substantial multi-decade capital programs in naval frigate construction on the Clyde, has radically reshaped procurement benchmarks for structural hardware. Procurement managers across the Glasgow City Region, South Lanarkshire, and West Dunbartonshire are moving away from short-term fastener replacements toward whole-life cycle cost optimization.
Key supply trends currently reshaping the Scottish titanium hardware market include:
Headquartered in Baoji, Shaanxi, our ISO-certified facilities bring over 13 years of precision metallurgical manufacturing to Scottish distributors and OEM engineering firms.
Direct access to premium vacuum-arc remelted (VAR) Ti-6Al-4V Grade 5 sponge and bar stock, ensuring ultra-low interstitial gas control.
Equipped with high-precision Swiss-type turning centers, multi-axis milling, and Sodick wire EDM capable of repeatable ±0.005mm tolerances.
Rolled thread profiles preserve unbroken metal grain flow along root contours, increasing joint dynamic fatigue endurance by up to 300% over cut threads.
We provide HD process videos and dimensional gauge verification for your exact batch before shipment, ensuring complete transparency before dispatch.
Daily express couriers (DHL/FedEx) reaching Glasgow Prestwick and Glasgow International in 4–6 days, plus sea freight to Grangemouth/Greenock.
Direct engineering answers addressing thread galling, international maritime standards, UK customs, and mechanical integration.
Titanium threads possess an affinity for friction-induced cold welding. We prevent galling by maintaining precise surface finishes (Ra < 0.4 μm) through precision thread rolling and offering factory-applied dry-film lubricants, MoS2, or micro-thin PVD titanium carbonitride coatings. We also guide your assembly team on adjusted torque values using titanium-compatible nickel-free anti-seize paste.
Grade 5 (Ti-6Al-4V) has a tensile yield strength of roughly 828–895 MPa, directly comparable to metric Property Class 8.8 structural steel while being 44% lighter. For Class 10.9 or 12.9 joints in extreme safety-critical applications, a one-to-one dimensional swap is not recommended without increasing thread nominal diameter or recalculating clamp load safety margins with our engineering desk.
Every shipment is accompanied by an authentic Mill Test Certificate to EN 10204 Type 3.1 detailing chemical composition (spectrographic analysis) and tensile/yield/elongation physical properties. Full dimensional inspection reports (CMM), coating thickness certificates, and Certificates of Conformity (CoC) to DIN/ISO/JIS specifications are standard inclusion.
We routinely supply UK commercial clients under DDP (Delivered Duty Paid) or DAP terms. For established engineering companies with a valid UK EORI number, shipments clear HM Revenue & Customs (HMRC) seamlessly through air freight terminals at Glasgow (GLA), Edinburgh (EDI), or sea freight channels with all customs documentation prepared in advance.
For temperatures between -40°C and +121°C, DIN 985 nylon-insert lock nuts provide excellent reusability and vibration dampening. For marine exhaust headers, subsea high-temperature pipelines, or aerospace assemblies operating from 150°C up to 400°C, our DIN 6927 all-metal prevailing torque or 12-point jet nuts are required, as they rely entirely on metallic thread displacement.
For catalog sizes (DIN 985/DIN 6927 from M3 to M24), standard MOQs start at just 100 to 200 pieces per specification. Custom CNC drawings, bespoke pitch threads, or special flange configurations typically require 300 pieces. Prototype sample runs can be produced within 5–7 working days, followed by air dispatch directly to Scotland.
Connect directly with Velnora's Baoji machining engineers. Send your CAD drawings (STEP, IGES, PDF), DIN/ISO hardware specifications, or target order volumes. We provide comprehensive DDP Glasgow cost modeling and technical feedback within 4 business hours.