Featured CNC Titanium Hardware & Specialized Fasteners
Precision-machined fasteners from certified Baoji titanium bar stock, manufactured to stringent ISO 9001 and motorsport specifications for the Nordic racing sector.



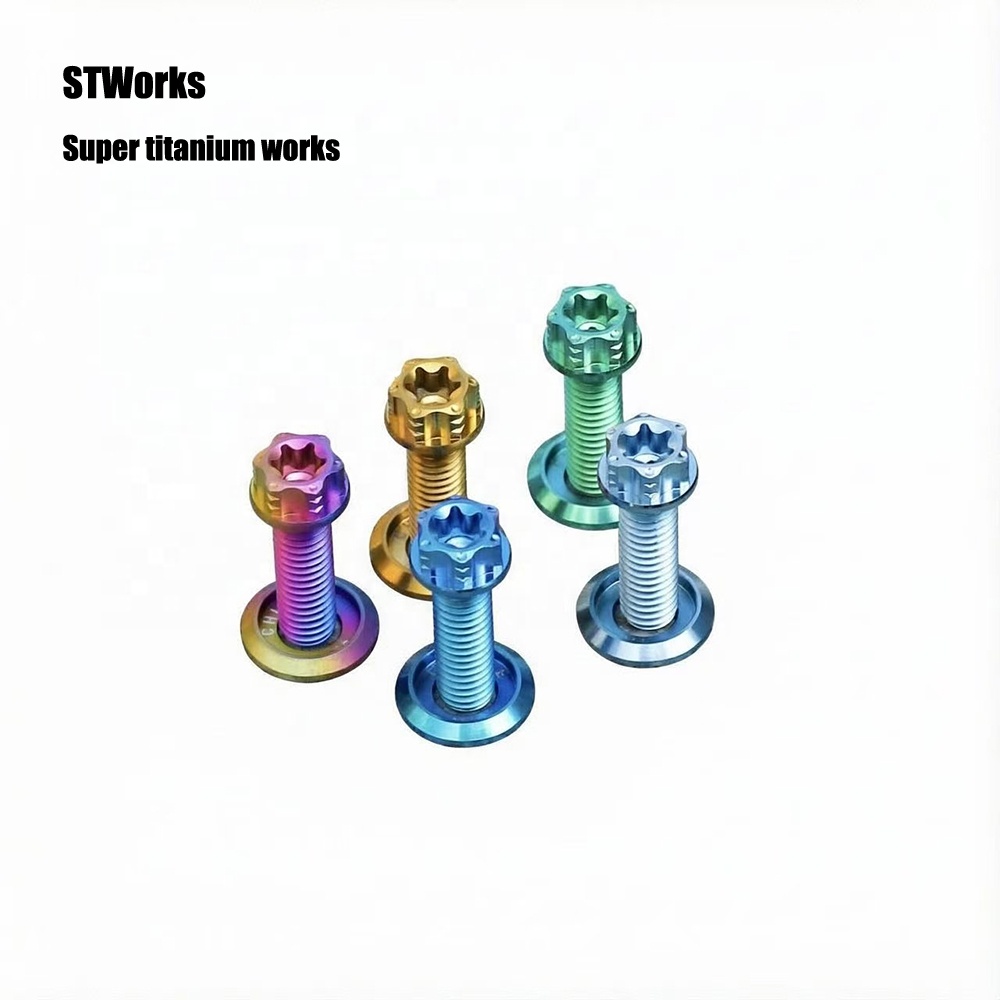
Industry White Paper: Kinematic Load Performance & Material Superiority
In high-displacement superbikes, rally raid builds, and custom performance streetfighters operating throughout the Espoo and Uusimaa regional motorcycle markets, the motorcycle rear axle assembly represents one of the most mechanically demanding structural points. The rear wheel nut must absorb sustained high-load axial clamping forces, withstand cyclic rotational oscillation, and endure dynamic shear shock loads induced by quick-shifting, hard acceleration, and regenerative engine braking.
Standard automotive and motorcycle original equipment manufacturers frequently utilize zinc-plated property class 8.8 or 10.9 structural steel hardware. While structurally adequate under static testing, these steel fasteners impose critical limitations on racing machines: an unnecessarily high rotational and unsprung mass penalty, as well as an extreme vulnerability to chloride stress corrosion when exposed to aggressive road de-icing agents utilized in southern Finland. Velnora Titanium bridges this gap through cold-formed and precision CNC multi-axis milled Ti-6Al-4V Grade 5 (TC4) motorcycle rear wheel nuts, engineered specifically to DIN, ISO metric, and bespoke OEM motorsport blueprints.
Localized Application Scenarios in the Espoo & Greater Finnish Ecosystem
How extreme sub-Arctic conditions, coastal Baltic salinity, and intense track demand dictate high-tensile Grade 5 titanium fastener deployment.
All-Weather Commuting & Winter Riding
Espoo's coastal climate presents severe challenges with sub-zero road salting and coastal humidity along the Gulf of Finland. Titanium's self-passivating TiO2 oxide layer prevents galvanic seizure and crevice corrosion, eliminating seized axle threads after winter storage.
Nordic Track Days & Circuit Racing
At regional racing facilities like Alastaro and KymiRing, reducing unsprung rotational mass on the rear swingarm assembly directly improves rear suspension response over curbs, quickens turn-in transitions, and stabilizes high-speed chain tension stability.
Custom Streetfighters & Heritage Builds
Espoo's vibrant custom motorcycle community demands both mechanical durability and aesthetic refinement. Our proprietary multi-stage vacuum PVD coating and micro-arc anodization deliver deep burnt-titanium, gold, and stealth-black finishes that resist gravel impact.
Technical Clamping Property Matrix: Titanium vs. Conventional Alloys
Comparative structural assessment illustrating why Grade 5 titanium represents the premier upgrade path for high-performance rear axle assemblies.
| Mechanical / Chemical Metric | Velnora Gr5 Ti-6Al-4V | OEM Class 8.8 Carbon Steel | AISI 316 Stainless Steel | 7075-T6 Billet Aluminum |
|---|---|---|---|---|
| Density (ρ) | 4.43 g/cm³ (-44% mass) | 7.85 g/cm³ | 8.00 g/cm³ | 2.81 g/cm³ |
| Tensile Strength (σb) | ≥ 950 - 1050 MPa | 800 MPa | 580 - 620 MPa | 572 MPa (Unsafe for Axle Nut) |
| Yield Strength (σ0.2) | ≥ 880 - 920 MPa | 640 MPa | 290 MPa | 504 MPa |
| Sub-Zero Impact Ductility (-40°C) | Retains >92% Charpy impact | Severe ductile-to-brittle transition | Moderate ductility | Prone to micro-cracking |
| Chloride / De-Icing Resilience | Immune (Noble passivity) | Rapid surface rust & galling | Pitting / Crevice sensitivity | Anodic oxidation breakdown |
Localized Market Growth Trends in Espoo & Northern Europe
The Finnish motorcycle sector, anchored by tech-forward enthusiasts and mechanical workshops across the Greater Helsinki-Espoo metropolitan belt, has transitioned away from generic mass-market replacement hardware toward high-integrity engineered components. Three decisive market dynamics are reshaping supplier selection for local dealerships, race teams, and independent tuning workshops:
- Accelerated Fleet Electrification & High-Torque Power Delivery: High-performance electric dual-sport motorcycles and superbikes deliver instantaneous torque to the rear hub. This requires rear wheel nuts with rolled threads and tight pitch tolerances (Class 6H/4h) to avoid micro-slippage under shock loads.
- Bespoke Customization & Low-Batch Flexibility: Espoo builders prioritize boutique, race-spec finishes with custom laser engravings, wire-EDM weight-reduction pockets, and specific lock-wire drill points conforming to FIM/SML Nordic racing regulations.
- Supply Chain Near-Shoring & On-Demand Precision: Rather than stocking thousands of redundant standard fasteners, regional distribution centers demand specialized OEM/ODM partnerships offering low minimum order quantities (MOQ from 50-100 units), full material test reports (MTR EN 10204 3.1), and real-time CNC verification.
Baoji Manufacturing Prowess: Tailored for Espoo Importers
Leveraging deep industrial positioning in China's Titanium Valley with strict global quality governance since 2013.
Aerospace-Grade Certified Ingots
We source raw titanium exclusively from certified sponge titanium suppliers. Each production heat number is accompanied by full 3.1 mill test certifications ensuring zero internal voids, porosity, or chemical segregation.
Precision CNC Turning & Thread Rolling
Unlike cheaper cut-thread fasteners that introduce fatigue notches, our rear axle threads are precision cold-rolled or CNC profile-turned with uniform root radii to increase thread fatigue limits by upwards of 35%.
Digital Factory Transparency
We solve cross-border procurement doubts through our digital production tracking. Overseas buyers receive high-definition video walkthroughs and optical comparator dimension inspections prior to dispatch.
Frequently Asked Questions for Nordic & Finnish Buyers
Technical guidance addressing import logistics, torque specifications, galling prevention, and bespoke OEM parameters.
How do we prevent thread galling when installing titanium rear wheel nuts on steel or titanium axles?
Titanium alloys have a natural tendency to gall when torqued dry against similar metals or bare steel. For Espoo mechanics and riders, we strongly recommend coating threads with a specialized anti-seize paste containing copper, molybdenum disulfide, or nickel. Furthermore, we apply precision micro-polishing and optional low-friction PVD coatings to lower the frictional coefficient.
What tightening torque value should be applied compared to the original factory service manual?
Because Grade 5 titanium possesses a lower modulus of elasticity (approx. 114 GPa vs. 210 GPa for steel) and when using anti-seize compound, tightening torque should generally be adjusted to approximately 80% to 85% of OEM dry steel specification to achieve identical clamping preload without overstressing thread roots. Specific torque charts are supplied with each OEM batch.
Can Velnora fabricate custom lock-pin or castellated nuts according to our 3D CAD files?
Yes. Our in-house engineering team works directly with STEP, IGES, DXF, or PDF engineering drawings. We frequently manufacture self-locking nylon insert styles (DIN 985 equivalents), safety-wire drilled flanged hex nuts, and bi-hex 12-point designs engineered for quick-change endurance racing hubs.
What are the typical shipping lead times and customs handling arrangements for deliveries to Espoo, Finland?
Sample orders and rapid batch runs ship via air express (DHL/FedEx/UPS) with a transit window of 4 to 7 business days directly to your workshop or distribution center in Espoo. We provide all required commercial documentation, HS codes (731815 / 810890), and origin declarations for smooth Finnish customs clearance through Tulli.
Accelerate Your Performance Hardware Portfolio in Espoo
Consult with our engineering team for rapid drawing reviews, torque calculations, and tailored wholesale quotes. Experience true aerospace precision delivered directly from Baoji's Titanium Valley to the Finnish motorsport community.