Engineered Fastening Systems: Product Catalog
Precision-machined structural hardware optimized for dynamic shear, unsprung mass reduction, and zero-corrosion longevity under demanding North Sea conditions.


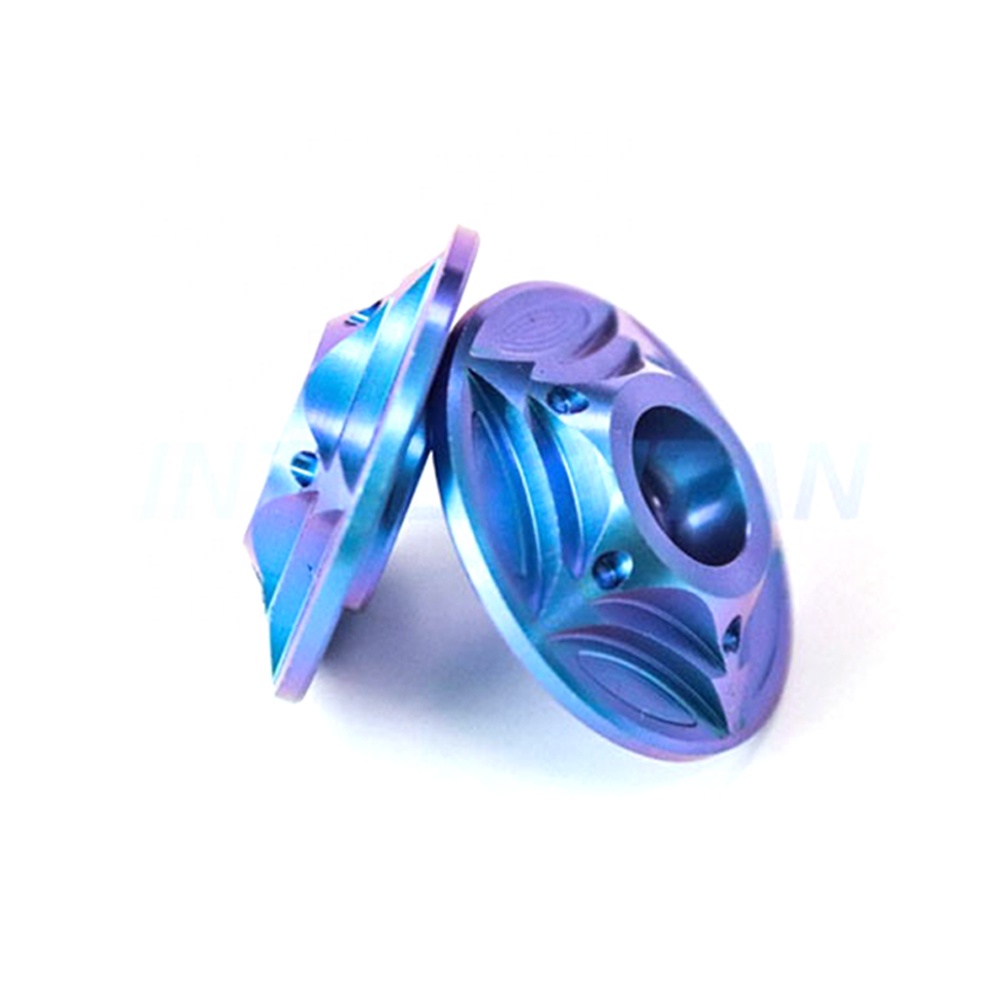

The Metallurgical Imperative: Rear Axle Retention in Coastal Scandinavia
In high-torque superbike, dual-sport enduro, and bespoke custom motorcycle platforms, the rear wheel axle nut serves as the principal load-bearing anchor across the swingarm and drive system. It sustains tremendous axial pretension, intense cyclic dynamic stress during rapid acceleration or trail braking, and significant torsional shear. For motorsport operators and distributors throughout Rogaland, Norway, and specifically the maritime port region of Stavanger, these mechanical challenges are compounded exponentially by atmospheric salinity and ambient humidity.
Conventional chrome-molybdenum or zinc-plated Grade 8.8 and 10.9 structural steel fasteners present inherent chemical liabilities in coastal Nordic climates. Marine-driven aerosolized chlorides infiltrate thread gaps, accelerating electrolytic oxidation and stress corrosion cracking (SCC). Concurrently, common aftermarket aluminum 7075-T6 fasteners suffer premature thread stripping, plastic deformation under standard torque ratings (often ranging from 90 Nm to 145 Nm for M18 through M25 axle spindles), and severe structural degradation above 120°C heat propagation generated by race-spec disc rotors.
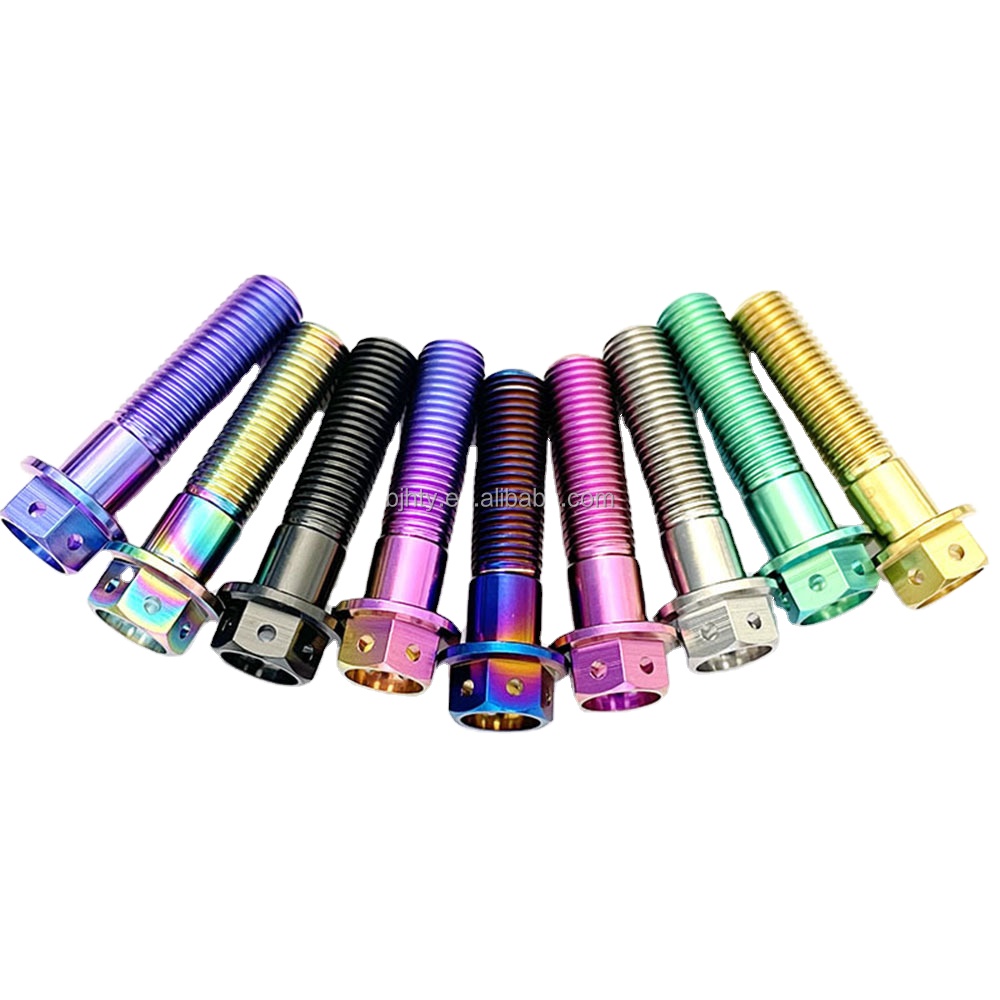
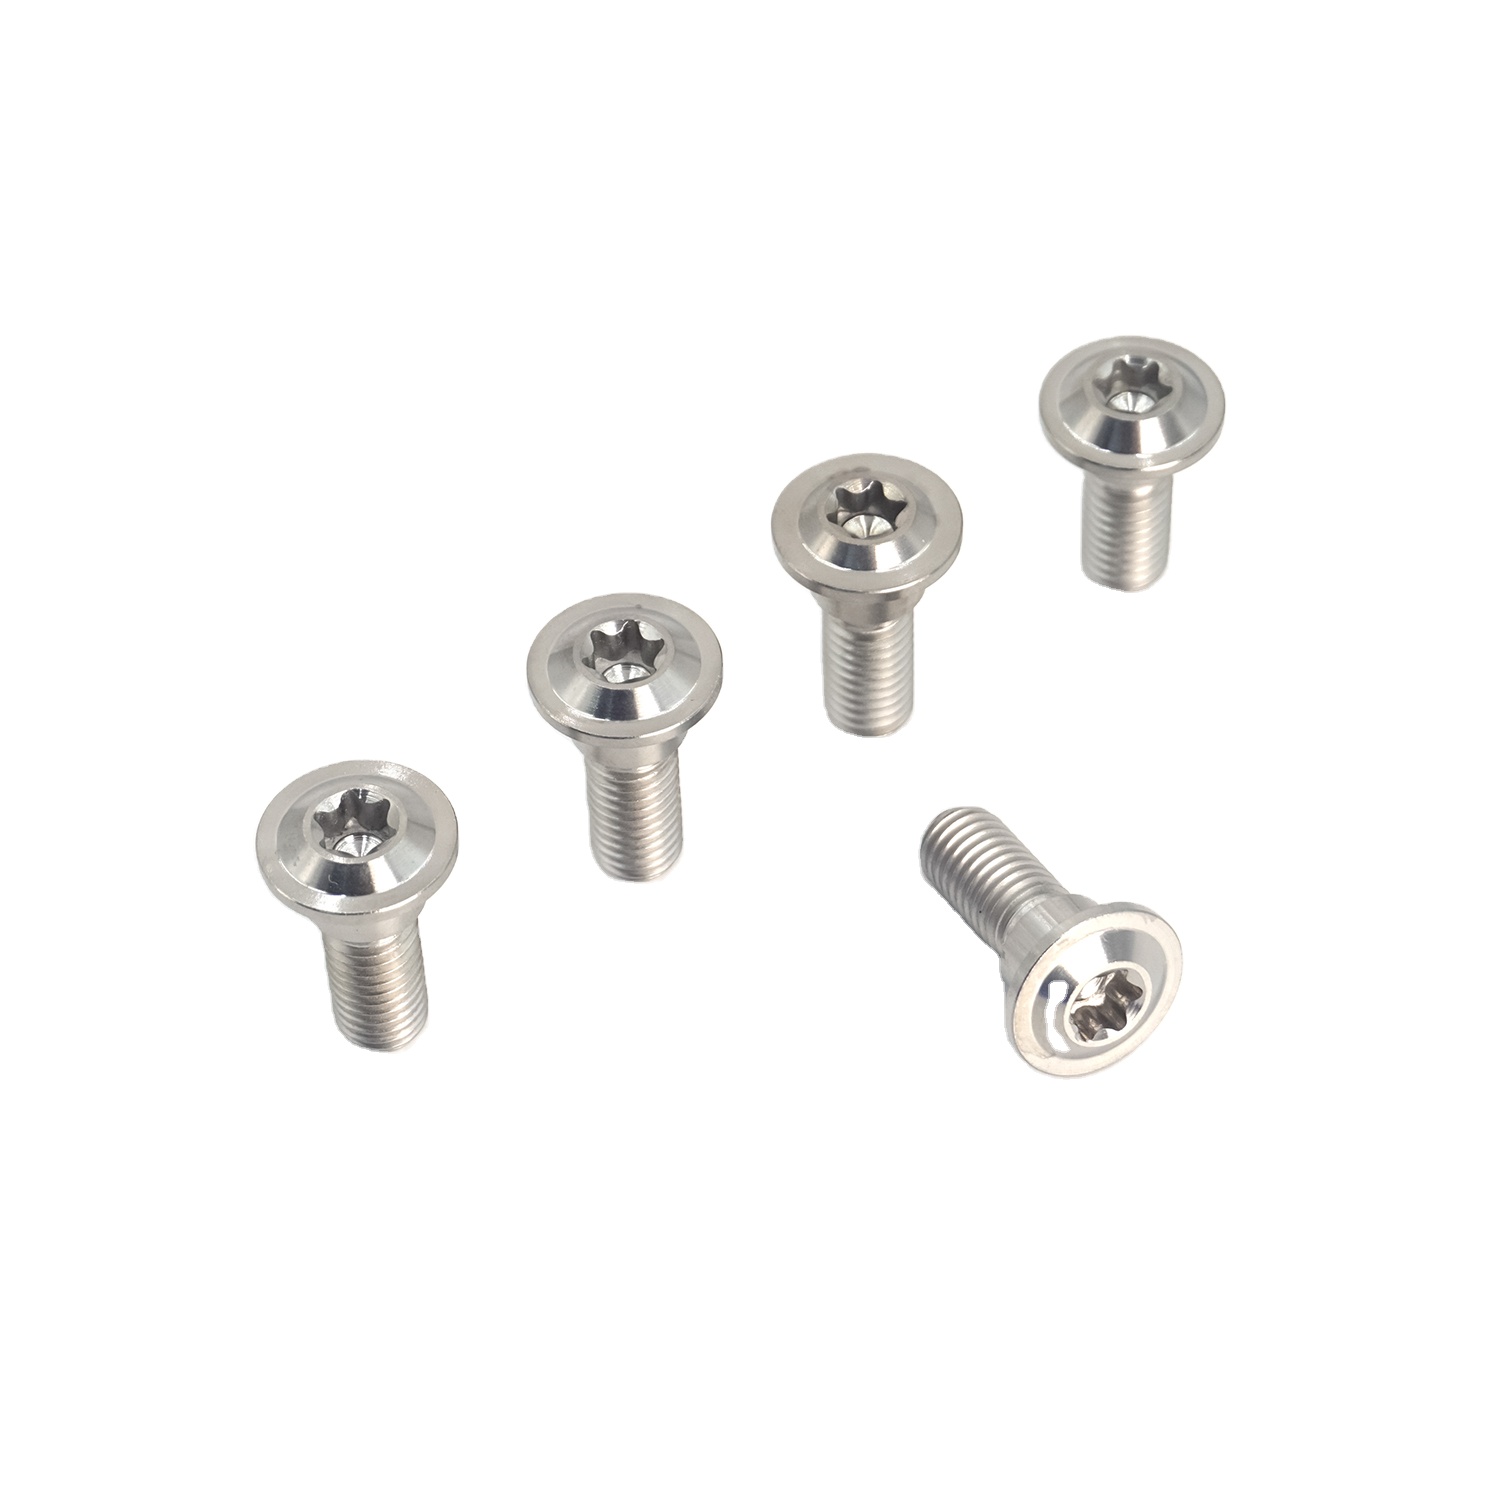
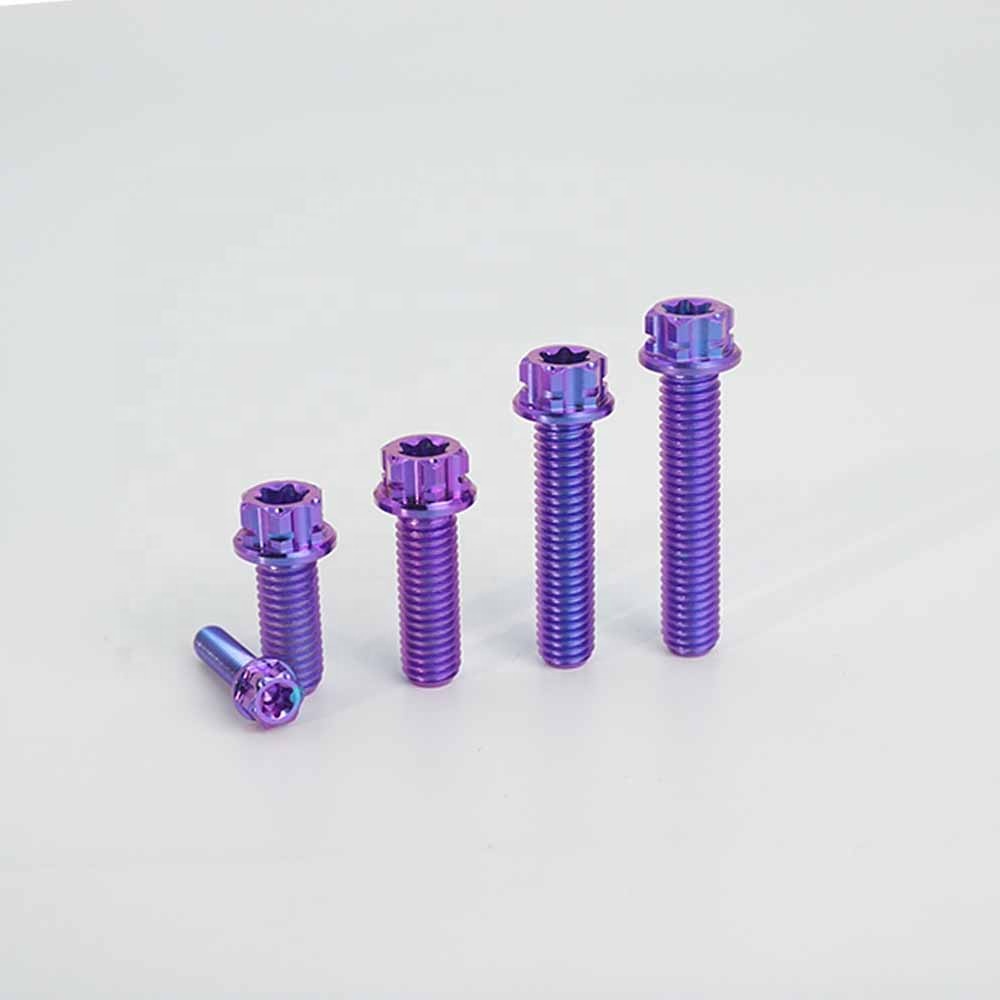
Velnora Titanium Industry addresses this engineering bottleneck by executing high-precision OEM/ODM production of Grade 5 Titanium (Ti-6Al-4V, TC4) rear wheel nuts. Sourced through the industrial heart of Baoji—China's Titanium Valley—and produced under rigid ISO and DIN manufacturing methodologies, our rear wheel nuts integrate rolled threads, CNC flanged surfaces with integrated friction reliefs, and an immunity to electrochemical chloride attack. This delivers racing teams, specialty motorcycle workshops, and component distributors across Western Norway an uncompromising balance of mechanical reliability, weight shedding, and perpetual surface integrity.
Local Application Scenarios: Stavanger's Motorsport & Maritime Engineering Landscape
Stavanger holds an elite global standing as Norway's energy capital and a thriving hub for advanced precision manufacturing, offshore subsea engineering, and high-performance motorsports. Local technical end-users maintain distinct operating envelopes where titanium fasteners transition from an aesthetic indulgence to a vital functional standard:
Fjord & Coastal Road Enduro
Navigating coastal passages along Rogaland (e.g., the North Sea Cycle and Motorcycle route) exposes drive assemblies to continuous ocean spray, fluctuating road de-icing salts, and rain. Gr5 rear axle nuts resist all galvanic corrosion without degrading or seizing into aluminum swingarm adjusters.
Unsprung Mass Race Engineering
At local racing venues such as Motorcenter Norway in Sokndal, race teams exploit our CAD-optimized, lightened flanged rear nuts. Cutting 44% of mass right at the wheel axle reduces unsprung gyroscopic inertia, drastically improving high-speed swingarm dampening and chassis turn-in.
Offshore Cross-Over Standards
Technicians in Stavanger expect fasteners matching offshore marine reliability. Our Ti-6Al-4V fasteners meet standard DIN/ANSI/JIS geometric tolerances while providing Norsok-level chemical resilience against atmospheric salt fogging and cyclic cold snaps.
Comprehensive Engineering Property Comparison
Selecting rear axle retention hardware demands rigorous data evaluation. The following matrix illustrates the performance advantages of Grade 5 Ti-6Al-4V compared to common industry alternatives:
| Material Specification | Yield Strength (MPa) | Tensile Strength (MPa) | Density (g/cm³) | Marine Salt Fog Resistance | Fatigue & Galling Index |
|---|---|---|---|---|---|
| Gr5 Ti-6Al-4V (Velnora Spec) | 825 – 880 | 895 – 1000 | 4.43 | Immune (Passivating TiO2) | Superior (CNC Rolled Threads) |
| Class 8.8 Structural Steel | 640 | 800 | 7.85 | Poor (Accelerated Galvanic Rust) | Standard (Vulnerable to Pre-Load Loss) |
| Class 10.9 Heat-Treated Alloy Steel | 940 | 1040 | 7.85 | Moderate (Requires Zinc/Nickel Dip) | Good (High Deadweight Penalty) |
| 7075-T6 Billet Aluminum | 480 | 540 | 2.81 | Fair (Anodic Pitting Susceptible) | Poor (High Shear Risk at >110 Nm) |
*Note: When installing titanium rear axle nuts against aluminum swingarms, anti-seize paste (containing nickel or copper base) or dry-film MoS2 lubricant must be applied to prevent cold welding and galling under high torque clamp loads.
Industrial & Procurement Trends Shaping Stavanger
Motorcycle fleet distribution and performance retail in Norway are shifting toward sustainable capital expenditure and premium lightweight components. Distributors and performance workshops across Stavanger and the broader Nordic region are prioritizing the following strategic pivots:
1. Shift Toward Total Lifecycle Fasteners: In a market governed by high labor rates for mechanical overhaul, workshop owners actively eliminate component failure modes. Steel axle nuts require frequent zinc re-plating or replacement due to salt-induced thread deterioration during harsh Scandinavian winters. Titanium fasteners present an infinite corrosion lifecycle, drastically lowering maintenance cycles for commercial fleet rentals and demanding private riders.
2. E-Mobility and Electric Powertrain Weight Sensitivity: As high-power electric motorcycles and lightweight adventure electric vehicles enter the Rogaland transport ecosystem, compensating for high-density lithium battery mass becomes paramount. Eliminating gram-level weight at rotating hub positions allows chassis designers to regain battery efficiency, accelerate suspension response, and balance total bike weight distribution.
3. Demand for Transparent Multi-Tier OEM/ODM Traceability: Modern procurement officers in Rogaland demand end-to-end digital auditing. Velnora answers this requirement by supplying raw material mill test certificates (MTC), dimensional CMM validation, and live CNC process video documentation with every production run.
Velnora Titanium: China's Titanium Valley Manufacturing Engine
Founded in 2013 in Baoji, Shaanxi—globally acknowledged as China's Titanium Valley—Velnora Titanium Industry Co., Ltd. operates a vertically integrated production plant dedicated to precision titanium machining, cold forging, thread rolling, and decorative PVD/anodization surface finishing.
Our workshop integrates advanced multi-axis CNC lathe centers, wire EDM tooling, and calibrated thread tapping stations compliant with DIN, ISO, ANSI, and JIS technical frameworks. With a permanent team of expert machinists and mechanical engineers, we eliminate third-party subcontractor delays, guaranteeing full process control from certified titanium bar stock to export-compliant wooden crate shipping.
Tailored CAD/STEP Engineering
Whether you require standard M18×1.5 Kawasaki rear axle nuts, M24×1.5 Ducati single-sided swingarm hub nuts, or fully bespoke castellated pin nuts, our engineers review 3D STEP/IGES models within four hours.
Verified Production Transparency
Every batch comes documented with unedited video walkthroughs of lathe operations, thread gauge testing, and spectrometer alloy verification, giving offshore purchasing teams total assurance before dispatch.
Global Direct Door-to-Door Logistics
Operating smooth air and sea logistics channels delivering directly into Rogaland, Oslo, and Bergen customs ports, offering DDP, CIF, and FOB terms tailored to European trade criteria.
Frequently Asked Questions: B2B Procurement for Stavanger Buyers
Essential engineering and contractual clarifications regarding OEM custom titanium axle hardware sourcing.
Why is Grade 5 (Ti-6Al-4V) preferred over commercially pure Grade 2 for rear wheel nuts?
Rear axle nuts are subjected to immense continuous shear loads and axial tension (typically requiring 90–145 Nm of torquing torque). Grade 2 commercially pure titanium has a nominal tensile strength of roughly 345 MPa, which is insufficient and risks catastrophic yielding under axle clamp forces. Grade 5 (Ti-6Al-4V) provides a minimum tensile threshold of 895–1000 MPa, exceeding Class 8.8 structural steel requirements while providing the requisite fatigue resistance for high-stress motorcycle drive systems.
How does Velnora prevent thread galling on titanium axle fasteners?
Titanium naturally forms an instantaneous microscopic oxide layer that can suffer friction welding (galling) when mated under high load against identical metals or aluminum threads. Velnora solves this through two manufacturing principles: First, our critical threads are precision rolled or micro-machined to Ra ≤ 0.4 μm surface roughness. Second, we can supply specialized PVD coatings or instruct technicians to apply dedicated high-pressure anti-seize paste during final installation, ensuring smooth torque application and repeatable release cycles.
What are the typical Minimum Order Quantities (MOQ) for custom OEM dimensions?
For custom rear axle nuts requiring non-standard thread pitches (e.g., M20×1.0, M22×1.5, or single-sided swingarm hub configurations up to M50), our standard production MOQ is typically 50 to 100 pieces per spec. For standard metric flange dimensions where tooling is already established, pilot runs starting from 20 pieces can be arranged to assist racing teams with pre-season dyno and track evaluation.
Can Velnora deliver customized locking mechanisms (such as castellated, nylon-insert, or pinch ring)?
Yes. We routinely fabricate DIN 985 compatible nylon-locking ring inserts, safety-drilled hex faces for lock-wire installation on race-sanctioned bikes, castellated crown cuts for split-cotter pins, as well as bi-hex (12-point) lightened designs with integral rotating flange washers.
What is the production lead time and shipping turnaround to Western Norway?
Standard OEM CNC sample machining cycles require 7 to 12 working days. Full batch manufacturing (500–2,000 pcs) typically executes within 18–25 days. Air express shipments (via DHL, FedEx, or UPS direct to Stavanger Sola Airport or regional hubs) require 4 to 6 business days, complete with automated tracking, customs documentation, and mill test certification.
Accelerate Your Custom Titanium Manufacturing Pipeline
Connect directly with our engineering division in Baoji. Send your 2D blueprints, 3D CAD files, or OEM sample specifications for a swift metallurgical review and volume quotation.
Inquire Now