Featured Titanium Handlebar Ends & Precision CNC Fasteners
Machined in China’s Titanium Valley (Baoji) and verified via multi-axis Wire EDM and coordinate measuring machines. Ready for containerized or express air shipping directly into Davidson County, Tennessee.
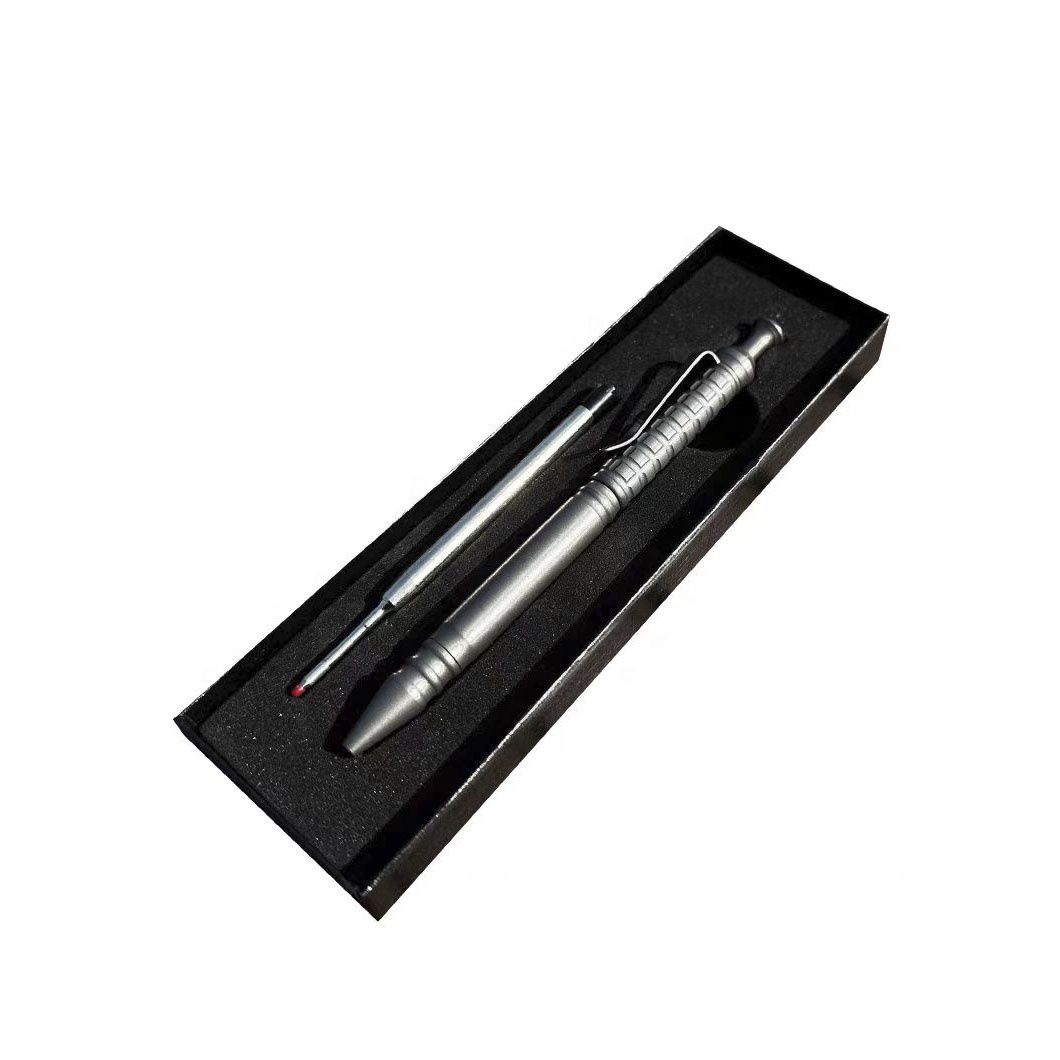
Cnc Machining Wire EDM Stainless Steel Multifunctional Bolt Titanium Alloy Tactical Pen Portable Outdoor EDC Ballpoint Pens
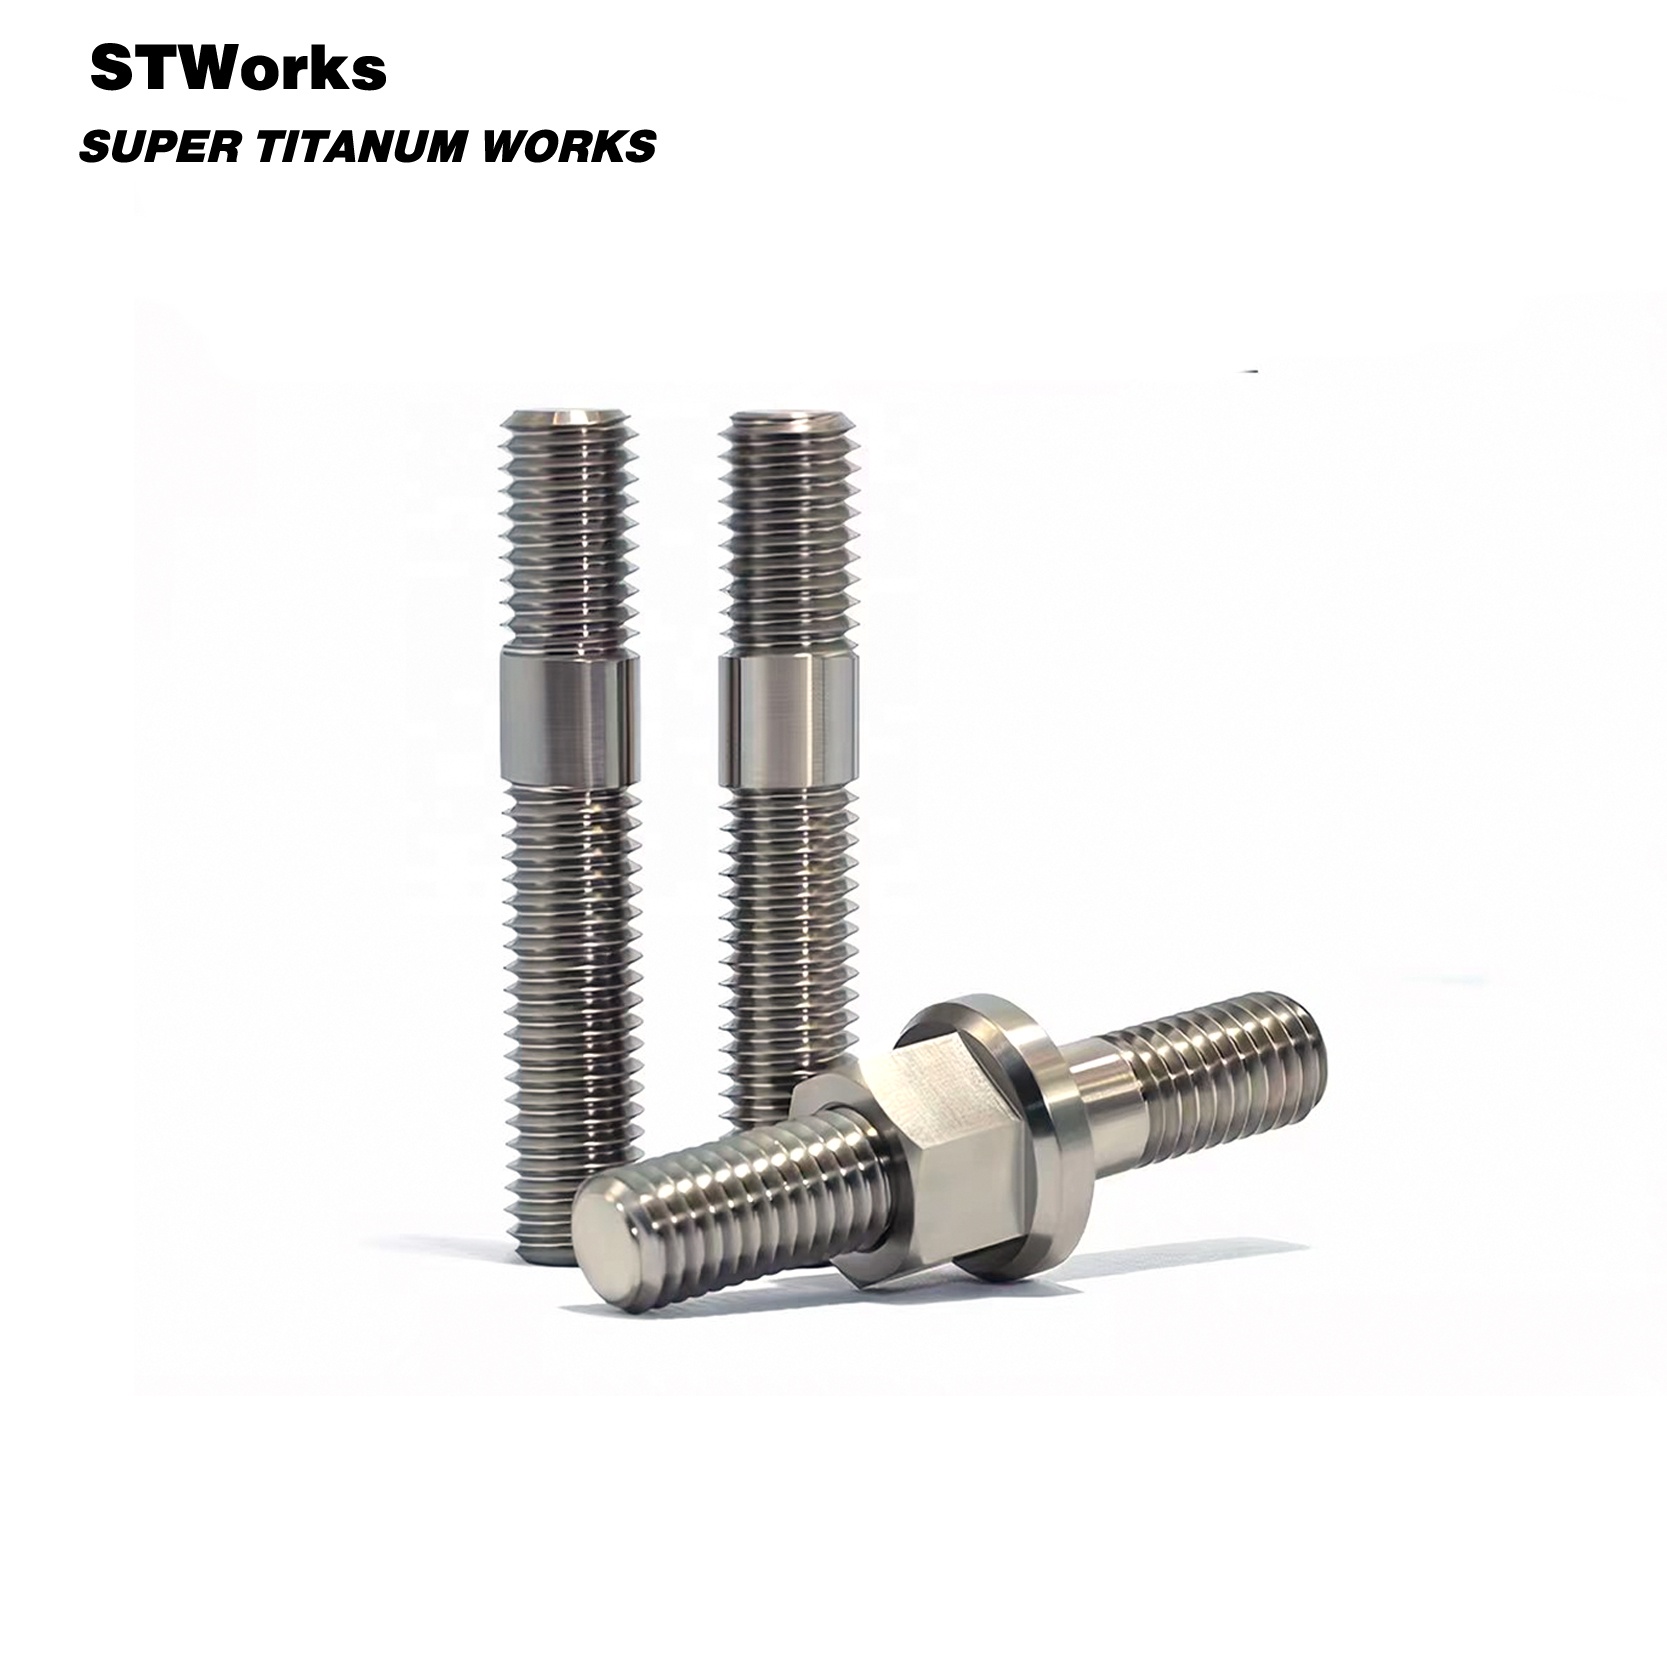
12 Point Nuts Titanium 6AL-4V Grade Exhaust Pipe Screws M8x1.25 Ultra Light Corrosion Resistant Motorcycle Auto Modification
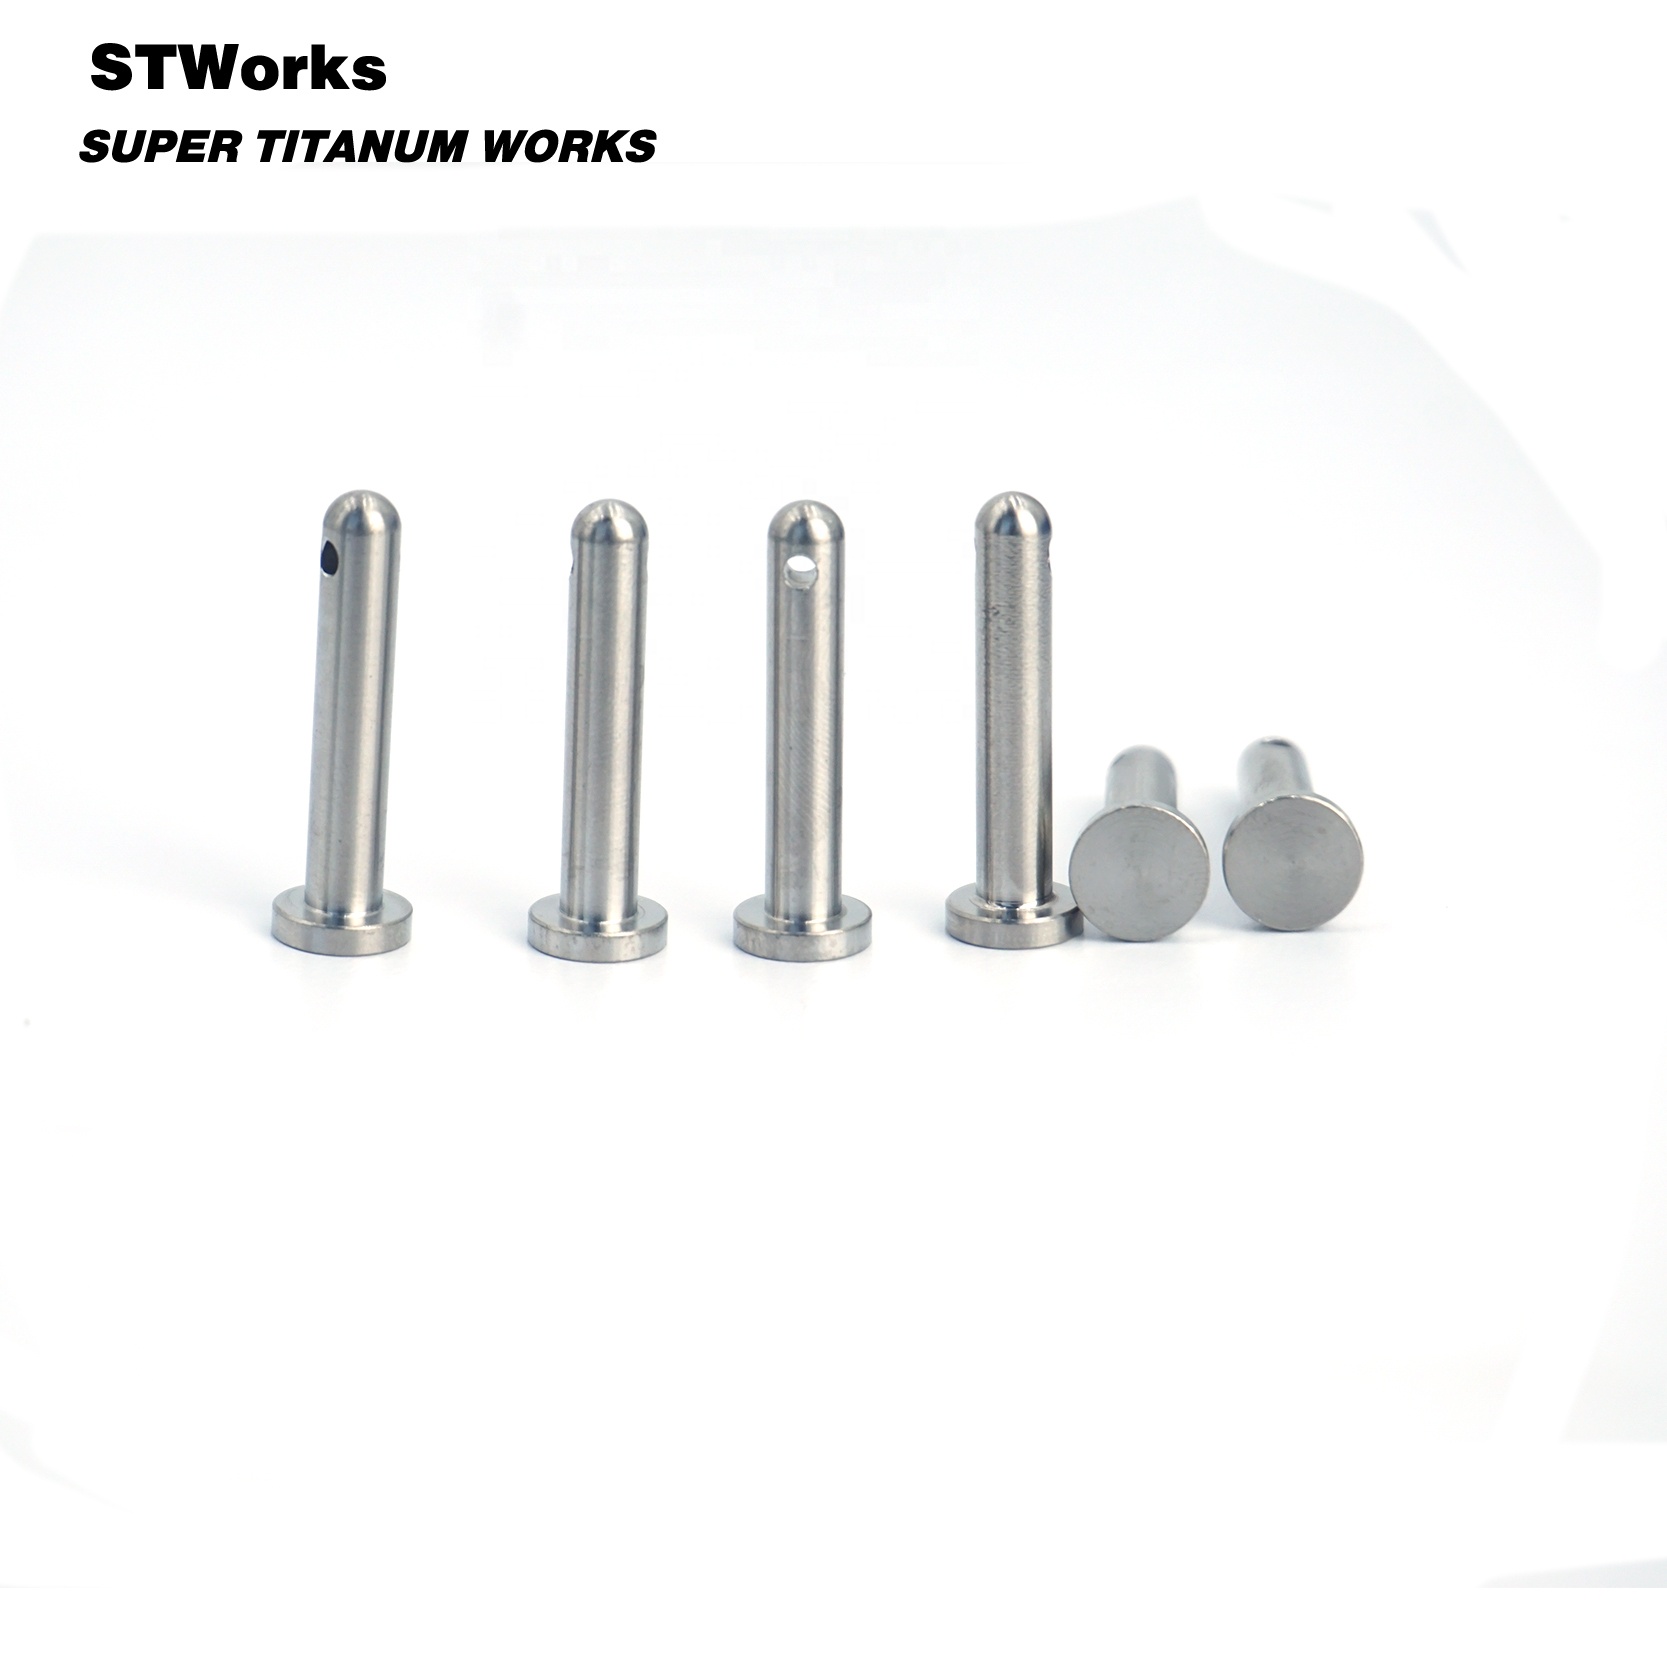
Titanium Alloy Clevis Pins Flat Head With Hole Cylindrical Locating Dowel Pins 3 20mm M3 M4 M5 M6 M8 M10 M12 M20

Titanium Screws M2 M2.5 Customized Cylinder Head Bolt Din912 Torx Micro Machine Screw

TC4 Titanium Ti Torx M5x16 /18/20/25mm Tapered Head Bolt with Washer Screw for Bicycle Stem Bolts
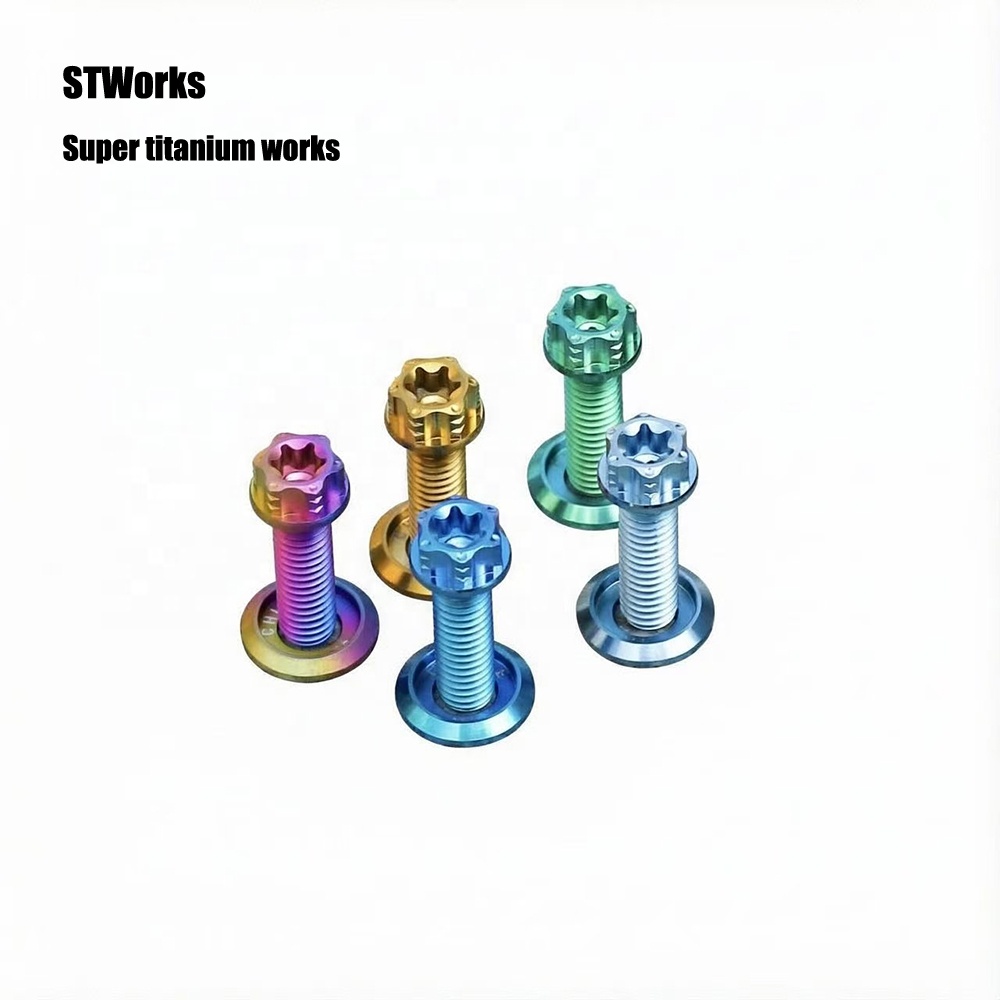
Titanium Alloy Bicycle Disc Brake Caliper Mounting Bolts Candy-Colored M6x20 with Washers
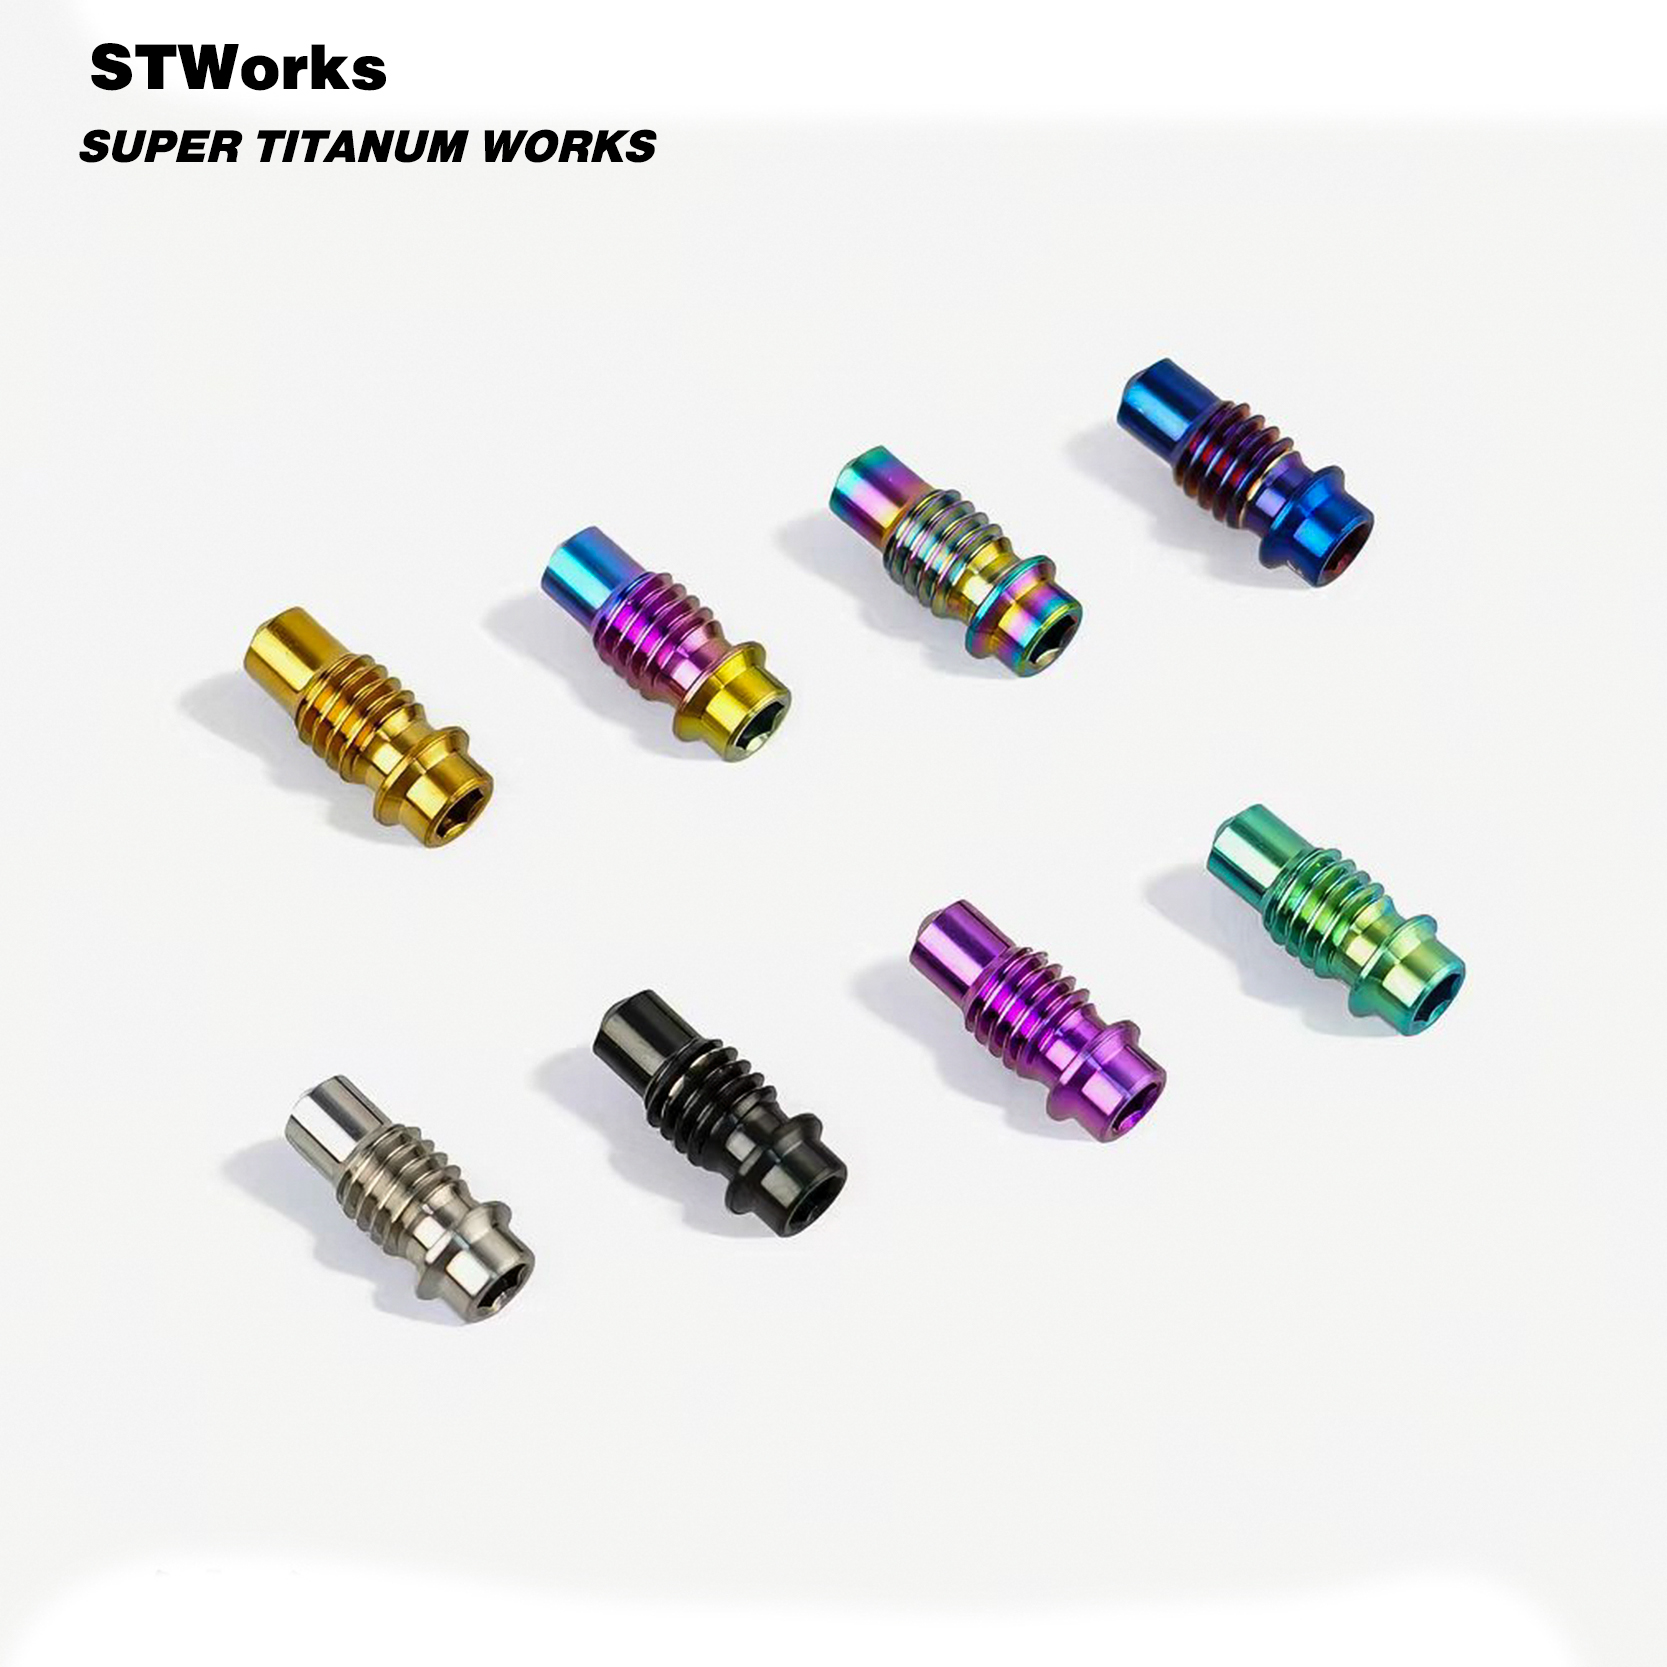
TC4 Titanium Caliper Bleed Port Screw for Shimano Road Disc Brake Caliper Road Bike Cycling Replacement Parts
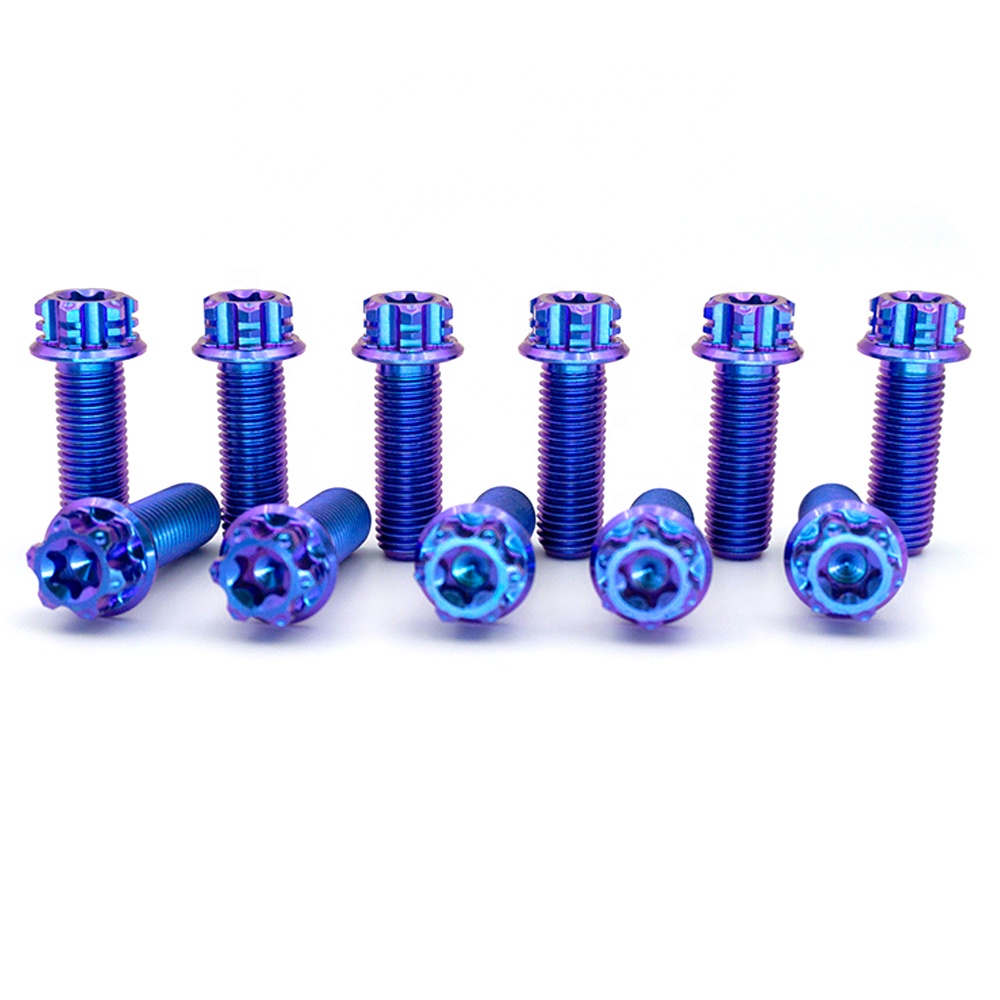
Titanium Alloy Hexagonal Flange Head Bolts and Screws for GR5 Motorcycle Modification
Engineering Superiority: Why Nashville Demands Baoji Titanium
An analysis of Ti-6Al-4V Grade 5 metallurgy, harmonic dampening advantages, and precision CNC bar end geometry tailored for the expanding cycling ecosystems of Greater Nashville.
Handlebar ends, expanding bar plugs, and cockpit interface screws are critical contact points directly dictating rider ergonomics, safety margin, and vibration attenuation. For professional bike boutiques in East Nashville, performance cycling shops around Green Hills, and custom motorcycle builders in the Gulch, conventional 6061-T6 aluminum or heavy chrome steel hardware represents a technical compromise. Aluminum suffers from notch fatigue and galvanic seizure, while steel introduces excessive rotational mass at the steering extremities.
Sourced directly from Baoji, China—globally acknowledged as "China’s Titanium Valley" producing over 65% of the world's raw aerospace titanium—Velnora Titanium Industry Co., Ltd. machines handlebar end assemblies and structural cockpit fasteners using certified Ti-6Al-4V (Grade 5, TC4) bar stock. Through cold-rolling threads, precision Swiss-type CNC lathe turning, and wire electrical discharge machining (EDM), our titanium components solve the exact challenges confronting riders tackling the rolling hills and unpredictable weather patterns of Middle Tennessee.
| Material Specification | Gr5 Ti-6Al-4V (Velnora Core) | Gr2 Commercially Pure Ti | 6061-T6 Anodized Aluminum | 316 Marine Stainless Steel |
|---|---|---|---|---|
| Density (g/cm³) | 4.43 (Optimized Cockpit Balance) | 4.51 | 2.70 | 7.98 (Exceedingly Heavy) |
| Ultimate Tensile Strength (MPa) | 950 – 1050 | 345 – 480 | 310 | 580 |
| Elastic Modulus (GPa) | 114 (Superior Vibration Damping) | 103 | 69 (Rigid / Road Buzz Fatigue) | 193 (Harsh Harmonic Transfer) |
| Relative Weight vs. Steel | -44.5% Mass Reduction | -43.5% | -66.2% | 0% Baseline |
| High-Humidity & Road Salt Resistance | Immune (Self-healing TiO₂ Film) | Immune | Susceptible to Crevice Pitting | Prone to Galvanic Galling |
| Vibration Absorption Coefficient | Exceptional (Cuts Neuroma/Fatigue) | High | Low (Transmits Harsh Chatter) | Minimal |
Engineered for Nashville’s Diverse Riding Topography
From high-speed Natchez Trace bikepacking excursions to rugged technical singletrack in Percy Warner Park, discover how our titanium handlebar ends withstand local conditions.
Percy Warner & Lock 4 MTB Singletrack
Mountain bikers negotiating rock gardens and tight oak tree clearances throughout Middle Tennessee demand handlebar ends that do not shear, deform, or crack when clipping rock faces. Our CNC hollow-core Grade 5 bar plugs utilize an internal multi-segment expansion collet that stays anchored under aggressive torsional impact.
- Zero crash-shatter risk unlike brittle carbon fiber caps
- Protects carbon bar ends from delaminating during ground contact
- Available in scratch-resistant micro-blasted or PVD oil-slick finishes
Natchez Trace Parkway Endurance & Gravel
Tennessee’s gravel and long-range road community endures 80+ mile days across variable humidity, coarse limestone trails, and river valley climbs. Titanium handlebar extensions and weighted bar dampeners absorb road chatter, preventing hand numbness and early muscle cramping along the Harpeth River loops.
- Substantial weight reduction on front steering pivot
- Ergonomic 15-degree sweep bar-end designs for shifting grip positions
- Integrated M5/M6 stem bolt matching for cohesive aesthetics
Custom Nashville V-Twin & Cafe Racers
Nashville’s vibrant custom motorcycle builders and hot rod garages on Nolensville Pike require heavyweight bar-end counterweights and 12-point exhaust hardware. Our titanium bar-ends diminish the 45-degree engine primary vibrations on cruiser handlebars, stabilizing mirrors and providing an exotic heat-treated burnt look.
- Custom weighted internal slugs up to 180 grams
- High-temperature resistance for exhaust pipe screws and brake calipers
- CNC fluted profiles with laser-etched custom shop branding
Market Trends Shaping Titanium Component Sourcing in Nashville
Key macroeconomic and demographic shifts fueling aggressive procurement of ultra-durable titanium cycling and automotive components across Davidson, Williamson, and Rutherford counties.
1. Greenways & Urban Mobility Surge
Nashville’s multi-million dollar expansion of the Cumberland River Greenway and Davidson County commuter corridors has spiked demand for high-mileage e-bikes and premium urban commuters where weatherproofing against rain and winter de-icers is paramount.
2. Boutique Gravel Custom Builds
Cyclists in Franklin, Brentwood, and Murfreesboro are shifting toward bespoke handbuilt frames (titanium, custom steel, aero carbon). Builders specify titanium handlebar ends, stem bolts, and disc caliper mountings to match unpainted titanium frames.
3. Supply Chain Direct-Sourcing
Distributors and regional master mechanics are bypassing intermediate domestic repackagers. Sourcing directly from verified Chinese manufacturers provides 40-55% margin recovery while retaining ISO and DIN standard traceability.
4. Custom Anodization Demand
Riders no longer accept plain black components. Electric violet, burnt bronze, candy gold, and splash-anodized Timascus finishes are commanding premium retail markups across independent bike dealers in Nashville.
Why Nashville Importers Partner With Velnora Titanium
Operating since 2013 in Baoji’s Precision Manufacturing Park, we integrate raw titanium sponge vacuum smelting, 5-axis CNC machining, wire EDM cutting, and strict metallurgical verification.
Certified Mill Test Reports (MTC)
We trace every titanium bar directly to its metallurgical source. Our parts include 100% material chemical composition and mechanical tensile stress test reports matching ASTM B348, DIN 912, and ISO standards, ensuring no recycled porous scrap enters production.
Real-Time Video Machining Updates
Eliminate cross-border supply chain blind spots. As documented in our verified supplier reviews, our production engineers provide live machining progress clips, EDM wire cutting footage, thread pitch gauge verification videos, and batch packaging proofs prior to dispatch.
Agile OEM / ODM Custom Geometry
Whether you require standard 22.2mm flat-bar mountain bike plugs, 23.8mm road drop-bar internal wedges, integrated bar-end mirror mounts, or custom laser engraving with your Nashville cycling club insignia, our engineering team handles CAD drawings within 24 hours.
3D CAD & Tolerancing Audit
Clients submit STEP, IGES, or detailed 2D blueprints. Our machinists conduct a manufacturing feasibility review to optimize clamping tolerances and eliminate unnecessary tool repositioning costs.
Cold Thread Rolling & CNC Turning
Unlike competitors who cut threads on standard lathes, our fastener threads are cold-rolled. This maintains continuous grain structure, preventing fatigue shearing under severe cyclical loads.
PVD / Electro-Chemical Finishing
Parts undergo ultrasonic degreasing followed by micro-arc oxidation or physical vapor deposition (PVD) to achieve vibrant rainbow, emerald, gold, or stealth black finishes with surface hardness up to HV 2200.
Nashville Buyer FAQ: Technical & Import Logistics
Clear, transparent answers addressing customs clearance, Tennessee climate considerations, galling prevention, and DDP shipping into Greater Nashville.
How do you ship titanium handlebar ends and fasteners directly into Nashville, TN?
We provide comprehensive Delivered Duty Paid (DDP) or CIF/FOB logistics tailored for Tennessee businesses. For sample runs and urgent inventory top-offs (50–500 pcs), we utilize express air cargo (DHL Express, FedEx International Priority, UPS) landing directly at Nashville International Airport (BNA) within 4 to 6 business days. All US customs declaration paperwork, Section 301 tariffs, and entry clearances are managed seamlessly with no paperwork bottlenecks for your receiving dock.
For recurring bulk distributor container loads, shipments clear through the Port of Savannah or Charleston and transit via intermodal rail directly into the Nashville CSX intermodal rail terminal, optimizing container freight economics.
How does Tennessee’s humid subtropical climate impact titanium bar plugs vs. aluminum?
Nashville experiences intense summer humidity (often exceeding 85% RH) accompanied by road grime, perspiration salt, and aggressive magnesium chloride brines applied during winter freeze alerts on Interstate 40 and local parkways. When aluminum bar plugs contact carbon handlebars in the presence of conductive moisture, galvanic corrosion accelerates, often welding the expander bolt permanently.
Grade 5 Titanium (Ti-6Al-4V) instantly regenerates a microscopic, chemically inert titanium dioxide (TiO₂) passivation layer when exposed to oxygen. It is completely impervious to sweat salts, atmospheric moisture, and de-icing chemicals, ensuring that expander wedges can always be removed for servicing years later.
What torque guidelines and anti-seize protocols should bike mechanics follow?
Because titanium has a low thermal conductivity and high friction coefficient, bare titanium threads tightened dry against other metals can experience friction-induced cold welding known as galling. We advise all Nashville assembly technicians to apply a high-quality copper or copper-free synthetic anti-seize paste (such as Finish Line Ti-Prep or Park Tool ASC-1) to all external threads prior to installation.
Torque specs for handlebar end expander bolts (typically M5 or M6) should be tightened strictly to 4.5 – 5.5 N·m using a calibrated torque wrench. Never use pneumatic or battery impact drivers on titanium cockpit hardware.
Can you manufacture custom expanding wedges for carbon bars with non-standard internal diameters?
Yes. While standard aluminum bars feature internal diameters of 18mm to 20mm, modern ultra-light aero road bars and thick-wall downhill carbon bars can range from 15.5mm to 21.5mm. We machine custom dual-taper expansion sleeves out of 6061 aluminum or Grade 2 titanium paired with Grade 5 compression bolts, guaranteeing a flush outer fit and non-slip clamping that will not crush delicate carbon fibers.
What are the minimum order quantities (MOQ) and lead times for OEM private labeling?
Standard catalog items (such as DIN 912 titanium bolts, disc caliper screws, and standard flat-head bar ends) have an MOQ of only 50 to 100 sets per specification. For custom CNC designs involving proprietary knurling, bespoke laser marking, or custom anodized color matching, our initial trial MOQ is typically 200 pieces.
Sample production lead times are 7 to 10 days, while bulk batch production (1,000–5,000 pcs) completes in 18 to 22 business days.
How do you guarantee thread precision and internal dimensional consistency?
Our quality control protocol incorporates a multi-tier gate review: 1) Spectrographic raw ingot material verification; 2) In-process CNC tool wear calibration after every 50 parts; 3) 100% thread ring gauge (Go / No-Go class 6g / 6H) inspection; 4) Coordinate Measuring Machine (CMM) dimensional verification; and 5) Random salt spray test validation for all surface treatments.
Connect Directly with Our Baoji Engineering Team
Ready to elevate your bike shop inventory, replace corroded OEM fleet hardware, or develop custom branded titanium handlebar ends for the Nashville market? Our engineering team replies with complete DDP quotes, CAD reviews, and material test certificates within 4 business hours.