Specialist Titanium Components Serving David Engineering Teams
Billet-machined from Ti-6Al-4V aerospace bar stock in China's Titanium Valley, verified with optical inspection and mill test certifications.



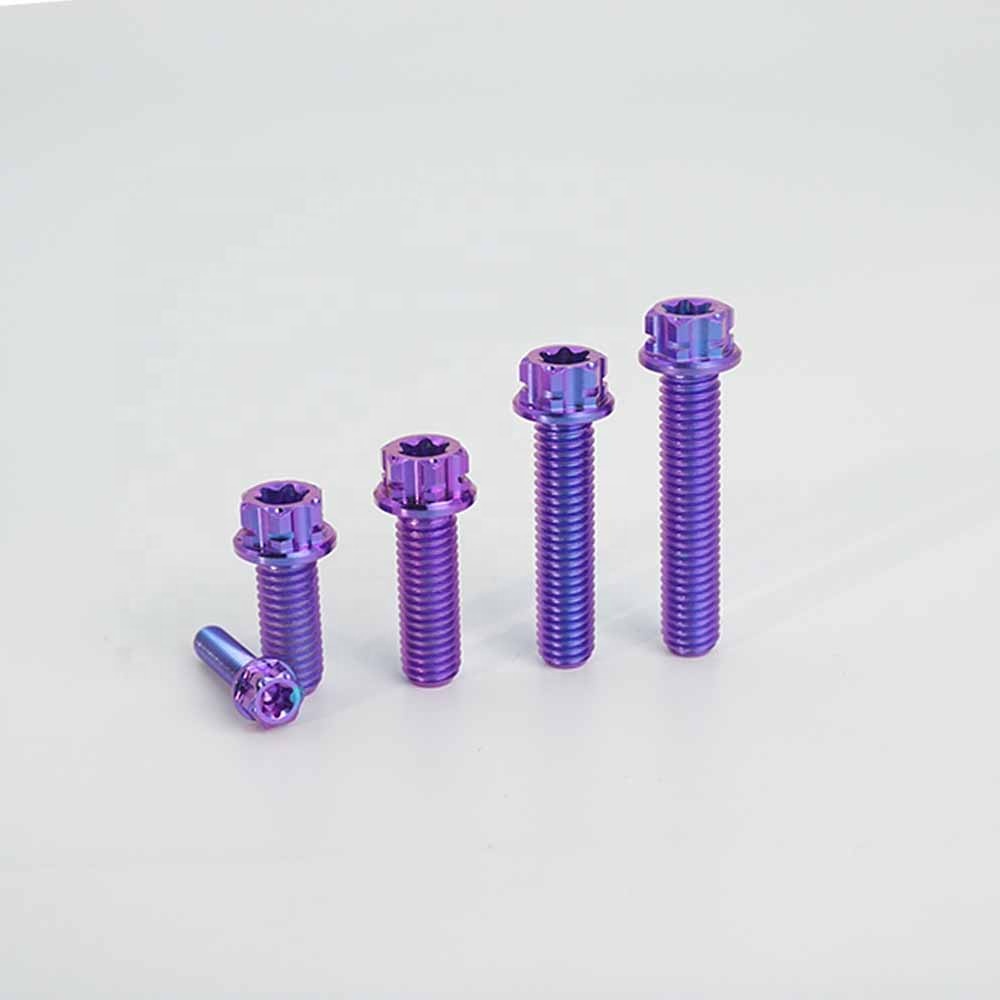
1. Advanced Valvetrain Dynamics: Why Ti-6Al-4V Exhaust Valve Spring Retainers Outperform Steel in Forced-Induction Applications
In high-performance internal combustion engines, the exhaust valve assembly operates under severe thermodynamic and cyclic stress profiles. While intake valves experience the cooling effect of incoming air-fuel charges, exhaust valves and their adjacent spring retainers are subjected to superheated combustion blow-by reaching upwards of 750°C to 850°C, accompanied by intense mechanical vibration. For engine builders, racing workshops, and performance aftermarket distributors in David, Chiriquí, the selection of the correct spring retainer material is the defining factor in surviving valve float, erratic harmonics, and high-RPM fatigue failures.
Standard OEM retainers manufactured from stamped mild steel or machined 4140 chromoly alloy carry significant reciprocating mass. Under high engine speeds exceeding 8,500 RPM, the inertia of a heavy valve spring retainer imposes tremendous parasitic drag on the valve spring. The spring must expend substantial energy merely to control the kinetic mass of the retainer and lock assembly, leading directly to valve float—where the valve head bounces off the seat or fails to track the camshaft lobe contour precisely. By contrast, Grade 5 Titanium (Ti-6Al-4V TC4) possesses a density of approximately 4.43 g/cm³, delivering a dramatic 40% to 45% reduction in reciprocating valvetrain weight compared to steel (7.85 g/cm³), while sustaining an ultimate tensile strength exceeding 895 MPa.
Valvetrain Inertia Principle: Cutting just 8 to 12 grams from each exhaust valve retainer reduces valvetrain kinetic energy exponentially at high engine speeds ($E_k = \frac{1}{2} m v^2$). This mass reduction effectively elevates the engine's float threshold by 600 to 1,200 RPM without necessitating destructive valve spring seat pressures that accelerate camshaft lobe wear.
Velnora Titanium Industry Co., Ltd., based out of Baoji—China's recognized Titanium Valley—manufactures CE certified titanium exhaust valve spring retainers that incorporate precision internal taper angles (standard 7°, 8°, or 10° Super 7/Super 10 lock collet configurations) broached with Swiss-style 5-axis CNC turning and wire EDM cutting. By adhering strictly to ISO 9001 and European CE standardizations (Machinery Directive compliance documentation and material chemical traceability EN 10204 3.1), Velnora ensures that racing stables and industrial engine workshops operating throughout Western Panama receive valvetrain hardware devoid of internal inclusions, lattice imperfections, or micro-cracking.
2. Metallurgical Comparison: Valvetrain Retainer Material Suitability Matrix
To assist David engine builders, marine logistics engineers, and tuning shops in making data-backed component selections, the comparative characteristics of commercial valve spring retainer materials are summarized below:
| Material Specification | Velnora Gr5 Ti-6Al-4V (CE Certified) | 4140 Hardened Chromoly Steel | 7075-T6 Billet Aluminum |
|---|---|---|---|
| Density (g/cm³) | 4.43 (Optimally Light) | 7.85 (Heavy Reciprocating Mass) | 2.81 (Extremely Light) |
| Tensile Strength (Yield / Ult.) | 828 / 895+ MPa | 700 / 950+ MPa | 480 / 540 MPa |
| Thermal Creep Resistance (400°C) | Superior (Maintains Lattice) | High | Catastrophic Failure (>150°C) |
| Fatigue Endurance Limit | 510 MPa (High Cyclic Life) | 460 MPa | 160 MPa (Prone to Snap) |
| Collet Step Wear Resistance | PVD DLC or Nitrided Hardened | Case Hardened | Very Low (Galls Rapidly) |
| Tropical Marine Corrosion | Total Immunity (Ti-Oxide Layer) | Prone to Oxidation & Rust | Prone to Galvanic Pitting |
3. Why CE Certification and EN 10204 3.1 Traceability Matter for Regional Exporters
Procuring valvetrain components from third-party intermediaries often introduces high failure rates caused by counterfeit or improperly alloyed titanium. Titanium scrap blends and Grade 2 commercial pure titanium lack the necessary vanadium (4%) and aluminum (6%) stabilizers. In an exhaust valvetrain, a retainer manufactured from Grade 2 or uncertified Grade 5 will experience ductile yield under spring load, pulling the valve locks straight through the center hole and dropping the exhaust valve into the cylinder—causing catastrophic piston, head, and cylinder bore destruction.
Velnora provides complete CE Certified conformity declaration alongside spectrometer-verified EN 10204 3.1 chemical analysis and tensile yield certificates for every shipment exported to Chiriquí. Our optical comparators and 3D coordinate measuring machines (CMM) maintain runout tolerances under ±0.005 mm, eliminating uneven spring coil pressure, lateral stem bending stresses, and guide wear.
Engineered for Chiriquí's High-Stress Operating Environments
How our CE certified titanium exhaust retainers solve specific environmental, topographic, and competitive challenges in David and Western Panama.
Local 1/4-Mile Drag & Circuit Racing
David is the motorsport nexus of Western Panama, hosting high-profile acceleration events and circuit showdowns. Local workshops frequently tune turbocharged Japanese (Toyota 2JZ-GTE, Nissan RB26/VR38, Honda K-Series) and European platforms running boost pressures upwards of 2.5 bar.
- Eliminates valvetrain float up to 10,200 RPM on solid-lifter setups.
- Accommodates dual-spring setups (inner & outer springs) with custom step diameters.
- Broached retainer pockets prevent spring rotation wear during anti-lag backfiring.
Chiriquí Highlands & Off-Road Rallies
From the humid coastal flats of David ascending toward the highlands of Boquete and Volcán Baru, engine builders confront intense thermal cycling and barometric pressure drops. Custom 4x4 Trophy Trucks and rally rigs require uninterrupted mechanical endurance.
- Immune to thermal fatigue across radical elevation and ambient temperature swings.
- Grade 5 toughness prevents stress corrosion cracking under constant shock loads.
- Lightens overhead valvetrain weight, lowering engine center-of-gravity.
Gulf of Chiriquí Marine & GenSets
Commercial fishing outboards, marine interceptor boats based at Puerto Pedregal, and continuous-run standby generators in David demand components immune to oceanic salt mist and heavy sulfur exhaust gases.
- Natural titanium oxide surface layer completely stops saltwater oxidation.
- Replaces prone-to-corrode steel spring caps in high-output outboard engines.
- Maintains mechanical integrity under non-stop continuous 24/7 industrial load.
Valvetrain Modernization Trends in David and Central America (2025–2030)
Strategic insights for engine parts importers, wholesale distributors, and machine shops serving Western Panama and cross-border commercial arteries.
Ethanol & Methanol Fuel Tuning
As flex-fuel (E85) and straight alcohol fuel tuning expand in David's drag racing circuits, higher exhaust gas volumes and violent ignition timings necessitate titanium's higher cyclic fatigue threshold over aluminum alloys.
Advanced DLC / PVD Coatings
Retainers are increasingly ordered with Physical Vapor Deposition (PVD) and Diamond-Like Carbon (DLC) micro-coatings, eliminating microscopic surface galling against hardened steel valve locks and aggressive high-lift cams.
Direct China-to-David Logistics
Wholesalers are bypassing North American reselling markups by importing directly from Baoji via express air freight (DHL/FedEx to Enrique Malek International Airport) or consolidated sea freight via Panama Pacific ports.
Custom Blueprint Machining
Universal fitments are yielding to CNC custom designs tailored to proprietary valve spring diameters (Beehive, PAC, Ferrea, Supertech profiles), with local builders supplying CAD files for rapid Chinese production runs.
Manufacturing Authority: Velnora Titanium Industry Co., Ltd.
Headquartered in Baoji, Shaanxi Province—the premier metallurgical center producing over 60% of China's titanium—Velnora has operated as a specialist manufacturer and exporter since 2013. Serving automotive, aerospace, cycling, and EDC sectors across 1,000+ global commercial partners.
5-Axis CNC Precision
Broaching, turning, and wire EDM with tolerances held to ±0.005 mm for perfect collet seating and spring concentricity.
Live Video Verification
We send production videos and high-res micrometric inspection footage before packing, so you verify quality before dispatch.
Global Certifications
Full CE certification for engine hardware exports, ISO 9001 quality systems, and verified EN 10204 3.1 material test reports.
Rapid Response Logistics
≤ 4-hour technical response rate with complete DDP/DAP export handling to Panama City and David, Chiriquí.
Frequently Asked Questions: Sourcing Titanium Retainers for David & Panama
Technical and logistical guidance for race engine shops, auto parts retailers, and industrial purchasers in the Chiriquí region.
What specific titanium alloy is used for your exhaust valve spring retainers?
All Velnora performance exhaust valve spring retainers are manufactured exclusively from certified Grade 5 Ti-6Al-4V (also designated as TC4 in Chinese national standards). This aerospace alpha-beta alloy contains approximately 6% aluminum to stabilize the alpha phase and 4% vanadium to stabilize the beta phase. It delivers a minimum yield strength of 828 MPa and an ultimate tensile strength exceeding 895 MPa, combined with exceptional cyclic fatigue endurance at elevated exhaust valvetrain temperatures. We do not use Grade 2 pure titanium or uncertified remelt stock for valvetrain components.
Can Grade 5 titanium retainers be used with dual-spring or Beehive valve springs?
Yes. We engineer retainers for single springs, dual springs with dampers, and modern conical Beehive spring designs. For dual-spring systems, our CNC turning centers machine a precise step shoulder with controlled inner step diameter (ID) and outer step diameter (OD) that accurately locates both spring coils without excessive interference. We can machine to standard specifications (such as PAC Racing, Supertech, Ferrea, or Crower dimensions) or manufacture entirely custom geometries from your technical drawing (PDF, STEP, or IGES format).
How do you prevent galling between the titanium retainer and the hardened steel valve locks/collets?
Titanium can exhibit galling when placed in high-friction, unlubricated contact with hard tool steel under reciprocating micro-movement. To prevent collet step indentation or fretting, our CE certified retainers feature fine-surface micro-finishing (Ra ≤ 0.4 μm) on the lock taper. Furthermore, we offer optional thermal oxidation, physical vapor deposition (PVD) Diamond-Like Carbon (DLC) coatings, or physical nitriding. When installing, we recommend applying a molybdenum disulfide assembly paste to ensure proper lock seating during initial torque cycles.
What lock taper angles do you manufacture (e.g., 7-degree, 8-degree, 10-degree)?
We routinely machine standard 7-degree (OEM American and Japanese fitment), 8-degree (European sports platforms), and 10-degree / "Super 10" racing tapers. Precision taper geometry is verified on optical shadowgraphs to prevent point-loading, ensuring that clamping force is uniformly distributed across the entire contact face of the valve stem locks.
How are shipments handled to David, Chiriquí, Panama, and what are typical lead times?
For small-to-medium wholesale orders (50 to 500 sets), we ship via air express (DHL, FedEx, or UPS Priority) with customs clearance routed directly to David or via Panama City (Tocumen / PTY) onward to Enrique Malek Airport (DAV). Air express delivery from our Baoji facility typically arrives in David within 5 to 8 business days. For container-scale sea freight, shipments are routed via Ningbo or Shanghai to Puerto de Balboa (Pacific side) or Manzanillo International Terminal (Colón), followed by bonded highway transport to David.
What documentation accompanies CE certified shipments to Western Panama?
Every commercial export is supplied with a comprehensive documentation dossier: the CE Certificate of Conformity, an EN 10204 3.1 Mill Test Certificate detailing chemical composition (spectrometer analysis of Ti, Al, V, Fe, C, N, H, O) and mechanical yield testing, dimensional CMM inspection reports, commercial invoice, and a packing list detailing net and gross weights. Laser marking of part numbers or client logos is available free of charge.
What is your Minimum Order Quantity (MOQ) for custom-dimension retainers?
For standard catalog profiles or existing tooling setups, our MOQ begins at just 50 to 100 pieces (suitable for 3 to 6 V8 or 4-cylinder engine sets). For completely bespoke OEM/ODM designs requiring custom tooling and CAD/CAM setup, our standard MOQ is 200 pieces. Sample pilot batches (e.g., 16 pieces for engine dyno validation) can be arranged upon request.
Why choose titanium retainers over 7075-T6 aluminum retainers for exhaust valves?
While 7075-T6 aluminum is lightweight and inexpensive, it has a critically low thermal failure point. Aluminum rapidly loses structural yield strength at temperatures above 150°C. In an exhaust valvetrain, where conductive heat transfer through the exhaust valve stem raises spring cap temperatures significantly, aluminum retainers suffer from micro-creep, lock pull-through, and sudden fatigue fractures. Titanium Grade 5 preserves its structural lattice, yield strength, and fatigue resistance well beyond 400°C, making it the only reliable lightweight choice for exhaust applications.
Ready to Elevate Your Engine Reliability in David?
Send your valve spring diameter, lock taper angle, or CAD drawings directly to our Baoji metallurgical engineering desk. Get complete technical reviews, factory direct wholesale quotes, and video inspection verifications within 4 hours.