Factory-Direct Titanium Fastener & Fluid Port Inventory
Precision CNC machined components engineered to DIN, ISO, and aerospace specifications from verified Grade 5 (Ti-6Al-4V) billet stock.

Custom Grade 5 Titanium Plate Tag Sandblasted Blank
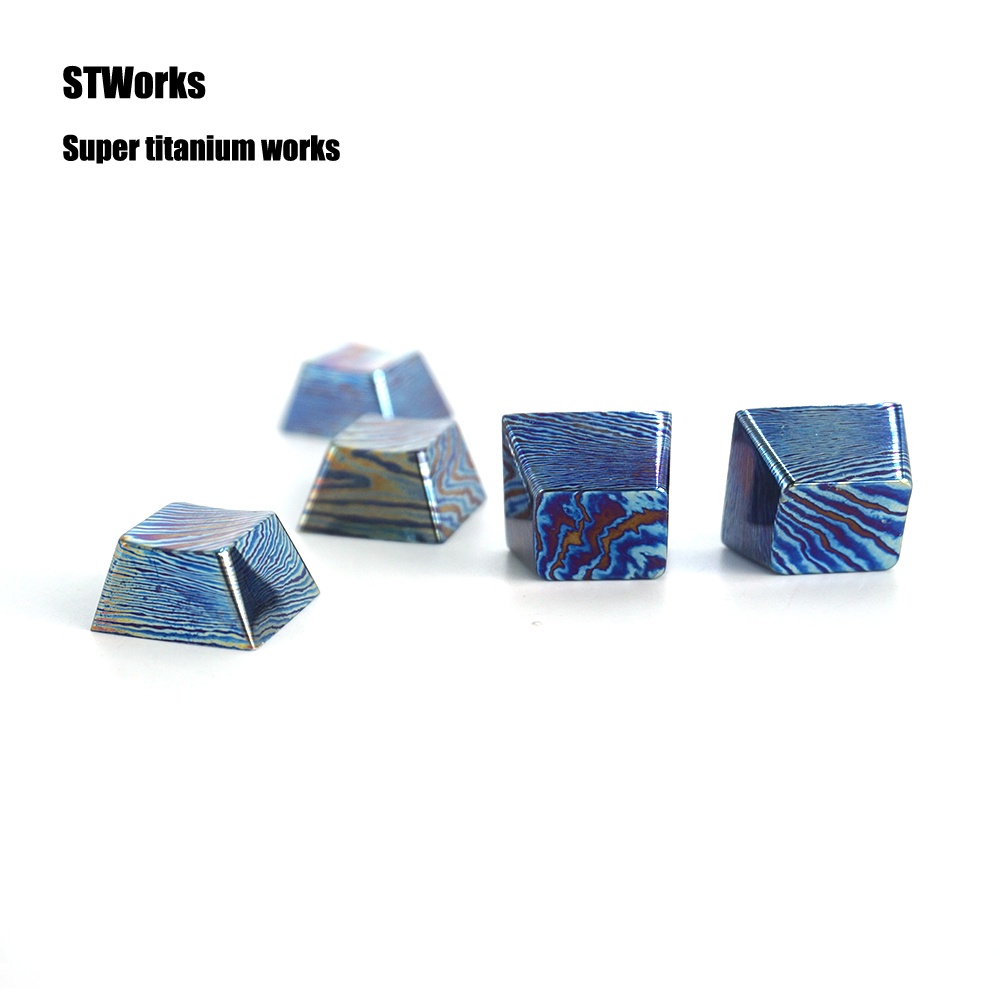
Titanium Gaming Keyboard Caps-CNC Machined Wire EDM
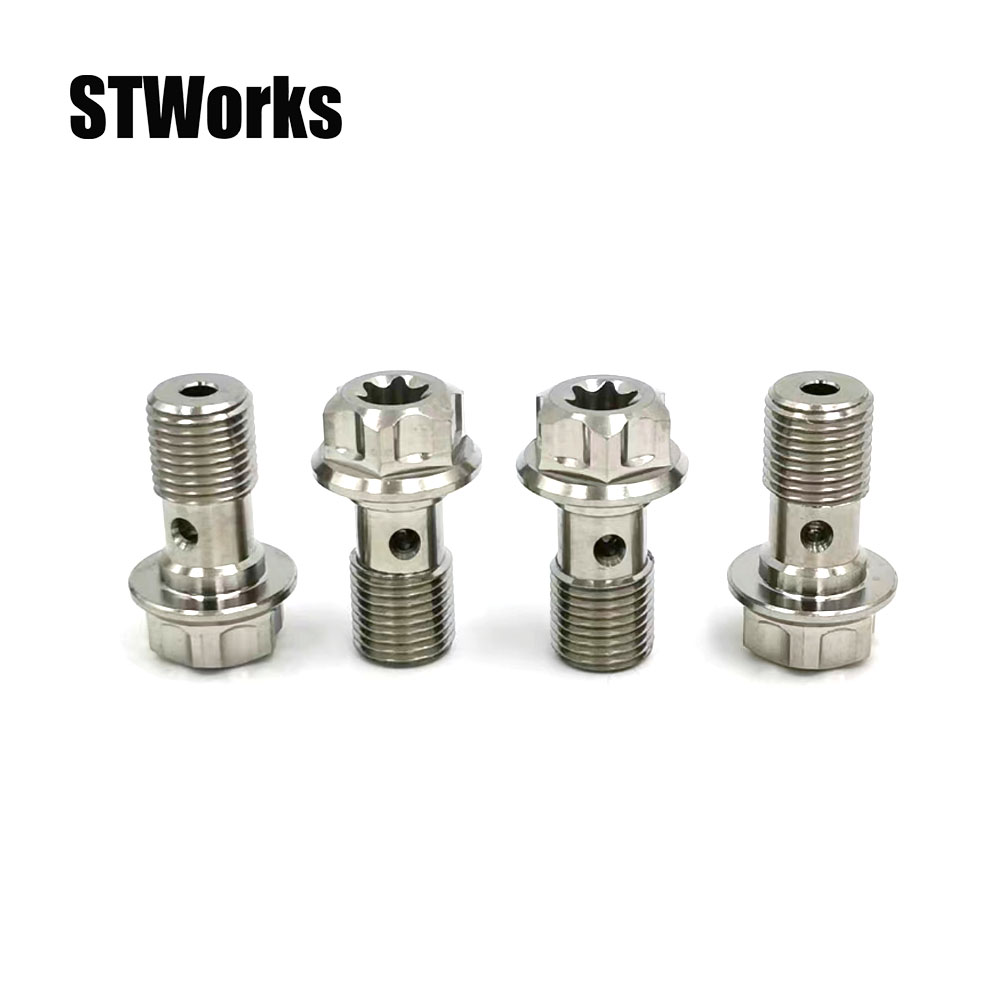
Gr5 Titanium Motorcycle Banjo Bolts Hex Head M10
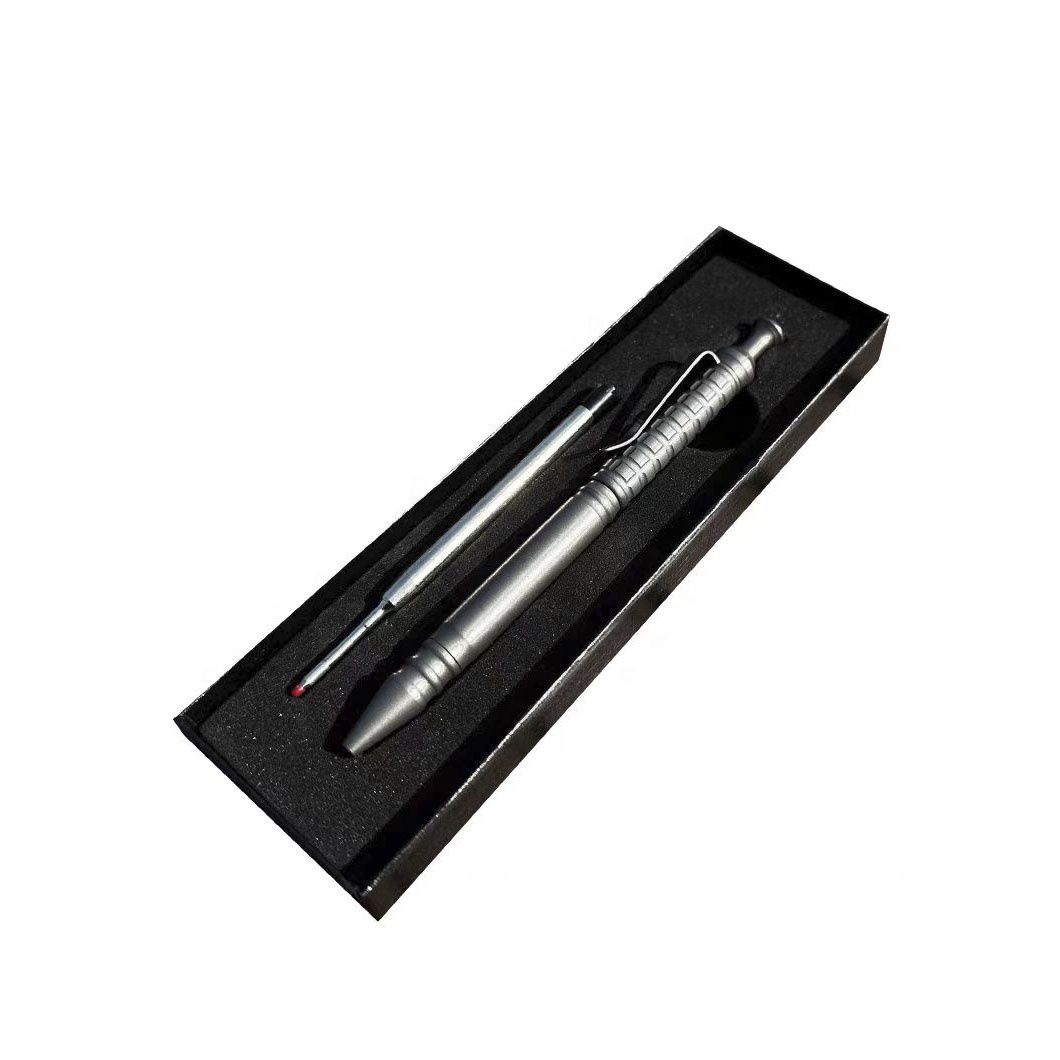
CNC Wire EDM Multifunctional Bolt Titanium EDC Pen
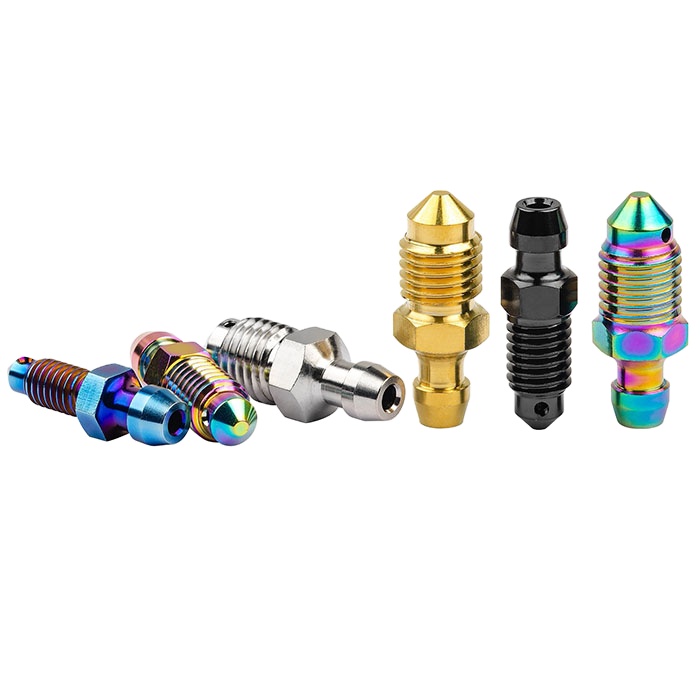
M10 Titanium GR5 Bolt Bleed Nipple Caliper Screws
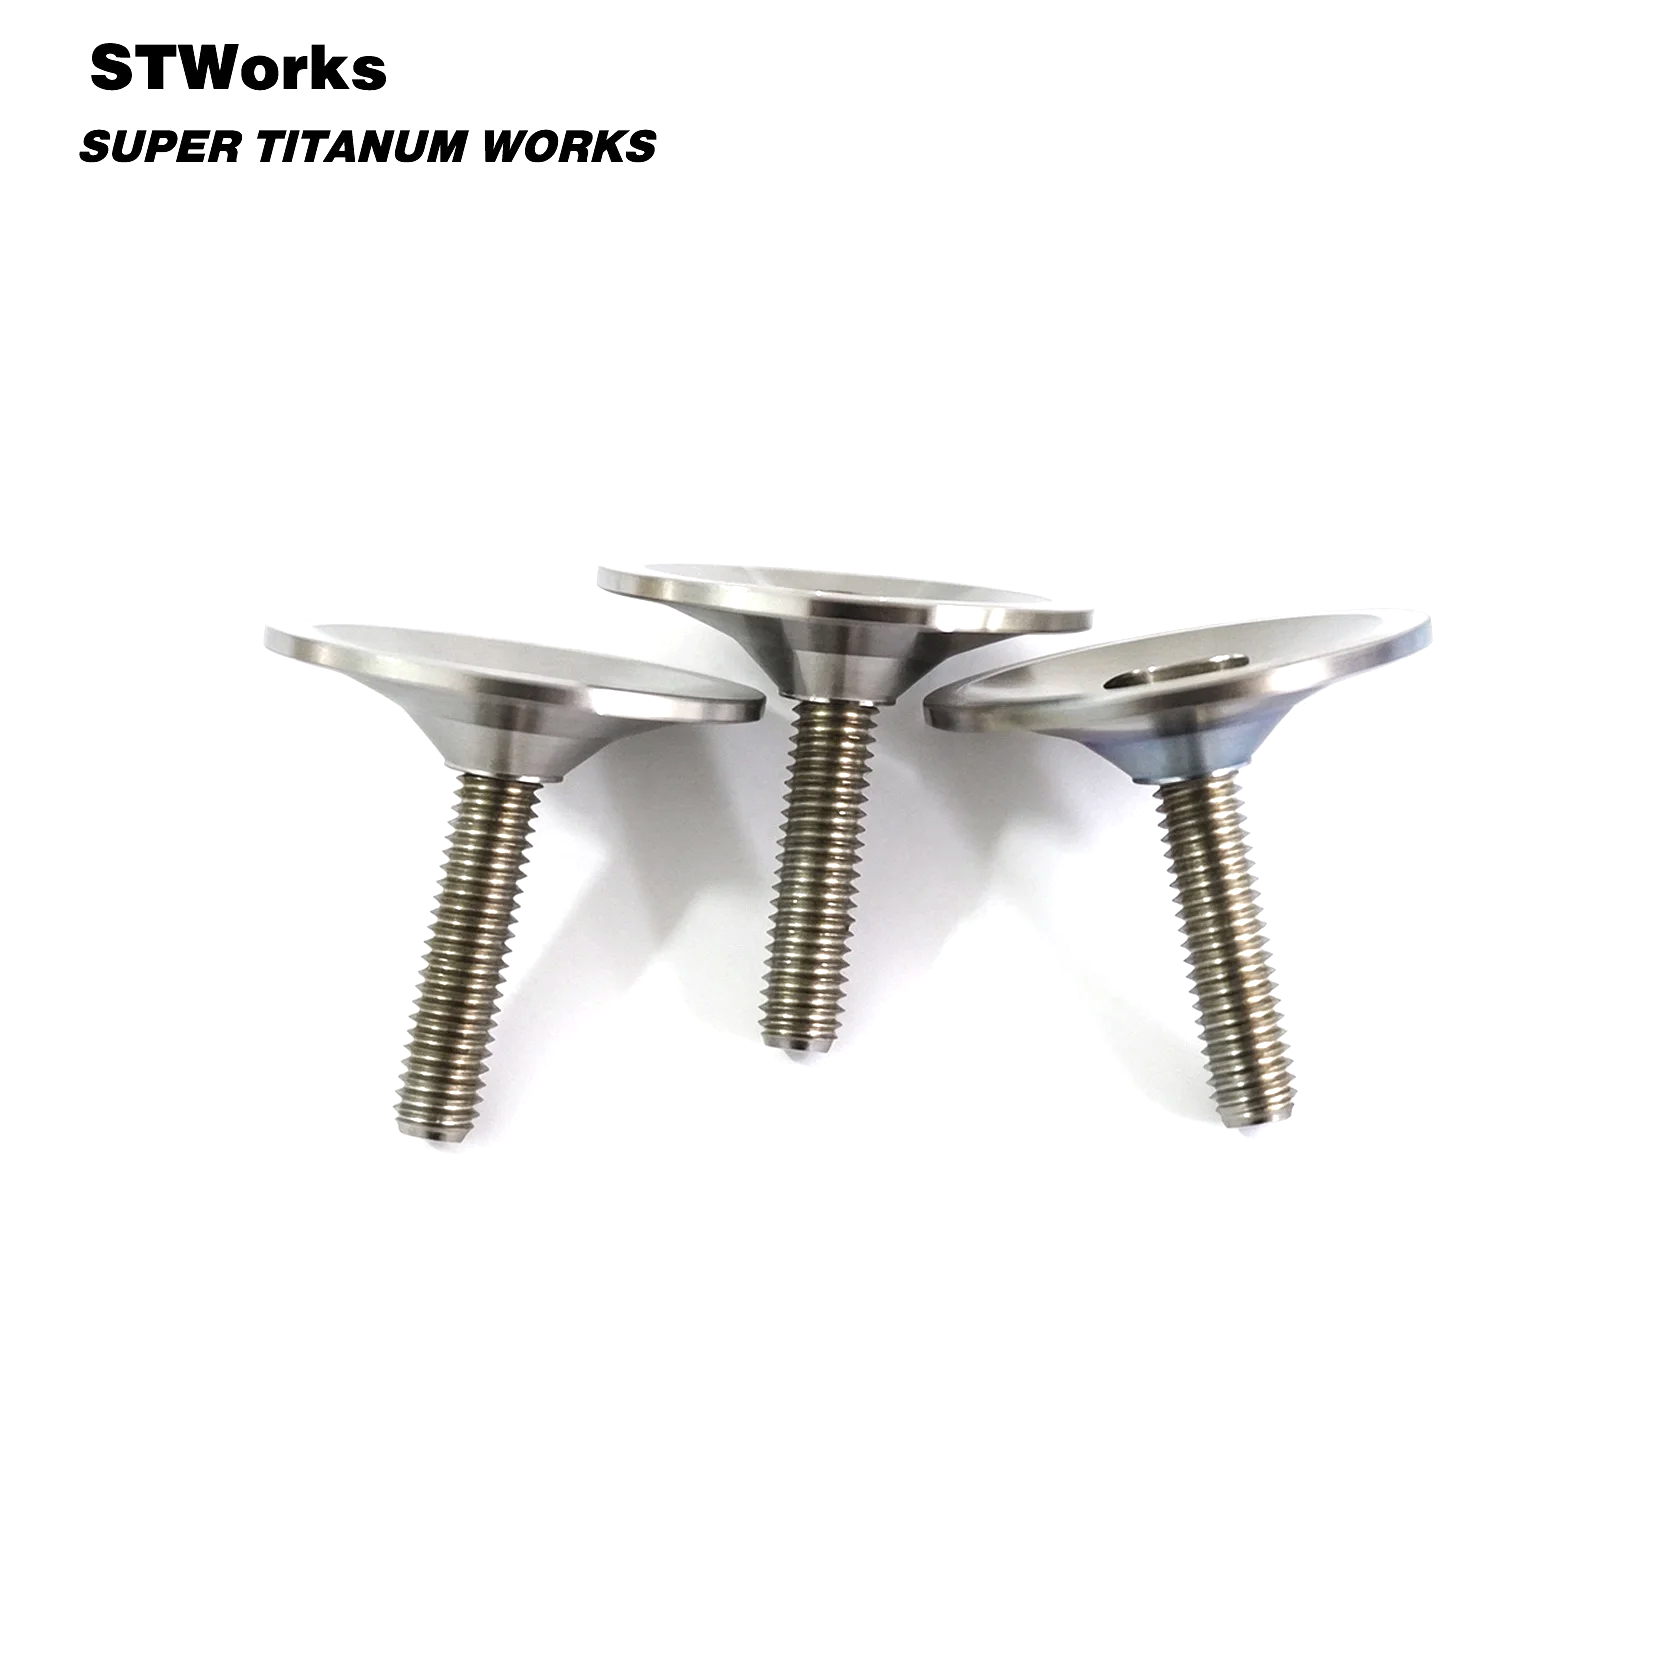
Titanium Bicycle Headset Top Cap CNC M6x30 Bolt
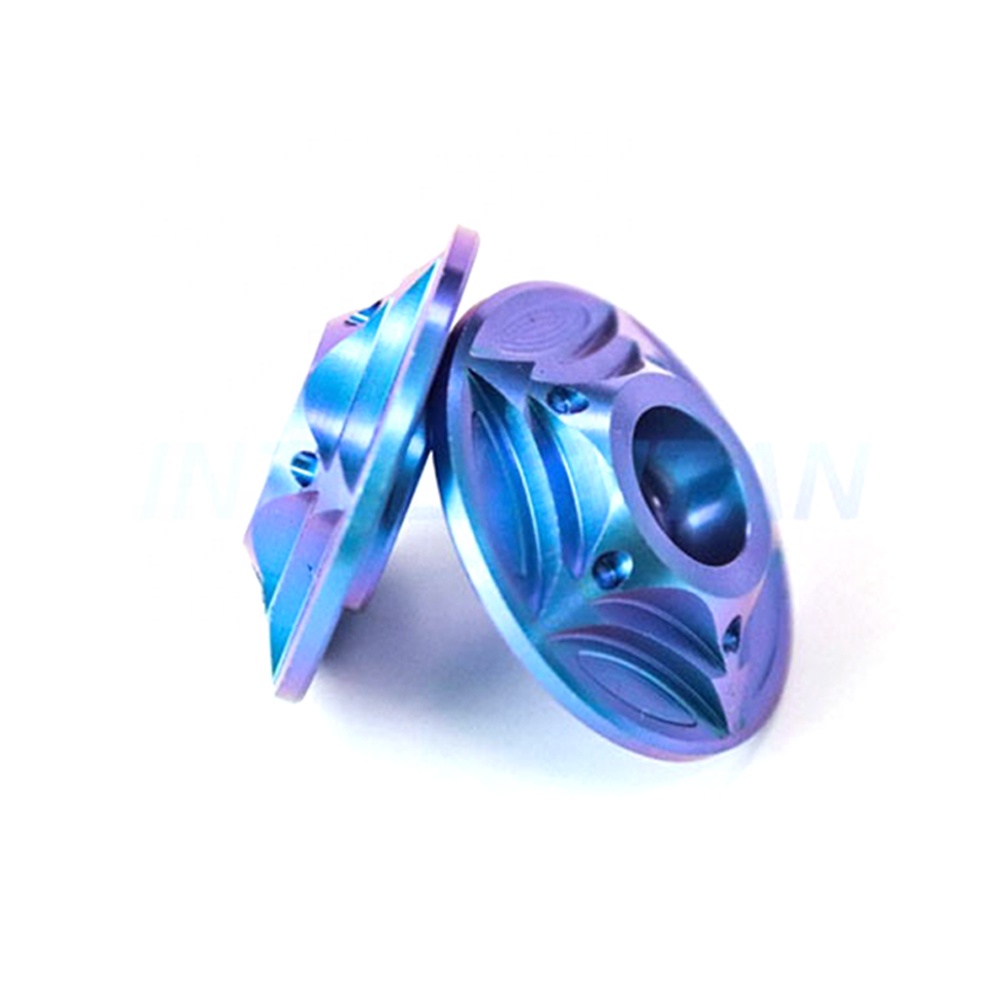
Customized Titanium Alloy Washers PVD Coated M6
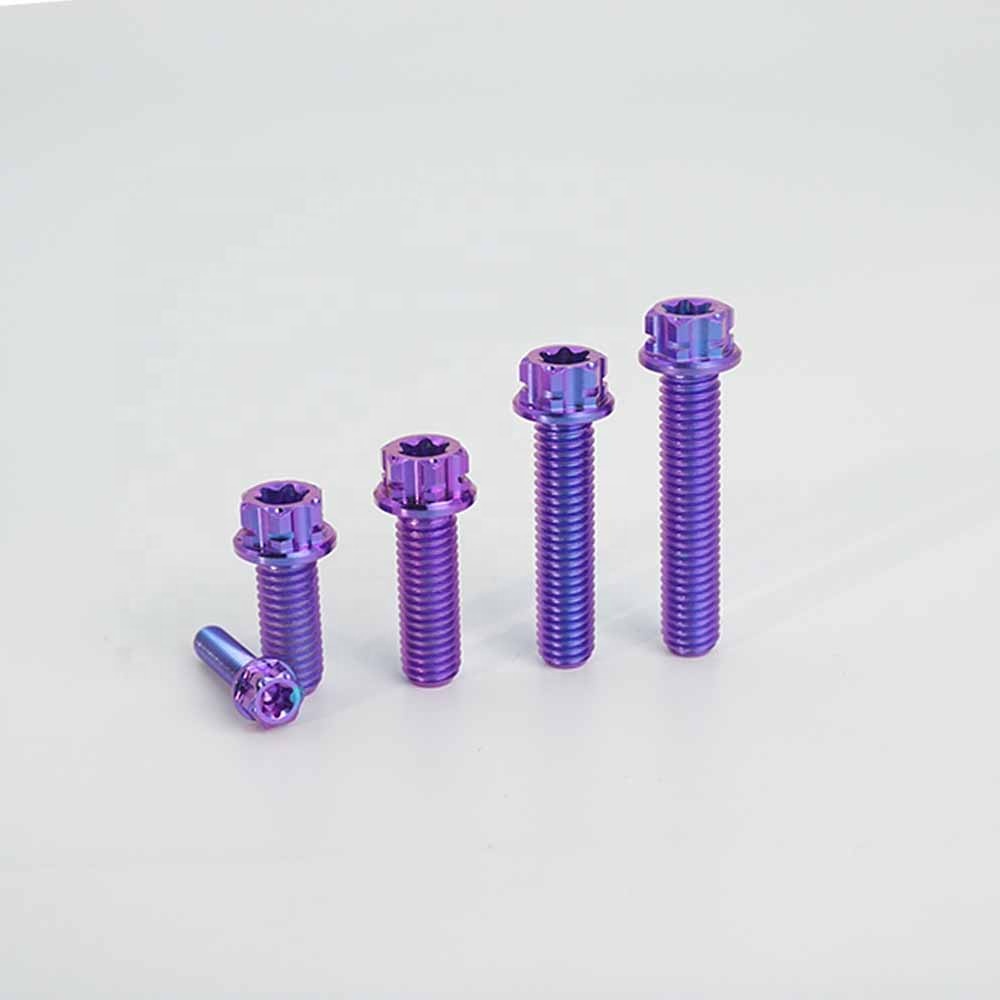
Gr5 Titanium Bolts M6x40 / M6x10 / M8x30 Flange
Executive Technical Brief: High-Pressure Titanium Banjo Fastener Dynamics
In high-performance hydraulic braking and lubrication circuits, the titanium banjo bolt is not merely a fastening element; it is an active pressure vessel subjected to complex multiaxial stress tensors. Unlike solid shank bolts whose primary design criterion is axial clamping force, a banjo bolt incorporates an internal axial fluid bore intersecting perpendicular radial cross-drilled discharge ports. This geometry induces acute stress concentration factors ($K_t$) precisely along the intersection edges of the fluid passages.
Under aggressive operational environments—such as MotoGP, Formula 1, endurance superbike racing, and aerospace actuator couplings—transient hydraulic shock waves can exceed 280 bar (4,060 PSI), coupled with thermal spikes beyond 220°C transmitted directly from brake caliper bodies. When traditional carbon steel or stainless steel hardware is deployed, it imposes an unacceptable unsprung mass penalty. Conversely, 7075-T6 aluminum alternatives frequently suffer catastrophic shear degradation and fatigue-induced thread creep under high pre-load torques.
Industrial procurement teams increasingly mandate Grade 5 Titanium (Ti-6Al-4V, UNS R56400 / TC4) as the quintessential standard. Possessing an exceptional strength-to-weight ratio (density of 4.43 g/cm³ versus 7.85 g/cm³ for steel), a yield strength exceeding 830 MPa, and immunity to chloride-induced pitting and DOT 4/5.1 glycol brake fluid oxidation, Ti-6Al-4V delivers fail-safe structural resilience. However, realizing these theoretical benefits requires extreme manufacturing discipline: single-point or rolled threads under strict dimensional control, thermal micro-deburring at interior cross-hole intersections to prevent notch-induced fatigue crack initiation, and advanced physical vapor deposition (PVD) to counteract titanium's native propensity toward galling during torquing sequences.
Top 10 Titanium Banjo Bolts Manufacturers & Factories
A rigorous metallurgical, dimensional precision, and OEM production capacity evaluation of the world's foremost fluid transfer hardware manufacturers.
Operating out of Baoji's Precision Manufacturing Park, Velnora leverages direct access to high-purity aerospace-grade Ti-6Al-4V ingots. Specializing in high-precision 5-axis Swiss CNC turning, cold thread rolling, and Wire EDM, Velnora manufactures M10x1.0, M10x1.25, and M8 single/double titanium banjo bolts with ultra-low micro-finish internal bores (Ra ≤ 0.4 μm).
Velnora's standout competitive edge is complete buyer transparency: providing in-situ CNC machining video feeds, optical profile dimension checks, spectrometer material validation, and rapid customized engineering turnarounds with an average response time of ≤ 4 hours.
Pro-Bolt is universally recognized in professional motorsport paddocks (Moto2, WorldSBK). Their titanium banjo bolts are machined from high-tensile aircraft-spec titanium billets, featuring pre-drilled hex flanges for race-regulation lock-wiring.
They maintain massive distribution hubs across Europe and North America, offering rapid off-the-shelf fulfillment for standard catalog metric thread pitches with high-end polished, blue, and black DLC coatings.
Racebolt is a dedicated UK manufacturer managing the entire component lifecycle from in-house multi-axis turning to finish inspection. Their titanium banjo line utilizes proprietary rolled-thread forming post heat treatment, delivering superior fatigue endurance in severe vibration environments.
Widely preferred by custom racing builders for bespoke dimensional profiles, including extended shank lengths accommodating proprietary dual-line aftermarket master cylinders.
As a legacy fluid system integrator for Formula 1 and defense hydraulics, Goodridge supplies complete turnkey systems comprising hoses, fittings, and matching titanium banjo fasteners. Their banjo bolts undergo rigorous hydrostatic burst testing exceeding 700 bar.
Ideal for defense and enterprise-level motorsport contractors requiring unified fluid dynamic warranties across couplings, olive inserts, and retaining bolts.
Operating advanced automated Star CNC sliding head lathes, HEL Performance produces titanium and stainless steel fluid routing hardware directly alongside their brake caliper and master cylinder product lines.
Their titanium banjo bolts focus heavily on flow-channel hydrodynamic radiusing, minimizing turbulence within hydraulic brake lines during violent antilock and emergency threshold braking cycles.
Pioneers of military surplus AN fluid architecture in high-output American racing, Earl's supplies titanium banjo bolts adapted for AN-3 and AN-4 micro-lines, dry-sump oil circuits, and extreme turbocharger cooling lines.
Engineered to withstand prolonged contact with aggressive synthetic esters, nitromethane blends, and elevated operational fluid temperatures up to 260°C without structural yielding.
Ticon Industries focuses exclusively on titanium manufacturing for motorsports. Their titanium banjo bolts and associated welded fluid bungs serve high-end time-attack, drifting, and marine offshore powerboat applications.
Their components emphasize clean metallurgical grain structures, superior laser mark traceability, and an extensive array of hard-anodized and raw bead-blasted surface options.
Ti64 bridges the gap between cold heading/forging and precision CNC post-machining. By pre-forging head profiles, continuous grain flow is preserved around the head-to-shank transition, significantly bolstering fatigue life against high cyclic line pressure pulses.
Favored in off-road trophy trucks and rally vehicles where severe chassis twisting forces impose heavy bending moments on rigid brake line unions.
Engineering premium aftermarket accessories for Japanese OEM dirt and dual-sport platforms (Honda, Yamaha, Kawasaki, Suzuki), ZETA manufactures ultra-lightweight titanium banjo bolts featuring scalloped hex head designs to shed every milligram of unsprung mass.
Features extremely precise thread tolerance bands (±0.015mm) engineered to interface flawlessly with cast aluminum master cylinders without stripping soft internal caliper threads.
Lunsford is an authoritative domestic US manufacturer of small-bore and micro-tolerance titanium fasteners. Their capabilities extend into specialized micro-banjo hardware utilized in drone telemetry hydraulics, robotic actuators, and karting braking systems.
Exceptional competency in machining Grade 5 titanium at diminutive dimensions (M4 to M8) where internal bore drilling without wall deflection is extraordinarily challenging.
Technical Capability Matrix: Global Banjo Bolt Production
Direct comparison of critical metallurgical standards, threading technology, burst rating, and quality control protocols.
| Manufacturer | Primary Material | Thread Forming Process | Burst Pressure Limit | Cross-Hole Deburring | In-Process Video QA | Standard Lead Time |
|---|---|---|---|---|---|---|
| Velnora Titanium | Certified Ti-6Al-4V Gr5 / TC4 | Cold Rolled (Post-Heat) | ≥ 480 bar (6,960 PSI) | Thermal & Micro-Electropolish | Yes (Mandatory) | 7–15 Days (Custom OEM) |
| Pro-Bolt UK | Aircraft Grade Titanium Billet | Single-Point Cut / Rolled | ≥ 420 bar (6,090 PSI) | Rotary Mechanical Clean | On Special Request | Stock / 21 Days Bespoke |
| Racebolt UK | Ti-6Al-4V Grade 5 | Precision Thread Rolled | ≥ 450 bar (6,525 PSI) | Automated Rotary Chamfer | No | 14–20 Days |
| Goodridge Ltd | Ti-6Al-4V / 316L Stainless | CNC Formed | ≥ 700 bar (Hydraulic System) | High-Pressure Fluid Jet | Enterprise Tier Only | Stock / Catalog Lead |
| HEL Performance | Billet Grade 5 Titanium | High-Speed Single-Point | ≥ 400 bar (5,800 PSI) | Dual Axis Radius Cut | No | Stock Distribution |
| Ti64 Superlite | Forged Head + Ti-6Al-4V | Rolled Threads | ≥ 460 bar (6,670 PSI) | Vibratory Tumble Polish | No | 15–30 Days |
Strategic Sourcing: Future Trends in Titanium Fluid Fasteners
Industrial procurement departments navigating the transition toward next-generation electric vehicles (EVs), lightweight hydrogen transport, and extreme motorsport platforms face fundamental shifts in supply chain architectures. Sourcing titanium banjo hardware requires moving past localized distributors toward direct factory integration:
Integrated Sensor & Telemetry Ports
Modern regenerative braking systems demand real-time hydraulic pressure transducers. Banjo bolts are evolving to feature integrated micro-sensor tapings directly within the bolt head, requiring advanced 5-axis Swiss-lathe concentricity to prevent hydraulic leakage under extreme transducer cycling.
Raw Material Geopolitics & Baoji Agglomeration
With Western titanium ingot processing strained by aerospace demand spikes, B2B buyers are bypassing intermediary brand markups to contract directly with manufacturers rooted in China's "Titanium Valley" (Baoji), securing guaranteed alloy pedigree, stable ingot supply, and direct price-per-kilogram manufacturing parity.
Digital Proof-of-Production Audits
Procurement teams are shifting away from static PDF Mill Test Reports (MTRs) which can be falsified. The new procurement standard demands verifiable digital proof—including live optical coordinate measuring (CMM) data, spectrometer elemental breakdown videos, and real-time machine run footage before shipment authorization.
Metallurgical Innovations: Advancing Failure-Free Banjo Joint Integrity
The mechanical failure of a titanium banjo bolt in a hydraulic circuit typically manifests via two distinct vectors: fatigue rupture at the fluid cross-hole junction and thread seizure or thread stripping due to galling. Recent breakthroughs in precision manufacturing have introduced advanced engineering remedies:
Cold Thread Rolling vs. Single-Point Cutting
Single-point cutting shears through the natural austenitic/alpha-beta grains of Ti-6Al-4V, generating microscopic surface notches that act as stress risers. Modern high-integrity banjo bolts mandate cold thread rolling after solution treating and aging (STA). Rolling deforms the material plastically, compressing grain lines along the thread profile, boosting root hardness by up to 15%, and increasing fatigue cycle endurance by over 300%.
Hydro-Erosion and Thermal Deburring
When cross-drilling radial fluid ports into the main hollow core, burrs inevitably form on internal intersecting shoulders. Left unaddressed, these burrs detach, causing catastrophic brake caliper seal scoring. Leading manufacturers now deploy abrasive hydro-flow polishing or thermal energy deburring to radius interior intersecting junctions, simultaneously smoothing fluid transitions and mitigating the $K_t$ notch effect.
Advanced PVD Physical Vapor Deposition
Titanium has a poor coefficient of friction against aluminum calipers, resulting in severe cold-welding (galling) when tightened dry. While copper anti-seize paste was historically mandatory, next-generation banjo bolts apply sub-micron Diamond-Like Carbon (DLC) or Titanium Nitride (TiN) via magnetron sputtering. This produces a micro-hardness exceeding 2,500 HV with a friction coefficient under 0.15, eliminating galling entirely.
Why Global Sourcing Directors Partner with Velnora
Headquartered in the epicenter of China's titanium supply chain (Baoji), Velnora Titanium Industry Co., Ltd. eliminates middleman volatility. Since 2013, our specialist engineering facility has provided end-to-end contract manufacturing for international distributors, hypercar constructors, superbike racing teams, and medical robotics firms.
- Aerospace-Grade Certified Gr5 Ti-6Al-4V (TC4)
- High-Speed 5-Axis Swiss Lathes & Wire EDM
- Full Dimensional Reports to DIN, ISO, JIS Standards
- Mandatory Live Production Inspection Videos
- Comprehensive PVD Coating: Black, Gold, Rainbow
- Rapid CAD/Drawings Technical Quotations (≤4 Hours)
Initiate an OEM Engineering Review
Upload your STEP, IGES, or PDF blueprints for direct analysis by our metallurgical machinists.
Send an InquiryFrequently Asked Questions: Sourcing Titanium Banjo Bolts
Direct technical guidance addressing torque recalculation, sealing ring compatibility, and fluid shear stresses.
Ready to Upgrade Your Hydraulic Fastener Supply Chain?
Connect directly with Velnora Titanium's engineering shop floor in Baoji, China. Receive drawing reviews, material composition reports, custom batch pricing, and verified CNC production video timelines.