Essential Titanium Knife Hardware & CNC Turning Components
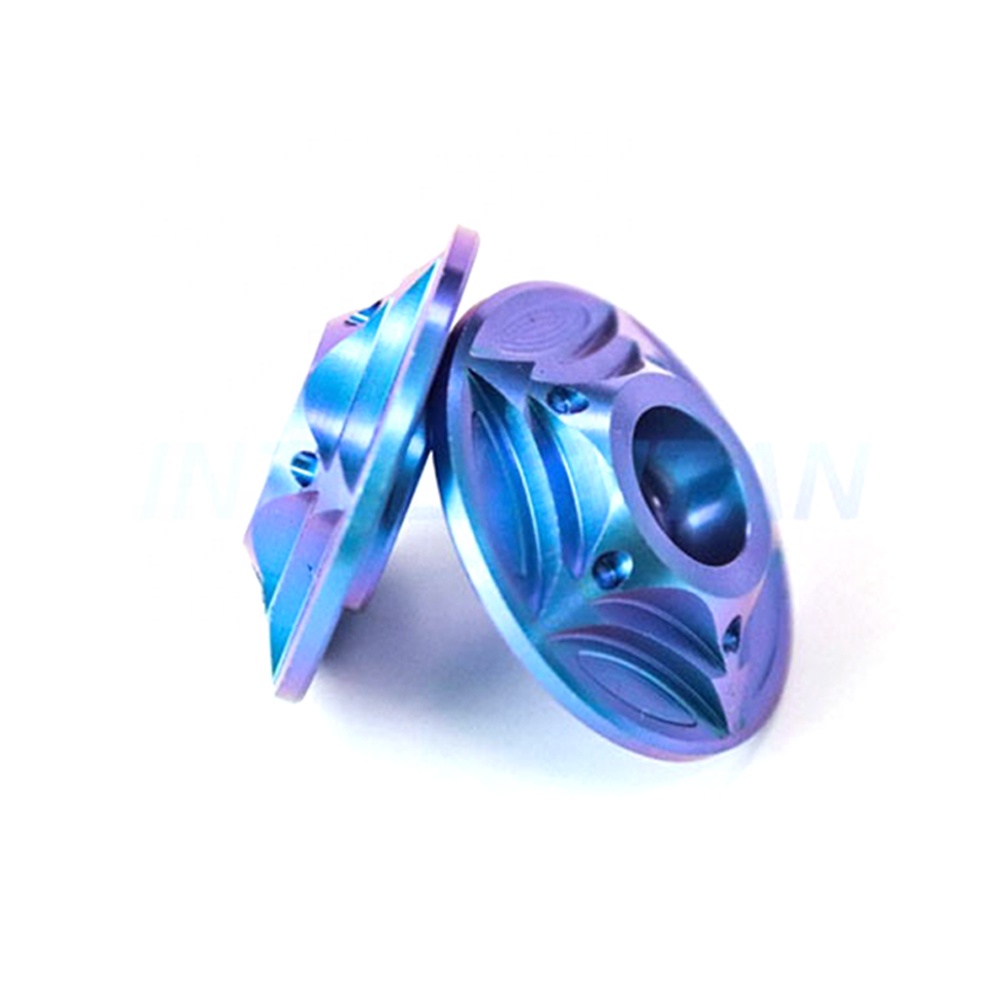
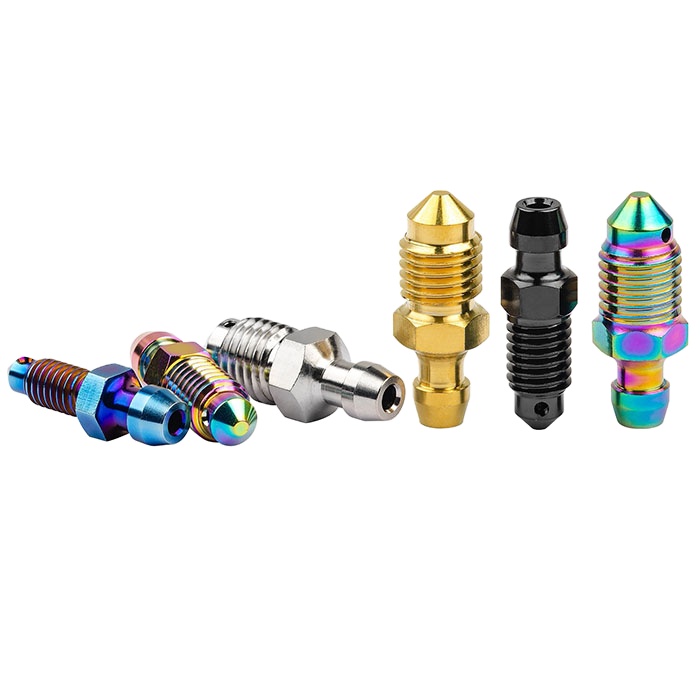
Every custom Timascus knife scale assembly requires micron-accurate fasteners, pivots, and precision hardware. Explore our flagship Grade 5 titanium machined components directly produced in our Baoji facility.

The Metallurgy of Timascus (Titanium Damascus) Knife Scales
Understanding solid-state diffusion bonding, recrystallization dynamics, and high-precision CAD/CAM contour milling for bespoke cutlery manufacturing.
Solid-State Diffusion Bonding
Authentic Timascus (also known as Mokuti or layered titanium) is not forged using liquid flux or brazing alloys. It requires alternating stacks of commercially pure Grade 2 titanium and high-tensile Grade 5 (Ti-6Al-4V) titanium, hermetically enclosed in an oxygen-free vacuum canister. Under Hot Isostatic Pressing (HIP) at temperatures exceeding 900°C and pressures above 100 MPa, atomic lattice migration occurs across grain boundaries without melting. The result is a monolithic billet that eliminates delamination risks during CNC high-speed end milling.
Optical Wave Interference Coloration
Unlike steel Damascus that relies on corrosive acid ferric chloride etching for contrast, Timascus achieves vibrant patterns through light interference via titanium dioxide (TiO2) film growth. Grade 2 and Grade 5 titanium possess distinct electrochemical oxidation potentials. When heated or electrically anodized at specific direct currents (20V to 110V), the oxide layer thicknesses differ across alternating strata. Incoming ambient light splits: one portion reflects from the top oxide boundary, another from the metallic substrate below, producing vivid chromatic patterns.
5-Axis CNC Precision & 3D Topography
To reveal the internal damascene woodgrain, raindrop, basketweave, or twist patterns, the scale surface must be contoured using ball-end carbide cutters or 3D high-speed toolpaths. Slicing through the layered strata exposes diagonal layer intersections. Our 5-axis machining centers maintain strict tolerances (±0.005 mm) on interior pivot basins, weight-relief pockets, detent ball runways, and lock-bar reliefs, ensuring smooth integration with folder liners and framelock systems.
Years in Precision Titanium
CNC Milling Tolerance
Global Knife & EDC Clients
Ultrasonic Flaw Inspected
Engineering Matrix: Timascus vs. Traditional Handle Scale Materials
Data-driven performance metrics for cutlery design engineers and production procurement managers evaluating mechanical rigidity, weight distribution, and cosmetic stability.
| Material Type | Alloy Strata Composition | Density (g/cm³) | Tensile Strength (MPa) | Corrosion Resistance | Finishing & Oxidation Behavior | Primary Industrial Use Case |
|---|---|---|---|---|---|---|
| Bimetal Timascus (Mokuti) | Ti Grade 2 + Ti Grade 5 (TC4) | 4.46 | 650 – 895 | Complete resistance to sweat/saltwater | Heat tinting (flame) & electrochemical anodizing | Luxury custom knife scales, bolsters, EDC clips |
| Tri-Metal Timascus | Ti Gr2 + Ti Gr5 + Ti Gr7 / Gr9 | 4.48 | 720 – 910 | Impervious to harsh marine environments | Tri-color spectrum (electric blue, amethyst, yellow-gold) | Ultra-premium knife scales, collector pens, bezels |
| ZircuTi (Zirconium-Ti) | Ti-6Al-4V + Pure Zirconium 702 | 5.35 | 580 – 820 | Exceptional acid and atmospheric stability | Deep lustrous jet-black alternating with neon Ti hues | High-contrast tactical folders, thumb studs, inlays |
| Pure Ti-6Al-4V (Grade 5) | Single phase α-β Titanium | 4.43 | ≈ 895 | Excellent ASTM B117 salt spray ratings | Uniform monochrome anodization or PVD hard coating | Framelock structural slabs, liners, internal frames |
| Aerospace 6061-T6 Aluminum | Al-Mg-Si Alloy | 2.70 | ≈ 310 | Moderate (requires Type III Hardcoat Anodizing) | Dye-based sulfuric anodizing; easily scratches to white | Mass production lightweight tactical folders |
| Carbon Fiber (3D Prepreg) | PAN Fiber + Epoxy Resin | 1.55 | ≈ 600 | Inert chemical matrix; susceptible to UV yellowing | Mechanical polishing only; no chromatic interference | Lightweight hunting knives, featherweight folders |
Future Procurement Trends for OEM/ODM Timascus Knife Scales (2025–2030)
Strategic insights for brand buyers, knife manufacturers, and sourcing directors adapting to evolving consumer aesthetics and advanced supply chain dynamics.
1. Transition to Factory Mid-Tech Runs
Historically limited to independent one-off custom makers, production cutlery brands are now incorporating Timascus into factory mid-tech series (100–1,000 units). Production facilities must provide tight consistency in layer distribution and billet thickness to facilitate standardized CAM programs across serial manufacturing.
2. Direct Sourcing from Baoji Clusters
Global cutlery enterprises are eliminating multi-tier trading brokers by establishing direct OEM partnerships in Baoji, China's Titanium Valley. Direct procurement guarantees raw material ingot traceability, mill test certificates (MTC), ultrasonic integrity verification, and lower kerf waste costs for finished scales.
3. Near-Net-Shape Wire EDM Preforms
Due to the premium cost of Timascus stock, standard subtractive machining from solid rectangular slabs produces 50–70% swarf waste. Modern procurement strategies utilize high-speed wire EDM profile blanks cut nested from master diffusion-bonded blocks, slashing raw stock scrap rates and machining cycle times.
4. Multi-Material Laminate Composites
Emerging market demand favors hybrid combinations, including Timascus-bolstered carbon fiber slabs and ZircuTi layered pivot assemblies. Sourcing teams are standardizing multi-axis indexable tooling to handle varying material machinabilities in one coordinated handle setup.
Manufacturing Evolution: Next-Gen Damascus Engineering
How precision metallurgy, robotic micro-milling, and precise electrochemical controls are transforming custom knife scale production.
Vacuum HIP Ingot Synthesis
Traditional manual forge-welding of titanium risks atmospheric alpha-case embrittlement and catastrophic layer separation under machining stress. Next-generation Timascus production utilizes automated industrial Hot Isostatic Pressing chambers. billets are evacuated under 10⁻⁴ Torr vacuum and forged under uniform gas-hydraulic pressure, creating complete atomic grain cohesion across the Gr2/Gr5 boundary.
Computer-Controlled Voltage Anodization
While artisan flame torching produces artistic, organic temper colors, commercial knife batches demand precise repeatability. Automated multi-tank anodization plants apply voltage control to 0.1V precision, ensuring that the 18V bronze, 28V royal blue, 58V gold, and 72V violet tones match across hundreds of handle scales.
Pyrophoric Swarf & Toolpath Science
Fine titanium and zirconium dust generated during scale contouring is pyrophoric. Modern CNC facilities deploy high-pressure flooded chilled synthetic coolant systems paired with diamond-like carbon (DLC) coated micro-grain carbide tools. This eliminates tool wear while maintaining high-luster finishes without micro-burrs in detent holes.
Velnora Titanium Industry: The OEM/ODM Manufacturing Benchmark
Headquartered in Baoji, China's Titanium Valley, since 2013. We bridge heavy metallurgical capabilities with artisan-grade CNC cutlery craftsmanship.
Titanium Valley Supply Chain
Immediate access to 80% of China's certified titanium sponge, vacuum arc remelting facilities, and plate rolling mills. We secure prime Grade 5 and Grade 2 certified feedstock with full batch traceability and zero scrap-metal adulteration.
Engineer-Led DFM Reviews
No non-technical intermediaries. Sourcing directors speak directly with CAM programmers and metallurgical engineers. We evaluate your 3D CAD models (STEP, IGES, SolidWorks) to optimize weight-relief pockets, stop-pin holes, and pivot chamfers within 4 business hours.
In-Process Live Video Verification
Total production transparency. We dispatch high-definition machining clips and macro photographic inspections during every stage: from billet wire EDM slicing to final 5-axis sculpting and anodic color treatment, keeping your QA team informed.
Flexible Scalability (From 1 to 5,000 Pcs)
Whether you require a single pair of bespoke Timascus handle scales for an award submission or mass-machined production batches for a commercial folding knife lineup, our dual-cell workshop accommodates both custom and volume OEM production.
Frequently Asked Questions by Cutlery Engineers & Buyers
Clear, authoritative technical answers regarding Timascus raw materials, machining speeds, thread galling mitigation, and custom knife scale tolerances.
What is the metallurgical difference between Timascus, Mokuti, and ZircuTi?
Timascus and Mokuti are industry terms referring to diffusion-bonded laminates composed of different titanium grades (most commonly Grade 2 commercially pure titanium paired with Grade 5 Ti-6Al-4V). Because the two alloys oxidize at varying rates, heat or anodization produces vibrant multi-colored patterns. ZircuTi introduces pure Zirconium (Zr 702) into the titanium matrix. When subjected to thermal oxidation, the zirconium layers turn an opaque, lustrous jet-black, providing striking contrast against the vivid anodized titanium strata.
Can Timascus be tapped for standard knife clip and pivot screws without stripping?
Yes, provided correct thread design guidelines are observed. Grade 2 layers in the laminate are softer than pure Grade 5. When tapping blind micro-holes (e.g., 2-56 UNC, M2, or M2.5) for pocket clips, we recommend maintaining thread engagement lengths at 1.8 to 2.2 times the major screw diameter. For extreme mechanical stress points, we integrate Grade 5 titanium threaded bushings or steel thread inserts to guarantee lifetime torque reliability.
How do you prevent warpage when CNC milling thin, asymmetric knife scales?
Titanium Damascus retains internal residual stresses from the diffusion bonding and hot rolling cycles. To eliminate bowing or warping during high-speed pocketing, Velnora subjects all billet blanks to a vacuum stress-relief annealing cycle (650°C for 2 hours with controlled furnace cooling) prior to machining. Furthermore, our CAM programs employ balanced two-sided roughing toolpaths, alternating cuts between internal weight-relief pockets and external 3D contours.
Can you machine custom internal cavities for nested liner locks and ball bearings?
Yes. Our precision 5-axis vertical machining centers maintain tight dimensional accuracy (±0.005 mm). We regularly mill intricate internal nesting pockets for stainless steel lock plates, ceramic detent ball channels, counterbored pivot races, and multi-tier caged ball bearings, ensuring drop-shut knife action right out of the box.
What surface finishes can be applied to Timascus knife scales before coloration?
We provide four standardized base surface finishes: Mirror Polished (yielding intense, glassy chromatic reflections), Satin Hand-Rubbed (delivering crisp, directional contrast favored by custom knifemakers), Ceramic Micro-Bead Blasted (yielding soft, muted pastel tones with an anti-slip tactile feel), and Acid Etched Topography (utilizing a mild fluorinated bath to selectively etch Grade 2 strata, creating tactile 3D relief ridges along the pattern lines).
What are the minimum order quantities (MOQ) and production lead times for OEM projects?
For custom knife makers requiring bespoke, one-of-a-kind scales or prototype evaluation pairs, our MOQ starts at just 1 pair. For mid-tech and production knife manufacturers, typical runs range between 50 and 500 sets. Prototype machining and initial sample dispatch typically take 10 to 14 business days, while volume batch runs ship within 20 to 30 days via express air freight (DHL, FedEx, UPS).
Accelerate Your Cutlery Line with Custom Timascus Scales
Whether you have finalized 3D CAD files (STEP/IGES) or require collaborative design-for-manufacturing (DFM) assistance, our engineering team in Baoji Titanium Valley is ready to quote your specifications within 4 business hours.