High-Performance Titanium Hardware & Custom Fastening Systems
Engineered from certified aerospace-grade raw stock with in-house CNC turning, thread cold rolling, and precision surface treatments to ISO, DIN, and aerospace benchmarks.
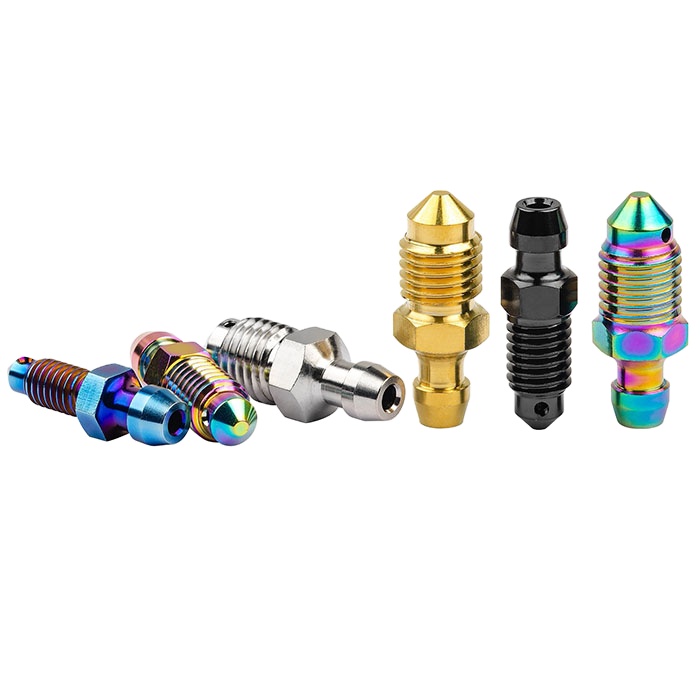

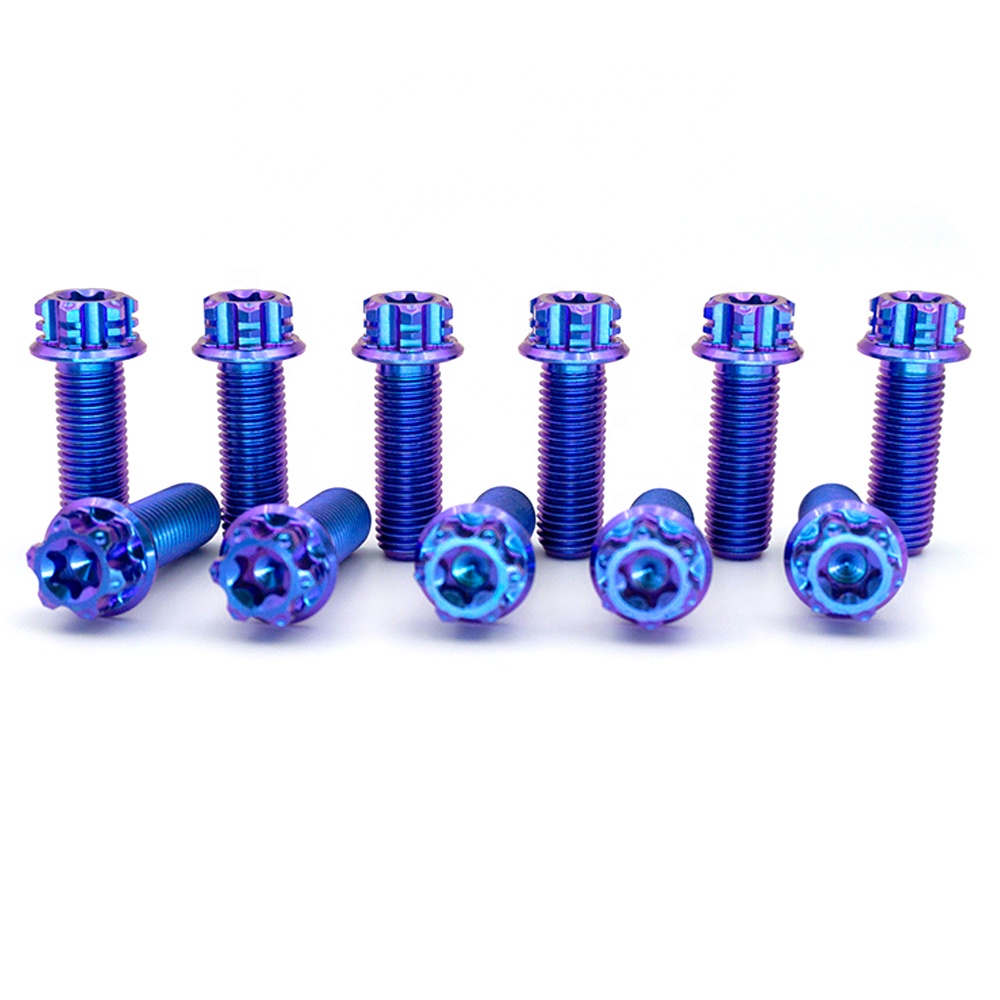
The Architecture of Titanium Blind Rivets: Why Grade 5 and Pure Titanium Dominate Critical Joints
In aerospace structures, advanced automotive chassis, and hyper-corrosive marine environments, standard aluminum or stainless steel blind rivets (pop rivets) often suffer mechanical failure, thermal distortion, or severe galvanic incompatibility. Sourcing engineers require structural blind fasteners capable of delivering high ultimate shear and tensile strength while minimizing parasitic airframe weight.
Dual-Component Blind Rivet Mechanics
A precision titanium blind rivet consists of two engineered elements: the tubular sleeve (body) and the internal mandrel (stem). In standard aerospace blind rivet assemblies (such as NAS1919 and NAS1921 standards), the sleeve is cold-upset or expanded against the blind side of the workpieces by pulling the mandrel head into the sleeve shank.
Our Baoji manufacturing facility executes cold-heading on vacuum-annealed Ti Grade 2 or Grade 5 titanium wire. Because titanium features a lower modulus of elasticity (~114 GPa) compared to carbon steel (~210 GPa), our mandrels are precision-machined with a micro-engineered break-neck groove that snaps at precise tensile loads, guaranteeing uniform clamping force without crushing sensitive composite laminates.
Galvanic Compatibility with Carbon Fiber (CFRP)
Carbon fiber is electrically conductive and possesses a noble standard electrode potential (+0.25V). When aluminum alloys (-0.90V) or standard carbon steels (-0.60V) are fastened through CFRP panels in humid, saline atmospheres, rapid galvanic cell degradation corrodes the fastener shank, causing joint loss.
Titanium naturally establishes a stable passive surface oxide film ($TiO_2$), exhibiting an electrode potential (+0.10V to +0.20V) virtually identical to graphite fibers. Titanium blind rivets represent the worldwide standard for uninsulated, weight-saving direct insertion into aerospace composite skins and nacelles.
Fastener Material Performance Matrix
| Fastener Grade / Alloy | Density (g/cm³) | Tensile Strength (MPa) | Shear Strength (MPa) | CFRP Galvanic Coupling | Max Operating Temp |
|---|---|---|---|---|---|
| Ti-6Al-4V (Grade 5 / TC4) | 4.43 | 950 – 1050 | ≥ 580 | Zero Galvanic Corrosion | 400°C (752°F) |
| Commercially Pure Ti (Grade 2) | 4.51 | 450 – 550 | ≥ 310 | Zero Galvanic Corrosion | 315°C (600°F) |
| A286 Stainless Steel | 7.92 | 900 – 1000 | ≥ 550 | Low Risk (Requires Sealant) | 650°C (1200°F) |
| Monel 400 (Ni-Cu Alloy) | 8.80 | 550 – 620 | ≥ 340 | Moderate Risk in Saline | 480°C (900°F) |
| 7075-T6 Aluminum | 2.81 | 510 – 540 | ≥ 300 | Severe Galvanic Attack | 120°C (248°F) |
Why Tier-1 OEM Sourcing Teams Partner with Velnora Titanium
Located in the heart of Baoji, Shaanxi—widely recognized as "China's Titanium Valley"—Velnora Titanium Industry Co., Ltd. has delivered precision titanium fasteners and CNC components since 2013 to over 1,000 global buyers.
Integrated CNC & Cold Heading
Equipped with Swiss-type CNC lathes, wire EDM, multi-station cold formers, and rolled-thread machines to ensure precise tolerance margins (down to ±0.005mm) across metric and imperial thread standards.
Raw Material Traceability
Every kilogram of Grade 5 (Ti-6Al-4V) and CP Titanium bar/wire originates from certified vacuum arc remelted (VAR) ingots, complete with Mill Test Certificates (MTC) conforming to EN 10204 3.1 standards.
Visual Verification Dispatch
We eliminate quality ambiguity by recording high-resolution optical inspection photos and production videos for each batch, allowing overseas buyers to audit finished rivets before international dispatch.
Rapid Technical Response
Our dedicated engineering desk provides complete drawing reviews (STEP, IGES, DXF, PDF) within 4 business hours, backed by a 95.7% confirmed response rate across global B2B procurement portals.
Future Procurement Trends in Titanium Blind Fasteners (2025–2030 Outlook)
Industrial procurement is undergoing a paradigm shift driven by aircraft decarbonization, hypersonic atmospheric vehicle design, electric vertical takeoff and landing (eVTOL) crafts, and commercial subsea clean-energy installations. B2B purchasing directors must navigate changing market dynamics to safeguard supply chain resilience.
Transition to Dual-Alloy Sleeves
Procurement specifications increasingly mandate composite blind fasteners with a high-ductility commercially pure titanium (Gr2) sleeve combined with a high-tensile Grade 5 (Ti-6Al-4V) mandrel. This hybrid architecture delivers higher pre-load clamp forces while preventing sleeve fracture during rapid blind-side tulip formation.
Automated Robotic Feed Riveting
With aerospace manufacturing shifting toward automated airframe riveting cells, demand for collated and cartridge-loaded titanium blind rivets is expanding at 14.8% CAGR. Fasteners require tighter stem diameter tolerances (within ±0.015mm) to prevent feed jamming inside high-speed pneumatic robotic end-effectors.
Near-Net-Shape Cold Heading
Traditional CNC lathe turning of titanium blind rivet sleeves generates up to 60% scrap rate. Sourcing managers are shifting contracts toward Chinese manufacturers employing multi-station cold heading and flashless heading techniques, reducing per-unit material costs by 22% to 35% without sacrificing grain structure continuity.
R&D Innovations Driving Next-Generation Titanium Blind Fasteners
How metallurgical advancements in titanium cold deformation, vacuum annealing, and solid dry-film lubrication are solving legacy fastening bottlenecks.
Overcoming Titanium Work-Hardening
Titanium exhibits rapid work-hardening during room-temperature plastic deformation. Advanced Chinese suppliers utilize warm-heading processes (holding wire stock between 250°C and 420°C) coupled with high-vacuum intermediate stress-relief annealing (10⁻⁴ Torr). This prevents micro-cracking at the rivet head junction while preserving internal dislocation density for maximum tensile strength.
Anti-Galling Physical Vapor Deposition (PVD)
Under heavy tensile draw forces, titanium-on-titanium contact surfaces are susceptible to severe frictional galling. Modern production applies aerospace-grade solid-film coatings—including molybdenum disulfide (MoS₂) dry lubricants and Type II sulfuric acid anodization—preventing mandrel binding, ensuring consistent break-stem release, and sealing the joint interface.
Closed-End Hermetic Sealing
For marine exhaust scrubbers, chemical processing vats, and hydrogen energy tank brackets, closed-end (waterproof) titanium blind rivets are replacing standard open-end variants. The rivet sleeve forms a 100% enclosed metal cup around the retained mandrel head, preventing liquid and gas leakage under hydrostatic pressures up to 3.5 MPa.
Frequently Asked Questions: Technical Buyer's Guide
Essential engineering and commercial considerations for purchasing agents sourcing titanium blind rivets and precision fasteners from China.
What are the key standard specifications governing aerospace titanium blind rivets?
Can titanium blind rivets be pulled using standard pneumatic or battery rivet guns?
How do you calculate the correct grip range for titanium blind rivets in composite panels?
What surface treatments prevent titanium galling during high-speed installation?
Why is Baoji the optimal manufacturing cluster for sourcing titanium fasteners?
What are the minimum order quantities (MOQ) and production lead times?
How does Velnora guarantee chemical composition and eliminate interstitial contamination?
Can blind rivets be manufactured with laser engraving or custom color anodization?
Request Technical Drawings, Tolerancing Audits & Samples
Send your STEP, IGES, or PDF specifications directly to our engineering desk in Baoji. Receive metallurgical feasibility feedback, cold-forming analysis, and volume pricing within 4 business hours.