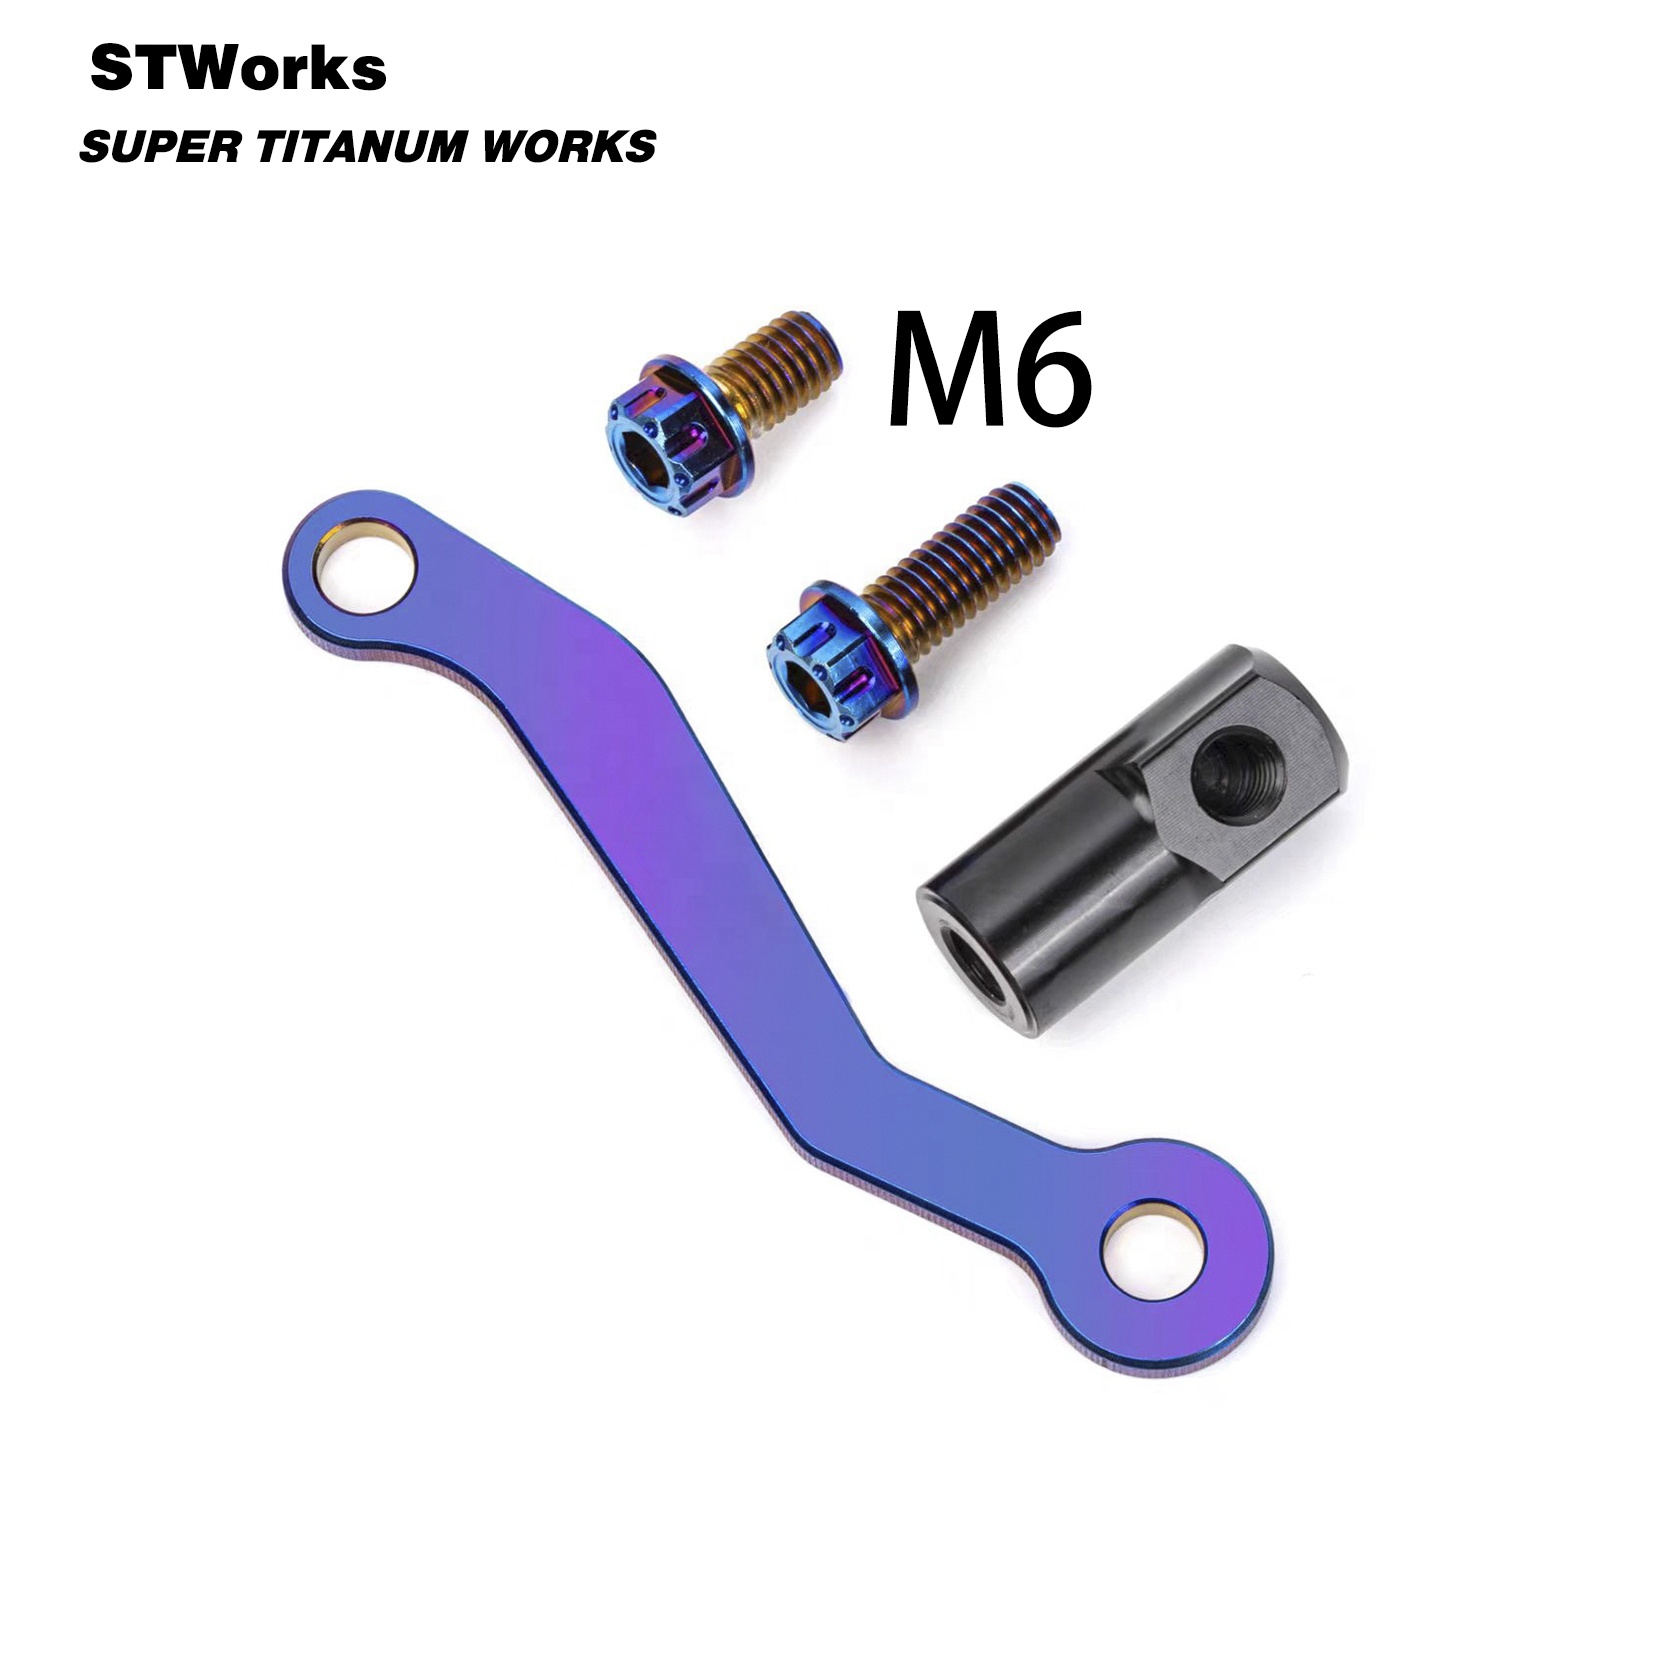
Factory Precision Portfolio
Precision CNC Titanium Fasteners & Hardware Series
Explore our flagship precision-turned components machined directly from certified aerospace bar stock at our Baoji manufacturing complex.

Engineering Whitepaper & Metallurgical Guide
Precision Titanium Acorn Nuts: The Definitive OEM/ODM Sourcing Standard
A comprehensive examination of DIN 1587, JIS B1183, and custom-engineered titanium domed cap fasteners for advanced mechanical assemblies.
In high-performance mechanical systems, structural integrity depends not only on tensile strength but on comprehensive joint protection. Titanium Acorn Nuts (also known as blind cap nuts, domed hex nuts, or crown nuts) represent the ultimate engineering union of mechanical fastening, atmospheric sealing, and visual refinement. Fabricated fundamentally in conformity with DIN 1587, ISO 4032 domed variants, and JIS B1183 standards, these closed-end fasteners shield protruding male threads against oxidation, chemical ingress, mechanical abrasion, and accidental snagging while trimming approximately 44% of mass relative to carbon and austenitic stainless steels.
As the preeminent global manufacturing nexus centered in Baoji—widely acknowledged as China’s "Titanium Valley"—Velnora Titanium Industry Co., Ltd. produces precision-machined titanium acorn nuts that conquer extreme operational stressors. From multi-stage motorsport suspension linkages, subsea robotic housings, and performance superbike cylinder heads to aerospace satellite fairings and high-purity semiconductor cleanroom arrays, our Grade 5 (Ti-6Al-4V) and Grade 2 (CP-Ti) domed fasteners establish the benchmark for mechanical reliability and dimensional accuracy.
Hermetic Blind-Dome Protection
The monolithic solid domed cap seals male stud threads completely from salt-fog, corrosive acids, road brine, and moisture condensation, stopping galvanic oxidation and thread seizure before it begins.
Aerospace Ti-6Al-4V TC4 Alloy
Boasting a baseline tensile yield surpassing 895–950 MPa, our Gr5 alloy provides an exceptional strength-to-weight ratio that easily replaces standard class 8.8 and stainless steel fasteners without joint fatigue.
Swiss Single-Point Threading
Single-point CNC internal threading and controlled blind-hole tapping yield ultra-smooth 6H tolerance class internal threads that resist microscopic galling and ensure flawless torque transfer.
Metallurgical Anatomy: Grade 5 (Ti-6Al-4V) vs. Grade 2 (CP Titanium)
Selecting the appropriate titanium grade represents the primary juncture in procurement. While consumer-grade fasteners frequently compromise by utilizing commercial purity titanium or mixed scrap remelts, structural industrial acorn nuts demand stringent metallurgical selection based on joint dynamics:
- Ti-6Al-4V (Grade 5 / TC4 / UNS R56400): An alpha-beta alloy containing 6% aluminum and 4% vanadium. Possesses a minimum tensile strength of 895 MPa, yield strength of 828 MPa, and hardness of 30–36 HRC. This material is mandatory for dynamic, vibration-heavy environments such as motorcycle rear sprocket assemblies, racing wheel hubs, cylinder head studs, and aerospace linkage caps.
- Commercially Pure Grade 2 Titanium (CP-Ti / UNS R50400): An unalloyed alpha titanium delivering exceptional ductility and yield strength around 275–345 MPa. Its supreme inertness to wet chlorine, organic chlorides, and marine splash zones makes Grade 2 acorn nuts the premier specification for chemical immersion vessels, electroplating racks, architectural cladding, and desalinization valve manifolds.
| Fastener Material | Density (g/cm³) | Tensile Strength (MPa) | Yield Strength (MPa) | Thermal Expansion (µm/m·K) | Marine Corrosion Resistance |
|---|---|---|---|---|---|
| Gr5 Ti-6Al-4V Titanium | 4.43 (Ultralight) | 950 – 1050 | 880 – 920 | 8.6 (Low Expansion) | Immune (Zero Pitting) |
| Gr2 CP Pure Titanium | 4.51 | 345 – 450 | 275 – 350 | 8.6 | Immune (Chemical Grade) |
| 316 Marine Stainless Steel | 8.00 (+80% Weight) | 580 – 680 | 290 – 320 | 16.0 (High Thermal Creep) | Subject to Crevice Corrosion |
| 7075-T6 Billet Aluminum | 2.81 | 510 – 540 | 430 – 480 | 23.4 (Extreme Drift) | Poor (Rapid Galvanic Rot) |
| Class 8.8 High-Tensile Steel | 7.85 | 800 – 830 | 640 – 660 | 11.5 | Severe Rusting without Plating |
*Data represents normalized metallurgical test specimens under laboratory conditions at 20°C. Verified under ASTM B348 and DIN 1587 testing parameters.
DIN 1587 Engineering Dimensional Geometry & Thread Relief Parameters
Unlike through-hole standard hexagon nuts, an acorn nut requires rigorous engineering calculations regarding blind hole depth (t), overall domed height (h), wrench across-flats dimension (s), and cap dome radius (r). A common manufacturing failure among low-tier suppliers is incomplete blind thread tapping: if the male stud bottoms out against an untrapped thread transition or inner dome apex before achieving clamping preload, the joint will suffer catastrophic fatigue loosening.
At Velnora, our multi-axis CNC turn-mill tooling introduces an internal undercut relief recess immediately following the last functional thread pitch. This guarantees 100% full-depth torque engagement across all standard metric threads (M4, M5, M6, M8, M10, M12, M14, M16, M20, M24) and unified imperial threads (1/4-20, 5/16-18, 3/8-16, 1/2-20) conforming strictly to Class 6H and 2B go/no-go plug gauge mandates.
Market Intelligence 2025–2030
Future Procurement Trends for Titanium Acorn Nuts
Strategic purchasing managers are fundamentally pivoting away from fragmented hardware brokers toward integrated, digitally-verified source manufacturers in China.
1. EV Battery & Busbar Sealing
Rapid electrification in commercial logistics and hypercars requires non-magnetic, spark-resistant closed cap nuts to secure high-voltage electrical interconnects and busbars while preventing accidental terminal shorts.
2. Full Batch Traceability (EN 10204 3.1)
Tier-1 procurement directives now demand verified Material Test Reports (MTRs) recording exact chemical heats, oxygen/nitrogen interstitial limits, and ultrasonic test certifications directly from source mills.
3. Integrated Flange Domed Designs
Procurement teams are standardizing on integrated flanged acorn nuts (combining DIN 1587 and DIN 6923), eliminating separate washers, reducing supply chain SKU counts, and accelerating robotic assembly cycles.
4. PVD Thin-Film Anti-Galling Layers
Purchasing agents increasingly favor pre-treated Physical Vapor Deposition (PVD) finishes, such as Diamond-Like Carbon (DLC) and TiN, which eliminate thread galling while providing rich, permanent aesthetics.
Product Evolution & R&D
Technological & Design Trends in Domed Fasteners
How cutting-edge precision tooling, multi-axis machining, and surface metallurgy are transforming simple hardware into engineered structural assets.
Skeletonized & Fluted Racing Domes
For MotoGP and Formula racing teams, every gram counts. Advanced 5-axis simultaneous CNC turning creates scalloped dome contours and weight-relief blind cavities that strip up to 18% additional weight while maintaining structural hoop stress limits.
Interference Oxide Anodizing (Color Science)
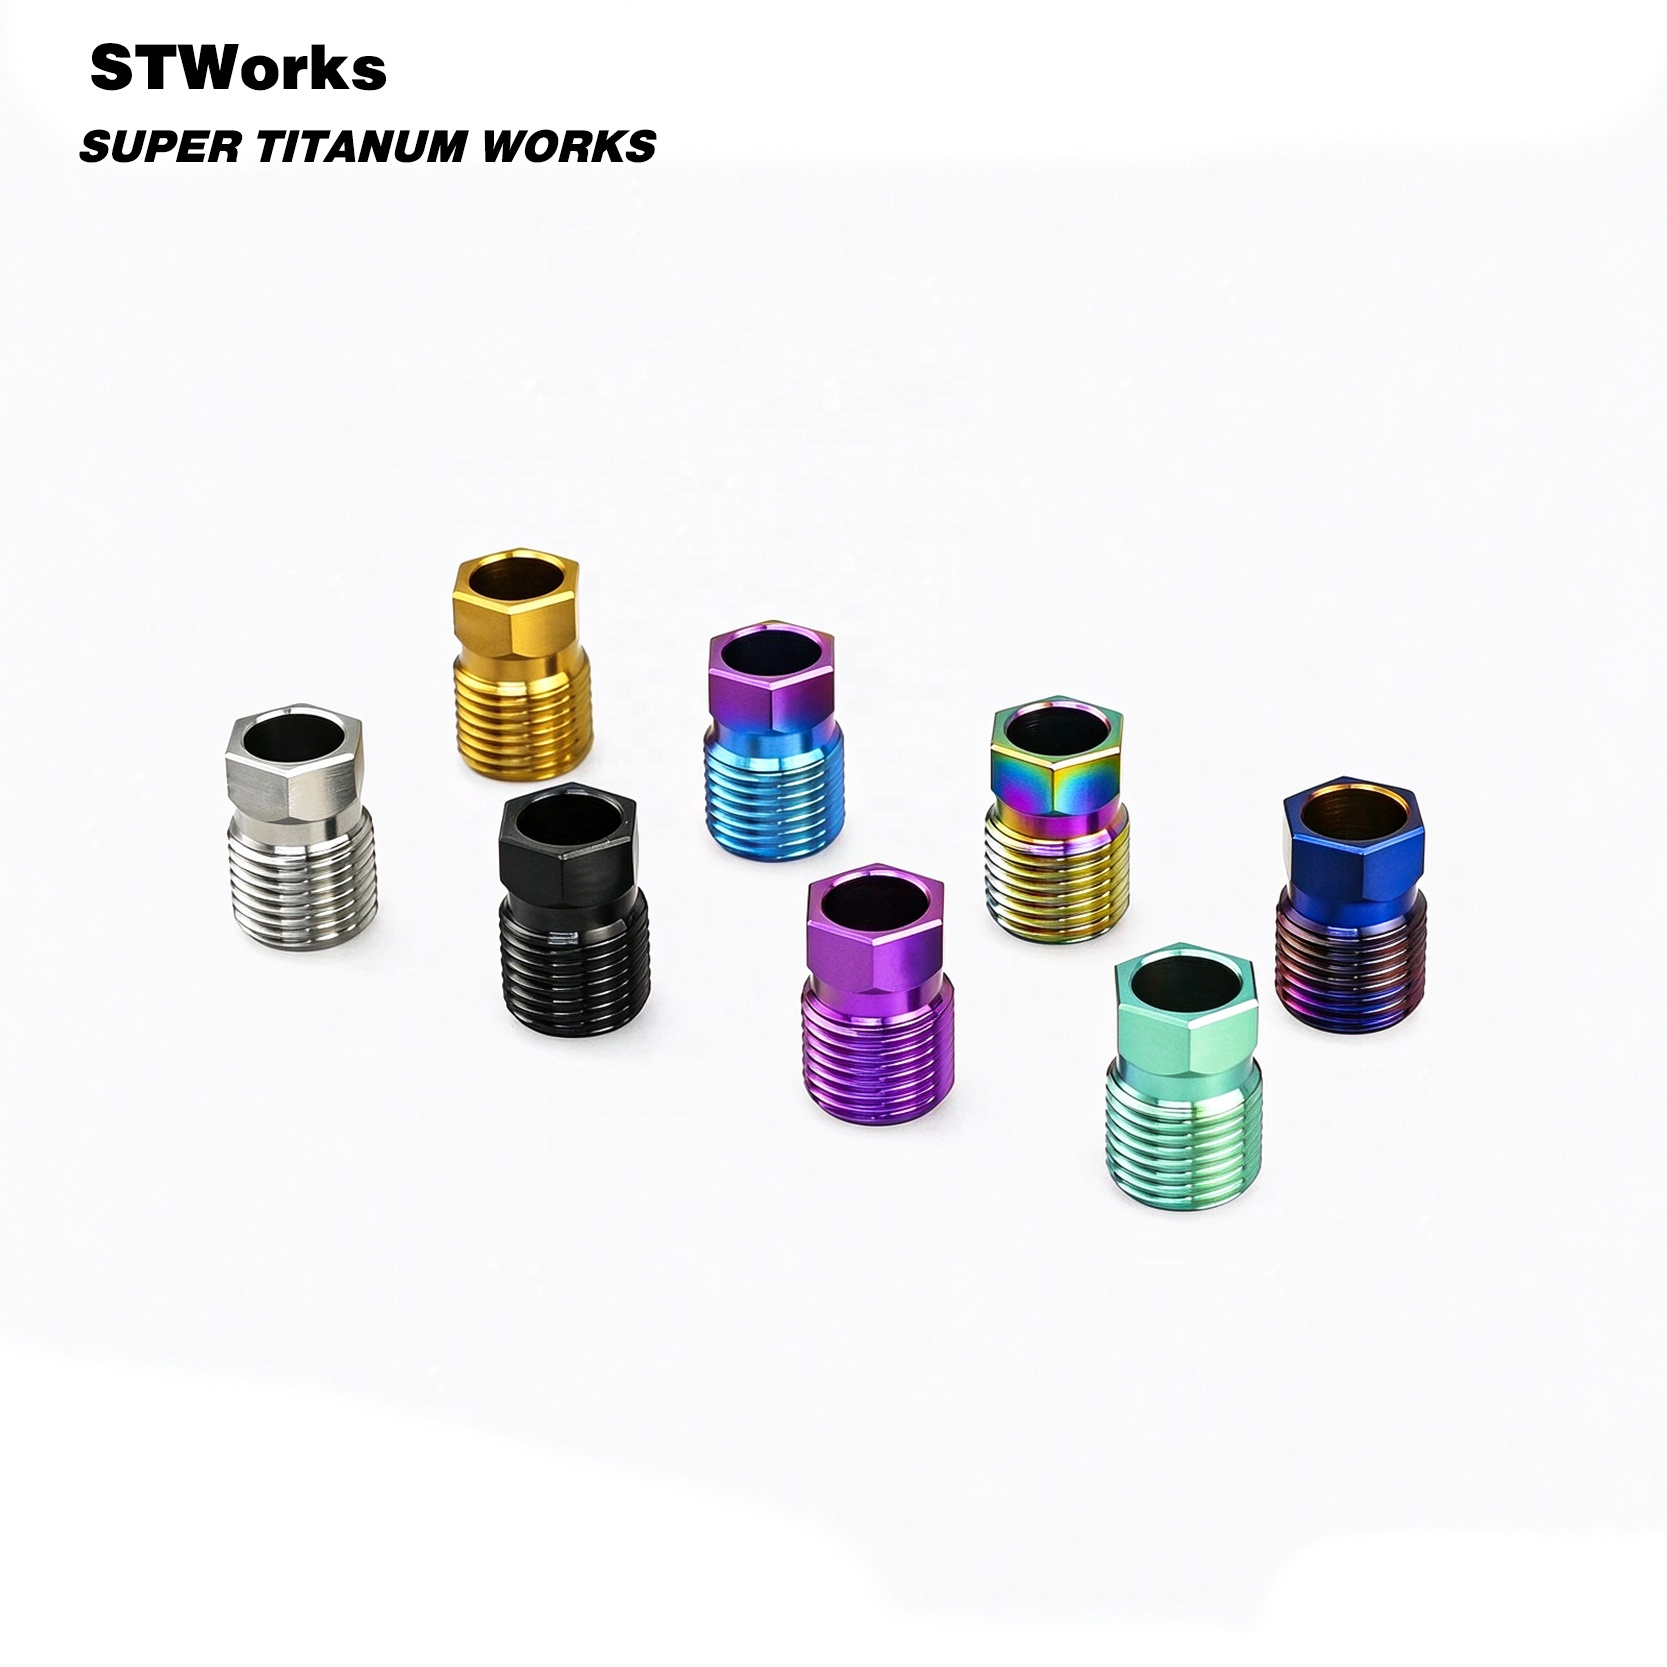
By controlling electrolytic voltage from 12V to 110V without pigments, we produce exact microscopic titanium dioxide (TiO2) film thicknesses. Light refraction creates vivid burnt blue, gold, purple, and green finishes that never peel or degrade.
Cold-Formed Heading vs. Precision Bar Turning
While mass consumer hardware relies on high-speed cold heading that causes internal micro-fissures in titanium, our high-spec acorn nuts are turned from solid annealed Ti-6Al-4V bar on Swiss CNC lathes to protect internal grain alignment.
Baoji Titanium Valley Advantage
Why Tier-1 Global Buyers Partner with Velnora
Established in 2013 in the heart of China’s titanium metallurgical epicenter, Velnora delivers engineering supremacy, end-to-end CNC agility, and complete export transparency.
13+
Years Manufacturing Excellence
1,000+
Global B2B Accounts Served
≤ 4h
Engineering Drawing Review
100%
Video Production Verification
Direct-to-Machinist Engineering
No intermediaries, sales agents, or bureaucratic delays. When you submit your 2D PDF, STEP, or IGES engineering drawings, you collaborate directly with machine programmers and metallurgical engineers located inside our Jinhe Precision Park facility.
Live Production Video Verification
We eliminate sourcing risk across oceans. For every production run of custom titanium acorn nuts, our team sends high-resolution macro videos and photos of Swiss turning, thread gauge testing, and anodizing before final packing and dispatch.
Unmatched Baoji Supply Chain Synergy
Located adjacent to national titanium sponge smelting and vacuum arc remelting centers, we secure certified Grade 5 aerospace billet at primary mill rates, allowing us to maintain rapid lead times and flexible MOQs from 50 to 50,000+ pieces.
Quality Control & Sourcing Checklist
How to Avoid Catastrophic Mistakes When Sourcing Titanium Acorn Nuts
Essential quality guidelines for procurement directors, mechanical engineers, and quality assurance inspectors.
1. The Science of Thread Galling (Cold Welding) & How to Prevent It
Titanium is characterized by an ultra-thin, highly stable native titanium oxide (TiO2) film that provides legendary corrosion resistance. However, when a titanium nut is fastened onto a titanium male stud under high clamping loads without lubrication, this oxide film can shear under friction. Exposed metallic micro-asperities instantly cold-weld together in a phenomenon known as thread galling. Best practice: Always mandate that your supplier apply rolled or single-point micro-finished internal threads (Ra < 0.4 µm). Additionally, specify high-pressure anti-seize lubricants containing molybdenum disulfide (MoS2) or copper paste, or request pre-applied baked dry-film lubricants or PVD nitride barrier coatings directly from our factory.
2. Ultrasonic Flaw Detection & Sponge Purity
Sub-standard manufacturers often introduce recycled, unrefined titanium turnings back into their melt, creating dangerous localized inclusions known as High-Density Inclusions (HDI) or Low-Density Interstitial Defects (LDI). These invisible metallurgical micro-voids act as primary fracture origins under fatigue torque. Ensure your Chinese manufacturing partner utilizes 100% vacuum double-melted (VAR) Grade 5 stock backed by ultrasonic test certificates and mill chemistry reports.
3. Thread Engagement Depth vs. Dome Clearance
A golden engineering rule for titanium fasteners is maintaining an effective thread engagement length equal to at least 1.5 times the nominal thread diameter (L ≥ 1.5D) when mating with lower-strength materials (such as aluminum engine blocks), or 1.2D when mating with titanium studs. When designing custom acorn nuts, verify that your male stud length leaves a minimum 1.5 mm clearance gap below the ceiling of the blind internal dome to prevent mechanical bottoming out during thermal expansion cycles.
Procurement Knowledge Base
Frequently Asked Questions by Global Sourcing Directors
Everything you need to know regarding standards, torque coefficients, MOQ, anodizing longevity, and custom drawing production.
What international fastener standards do you manufacture titanium acorn nuts to?
We manufacture directly to DIN 1587 (high-type cap nuts), JIS B1183 (low-profile domed cap nuts), and ISO standards. We also produce custom-engineered domed acorn nuts with integrated wide flanges, 12-point multi-hex heads, or security tamper-resistant drive styles machined strictly to your STEP, IGES, or 2D PDF technical drawings.
Can a Grade 5 titanium acorn nut directly substitute for stainless steel or carbon steel nuts?
Yes. Grade 5 (Ti-6Al-4V) delivers a tensile yield strength of 895–950 MPa, making it structurally superior to A2-70 (700 MPa) and A4-80 (800 MPa) stainless steel nuts, and directly comparable to Class 8.8 and 10.9 high-tensile carbon steel fasteners. Furthermore, it cuts 44% of component mass while offering complete immunity to saltwater pitting and chemical stress-corrosion cracking.
What torque coefficient (k-factor) should be applied when tightening titanium acorn nuts?
Dry titanium-on-titanium friction generates an erratic torque coefficient of k = 0.30 to 0.40, which drastically increases galling risk. When installing titanium acorn nuts, we recommend using an approved anti-seize paste (such as molybdenum disulfide or copper base), which stabilizes the k-factor between 0.12 and 0.15. Torque values should typically be reduced by 15% to 20% compared to dry steel torque charts.
How durable is the colored anodized layer on your titanium acorn nuts?
Unlike aluminum anodizing, which relies on organic dyes that fade under UV light, titanium anodizing is a physical oxide layer (TiO2) grown directly out of the metal matrix. The color is created entirely by microscopic optical light interference. It will not flake, chip, peel, or fade under prolonged ultraviolet exposure, engine heat up to 400°C, or saltwater splash zones.
What is your typical Minimum Order Quantity (MOQ) and production lead time?
For standard DIN 1587 titanium acorn nuts in common metric sizes (M6, M8, M10, M12), our MOQ starts at just 100 to 200 pieces, with off-the-shelf stock ready for dispatch within 48 hours. For bespoke OEM/ODM custom drawing runs requiring unique threads or flanged profiles, standard prototype runs are 50–100 pieces, with volume production lead times typically ranging between 12 to 22 business days.
Do you provide material test certifications and dimensional inspection reports?
Yes. Every export shipment is accompanied by a formal EN 10204 3.1 inspection certificate documenting exact chemical composition (spectral analysis) and mechanical properties (tensile, yield, elongation). Additionally, our QA department provides optical comparator and CMM dimensional inspection reports with thread go/no-go gauge pass verification.
Ready to Upgrade Your Fastening Assemblies with Certified Titanium?
Send your CAD files (STEP, IGES, PDF) or target standard specifications today. Our senior metallurgical machinists in Baoji will evaluate your tooling tolerances and provide an official quotation within 4 hours.
Contact Us