Featured Precision Titanium Components & Fasteners
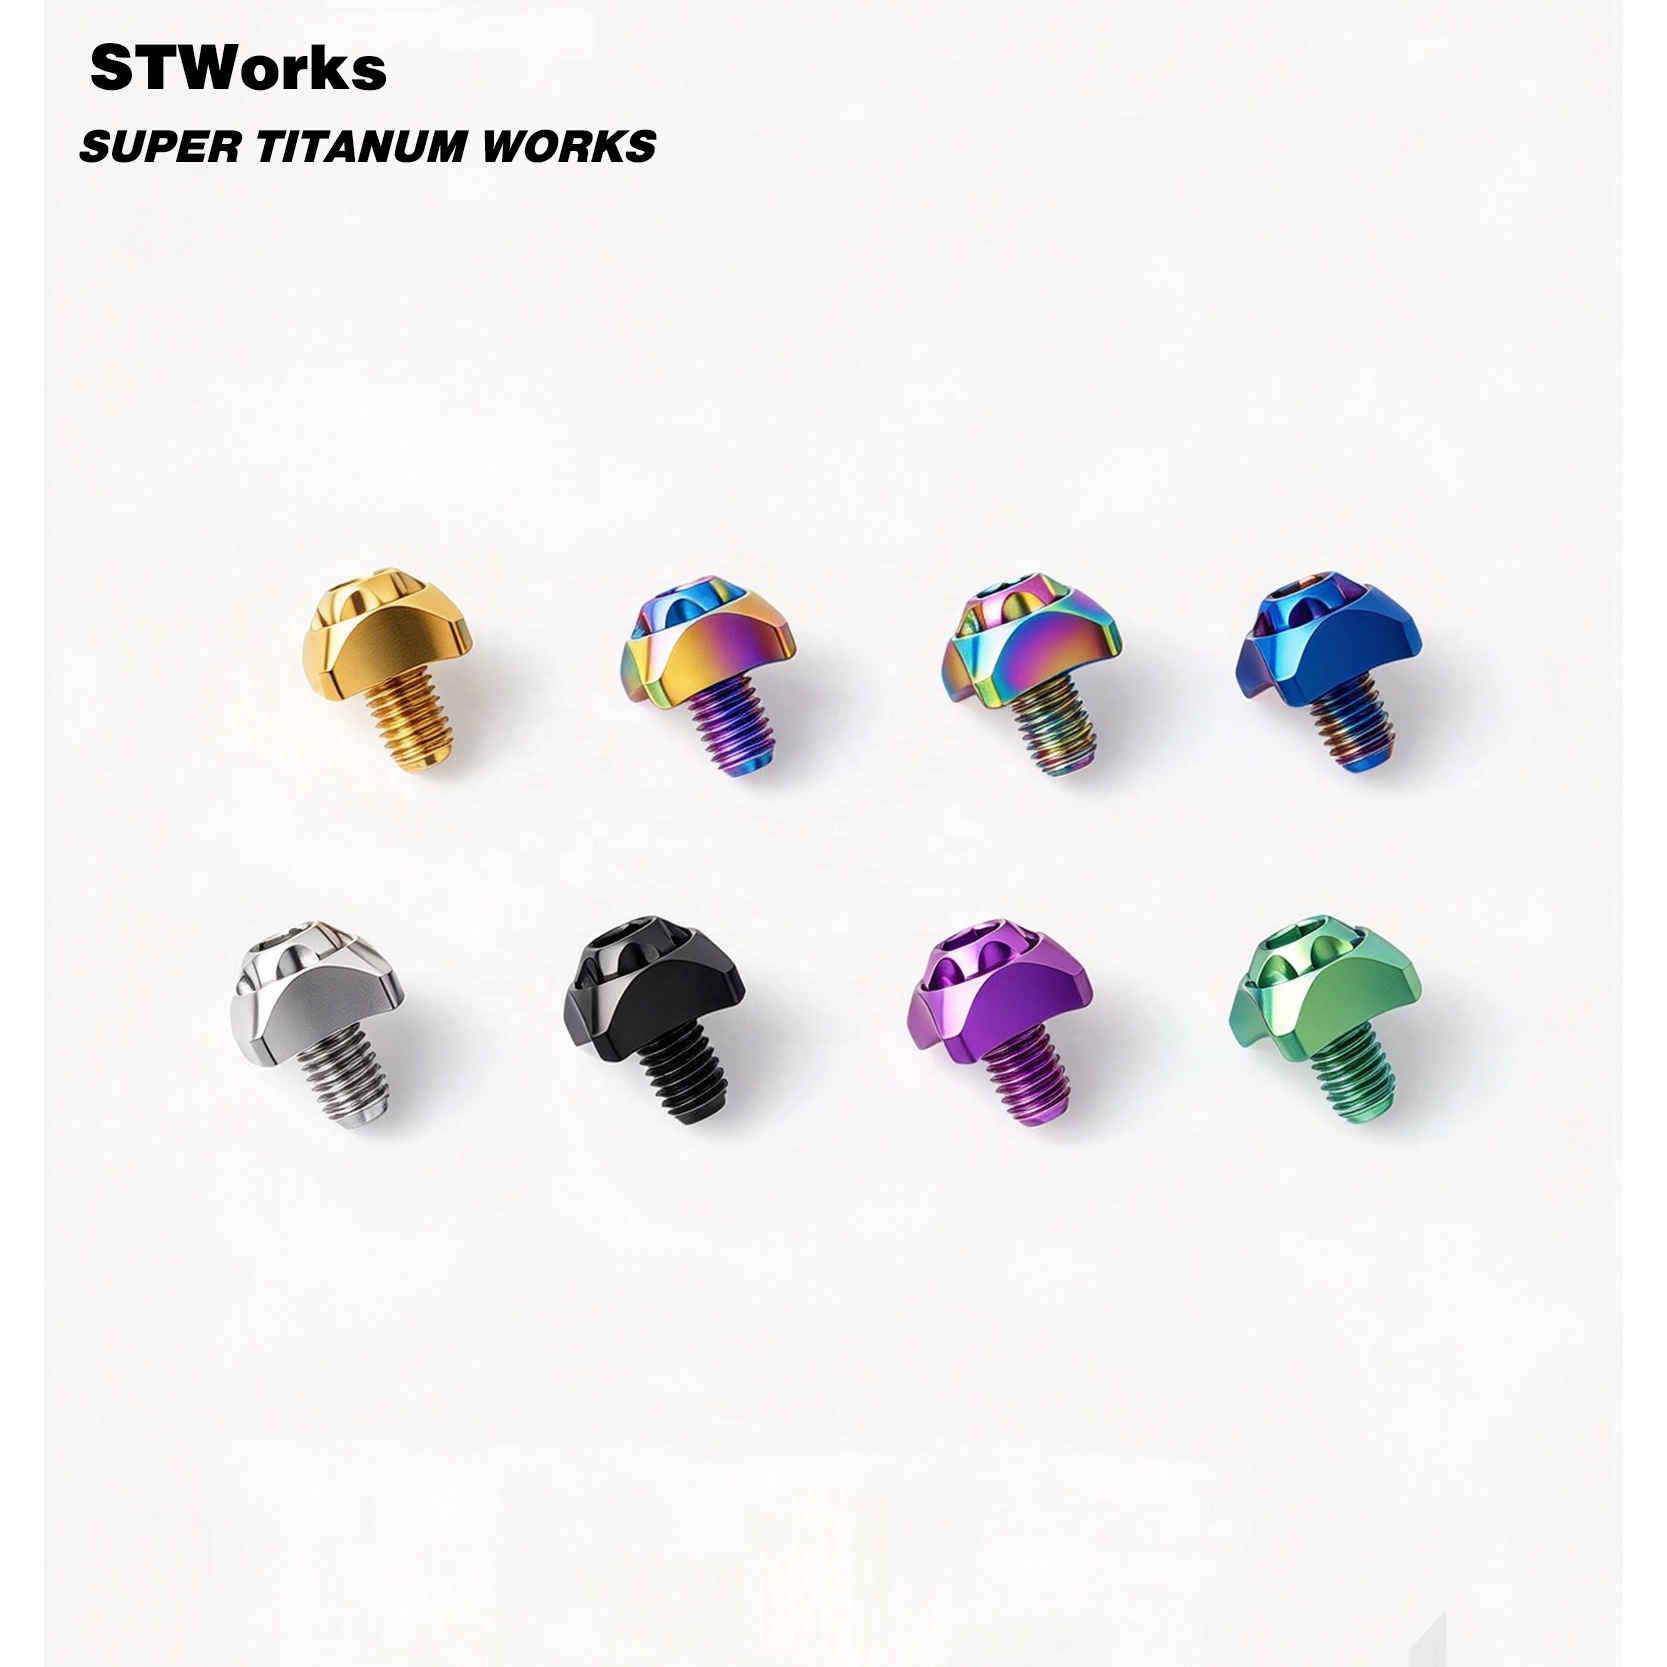
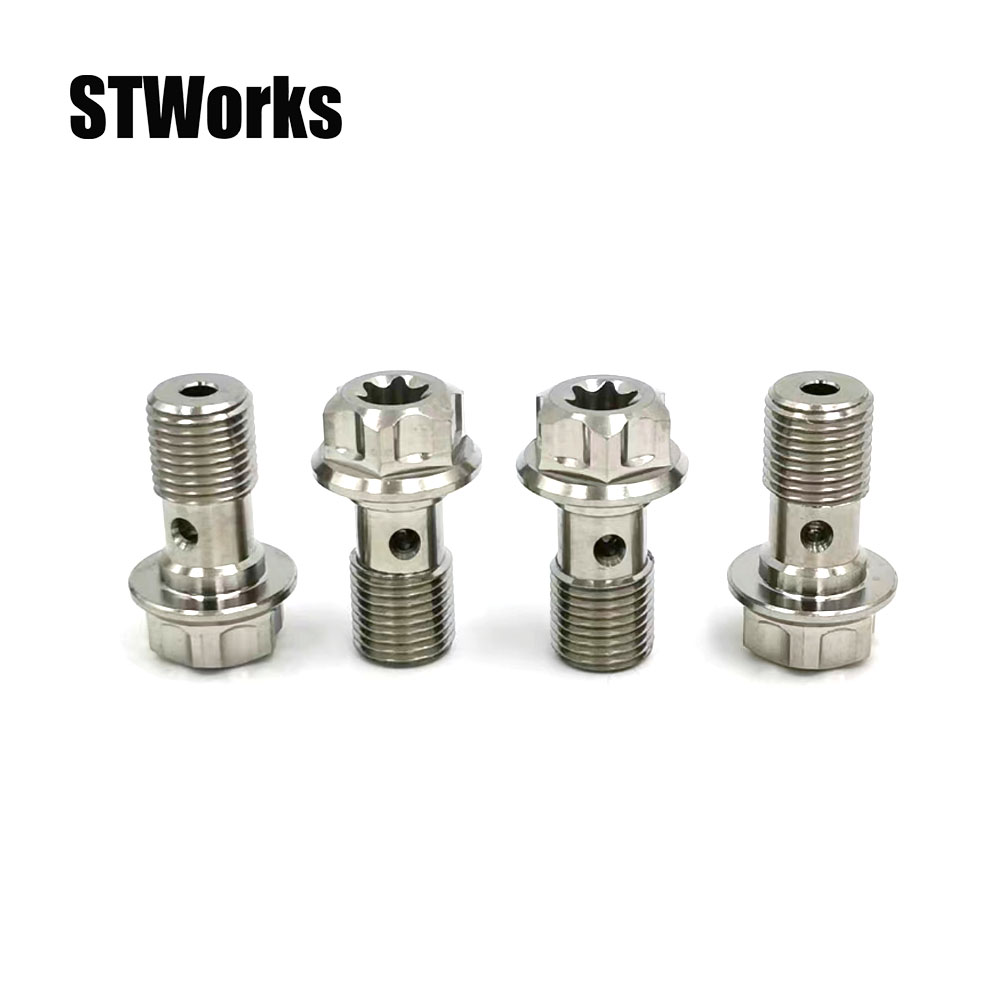
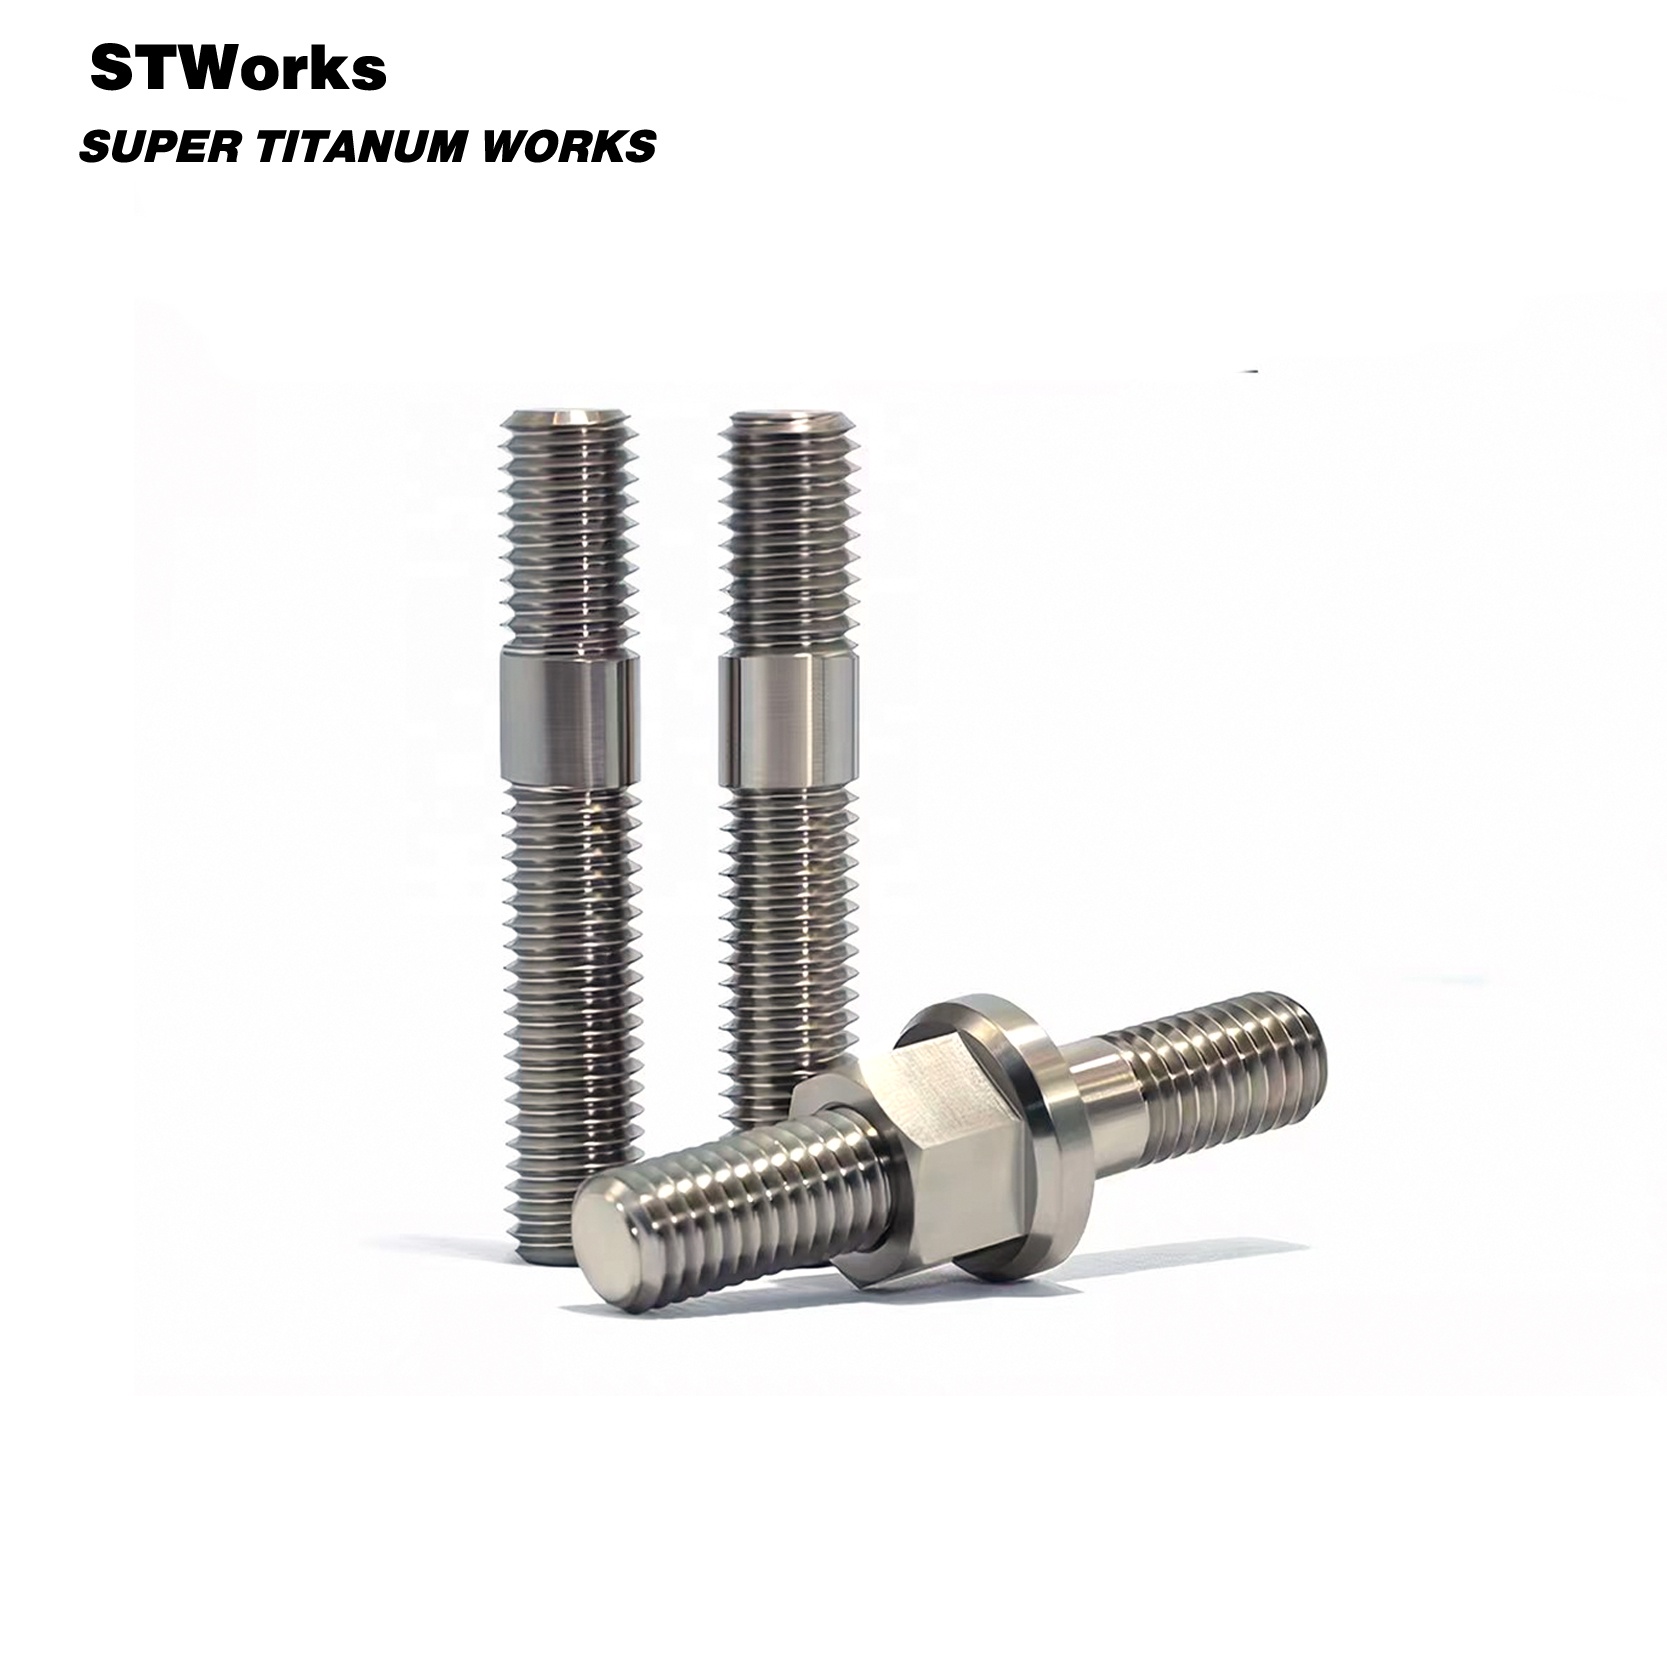
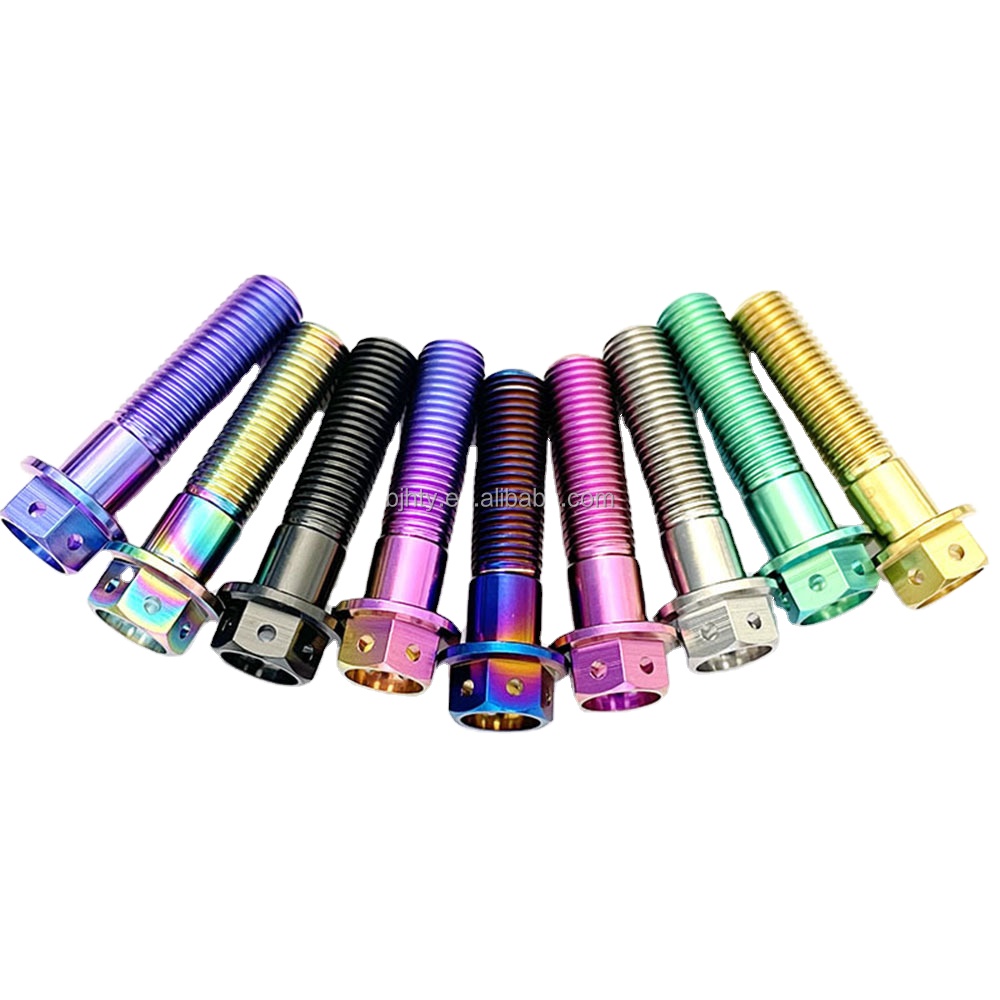
Engineered to strict aerospace and motorsport tolerances, each item reflects our advanced CNC turning, wire electrical discharge machining (EDM), and electrochemical anodization capabilities in Baoji.


1. The Metallurgy and Physics of Solid-State Diffusion-Bonded Timascus
In modern everyday carry (EDC) design, custom folding knives, and luxury tactical accessories, Timascus (also known in metallurgical circles as Titanium Damascus or Mokuti) stands as the pinnacle of functional decorative metallurgy. Unlike ornamental pattern-welded steel, which relies on iron-carbon phase shifts and chemical acid etching, genuine Timascus is a composite laminate formed entirely from varying grades of titanium alloys. The most revered industrial configuration utilizes alternating strata of Commercially Pure Grade 2 Titanium (CP-Ti) and Alpha-Beta Titanium Alloy (Grade 5 Ti-6Al-4V), or sophisticated ternary mixes introducing Grade 7 (with Palladium additions for grain boundary control) and Grade 9 (Ti-3Al-2.5V).
The manufacturing process initiates through Hot Isostatic Pressing (HIP) in high-vacuum sealed inert environments. Under pressures exceeding 100 to 150 MPa and temperatures maintained between 880°C and 940°C—below the beta-transus threshold of Ti-6Al-4V—atomic cross-diffusion occurs across the interfaces without forming brittle intermetallic compounds or introducing molten weld pools. This solid-state atomic diffusion bond yields continuous structural ductility, zero delamination propensity under cyclic elastic deflection, and an identical shear strength profile across the joint plane.
Information Gain: Why Timascus Over Standard Grade 5 Titanium for Pocket Clips?
While isotropic Grade 5 titanium offers a standard yield strength of ~895 MPa, a diffusion-bonded Timascus pocket clip engineered with oriented layer flow exhibits micro-laminated damping characteristics. When subjected to recurrent pocket-lip insertion fatigue (spring deflection), the alternating phase boundaries impede micro-crack propagation while showcasing differing light-refraction indices when oxidized electrochemically or thermally.
2. Engineering & CNC Precision Machining of Timascus Pocket Clips
Machining Timascus pocket clips demands an entirely different operational paradigm compared to standard titanium bar machining. As a premier China Timascus pocket clips manufacturer based in the industrial epicenter of Baoji, our facility leverages multi-axis Swiss-type lathes, high-speed 5-axis CNC machining centers, and ultra-fine brass wire electrical discharge machining (EDM) to address the following engineering challenges:
Wire EDM Contouring
Submerged brass-wire cutting under deionized dielectric fluid preserves the laminar flow integrity, preventing thermal work-hardening along the peripheral contours.
5-Axis 3D Contouring
Ball-nose end mills execute continuous sweeping toolpaths for organic ergonomics, sculpted ramps, and precision-countersunk screw hole arrays down to ±0.005mm.
Calibrated Retention Force
Pocket clip spring deflection curves are mathematically balanced. Pre-tension angles are set between 12° and 18° to provide 3.2 N to 4.8 N retention force without fabric damage.
Electrochemical Anodization
Sub-micron dielectric titanium oxide (TiO₂) layers create interference colors: Grade 2 CP turns gold/cyan at low voltages, while Ti-6Al-4V transforms into vibrant magentas and deep blues.
A fundamental failure point of low-tier pocket clip machining is tool chatter during thin-wall milling. A typical sculpted clip tapers from a 3.5mm thick mounting pad to a 1.2mm spring arm, terminating in a 2.5mm contoured pocket entry bill. Machining across alternating titanium layers means the cutting tool continuously transitions between soft Grade 2 (~200 HV) and tough Grade 5 (~350 HV). Without custom toolpath trochoidal damping, feed-rate optimization, and high-pressure cryogenic or emulsion coolant, delamination tears or micro-burrs can arise. Our automated 5-axis DMG MORI and Brother machining centers utilize custom carbide tooling coated with nano-composite AlTiN to ensure mirror surface finishes before hand polishing.
3. Technical Comparison: Timascus vs. Conventional Pocket Clip Alloys
When specifying hardware for custom knife OEM projects, titanium pens, flashlights, or high-end EDC gear, procurement engineers must weigh mechanical elasticity, corrosion resistance, cosmetic appeal, and mass. The matrix below contrasts the dominant pocket clip materials:
| Material Property / Criterion | Timascus / Mokuti (Ti-CP + Gr5) | Grade 5 Titanium (Ti-6Al-4V) | AISI 301 / 304 Spring Steel | 6061-T6 Billet Aluminum |
|---|---|---|---|---|
| Density (g/cm³) | 4.46 (Ultra-Light) | 4.43 (Ultra-Light) | 7.90 (Heavy baseline) | 2.70 (Very Light) |
| Yield Strength (MPa) | ~620 – 780 (Composite Avg.) | 895 – 930 | 800 – 1100 (Work-hardened) | 276 (Low) |
| Modulus of Elasticity (GPa) | 108 – 112 | 114 | 193 – 200 | 69 |
| Corrosion Resistance (Chloride/Sweat) | Immune (Bio-inert oxide) | Immune (Bio-inert oxide) | Moderate (Pitting risk) | Moderate (Requires Anodize) |
| Aesthetic & Collectibility Value | Highest (Iridescent Damascus) | Industrial / Monolithic | Low / Utilitarian | Low / Standard |
| Spring Fatigue Retention | Superior (Elastic Memory) | Excellent | Good (Prone to plastic set) | Poor (High creep risk) |
4. Global Sourcing & Procurement Trends for Custom EDC Hardware
The global marketplace for high-grade everyday carry gear, precision custom cutlery, and boutique tactical equipment has matured rapidly. B2B buyers, knife brands, and custom builders are moving away from stamped sheet-metal clips toward bespoke 3D CNC sculpted Timascus pocket clips. As an authority manufacturer in China, we observe four macro procurement trends reshaping the industry:
1. Standardized Hole Pitch with Custom Contouring
Brands now demand universal mounting compatibility—such as standard 3-hole Benchmade/Emerson spacing or 2-hole Spyderco layouts—while integrating aggressive 3D faceted geometry and custom Timascus grain directions that align with handle scales.
2. Deep-Carry Concealment Ergonomics
Modern consumers overwhelmingly favor deep-carry profiles where the mounting screws sit flush or sub-flush beneath the retention loop. This requires complex 4-axis undercut milling and wire EDM wire-loop clearances to prevent screw head interference.
3. Hybrid ZircoTi & Multi-Alloy Layering
Beyond traditional 2-metal Timascus, tier-one designers are transitioning to Zirconium-infused Titanium composites (ZircoTi). Upon torching or bath oxidation, the Zirconium layers turn jet-black, creating stark contrast against electric blue and golden titanium bands.
5. Enterprise Advantages: Sourcing from Baoji Titanium Valley
Headquartered in Baoji, Shaanxi Province—known worldwide as China's Titanium Valley—our operations integrate more than a decade of specialized non-ferrous metallurgy and precision CNC fastener engineering. When partnering with Velnora Titanium Industry for OEM and ODM Timascus pocket clip production, overseas clients gain decisive structural advantages:
- Raw Material Authenticity & Traceability: Direct partnerships with domestic aerospace sponge titanium suppliers ensure every batch of Grade 2, Grade 5, and custom Timascus billet possesses mill test certification (MTC), verifiable chemical composition, and uniform diffusion-bond density.
- Integrated CAD/CAM Engineering Support: We assist international knifemakers, kickstarter creators, and industrial brands in optimizing 3D CAD models (STEP, IGES, DXF) to minimize wire-cut cycle times, prevent stress concentrations at bend radii, and guarantee spring tension consistency.
- Full Spectrum Surface Treatments: In-house micro-sandblasting, mirror polishing, chemical deburring, high-voltage multi-step anodizing, thermal flame oxidation, and physical vapor deposition (PVD) DLC black diamond coatings.
- Live Production Verification: We eliminate international procurement anxiety by supplying high-definition inspection photos, 3D coordinate measuring machine (CMM) reports, and direct CNC machining video verification prior to batch dispatch.
Manufacturing Capacity in Numbers
Our Baoji production floor operates under rigorous ISO-compliant quality control matrices, serving over 1,000 distributors and industrial brands worldwide.
Frequently Asked Questions by B2B Buyers
Key technical answers regarding raw material validation, spring temper physics, custom MOQ runs, and surface preservation.