Gr5 Anodized
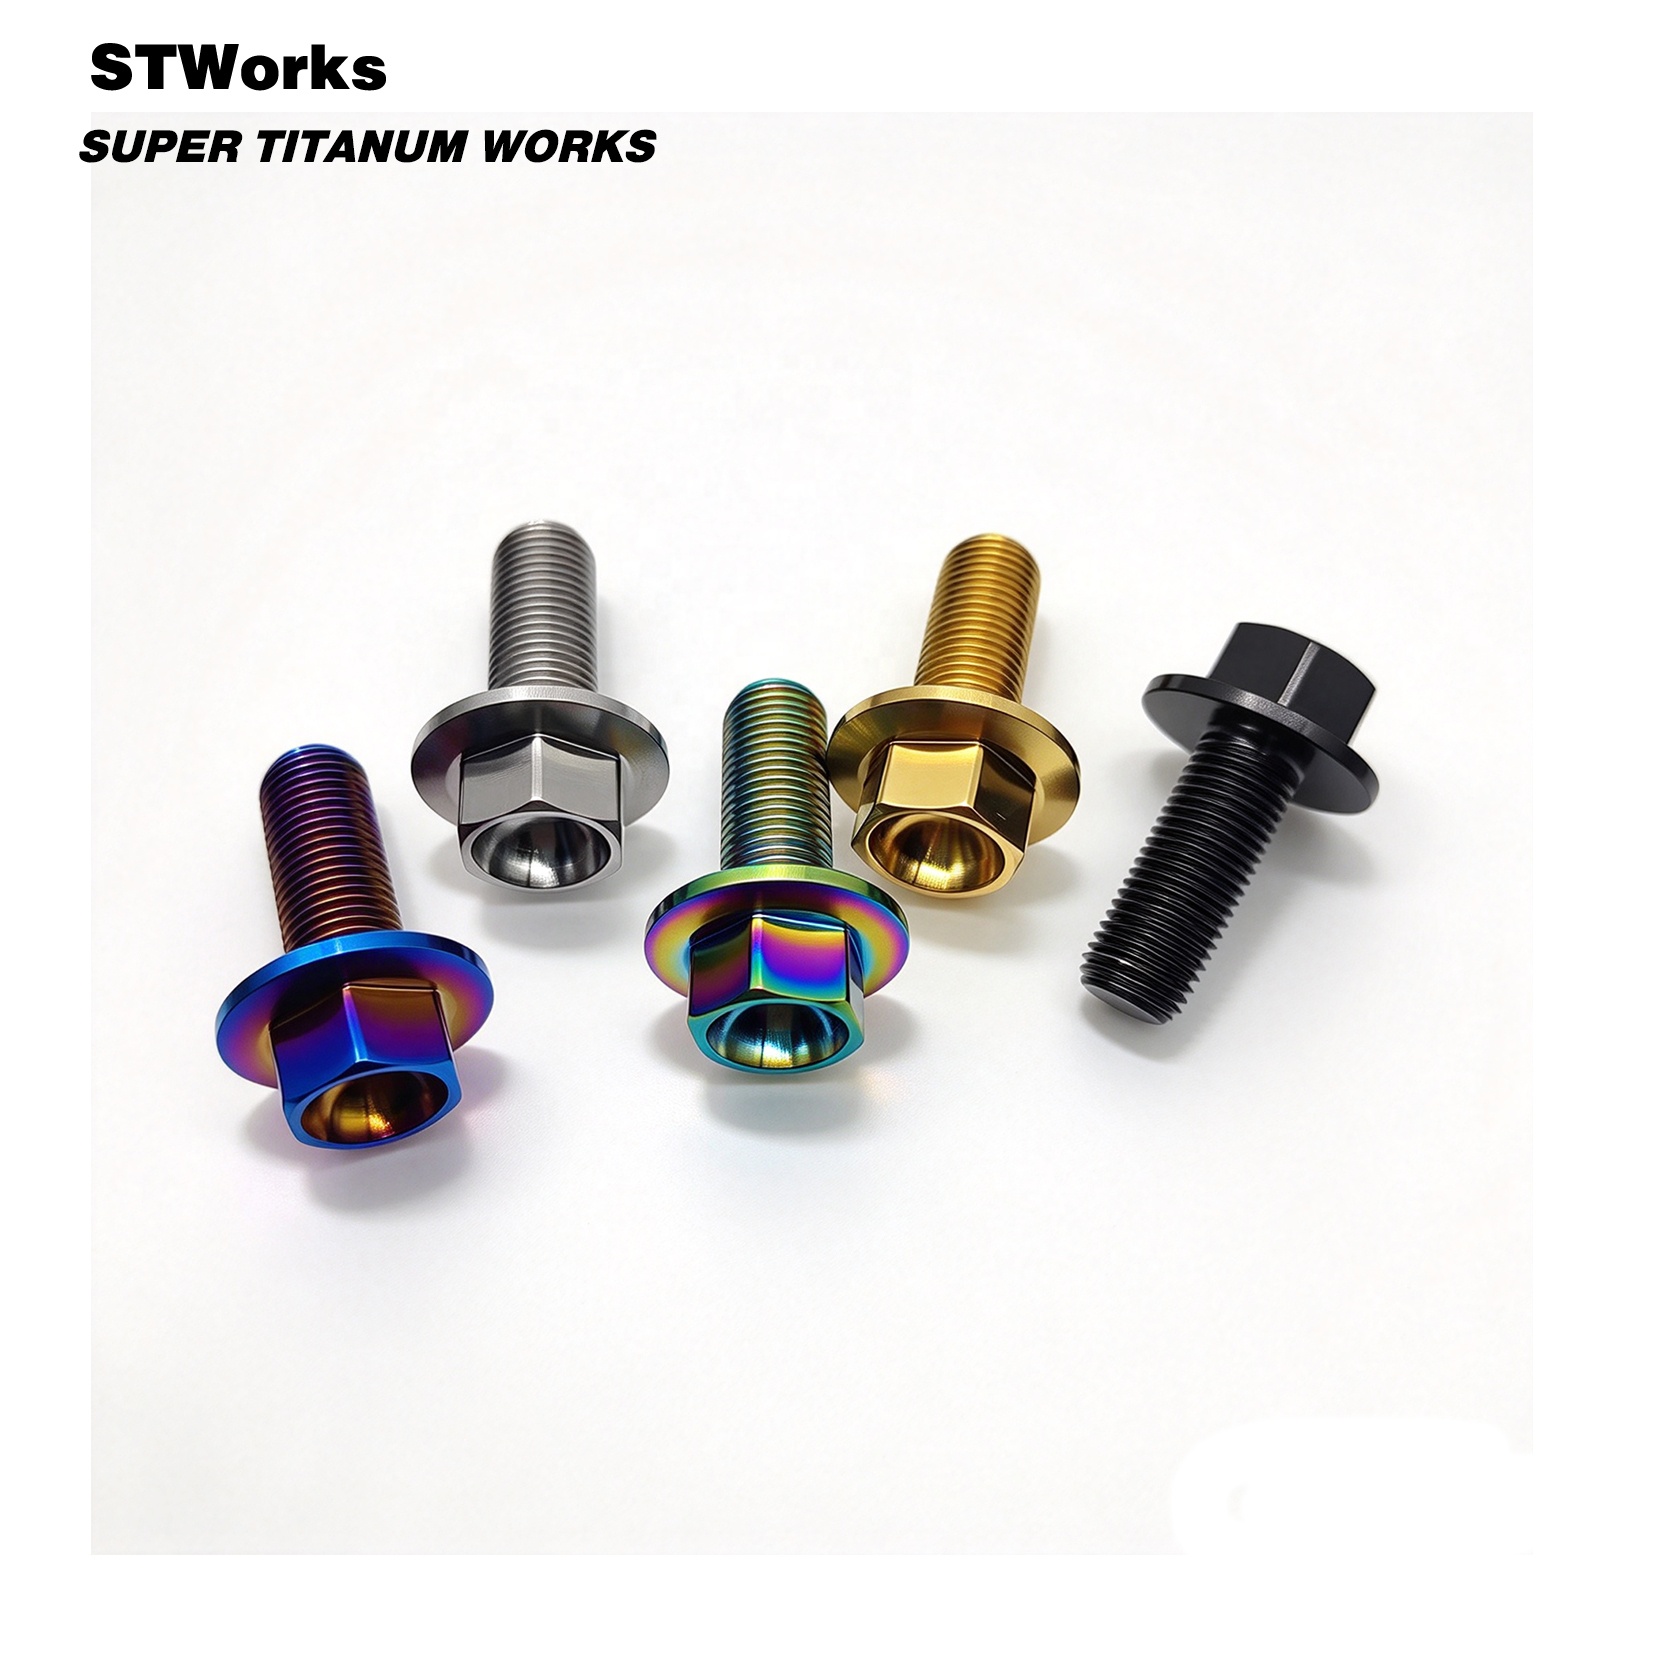
Milled and turned directly at our Jinhe Industrial Park facility in Baoji. Each titanium component represents our core metallurgy standards: tight tolerances (±0.005mm), certified Ti-6Al-4V Grade 5 alloy, and zero-defect thread finishes.
Timascus (also known commercially as Moku-Ti or Titanium Damascus) represents the absolute zenith of luxury metallurgic craftsmanship. Unlike traditional ferrous Damascus steel, which relies on high-carbon and nickel alloy steels forge-welded in atmospheric forge fires with borax flux, titanium is chemically hyper-reactive to atmospheric oxygen, nitrogen, and hydrogen at forging temperatures above 500°C (932°F).
As China's premier titanium manufacturer located in Baoji ("China's Titanium Valley"), Velnora Titanium has mastered the extreme science of Hot Isostatic Pressing (HIP) and high-vacuum solid-state diffusion bonding. We laminate alternating layers of CP Grade 2 Titanium (offering vivid blues, deep indigos, and vibrant purples under controlled oxidation) and Grade 5 Ti-6Al-4V alloy (which yields bright gold, bronze, and rose undertones with exceptional tensile strength of ≥895 MPa).
For custom luxury pen turners, boutique writing instrument brands, and tactical EDC toolmakers, our Timascus pen blanks deliver what inferior billets cannot: 100% molecular bonding along the laminate boundaries with zero delamination risk during deep hollow gun-drilling, high-speed lathe turning, or M10/M12 threading.
When turning a cylindrical pen blank on a CNC lathe or manual metalworking lathe, the exterior pattern changes rapidly as the bar's diameter is reduced. Our forge manipulates the 3D internal grain deformation specifically for pen barrel cross-sections.
Forged with uniform pitch torsional rotation after diffusion bonding. As pen turners taper the blank toward the grip section and clip finial, the spiral tightens symmetrically, forming hypnotic diagonal striations that highlight natural anodizing gradients along the pen barrel.
Multi-directional hemispherical die-coining penetrates alternating alpha and alpha-beta titanium phases. When turned down to pen sleeve thicknesses of 0.8mm–1.2mm, concentric elliptical eyes appear consistently around the circumference without dead spots.
Forged using multidirectional cross-axial folding and controlled press manipulation. Produces organic marbleized swirl patterns resembling interstellar clouds. Each turned pen is guaranteed 100% visually unique for high-ticket limited-edition collector series.
Why international pen manufacturers are shifting from traditional Damascus steel, brass, and acrylics to aerospace-diffusion-welded titanium composite blanks.
| Characteristic / Parameter | Velnora Timascus (Ti+Ti) | Traditional Steel Damascus | 7075-T6 Aerospace Aluminum | Naval Brass (C46400) |
|---|---|---|---|---|
| Density & Specific Weight | 4.46 g/cm³ (Ideal Balance) | 7.85 g/cm³ (Excessively Heavy) | 2.81 g/cm³ (Feels Toy-Like) | 8.41 g/cm³ (Hand-Fatiguing) |
| Skin Biocompatibility & Allergen | 100% Hypoallergenic (Medical Safe) | Contains Nickel (Contact Allergies) | Requires Anodized Seal Layer | Oxidizes, Smells Metallic on Skin |
| Corrosion Resistance | Impervious to Sweat, Salt & Ink | Rusts without Oil / Micro-pitting | Susceptible to Galling & Pitting | Tarnishes to Dark Verdigris |
| Coloration Mechanism | Electrolytic & Thermal TiO2 Prism | Acid Etching Only (Black / Gray) | Organic Acid Dye Anodizing | Chemical Patination Only |
| Lathe Chip Breaking & Machining | Consistent (No Delamination) | Hard Spots Cause Tool Chipping | Soft, Free Cutting | Excellent Free Machining |
| Luxury Perceived Market Value | Ultra-High (Tier 1 Collector Tier) | Moderate to High | Mid-Tier Commercial | Budget to Everyday EDC |
A definitive production guide for pen turners: optimizing feeds, speeds, tooling substrates, and heat-patina temperatures to achieve museum-grade results without ruining expensive composite stock.
Because Timascus combines softer CP titanium with tougher Grade 5 Ti-6Al-4V, standard tooling will experience varying cutting resistance. We recommend ultra-sharp, uncoated micrograin carbide inserts (such as CCGT or DCGT inserts with positive rake angles). Keep surface cutting speeds at 90–140 SFM (28–42 m/min) with constant, positive feed to avoid work-hardening the CP layers.
When hollowing pen barrels to accept Schmidt, Bock, or Jowo nib feeds, drill wandering is catastrophic. Use parabolic flute titanium-nitride drills with high-pressure pecking cycles. For cap and grip threads (e.g. M10x0.5 or M12x0.75 triple-start), always apply specialized chlorinated tapping paste to eliminate galling between tool flanks and titanium chips.
Post-machining, mirror-polish the blank up to 3000 grit, followed by ultrasonic degreasing in pure acetone. A brief 10–15 second dip in a 3% hydrofluoric/nitric acid bath preferentially micro-etches the CP titanium, creating tactile layer relief. When heat-torched with a clean propane flame or heated to 380°C–420°C, differential oxidation turns CP2 vivid electric blue while Gr5 shifts into intense gold and amethyst.
As the international EDC and bespoke fountain pen markets expand, strategic procurement professionals must align with major metallurgical shifts over the next five years.
While classic two-alloy Timascus remains the industry benchmark, market demand is soaring for tri-metal billets incorporating pure Zirconium (Zr702). Upon thermal oxidation, zirconium transforms into diamond-hard obsidian-black zirconium dioxide (ZrO2). This creates ultra-high contrast pens featuring jet-black stripes juxtaposed against radiant blue and golden titanium bands.
Solid Timascus rods force luxury turners to core out up to 65% of expensive raw material into non-reusable swarf. Velnora is pioneering pre-trepanned, seamless hollow Timascus tubes with precision ID and pattern concentricity, reducing turners' raw stock costs by up to 35% while slashing machining cycle times by half.
High-end pen collectors demand authentic metallurgical provenance. High-tier European and American brands now mandate mill test certifications (MTC) proving vacuum-arc remelted sponge titanium origin. Velnora provides full spectrographic assay verification and ultrasonic NDT batch testing reports for every consignment.
Founded in 2013 and anchored in Jinhe Industrial Park, Baoji, Velnora combines raw titanium melting proximity with high-precision CNC machining, wire EDM cutting, and bespoke metallurgical forge technology.
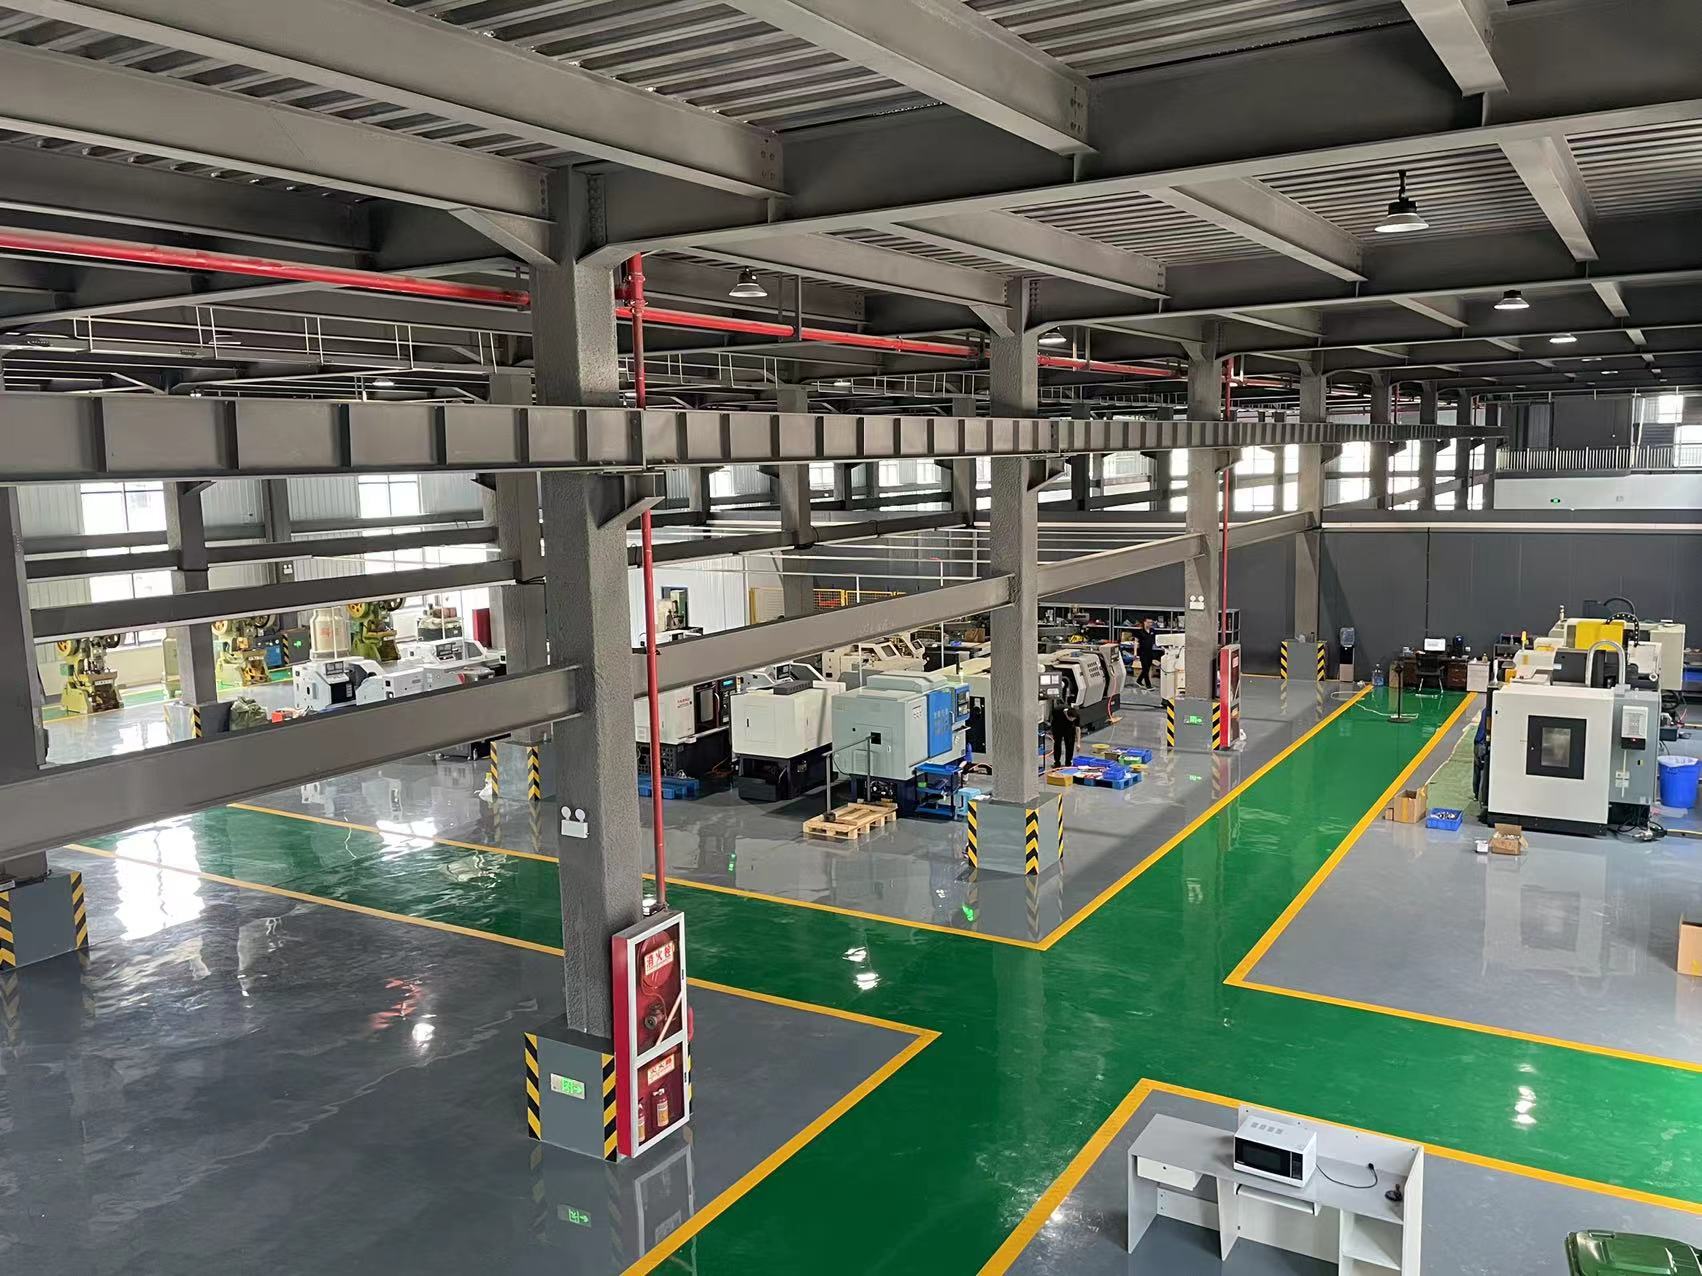
High-precision turning centers capable of holding ±0.005mm tolerances for intricate pen clips, grip sections, finials, and screw caps with aerospace-grade thread profiles.
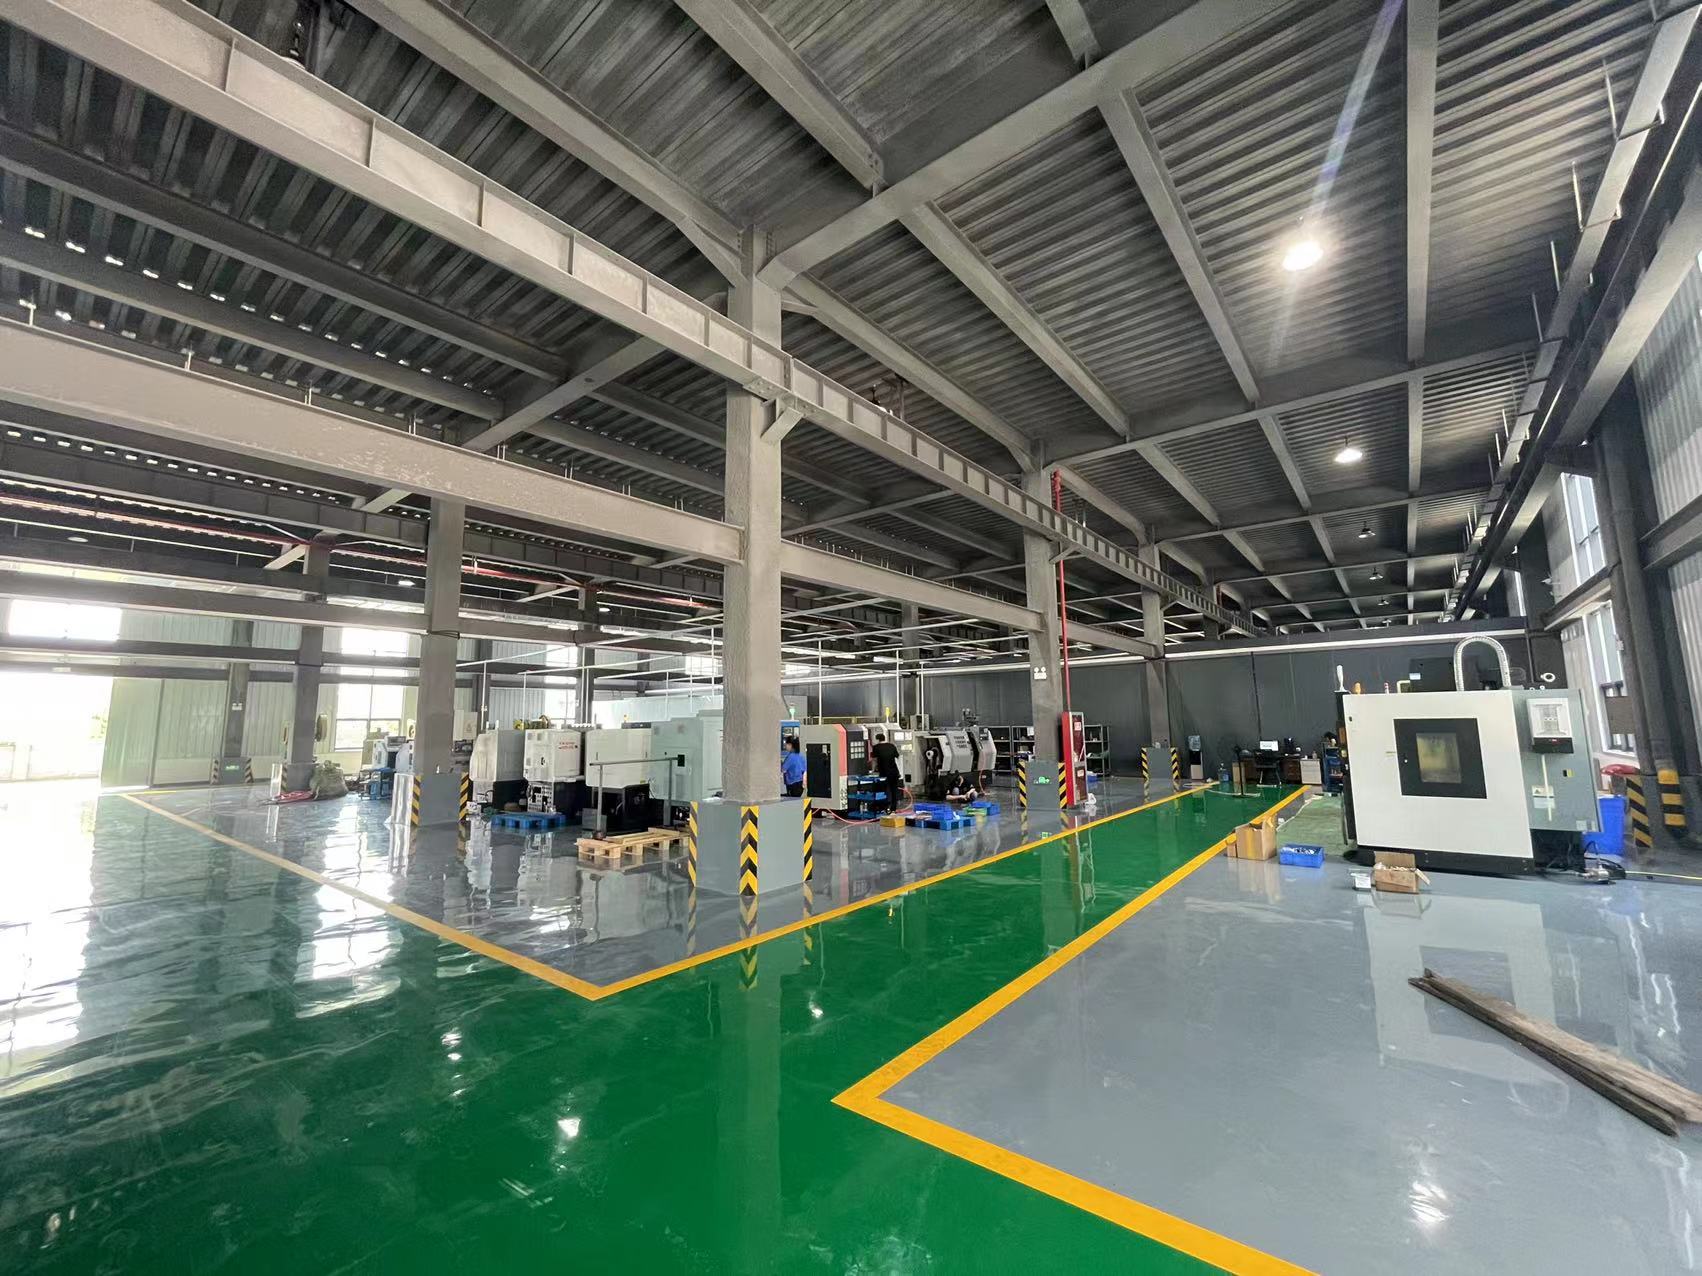
Every Timascus billet undergoes ultrasonic non-destructive testing (NDT) to ensure zero micro-porosity, zero inclusion entrapment, and 100% diffusion bond integrity.
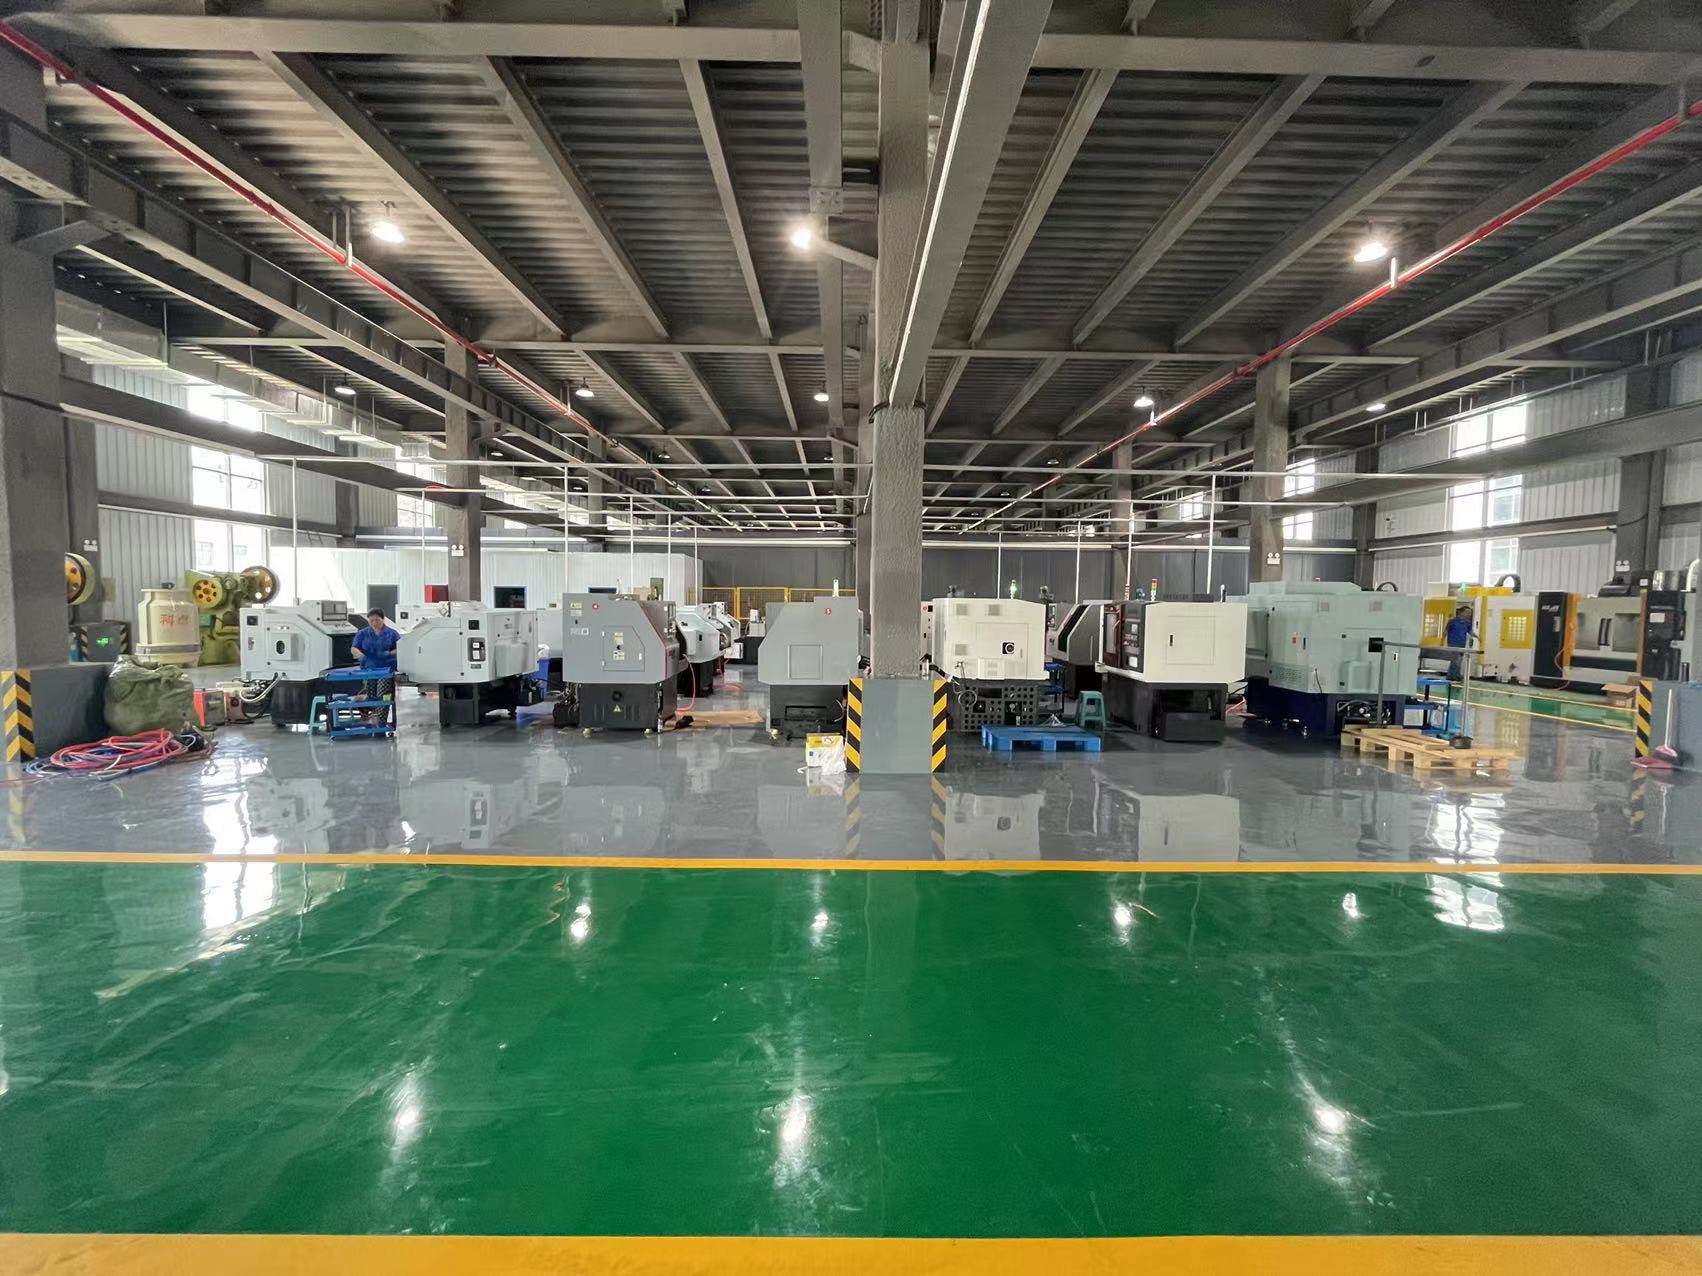
Serving over 1,000 international B2B clients across North America, Europe, Japan, and Australia with custom packaging, protective oil sealing, and live video production proofs.
Technical guidance direct from our master metallurgical engineers for custom pen turning studios, CNC machine shops, and purchasing directors.
Our standard Timascus pen blanks are composed of Commercially Pure Grade 2 Titanium (CP2) diffusion-bonded with Grade 5 Titanium (Ti-6Al-4V / TC4). CP Grade 2 is selected for its superior ductility and its electrochemical potential to develop striking cyan, royal blue, and amethyst oxide layers at lower voltages (25V–45V). Grade 5 titanium adds structural rigidity, tensile strength (≥895 MPa), and resistance to thread wear, while shifting into high-voltage golden yellow, rose, and green hues (60V–90V). On custom request, we also forge three-alloy billets incorporating Grade 7 (palladium-stabilized) or pure Zirconium (Zr702) for black contrast.
Delamination in inferior titanium Damascus occurs when forge-welding is performed in an open atmosphere or under insufficient vacuum, allowing interstitial oxygen and nitrogen to create brittle alpha-case titanium interfaces. Velnora eliminates this by enclosing descaled, mirror-cleaned sheets inside hermetically welded stainless steel canisters evacuated to 10^-4 Torr, followed by Hot Isostatic Pressing (HIP) at temperatures exceeding 880°C (1,616°F) under 120–150 MPa of hydrostatic argon pressure. This forces atomic-level grain boundary migration across alloy layers, transforming the stack into a monolithic solid with 100% shear bond strength.
We stock centerless-ground round rods in diameters tailored for pen turning: 12.7mm (1/2"), 14.0mm, 15.87mm (5/8"), 18.0mm, 20.0mm, and 25.4mm (1.0"). Standard lengths range from 120mm to 150mm for single-pen blanks, or continuous 500mm–1000mm bars for automated CNC Swiss lathe bar feeders. We also forge custom rectangular blocks, flats, and hollow tubes to customer CAD specifications.
Both methods yield exceptional finishes depending on your aesthetic goal:
Flame Polishing (Torch Coloration): Delivers organic, iridescent rainbow transitions. Use a clean micro-torch or propane flame, rotating the pen barrel smoothly after polishing to 2500+ grit and solvent cleaning. As soon as the golden-bronze shifts to rich violet and electric blue, quench in clean water.
Electrochemical Anodizing: Delivers precise, repeatable batch colors. In an electrolyte bath (such as a 1%–3% trisodium phosphate or ammonium sulfate solution), applying 25–35 volts yields vibrant purple/blue patterns, while 65–85 volts yields vivid golds, magentas, and greens.
For standard in-stock Timascus pen blanks (e.g. 14mm–18mm twist pattern rods), our MOQ is as low as 1 piece for prototype testing. For custom pattern pressings, specialized alloy pairings (such as ZircuTi), or proprietary diameter runs, our typical MOQ is 10–20 pieces or 5 kg total weight. Standard inventory ships within 24–48 hours; custom forge tooling runs ship within 12–18 business days with DHL/FedEx Express door-to-door delivery.
Yes. In addition to supplying raw unmachined and centerless-ground Timascus rods, Velnora operates a complete precision CNC machine shop in Baoji equipped with Swiss-type automatic lathes, 4-axis milling centers, and Sodick wire EDM machines. We routinely machine complete pen barrels, caps, clips, bolt-action mechanisms, and Begleri beads directly to customer 2D/3D drawings (STEP, IGES, DXF) under strict NDA protection.
Whether you need a single prototype blank for a bespoke commission or bulk production runs of centerless-ground rods for automated CNC machining, our engineering team in Baoji is standing by with metallurgical reports, pattern samples, and immediate direct mill pricing.