Precision Titanium Cockpit & Fastener Components
Manufactured to aerospace tolerances (±0.02mm), ensuring optimal preload distribution, galvanic safety on carbon steerers, and featherweight structural rigidity.

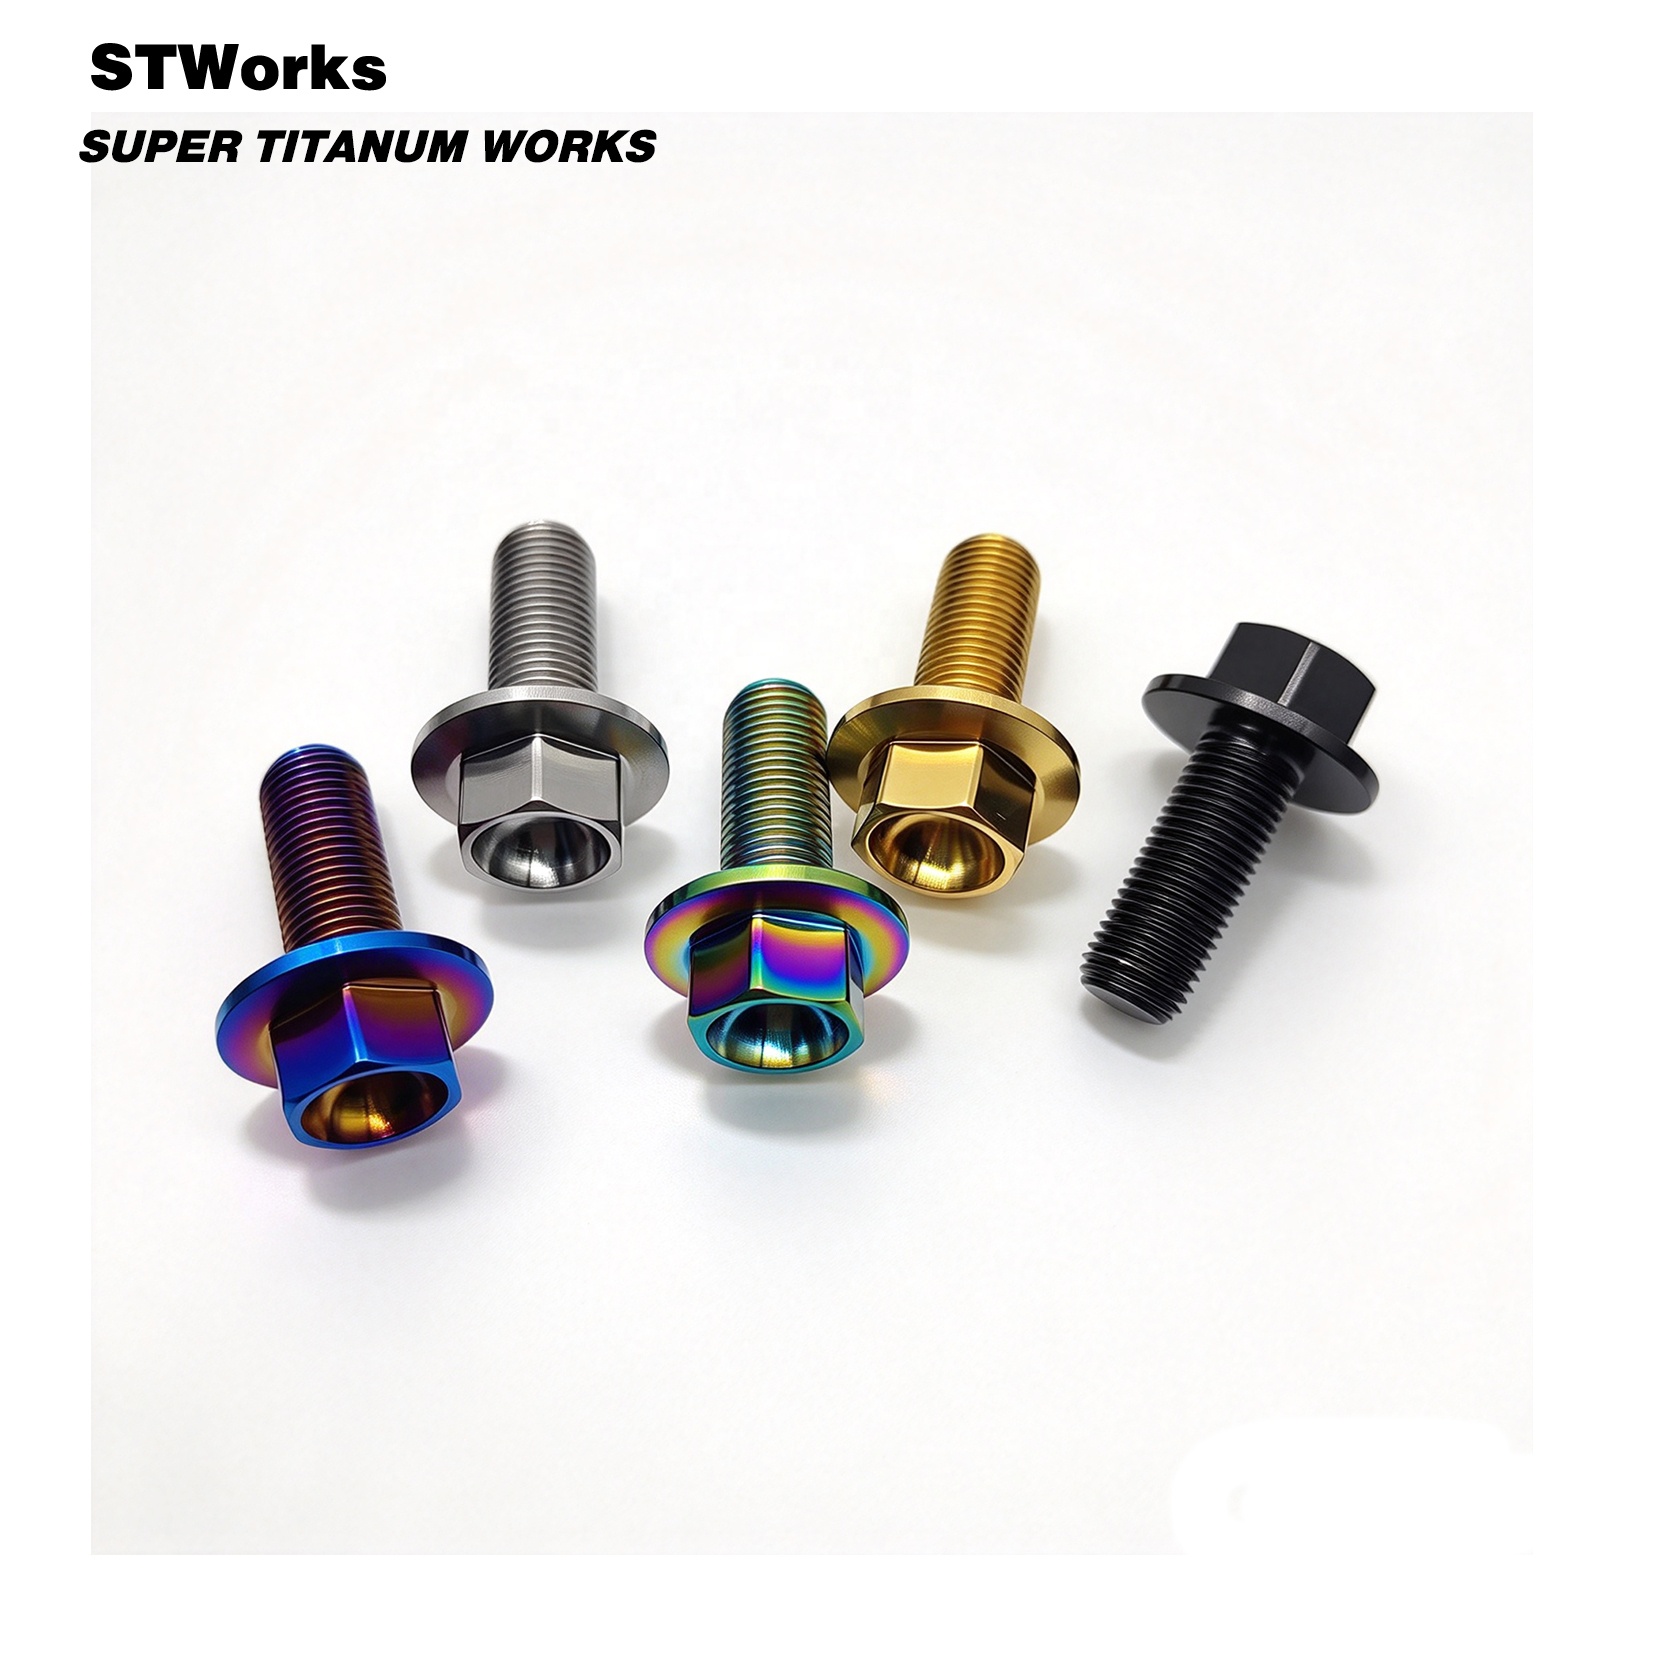
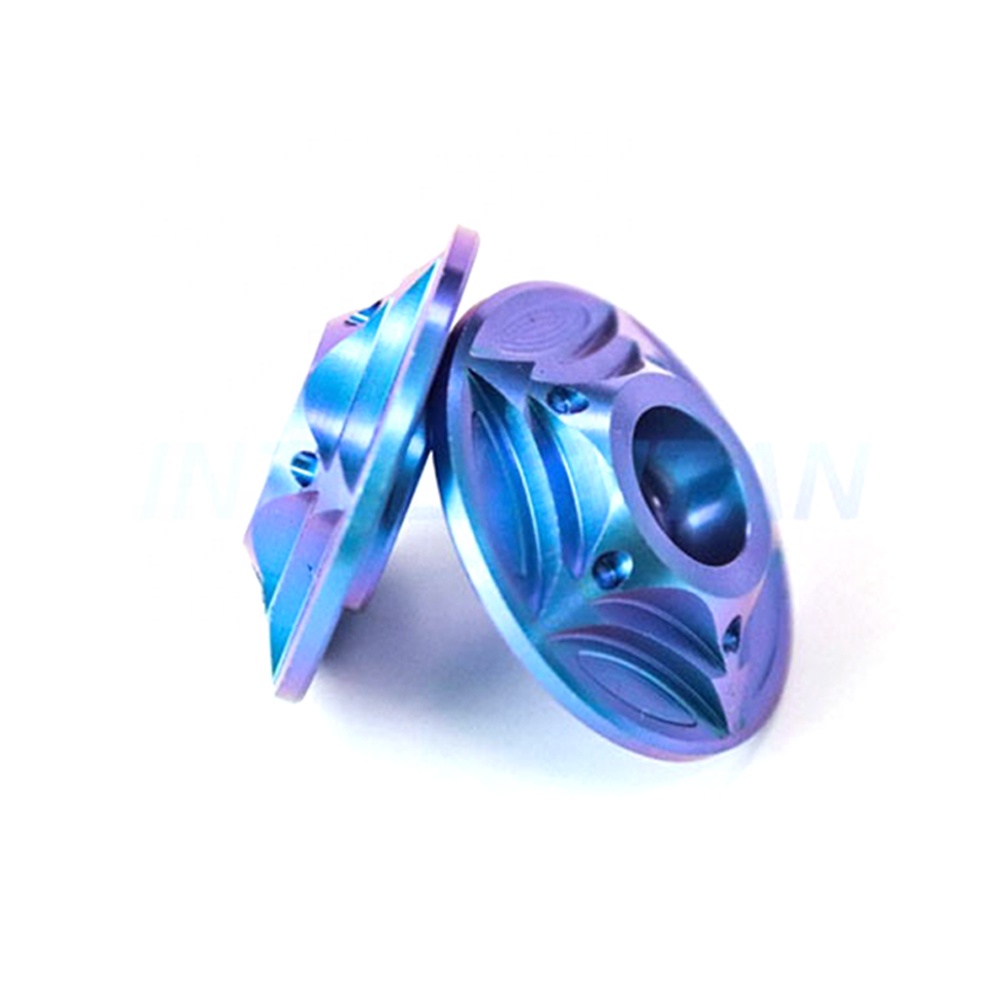
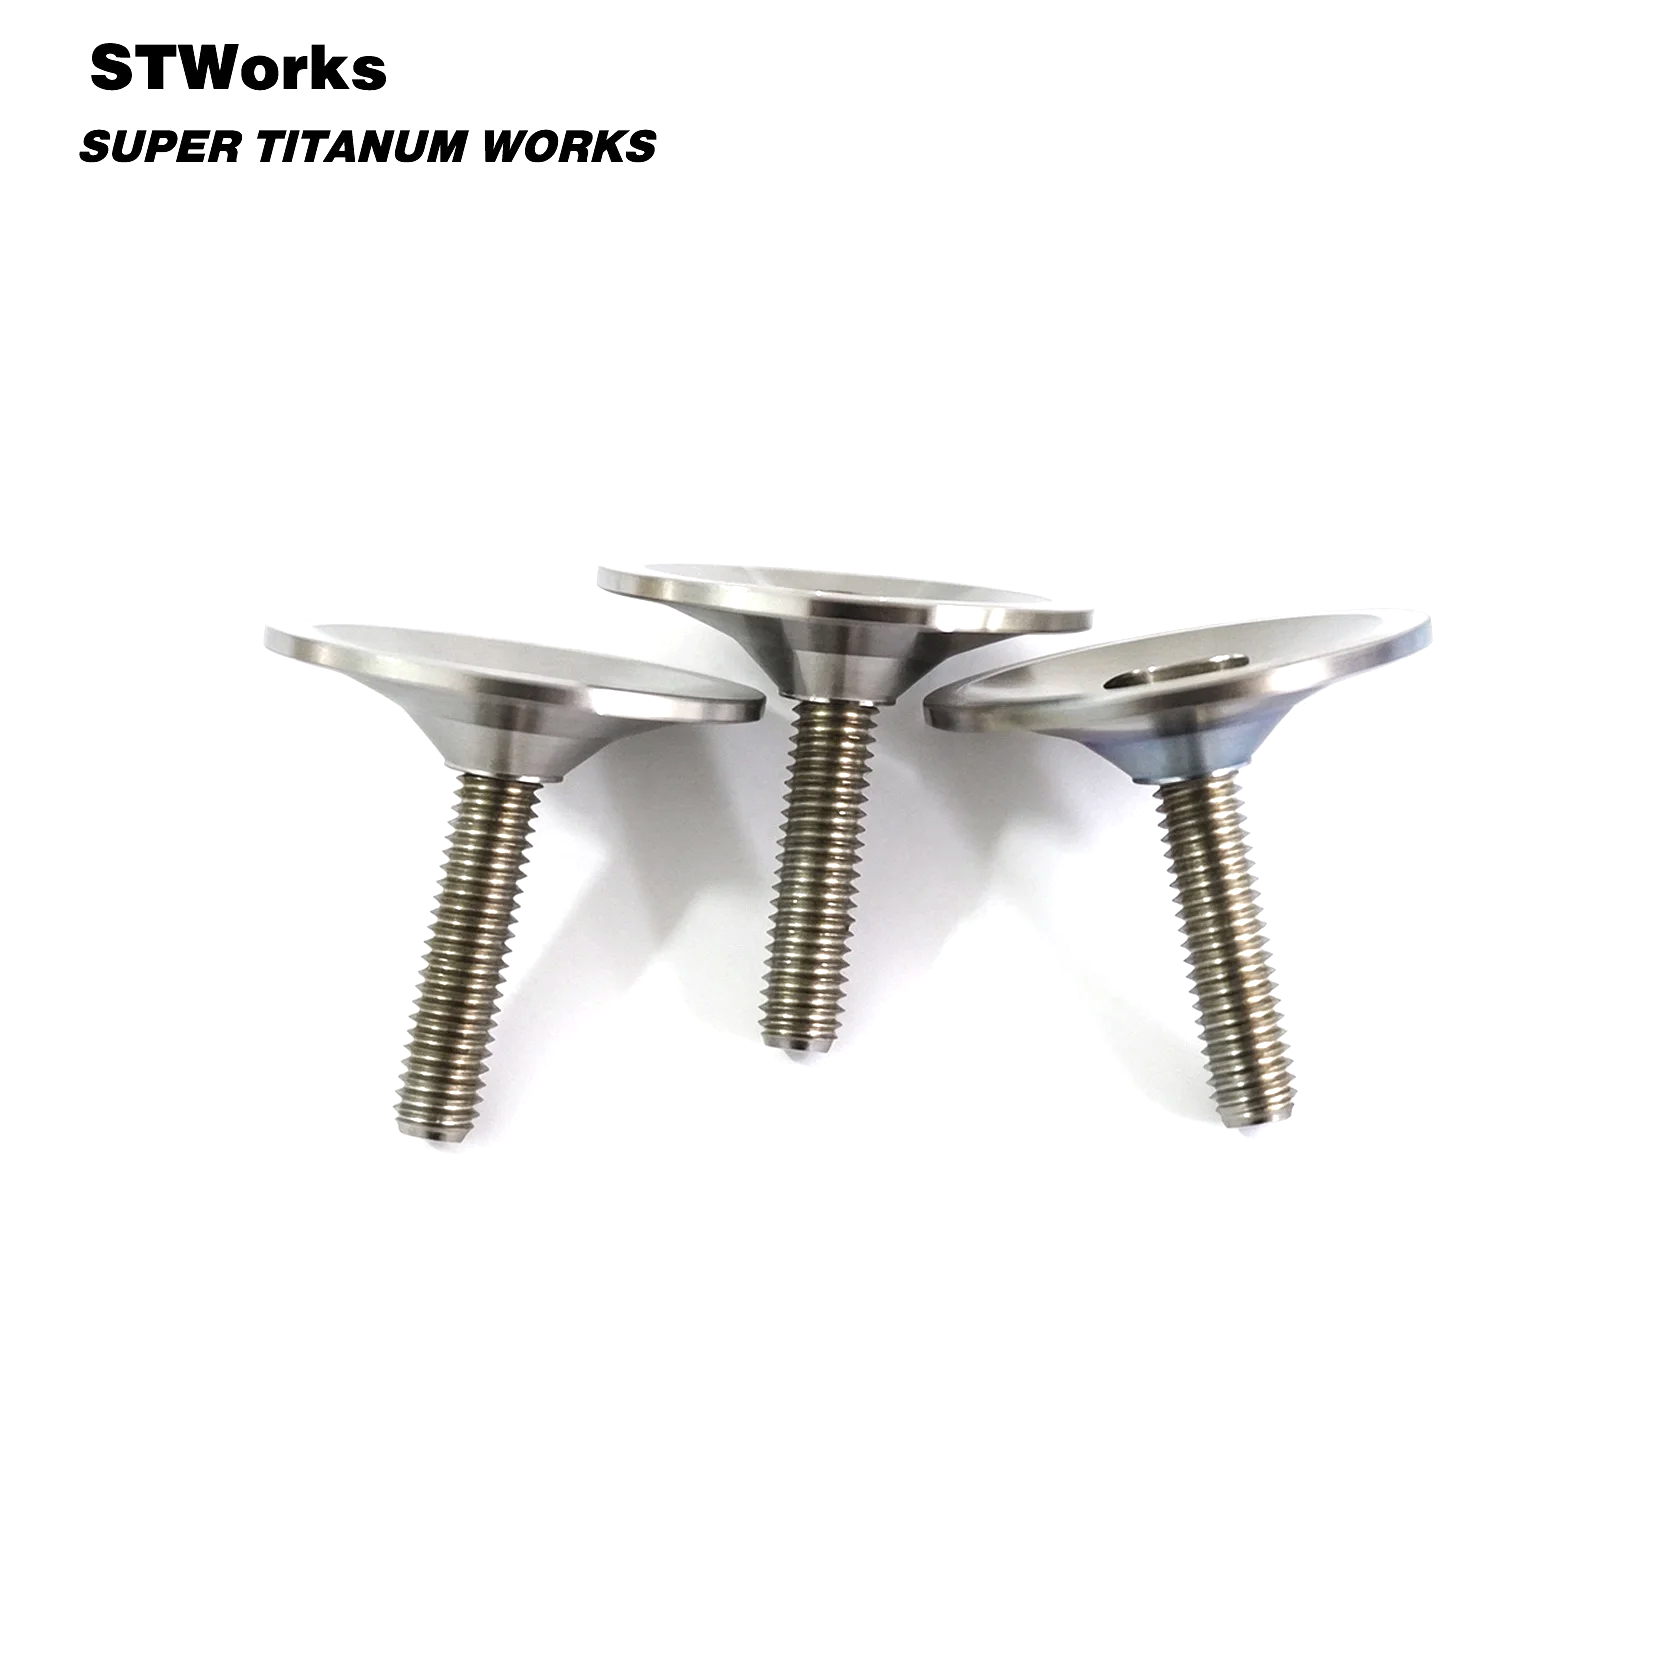
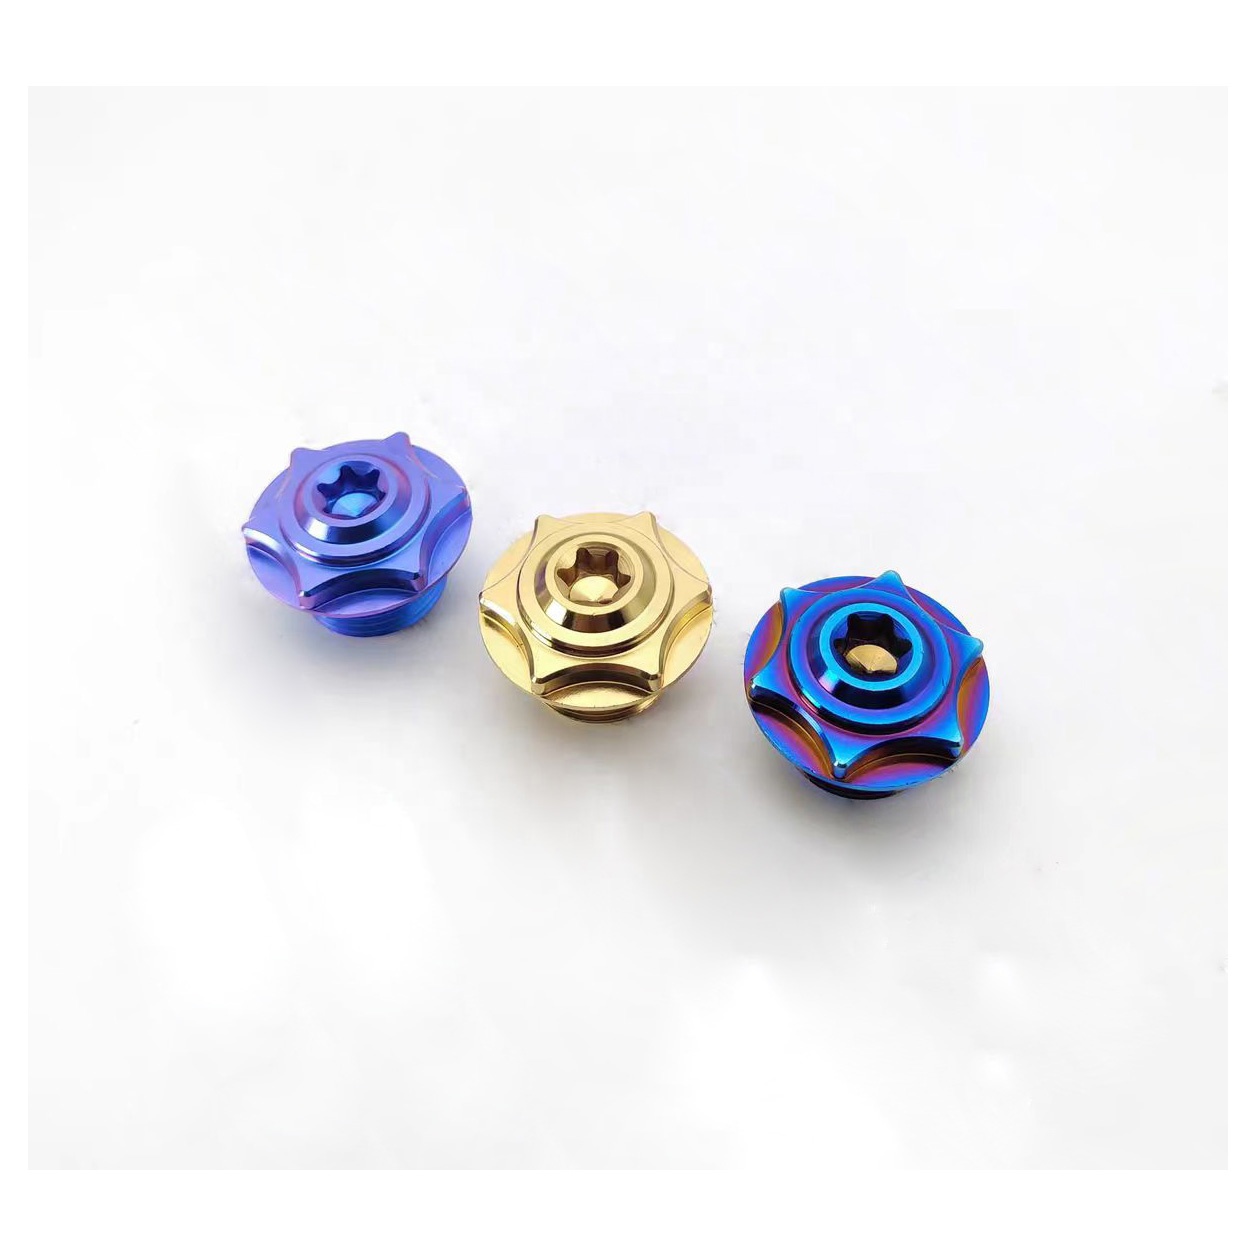
Precision Architecture of Titanium Headset Spacers
In modern high-performance bicycles, headset spacers are load-bearing structural interfaces directly influencing steering compliance, steerer tube life, and bearing preload retention under high fatigue cycles.
Why Titanium Outperforms Aluminum and Carbon Fiber Spacers
While standard consumer bicycles often rely on punched 6061-T6 aluminum rings or molded carbon composite spacers, performance-driven OEMs and custom frame builders specify CNC-machined titanium for three critical mechanical reasons:
- Absolute Compression Parallelism: CNC-lathed end faces within ±0.01mm ensure angular cocking against headset angular contact bearings is completely eliminated.
- Zero Creep & Micro-Crush: Unlike resin-bonded carbon fiber that can suffer micro-delamination under continuous stem clamp torque (5–8 Nm), titanium maintains strict dimensional stability.
- Electrochemical Non-Reactivity: When properly passivated or PVD treated, titanium prevents galvanic corrosion against aluminum stems and carbon fiber steerers.
Velnora manufactures spacers using both Grade 9 (Ti-3Al-2.5V, CWSR seamless tube) for ultralight, thin-wall cylindrical configurations and Grade 5 (Ti-6Al-4V) billet for complex aerodynamic cable-routing geometries.
| Material Specification | Yield Strength (MPa) | Tensile Strength (MPa) | Elastic Modulus (GPa) | Density (g/cm³) | Axial Preload Stability | Galvanic Safety (Carbon) |
|---|---|---|---|---|---|---|
| Grade 9 Titanium (Ti-3Al-2.5V CWSR) | ≥ 620 | ≥ 725 | 105 | 4.48 | Exceptional (Zero Relaxation) | High (Native Oxide Film) |
| Grade 5 Titanium (Ti-6Al-4V TC4) | ≥ 825 | ≥ 895 | 114 | 4.43 | Maximum (Heavy Impact Proof) | High (Passivated) |
| 6061-T6 Aluminum Alloy | ≈ 276 | ≈ 310 | 69 | 2.70 | Moderate (Subject to Brinelling) | Low (Severe Galvanic Risk) |
| Toray T700 Carbon Fiber Prepreg | N/A (Anisotropic) | ≈ 600 (Hoop) | ≈ 80 | 1.55 | Low (Resin Creep Under Preload) | Neutral (Matrix Dependent) |
| 316L Stainless Steel | ≥ 220 | ≥ 520 | 193 | 8.00 | High | Moderate |
CE Certification & EN ISO 4210 Compliance Standards
In the European and North American markets, structural cockpit hardware must adhere strictly to international safety mandates to prevent catastrophic steering failure under dynamic cyclic stress.
EN ISO 4210-2 & 4210-5 Testing
Our titanium headset spacers undergo rigorous axial compression tests exceeding 15,000 N and dynamic steering stem fatigue tests without structural deflection, wall buckling, or bearing ring indentation, exceeding the standard safety margins required for road racing and downhill MTB applications.
Full CE Conformity Declaration
Each production batch is supplied with an official Declaration of Conformity (DoC) and certified EN 10204 3.1 Material Test Reports (MTR). This enables OEM bicycle manufacturers in the European Union to seamlessly incorporate our components into their CE marked complete bike assemblies.
Aerospace Chemical Traceability
All titanium ingots are procured with 100% melt-origin verification from state-certified titanium producers in Baoji, China. Chemical composition (Fe, O, C, N, H impurity limits) and microstructural alpha-beta grain morphology are verified via spectral optical emission analysis before turning.
Why Tier-1 Bicycle Brands Partner with Velnora Titanium
Founded in 2013 in Baoji—known globally as "China’s Titanium Valley"—Velnora Titanium Industry Co., Ltd. combines advanced Japanese multi-axis CNC lathes, in-house metallurgical testing, and agile contract manufacturing.
Digital Transparency: Production Video Verification
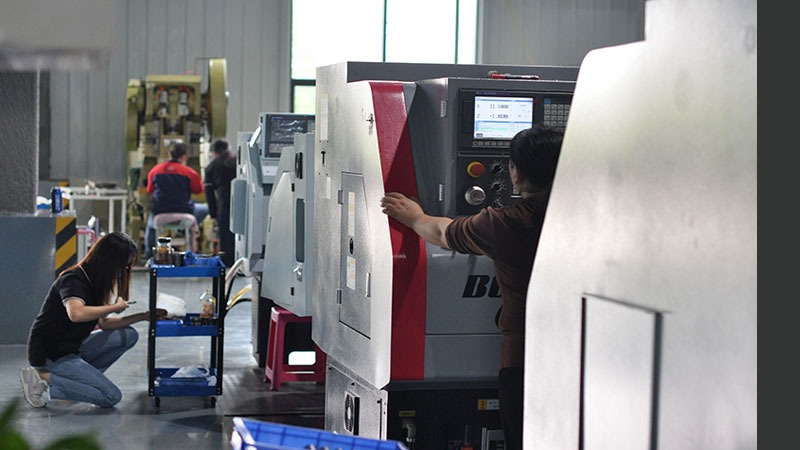
We believe international procurement should be completely free of surprises. Velnora maintains an active library of over 900 verified component production videos, allowing international procurement managers to observe live CNC machining, chamfering, ultrasonic degreasing, and laser etching procedures.
During sample manufacturing and bulk production runs, our quality team transmits milestone inspection footage and dimensional coordinate measurement machine (CMM) data directly to the client before packing and dispatch.
Future Procurement Trends in Titanium Cycling Hardware (2025–2030)
The cycling industry is witnessing unprecedented architectural shifts toward integrated aero cockpits, electronic shifting, and severe weight optimization. Sourcing managers must plan for the following evolutions:
1. Fully Integrated Internal Cable Routing (ICR)
Traditional round 1-1/8" cylindrical spacers are rapidly transforming into aerodynamic teardrop, truncated airfoil, and D-shaped profiles featuring dedicated internal cavities for brake hydraulic hoses and electronic Di2/AXS wiring. Multi-axis CNC milling and interlocking tongue-and-groove alignment pins are now standard OEM requirements to prevent rotation during high-torque sprints.
2. Selective Laser Melting (SLM 3D Printing) Hybrids
Additive manufacturing using Grade 5 titanium powder allows internal hollow lattice networks (cellular gyroid structures) that cannot be machined via subtractive turning. This results in a 35% weight reduction while preserving the full compressive modulus required by EN ISO 4210 standards. Velnora is pioneering hybrid workflows combining SLM additive printing with CNC precision-faced seating ends.
3. Ultra-Durable PVD Thin-Film Coatings
Traditional thermal and electrochemical anodizing creates vibrant colors via optical wave interference, but can experience fading when subjected to strong UV radiation or aggressive degreasers. Future B2B purchasing is heavily shifting toward Physical Vapor Deposition (PVD) titanium nitride (TiN) and diamond-like carbon (DLC) coatings, providing scratch hardness exceeding 2,500 Vickers with permanent colorfastness.
B2B Procurement & Engineering FAQ
Direct technical and commercial answers designed to streamline supplier qualification and specification reviews for purchasing teams and bike engineers.
What are the key standard dimensions available for titanium headset spacers?
How do you guarantee that titanium spacers will not damage carbon fiber steerer tubes?
What surface finish options are provided for private-label OEM brands?
What documentation is supplied to verify CE certification and material compliance?
What are the minimum order quantities (MOQ) and production lead times for custom tooling?
Can titanium spacers gall or cause crevice corrosion when exposed to wet conditions?
Ready to Engineer Custom Titanium Spacers for Your Bike Range?
Submit your 2D engineering drawings (PDF/DWG) or 3D CAD files (.STEP / .IGES). Our senior manufacturing engineers in Baoji will evaluate tolerances, weight-saving fluting, and PVD options with a binding quotation within 4 hours.