Gr5 Anodized
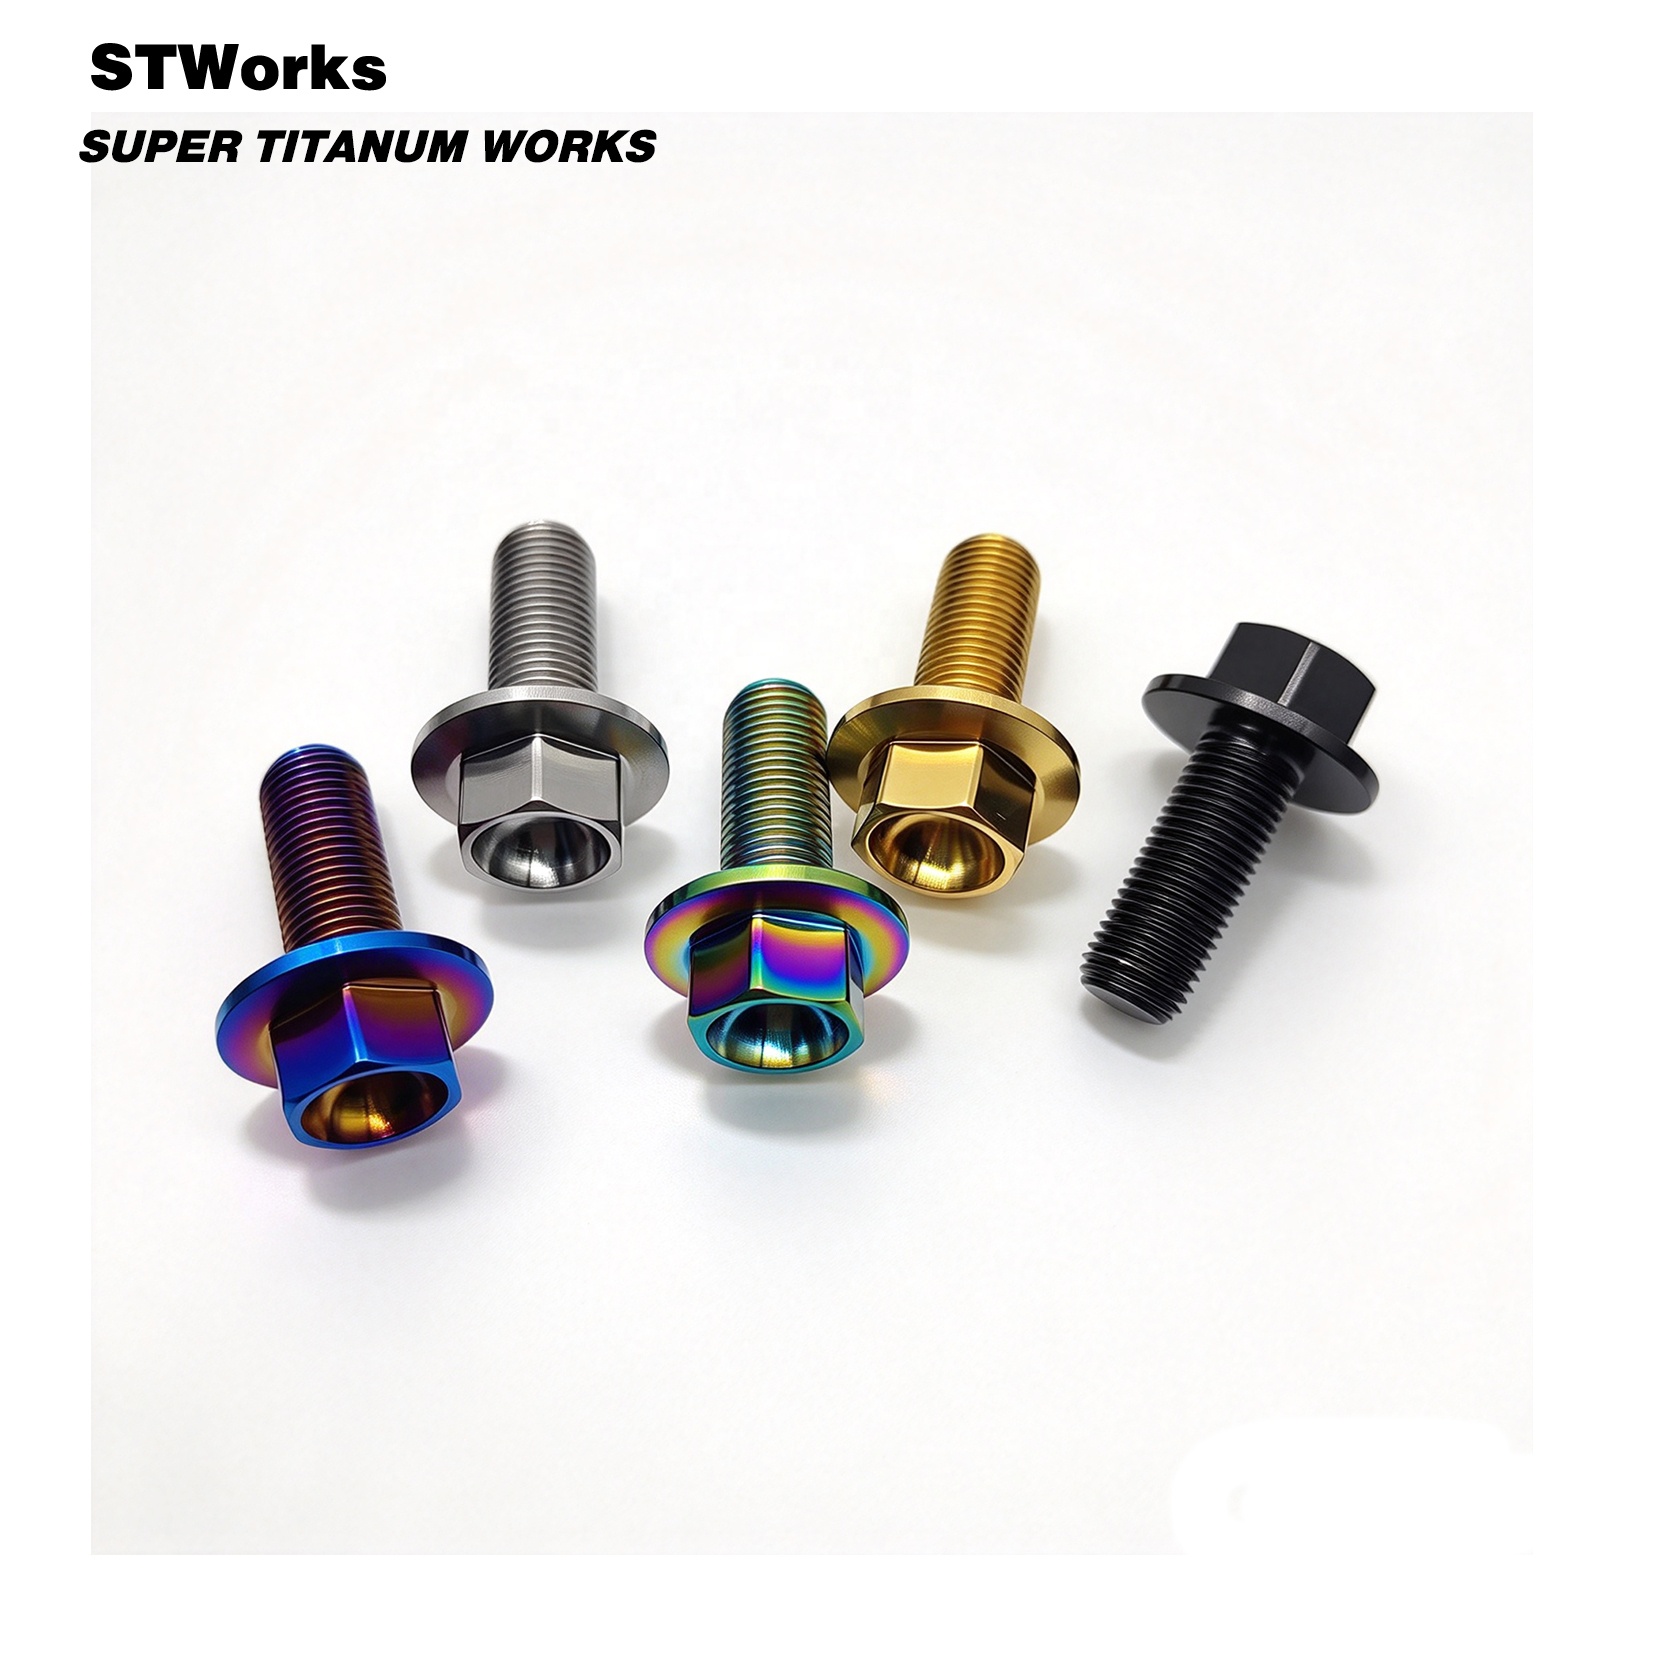
Direct from our specialized Baoji machine park: every item represents high-precision multi-axis CNC milling, high tensile integrity, and biocompatible surface finishing calibrated for high-stress duty.

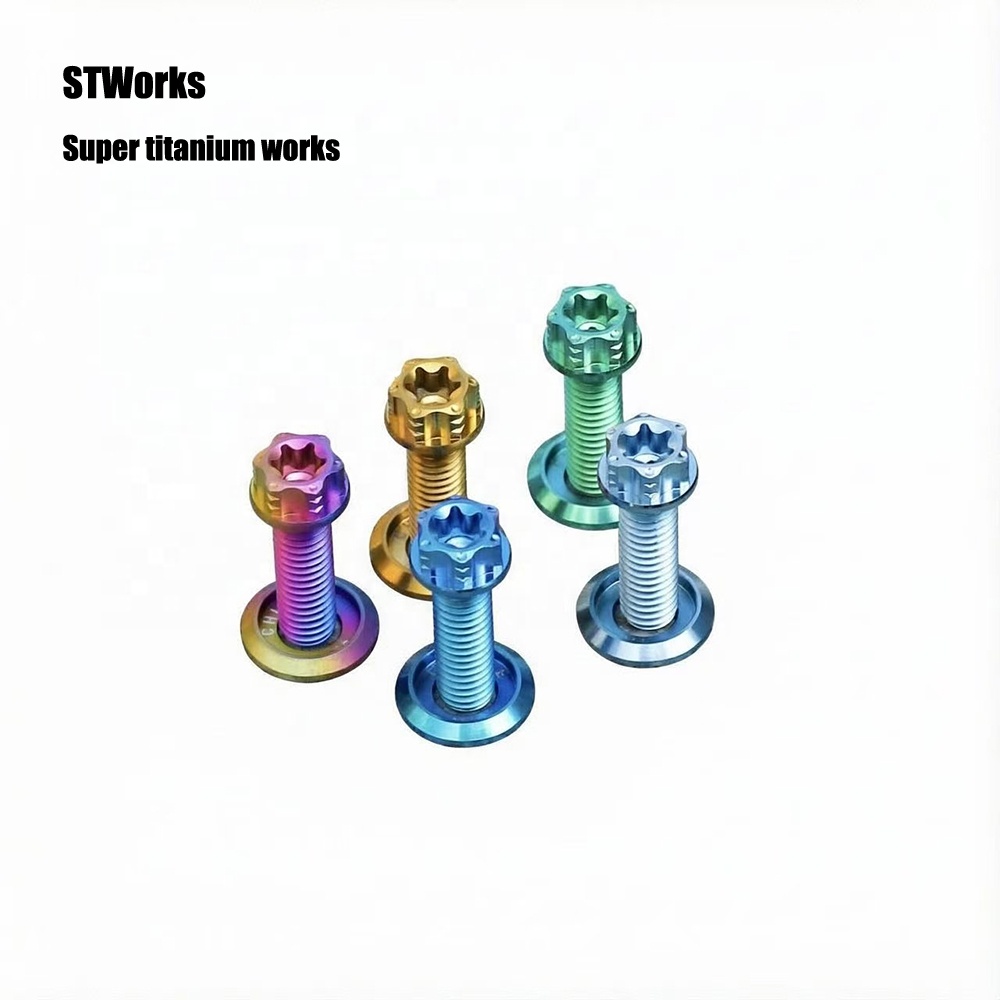
For tactical gear manufacturers, luxury apparel brands, and safety harness converters, selecting the proper grade of titanium hardware directly impacts mechanical dependability, user dermatological safety, and regulatory compliance across global export zones.
Traditional zinc alloy (Zamak) die-cast buckles and generic plated steel hardware suffer from catastrophic brittle fracture under shear loads and rapid corrosion in saline or sweaty environments. By contrast, Grade 5 Titanium (Ti-6Al-4V, UNS R56400 / TC4) exhibits a minimum tensile strength of 895–950 MPa and a yield strength exceeding 828 MPa, delivering an exceptional strength-to-weight ratio that is approximately 44% lighter than stainless steel yet mechanically robust enough to withstand ballistic webbing pull-stresses exceeding 15 kN.
As an authoritative manufacturer based in Baoji—widely acknowledged as China’s Titanium Valley—Velnora Titanium Industry Co., Ltd. machines monolithic unibody and multi-link belt buckle mechanisms directly from vacuum-arc remelted (VAR) certified aerospace billets, eliminating internal casting voids, micro-fissures, and weld-joint vulnerabilities.
Our manufacturing processes align with the essential health and safety mandates of EU PPE Regulation (EU) 2016/425 for structural harness components, Machinery Directive 2006/42/EC for quick-release load latches, and REACH Annex XVII for hazardous chemical restrictions.
Direct empirical comparison of belt buckle hardware materials. Evaluate structural load capabilities, density savings, and biological compatibility prior to finalized OEM drawing submission.
| Performance Characteristic | Gr5 Titanium (Ti-6Al-4V) | Gr2 Pure Titanium | 316L Stainless Steel | 7075-T6 Aerospace Al | Zamak 5 (Zinc Die-Cast) |
|---|---|---|---|---|---|
| Density (g/cm³) | 4.43 (Lightweight) | 4.51 | 8.00 (Heavy) | 2.81 | 6.60 |
| Tensile Yield Strength (MPa) | ≥ 828 – 920 | ≥ 275 – 350 | ≥ 220 – 310 | ≥ 503 | ≥ 250 (Brittle) |
| Ultimate Tensile Strength (MPa) | ≥ 895 – 1000 | ≥ 345 | ≥ 520 – 680 | ≥ 572 | ≥ 330 |
| Skin Biocompatibility (REACH / EN 1811) | 100% Bio-Inert, Zero Ni | 100% Bio-Inert, Zero Ni | Trace Nickel Leaching Risk | Skin Oxidation Staining | High Sensitization Risk |
| Salt Fog Resistance (ASTM B117) | > 2,000 Hours (Immune) | > 2,000 Hours (Immune) | Pitting after 400–600h | Pitting/Exfoliation Corrosion | Rapid White Rust Oxidation |
| Magnetic Permeability (μr) | 1.00005 (Non-Magnetic) | 1.00004 (Non-Magnetic) | 1.008 (Slightly Magnetic) | 1.00002 (Non-Magnetic) | Non-Magnetic |
| Primary Application Fit | Mil-Spec Riggers, EDC, Luxury | Hypoallergenic Casual Belts | Standard Marine Fittings | Low-Stress Tactical Webbing | Cheap Fast-Fashion Buckles |
Since 2013, our production facility in Baoji’s Jinhe Precision Industrial Park has engineered custom titanium hardware for clients across North America, Europe, Japan, and Australia.
Equipped with high-precision CNC machining centers, wire EDM slicing, and Swiss-type turning machines capable of sustaining micro-tolerances down to ±0.005 mm on pivot axles, tongue catches, and quick-release spring latches.
Every titanium bar stock delivery is accompanied by verified EN 10204 Type 3.1 chemical spectrometry and mechanical tensile test reports. Thread geometries are validated using optical shadowgraphs and coordinate measuring machines (CMM).
Buyers never face blind production cycles. Our team provides high-definition video walkthroughs and CNC run footage of your exact batch machining, surface anodizing, and load testing prior to international palletization and air dispatch.
Beyond commercial Grade 5 and Grade 2 titanium, our workshop specializes in diffusion-bonded Timascus (layered Damascus titanium). Each piece showcases unique damascene flame grain patterns for high-end bespoke luxury collections.
We convert customer IGES, STEP, DXF, or PDF engineering concepts into physical prototypes within 7 to 10 days. Options include micro-bead blasting, PVD diamond-like carbon (DLC), multi-voltage anodizing, and fiber laser engraving.
Direct communication with experienced technical tooling engineers. With a historical 95.7% prompt response rate, your CAD reviews, material certification requests, and shipping quotation inquiries are processed within hours.
Procurement directors and product line executives must navigate changing supply chain dynamics, stricter environmental directives, and advancing micro-machining capabilities.
High-end technical apparel and military operators increasingly mandate sub-40 gram buckle architectures. Advances in 5-axis trochoidal high-speed milling permit hollowed-out internal geometry without reducing safety break-strengths below 10 kN.
With tightening enforcement of European REACH Annex XVII regulations regarding nickel release in items having direct, prolonged skin contact, luxury houses are phasing out electroplated zinc and brass hardware entirely in favor of unalloyed Ti and Grade 5.
Traditional toxic wet-plating chemical baths are being superseded by physical vapor deposition (PVD). Diamond-Like Carbon (DLC) yields surface hardness exceeding 3,000 HV, offering extreme scratch resistance in tactical matte black, bronze, and rainbow finishes.
Enterprise defense contractors and industrial safety brands now mandate lot-traceable digital documentation directly tied to titanium raw sponge heat numbers. Single-source provenance from Baoji provides unadulterated quality security against recycled scrap titanium.
The market is pivoting rapidly from traditional hole-and-prong mechanisms toward gear-driven, track-locking ratchet buckles. CNC micro-machining of titanium internal pawls prevents teeth rounding and guarantees lock stability over 100,000+ cycle engagements.
For complex architectural buckle concepts, direct metal laser sintering (DMLS) 3D printing in Ti-6Al-4V combined with post-sinter CNC finishing of mating faces is emerging as a commercially viable approach for low-run artisan luxury editions.
Clear, definitive technical clarifications addressing metallurgical properties, structural load ratings, tooling lead times, and global shipping policies.
Every commercial production batch is supported by a comprehensive technical documentation pack. This includes an authentic EN 10204 Type 3.1 Inspection Certificate confirming chemical spectrometry and mechanical physical test values (yield strength, elongation, tensile break), third-party laboratory verification of compliance with REACH Annex XVII (EN 1811 Nickel Release standard ≤ 0.5 μg/cm²/week), and Certificate of Conformity under EU PPE directives for structural tactical buckles.
While Grade 2 commercially pure titanium is exceptionally corrosion-resistant and cost-effective, its tensile yield strength is modest (≈ 275–350 MPa). Under severe lever-arm moments or sudden webbing tension (such as tactical rapelling or tool-loaded duty belts), Grade 2 can undergo plastic deformation. Grade 5 titanium offers more than double the yield strength (≥ 828 MPa), ensuring that buckle frames, prongs, and internal quick-release spring latches maintain structural integrity without bending or binding.
Titanium alloys have a natural tendency to gall when two unlubricated mating surfaces experience friction under high torque. We mitigate this through several precision engineering methods: rolled threads rather than cut threads where possible, high-precision Ra ≤ 0.4 μm surface polishing, anti-friction PVD DLC coatings, and the recommendation of titanium-compatible molybdenum disulfide (MoS&sub2;) or fluoropolymer assembly compounds during final customer webbing installation.
For bespoke CNC machined designs created directly from customer 3D CAD files (STEP/IGES), our standard production MOQ is typically 100 to 300 pieces, depending on structural geometry and surface finish complexity. For rapid prototyping and initial proof-of-concept sampling, we accommodate small pilot runs of 10 to 50 pieces. Specialty Timascus (Mokuti) luxury custom items can be ordered starting from 1 piece.
Titanium anodization is an electro-chemical oxidation process that grows a controlled, transparent titanium dioxide (TiO&sub2;) film on the metal’s surface. By calibrating the bath voltage from 12V to over 100V, the oxide layer thickness precisely varies between 20 nm and 300 nm. Incident light reflects off both the outer oxide film and the underlying substrate, creating interference colors (bronze, purple, deep blue, gold, rose, or green). Because no organic pigments are utilized, the color will not peel, chip, or flake into clothing fibers.
Yes. When engineered specifically for industrial safety harnesses, tactical riggers belts, or tree-climbing saddles, our heavy-duty quick-release buckle mechanisms undergo destructive static tensile pull-testing. We design and manufacture custom cross-sections capable of exceeding 15 kN to 18 kN (≈ 3,370 to 4,045 lbf) straight-line pull tests without latch disengagement or structural shear failure.
Our engineering team works seamlessly with standard industrial 3D vector and solid modeling formats including STEP (.stp), IGES (.igs), Parasolid (.x_t), and SolidWorks (.sldprt). For dimensional tolerance specifications, thread callouts, and surface texture annotations, please also supply a corresponding 2D engineering drawing in vector PDF or DWG format.
Tooling setup and rapid prototype samples are completed within 7 to 10 working days. Upon sample sign-off and receipt of production deposit, standard mass CNC machining runs (500–2,000 units) require approximately 18 to 25 calendar days. For urgent global delivery, we partner with DHL Express, FedEx Priority, and air freight forwarding to reach European and American hubs within 3 to 5 transit days.
Yes. Our in-house fiber laser marking systems deliver high-definition microscopic engraving for brand logotypes, batch serial numbers, and custom tactical QR codes. Additionally, our 4-axis and 5-axis CNC machining centers can carve custom diamond knurling, organic texturing, or tactile grip patterns directly onto outer buckle bevels.
Quality assurance follows strict ISO 9001 protocols. Each production lot undergoes 100% aesthetic inspection for tool marks, burrs, or anodizing color variations, followed by AQL 1.0 statistical CMM dimensional verification. Before final bubble wrapping and vacuum export packing, we send full batch inspection videos and photographs directly to your procurement manager for final dispatch authorization.
Send your 2D/3D drawings, webbing slot dimensions, finish specifications, and annual volume requirements directly to our engineering desk. Receive an authoritative feasibility review and competitive factory direct quotation within 4 hours.